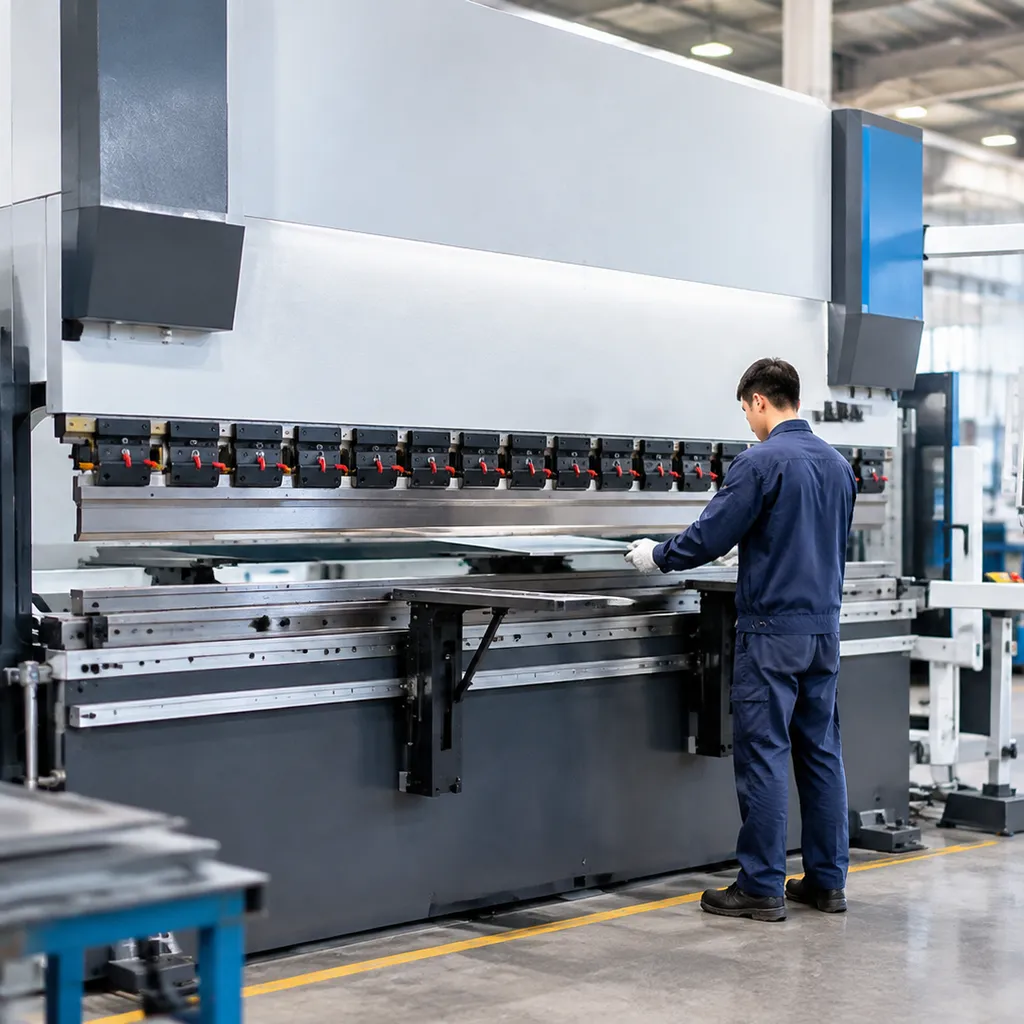
Formula details
Product Details
Overview
Why Choose Our 6 Axis CNC Press Brake Bending Machine?
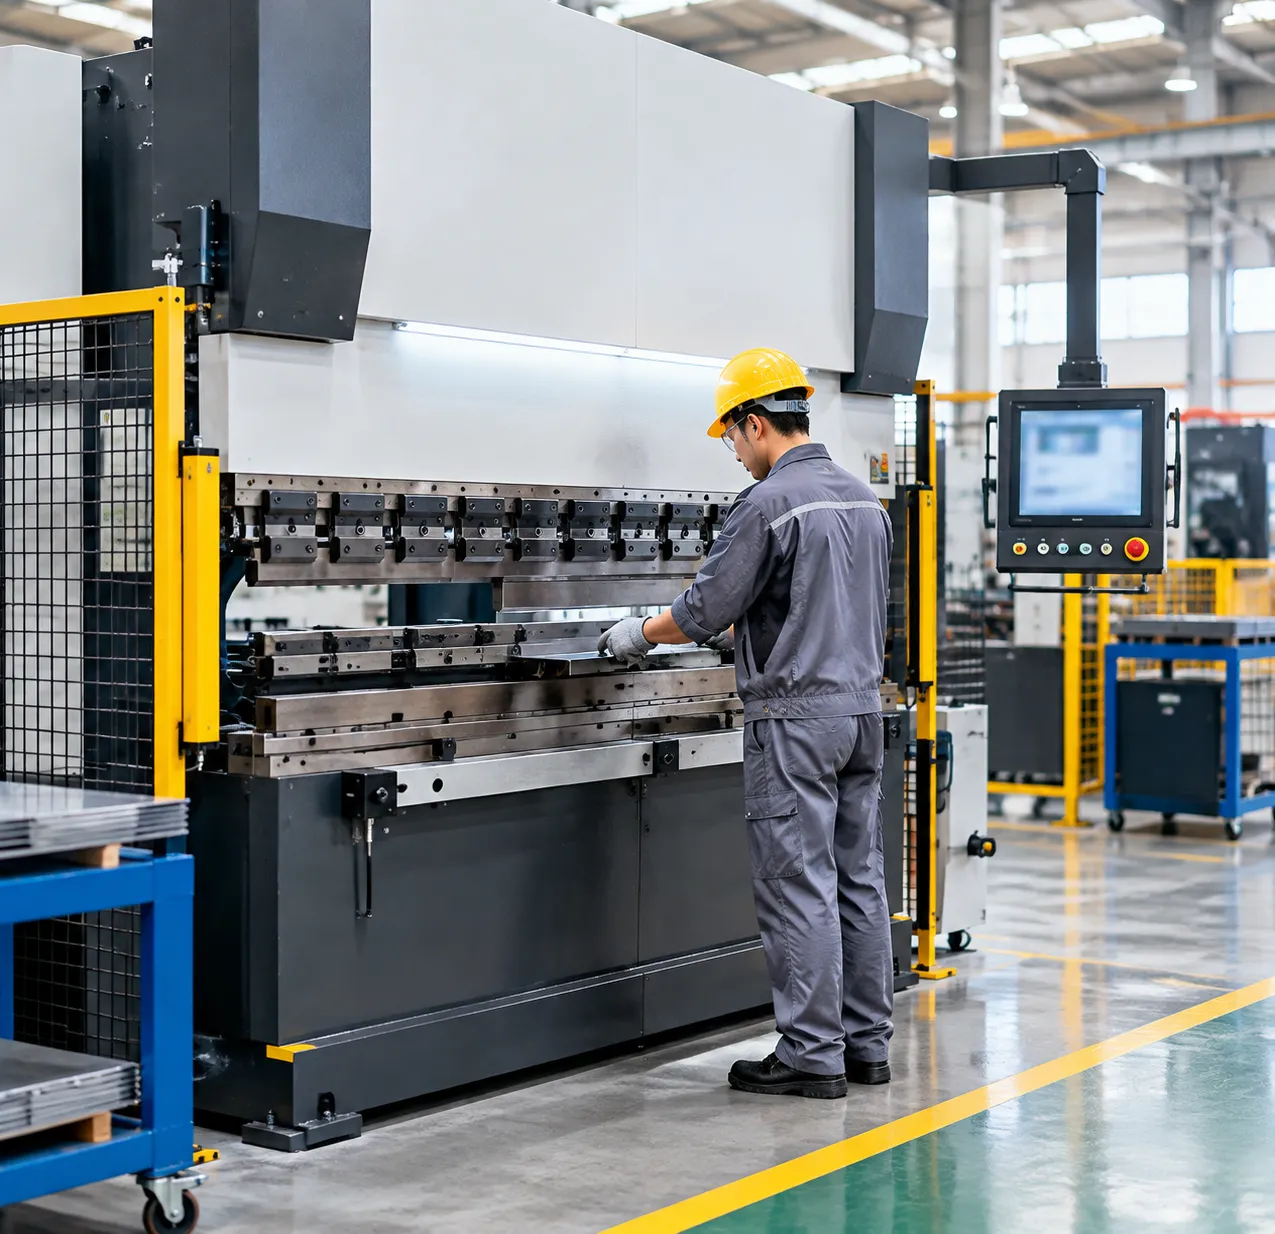
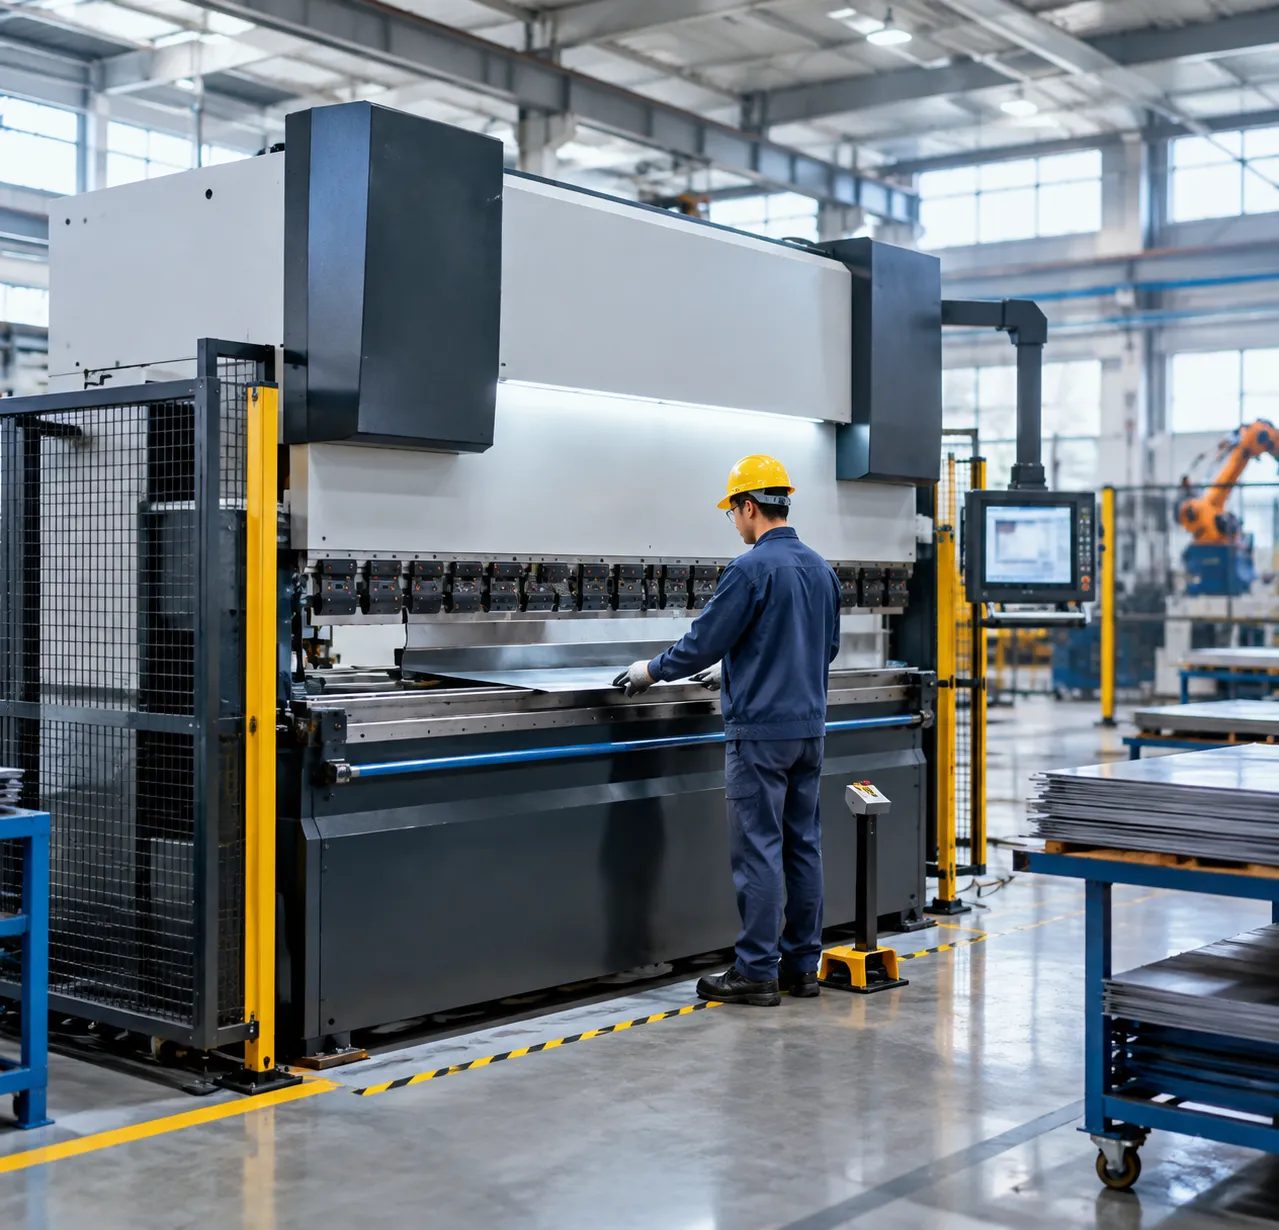
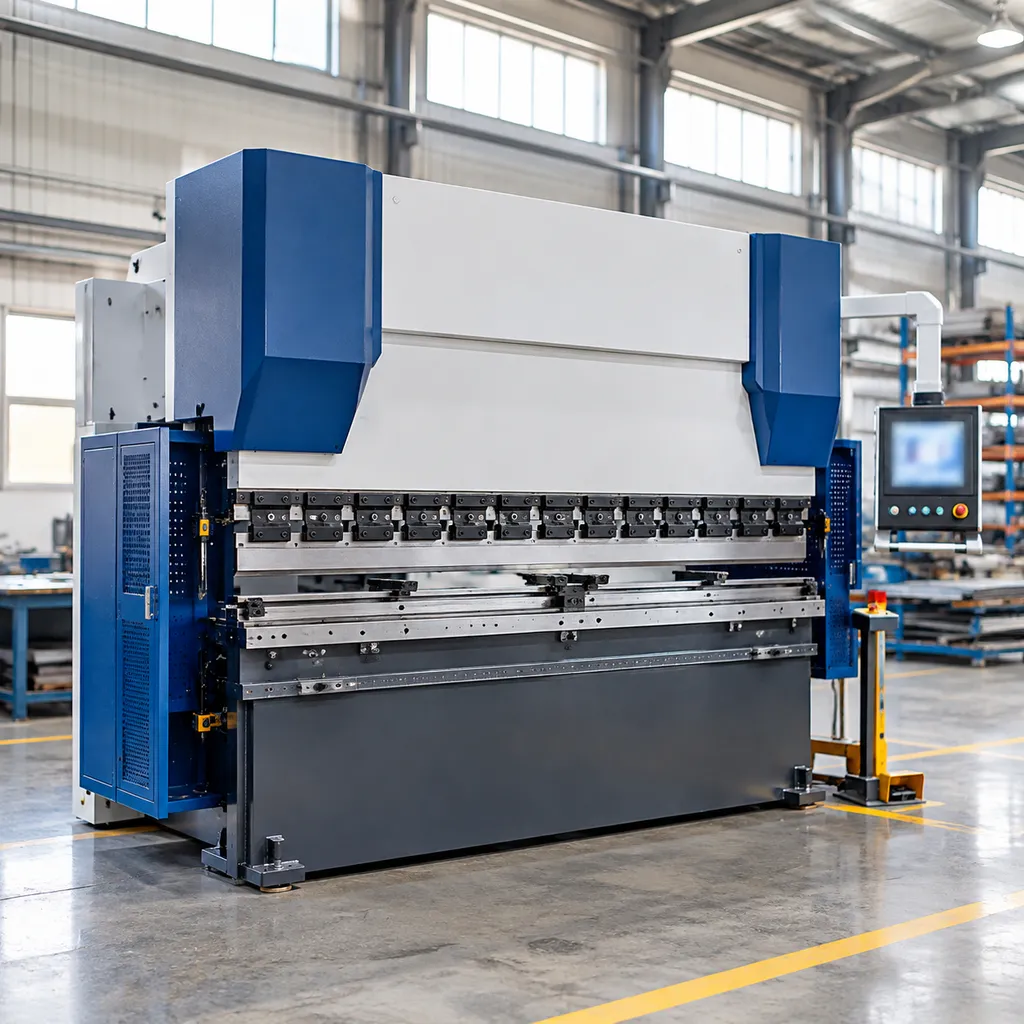
Sheet metal fabricators constantly fight three bottlenecks: slow backgauge positioning between steps, angle deviation on off-center loads, and endless test bends on custom jobs. As a specialized 6 axis cnc press brake manufacturer and direct cnc press brake bending machine factory, we eliminate these production losses through precision motion engineering, dynamic hydraulic balancing, and rigid structural design.
Full Ram Synchronization for Complex Multi-Step Bends
Our machines utilize independent dual-cylinder control via electro-hydraulic proportional valves to drive the Y1 and Y2 axes. This system monitors and corrects ram tilt in real time, delivering consistent angle accuracy even under severe off-center bending loads.
-
- Closed-loop optical feedback: Linear optical encoders continuously monitor the position of both sides of the ram, holding synchronization tolerances within ±0.01 mm.
- Off-center loading capability: Handle progressive tooling setups, staggered dies, and asymmetric parts along the full table length without frame distortion or uneven angle depth.
- Deep multi-step sequences: Complete complex multi-bend geometries, closed boxes, and narrow reverse flanges in a single uninterrupted work cycle.
Zero Setup Delays on High-Mix Sheet Metal Jobs
High-mix, low-volume sheet metal processing demands instant adaptation. Our multi-axis backgauge assemblies to eliminate manual tape measurements, gauge block adjustments, and manual finger realignment.
-
- Automated multi-axis backgauge: High-speed servo motors drive the gauge fingers instantly to programmed coordinates across X, R, Z1, and Z2 axes.
- Instant part changeover: Switch from narrow chassis components to deep industrial panels in seconds by recalling stored CAD/CAM programs directly at the CNC terminal.
- Zero trial-and-error scrap: Automated sequence calculations and mechanical crowning compensation prevent flange distortion and eliminate manual shimming on the first part.
| Production Factor | Standard 3 or 4-Axis Press Brake | Our 6-Axis CNC Bending Machine | Shop-Floor Benefit |
|---|---|---|---|
| Backgauge Motion | Linked X and manual R/Z positioning | Independent automated X, R, Z1, Z2 servo axes | Eliminates manual finger adjustments between bends |
| Asymmetric Bending | Risk of ram tilting and uneven angles | High-speed Y1/Y2 dual closed-loop sync | Permits off-center staged bending operations |
| Part Changeover Time | 15 to 30 minutes per profile | Less than 2 minutes via automated program recall | Maximizes machine uptime on small batch runs |
| Flange Consistency | Frequent manual shimming required | CNC-driven motorized crowning compensation | Delivers straight, uniform angles end-to-end |
Factory-Direct Quality Built from Raw Plate to Finished Machine
We maintain complete control over every stage of production at our 6 axis cnc press brake factory in China. Instead of outsourcing structural work, our engineering team manages the entire fabrication cycle in-house.
-
- Solid structural fabrication: Heavy steel plates are cut, fully welded, and thermally annealed in heat-treatment furnaces to eradicate residual internal stress before precision machining.
- Single-setup heavy machining: Machine frames and beds are milled on oversized CNC floor-type boring and milling machines in a single clamping setup, guaranteeing absolute alignment between guide rails, cylinders, and tooling slots.
- Factory-direct supply chain: Sourcing directly from our facility gives fabricators access to dependable industrial machinery, factory-level technical support, and transparent equipment costs without third-party dealer markups.
6+1 Axis Kinematics: How Our Motion Control Delivers Extreme Accuracy
Angle variation, flange mismatch, and part deflection eat away at shop productivity. We design our multi-axis drive geometry to remove manual intervention from every bending cycle. When you choose an electro-hydraulic synchronous CNC press brake forming machine for precise metal bending, true real-time axis synchronization ensures exact angles from the first stroke.
Dual-Axis Ram Synchronization (Y1 & Y2)
Ram movement depends on closed-loop feedback rather than hydraulic guesswork.
Direct Optical Linear Scales: Mounted to a separate C-frame on both side housings, high-resolution scales track the exact mechanical position of the beam, completely isolated from side-frame load deflection.
Proportional Valve Response: Dual independent cylinders automatically adjust flow dynamically, maintaining Y1/Y2 parallelism within ±0.01 mm even under off-center loading.
Unequal Bend Angles: Set different depths on Y1 and Y2 to form tapered flanges or compensate for asymmetric blank resistance without custom tooling.
Dynamic 6-Axis Backgauge Automation (X, R, Z1, Z2)
Our automated backgauge systems position sheet edges instantly across tight tolerances.
X-Axis Front-to-Back Servo Positioning: High-speed brushless servo motors and ground ball screws drive backgauge fingers precisely along hardened linear rails, eliminating mechanical backlash and hunting.
R-Axis Vertical Elevation: The gauge bar automatically steps up or down to support reverse bends, pre-bent downward flanges, and multi-die setups without manual height resetting.
Z1 & Z2 Independent Lateral Movement: Motorized gauge fingers slide side-to-side automatically across the machine width. They position themselves for narrow blanks, asymmetrical parts, and staggered stations without operator setup delays.
| Axis Name | Motion Vector | Working Accuracy |
|---|---|---|
| Y1 / Y2 | Left/Right Ram Cylinder Stroke | ±0.01 mm |
| X | Horizontal Front-to-Back Travel | ±0.02 mm |
| R | Vertical Finger Elevation | ±0.05 mm |
| Z1 / Z2 | Transverse Left-to-Right Spread | ±0.10 mm |
| V (Crowning) | Bed Deflection Compensation | CNC Dynamic Calculation |
Motorized Mechanical Crowning (The +1 Axis)
Under heavy tonnages, every press brake frame deflects naturally, causing canoe-shaped parts where center angles open up wider than the ends. Our cnc press brake bending machine manufacturer plant integrates a motorized dynamic wave crowning table:
Opposing Wedge Blocks: Dual-direction micro-convex wedges run along the full length of the lower bed.
CNC-Driven Curve Calculation: The controller calculates sheet thickness, tensile strength, and target angle to adjust the wedge curve before the punch contacts the sheet.
Consistent Angle Uniformity: Compensates directly along the bend line to maintain exact 90° bends from tip to tip without shimming dies.
Industrial Build: Heavy-Duty Steel Frame and Core Hydraulic Hardware
Annealed Stress-Relieved Steel Frame Eliminates Structural Flex
-
- Solid Monoblock Structure: Welded using high-strength structural plate steel, providing extreme torsional rigidity under full bending loads.
- Thermal Annealing Treatment: The entire frame undergoes controlled electric furnace stress relief to eliminate internal weld stresses, preventing frame twisting or angle distortion over decades of operation.
- Single-Setup Machining: Machined on giant five-face CNC gantry milling centers to ensure strict parallelism between the bed, ram guides, and cylinder mounts.
Bosch Rexroth Proportional Valves Provide Stable Hydraulic Pressure
We equip our CNC hydraulic press brakes with German-engineered Bosch Rexroth hydraulic systems to achieve ultra-responsive, closed-loop fluid control:
-
- Dual Proportional Valves: Direct, real-time micro-adjustments feed oil to each hydraulic cylinder independently, ensuring exact Y1/Y2 synchronization even during off-center multi-station bends.
- Low Noise and Cool Running: High-pressure gear pumps and low-friction seals prevent oil overheating during 24/7 shifts.
- High-Purity Piping Connections: Seamless cold-drawn tubing and flared O-ring face fittings eliminate hydraulic leaks and pressure drop.
Brushless Yaskawa Servo Drives and Schneider Electric Cabinet
Our cnc press brake bending machine factory uses top-tier electrical controls to ensure rapid multi-axis movement:
-
- Yaskawa High-Inertia AC Servos: Drive the X, R, Z1, and Z2 backgauge axes along dual-rail linear guides and precision ground ball screws for instant acceleration and vibration-free stops.
- Schneider Electric Controls: The IP54-rated, climate-controlled electrical enclosure features Schneider contactors, thermal relays, and circuit breakers designed to international CE and ISO safety codes.
- Integrated Safety Monitoring: Fast dual-channel safety relays communicate directly with the CNC system to halt ram motion instantly if safety curtains or emergency stops are triggered.
Smart CNC Controllers for 6 Axis Press Brake Automation
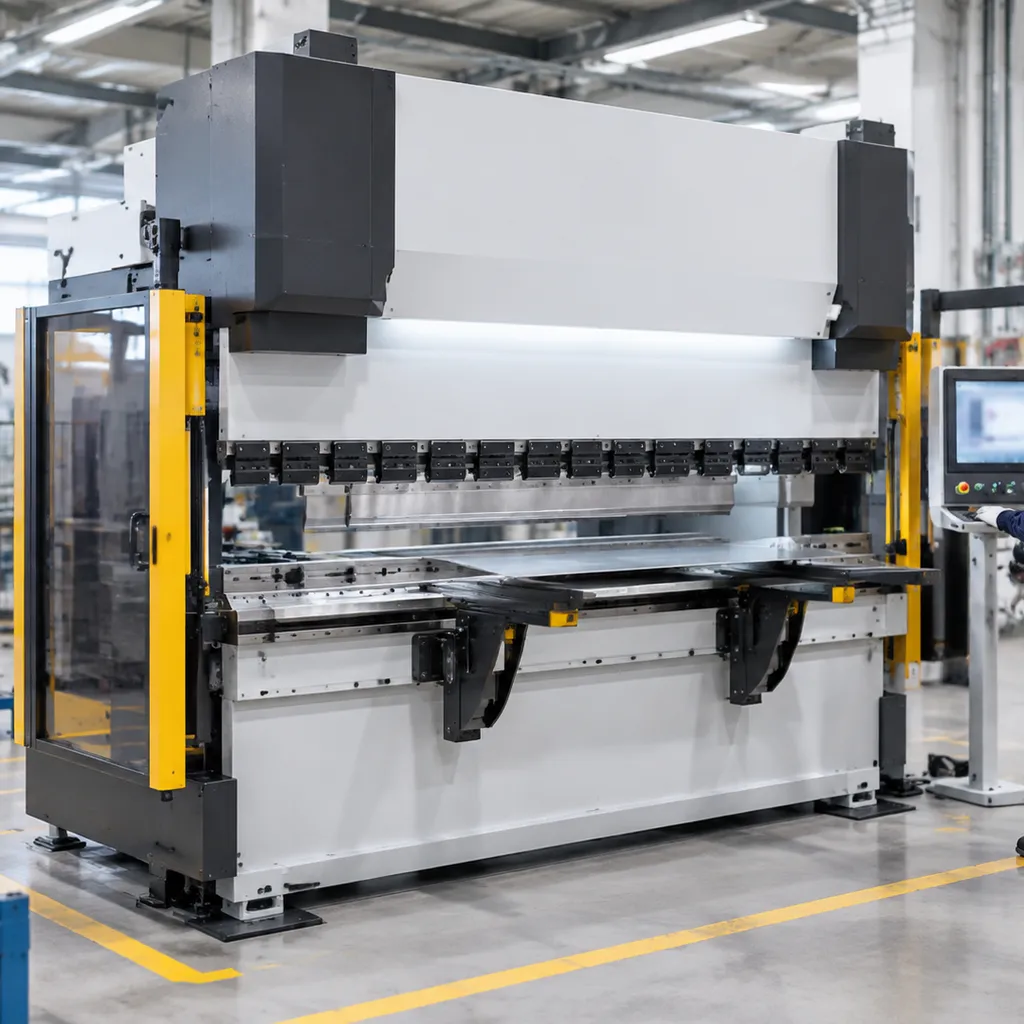
A multi-axis press brake needs a control interface that eliminates trial-and-error scrap. As an experienced cnc press brake bending machine manufacturer, we configure our systems with industrial-grade graphical interfaces that handle complex tooling layouts, multi-bend jobs, and dynamic axis calculation right out of the box. Understanding the leap in efficiency starts with reviewing the key differences between NC and CNC press brakes to see how graphic numerical control eliminates manual calculation errors on complex parts.
Delem DA-66T and DA-69T Touch Screens Generate 3D Bend Simulations
We fit our premium builds with native Dutch Delem systems to guarantee flawless axis synchronization:
-
- Delem DA-66T: Offers 2D graphical programming with real-time 3D part visualization, automated bend sequencing, and dynamic crowning calculation on a 17-inch high-resolution color touchscreen.
- Delem DA-69T: Upgrades to full 3D multi-touch programming and CAD/CAM importing, rendering sheet metal manipulation in real time for heavy-duty production lines.
- Instant Program Conversion: Direct DXF, STEP, and IGES file imports allow offline CAD-to-toolpath generation without holding up machine runtime.
Automatic Tool Collision Checks and Bend Sequence Optimization
Our delem da66t controller press brake configurations run automatic geometric checks before the upper beam moves a single millimeter:
-
- Interference Detection: Scans programmed paths against backgauge fingers, punch profiles, and lower dies to prevent machine crashes.
- Optimal Sequence Logic: Automatically calculates the most efficient bend order to reduce sheet rotations and operator handling fatigue.
- Angle and Crowning Compensation: Computes material springback and drives the mechanical crowning table automatically based on sheet thickness, tensile strength, and V-opening width.
Flexible Cybelec and ESA Numerical Control Alternatives
To match specific regional factory workflows, our 6 axis cnc press brake factory also installs proven alternative control units:
-
- ESA S660W / S675W (Italy): Renowned for robust 3D graphical processing, open Windows-based architecture, and seamless integration into automated robotic bending cells.
- Cybelec CybTouch & ModEva Series (Switzerland): Highly intuitive touch operation with advanced multi-axis backgauge kinematic calculation and rapid batch programming.
- Custom Software Integration: Every controller unit comes fully configured, pre-wired into the main cabinet, and calibrated to your exact axis setup before leaving our factory floor.
Standard 6 Axis CNC Press Brake Machine Parameters
As a dedicated 6 axis cnc press brake manufacturer, our factory builds machines designed to handle everything from thin precision sheet metal to heavy plate forming. We configure our standard cnc press brake bending machine line to balance high bending speeds, rigid deflection control, and consistent cycle accuracy.
Available Bending Capacity from 40 Tons up to 1000 Tons
Our manufacturing program covers light electrical cabinetry work up to heavy structural forming:
-
- Compact series (40T – 100T): Optimized for high-speed cycle rates, small brackets, and rapid job changes.
- Mid-range workhorses (135T – 320T): The shop standard for enclosures, automotive brackets, and general sheet fabrication.
- Heavy-tonnage models (400T – 1000T): Built with deep side frames to handle thick plate, hard-wearing structural steel, and high-tensile materials without structural strain.
Working Table Lengths from 1250 mm to 6000 mm
We manufacture standard bed lengths from 1250 mm up to 6000 mm, with custom tandem setups available for oversized profiles. Every bed is precision machined to ensure tight tolerances across the full bending width:
-
- Short-bed units (1250 mm – 2000 mm): Compact footprint, fast approach speeds, and reduced energy consumption.
- Standard-bed units (2500 mm – 4000 mm): Accommodate standard 4x8 ft and 5x10 ft commercial sheet sizes.
- Long-bed units (5000 mm – 6000 mm): Rigid dual-cylinder design engineered to prevent mid-bed angular deviation over long workpieces.
Strict ±0.01 mm Positioning and Repeatability Tolerances
Every electro-hydraulic synchronous press brake leaving our facility delivers reliable shop-floor accuracy:
-
- Ram Repeatability (Y1/Y2): ±0.01 mm, controlled via closed-loop glass scales.
- Backgauge Repeatability (X-axis): ±0.01 mm, driven by hardened ball screws and servo drives.
- Backgauge Elevation (R-axis): ±0.02 mm positional accuracy for stepped flanges.
- Finger Gauges (Z1/Z2): ±0.05 mm independent lateral positioning for asymmetrical sheet stops.
Standard Ram Stroke, Throat Depth, and Daylight Open Height Data
Our factory produces standard configurations designed to accommodate deep box bending, tall tooling sets, and large return flanges.
| Model Series | Nominal Force (Tons) | Bed Length (mm) | Daylight / Open Height (mm) | Ram Stroke (mm) | Throat Depth (mm) |
|---|---|---|---|---|---|
| HDP-60/2000 | 60 Ton | 2000 | 420 | 180 | 320 |
| HDP-100/3200 | 100 Ton | 3200 | 460 | 200 | 350 |
| HDP-160/3200 | 160 Ton | 3200 | 500 | 250 | 400 |
| HDP-250/4000 | 250 Ton | 4000 | 580 | 300 | 450 |
| HDP-400/5000 | 400 Ton | 5000 | 650 | 360 | 500 |
| HDP-600/6000 | 600 Ton | 6000 | 780 | 400 | 600 |
We also build extended daylight gaps and deep throats on demand to match your exact tooling libraries and clearance requirements. Check our complete inventory of industrial sheet metal bending machines built directly for global export.
Quick-Change Tooling and Clamping Options
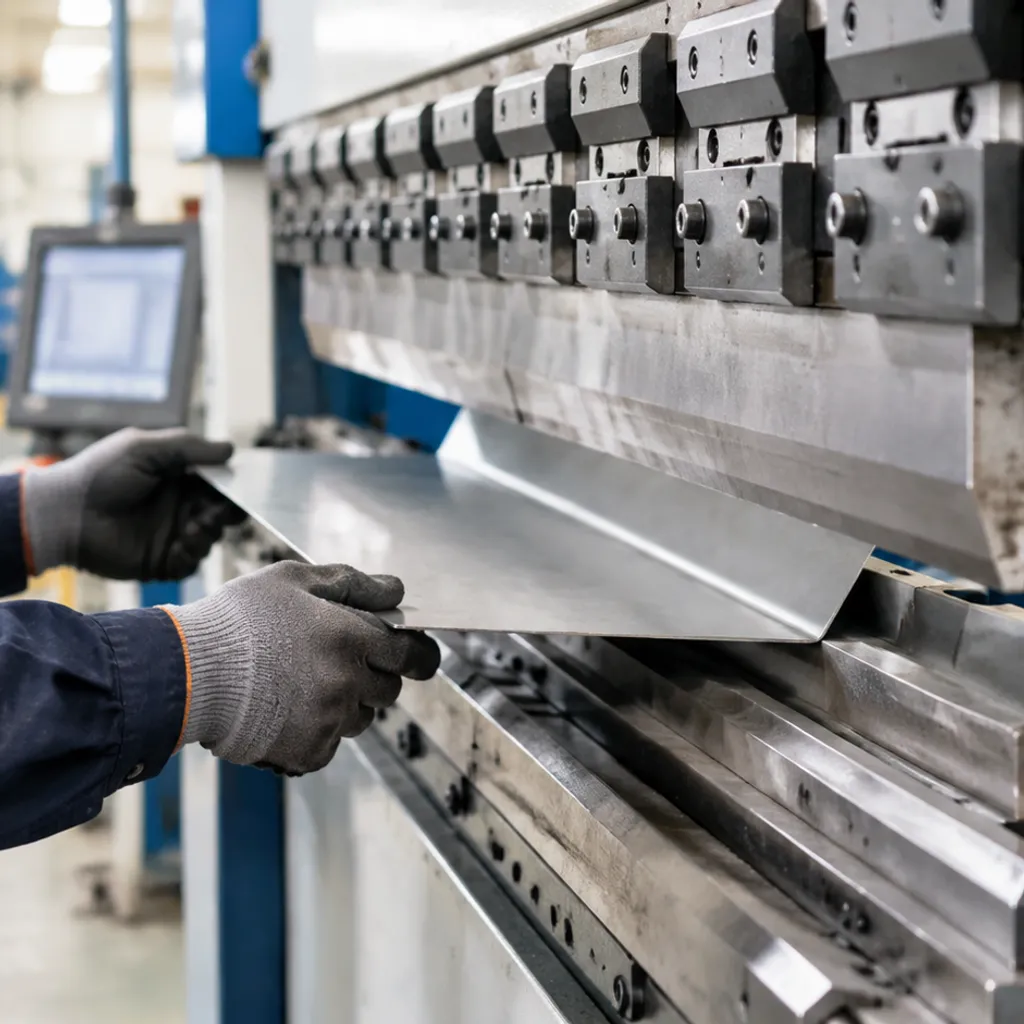
European and Amada Style One-Touch Punch Clamps
Our quick-release mechanical and pneumatic clamping systems eliminate manual bolt tightening along the upper beam.
-
- Vertical tool loading: Insert punches directly from the front without sliding them in from the side of the machine.
- Instant mechanical lock: One-touch levers seat and align punches squarely against the ram shoulder automatically.
- Universal fit: Fully compatible with standard European-style and Amada-type upper punch tangs.
- Hydraulic and pneumatic upgrades: Push-button clamping options let operators release an entire tooling row in two seconds.
Hardened 42CrMo Sectional Punches and Multi-V Lower Dies
Every 6 axis cnc press brake supplier knows that bending precision starts with tool steel integrity. We mill our standard dies from forged 42CrMo alloy steel, through-hardened to 47–52 HRC to resist wear under heavy production loads.
| Tooling Type | Material Grade | Hardness Depth | Standard Segment Sizes |
|---|---|---|---|
| Top Punches | 42CrMo Forged Alloy | 47–52 HRC | 10, 15, 20, 40, 50, 100, 200, 300 mm |
| Multi-V Dies | 42CrMo / T8 | 47–52 HRC | Solid 835 mm rails or sectional sets |
| 2-V Self-Centering Dies | 42CrMo Forged Alloy | 48–53 HRC | Precision ground split sections |
| Lower Die Rail Riser | C45 Carbon Steel | Quenched Bed | Matches overall bending table length |
Sectional segments give your shop the flexibility to assemble exact tooling lengths for box bending without grinding or custom shimming.
Custom Gooseneck Tools, Acute Angle Punches, and Hemming Sets
Standard tooling cannot handle deep return flanges or safety hems. Our 6 axis cnc press brake factory engineers and grinds specialty profiles directly in-house to match complex part geometries:
-
- Gooseneck Punches: Generous relief profiles clear deep return bends and channel sidewalls on four-sided pan forming.
- Acute Angle Punches (30° / 26°): Designed for extreme pre-bends and high spring-back materials like stainless steel.
- Spring-Loaded Hemming Tables: Two-stage bottom dies execute the initial acute bend and flat seam crush in a single pass.
- Radius Tooling: Heavy-duty radius inserts prevent micro-fracturing on high-tensile structural steel plates.
We verify all custom punch-and-die geometry using our 3D controller simulations to ensure zero collisions with backgauge fingers, as proven across our documented client case studies.
Factory QC and Calibration Standards from Our China Plant
As a direct 6 axis cnc press brake factory and specialized cnc press brake bending machine manufacturer, we eliminate deflection, misalignment, and electronic drift directly on our shop floor. Every machine undergoes rigorous mechanical machining and optoelectronic testing before packing to guarantee out-of-the-box accuracy for demanding metal fabrication jobs.
Heavy-Duty CNC Floor Borers Mill Every Frame in a Single Setup
Frame twisting and bed-to-ram tilt start with poor machining practices. Our plant prevents structural variance at the foundational manufacturing stage:
One-Step Machining Pass: After full thermal annealing to relieve internal welding stress, we mount the entire unified frame onto our heavy-duty CNC floor-type boring and milling machine.
Single-Setup Tooling: Cylinder mount pockets, linear scale mounting guides, upright throat cutouts, and table bolster surfaces are all milled in a single clamping cycle.
Absolute Mechanical Parallelism: Machining all critical mounting points together locks in squareness across the uprights, giving our 6 axis cnc press brake china build rock-solid mechanical alignment without relying on shims.
Renishaw Laser Interferometers Verify Positioning Across All Axes
Optical and mechanical calibration sets the performance baseline for every electro-hydraulic synchronous press brake we export:
Sub-Micron Laser Verification: We use Renishaw dual-frequency laser interferometers to calibrate linear scales on the Y1 and Y2 ram cylinders, as well as the high-speed ball screws on the X, R, Z1, and Z2 backgauge axes.
Pitch and Yaw Compensation: The system automatically maps positional deviations, backlash, and pitch errors across the entire stroke length, directly populating the CNC controller's compensation tables.
Repeatability Audits: Linear positioning repeatability must hold consistently within ±0.01 mm across repeated test passes before sign-off.
72-Hour Non-Stop Dry Cycling and 90-Degree Test Bends
Before any machine leaves our cnc press brake bending machine factory, it must pass strict operational stress runs:
Continuous Endurance Testing: The hydraulic system, proportional valves, and electrical cabinet run through a 72-hour non-stop dry cycling sequence to confirm valve response stability, oil temperature management, and zero hydraulic leakage.
Real-World Sample Bending: We run dynamic 90-degree bend tests across the entire bed length using certified sheet metal. Technicians measure bend angles at multiple points along the bed using digital protractors to calibrate the motorized mechanical crowning table.
Unified Quality Standards: Whether building high-tonnage industrial machines or compact production lines alongside our small electric press brake line, each unit is shipped with an individual factory calibration certificate and inspection checklist.
Industrial Sheet Metal Bending Applications
We design our multi-axis machines to handle demanding jobs that require extreme precision, fast setups, and zero rework. Our machines tackle complex folding profiles across major metal-forming sectors:
-
- Precision electrical enclosures, switchgear, and server racks: Tight tolerance box folds, multi-bend returns, and precise offset profiles without backgauge interference. The independent Z1/Z2 fingers and motorized crowning eliminate side-to-side variation across delicate 1.0 mm to 2.5 mm cold-rolled steel and galvanized sheets.
- Automotive chassis brackets and structural transport parts: High-tonnage forming of high-strength structural steel and thick alloy brackets. Our machines provide the rigidity and ram accuracy needed for multi-stage bending sequences without structural frame deflection.
- Architectural facade panels, elevator cabins, and stainless cabinets: Long-span panels requiring pristine cosmetic finishes. Controlled dynamic crowning prevents canoe-effect angle drift along entire sheet lengths, ideal for integration into full-line sheet metal bending solutions where surface scratching must be prevented.
- Heavy HVAC ducting and industrial ventilation housings: Deep box-and-pan channel work, hemming operations, and tapered airflow transitions processed quickly by programming custom gauge stops directly into the CNC interface.
Whether bending thin stainless skins or heavy-gauge carbon steel brackets, our machines deliver precise angle consistency from the very first piece. Fabricators looking to scale output can also integrate these units directly into automated sheet metal production lines for continuous robotic bending runs.
Direct Sourcing, Export Packing, and Global Service Support
Buying directly from ourfactory cuts out broker markups and connects your floor managers straight to the build engineers. As a specialized cnc press brake bending machine manufacturer, we ensure your machine is built to exact shop requirements, packed for rough ocean transit, and supported across its entire operational life.
Customized Throat Openings, Stroke Lengths, and Robotic Cell Setups
Standard dimensions do not fit every production run. We modify core mechanical dimensions directly on our heavy machining floors to match your tooling and clearance needs:
-
- Deepened throat gaps: Custom throat depths up to 800 mm or more to clear wide flanges, deep boxes, and architectural panels.
- Extended stroke and daylight: Expanded open height accommodates tall gooseneck punches, custom hemming sets, and large-radius dies.
- Automation integration: Direct PLC handshakes and safety light curtain interfaces configured for automated sheet feed tables and robotic panel bending cells.
Vacuum Barrier Anti-Rust Wrapping and Heavy Steel Transport Skids
Salt air, moisture, and road vibration during ocean freight will ruin raw metal surfaces if packaging is compromised. As a trusted 6 axis cnc press brake supplier exporting globally, we use strict industrial export packaging standards:
-
- Vapor-corrosion and vacuum sealing: All machined surfaces receive heavy anti-corrosion grease before the entire machine is sealed in puncture-resistant vacuum foil barriers with heavy industrial desiccant packs.
- Heavy-gauge steel bases: We bolt the machine frame onto reinforced steel skids rather than soft wooden pallets, preventing frame twisting inside the container.
- Axis lock-down bracing: Ram cylinders, crowning tables, and backgauge carriages are mechanically locked using heavy transport brackets to protect servo ball screws and optical linear encoders from shock loads.
Multi-Year Structural Warranty and Lifetime Remote Engineering Help
Our relationship starts when the machine touches your shop floor. Every cnc press brake bending machine leaves our floor backed by reliable operational safeguards:
-
- Heavy frame warranty: Multi-year structural protection covering our annealed, stress-relieved steel side frames and bed.
- Component protection: Direct warranty coverage on hydraulic proportional valves, CNC controllers, and brushless servo systems.
- Lifetime remote technical support: Built-in industrial network modules allow technicians from our global service department to connect to your CNC system remotely for instant parameter tuning, software diagnostics, and tooling sequence troubleshooting.
Frequently Asked Questions About 6 Axis CNC Press Brakes
What makes a 6 axis press brake better than a 4 axis machine?
A standard 4-axis machine limits your backgauge to linked movement. With a 6 axis cnc press brake china build, you get independent control over the Y1, Y2, X, R, Z1, and Z2 axes:
Asymmetrical Bending: Z1 and Z2 gauge fingers move independently along the bed, letting you position stepped flanges and tapered parts without manual gauge stops.
Flange Height Control: The motorized R-axis automatically lifts or lowers the backgauge fingers to support pre-bent shapes and complex box folds.
Higher Part Throughput: Zero manual repositioning cuts handling downtime by up to 50% on multi-station setups.
Can your factory build custom throat depths and daylight heights?
Yes. As an experienced cnc press brake bending machine manufacturer, we weld, stress-relieve, and machine all frames in-house. We regularly tailor side-frame geometry to job specs:
Deep Throat Openings: Extended depths up to 800 mm or more for wide return flanges.
Increased Daylight & Stroke: Custom vertical clearances to clear tall box bending and deep gooseneck punches.
Specialized Tonnage Frames: Whether you need a small high-speed station or a 400-ton press brake for heavy-duty metal forming, our engineering team scales the bed structure and hydraulic blocks to eliminate deflection under load.
What is the standard manufacturing lead time for custom orders?
Standard models in popular tonnages are frequently prepped for assembly, but built-to-order multi-axis units follow a strict production schedule:
Standard configurations: 25 to 35 calendar days from design confirmation to final factory trials.
Custom heavy-tonnage or long-bed builds: 45 to 60 calendar days, accounting for stress-relieving thermal cycles, precision CNC portal milling, and laser calibration.
How do you handle 3-phase power voltage and system languages for export?
Every machine shipped from our 6 axis cnc press brake factory is adapted to match your shop's utility grid and local operating team:
Electrical Integration: Factory transformers and servo drives matched to your regional supply (such as 208V, 220V, 380V, 415V, 440V, or 480V at 50Hz/60Hz).
Multi-Language Interfaces: Controllers like Delem, ESA, and Cybelec are pre-loaded in English, Spanish, German, French, Portuguese, Turkish, and other languages.
Standardized Components: Schneider electric cabinets, metric and inch measurement toggles, and universal labeling simplify local shop maintenance.
Do you offer overseas technician dispatch for setup and operator training?
Yes. As a direct 6 axis cnc press brake supplier, we provide flexible commissioning options depending on shop readiness:
On-Site Field Engineers: We dispatch technicians to handle leveling, hydraulic fluid checks, axis zero-point calibration, and on-site operator training.
Turnkey Remote Commissioning: High-definition video diagnostics, complete English wiring diagrams, and direct screen-share support for shops handling their own installation.
Tooling Support: We walk your operators through 3D tool collision setup, program storage, and automatic crowning adjustments before running your first production batch.
How to Get a Direct Factory Quotation and Technical Sheet
Getting an accurate quote and comprehensive machine specification sheet directly from our cnc press brake bending machine factory is straightforward. We bypass trading markups, giving you transparent factory pricing, certified build configurations, and fast engineering feedback.
1. Send Us Your Core Bending Requirements
To ensure the machine tonnage, throat depth, and frame stiffness match your production needs, provide your key baseline parameters:
-
- Material Types: Mild steel, stainless steel, aluminum, or high-tensile plate (such as Hardox).
- Maximum Thickness: Maximum sheet gauge required for air bending or bottoming.
- Bending Length: Maximum part length (standard beds range from 1,250 mm to 6,000 mm).
- Flange Profiles: Complex Z-bends, deep boxes, return flanges, or narrow hems.
2. Configure Your System Architecture
Select your preferred sub-systems based on your operational workflow. Every 6 axis cnc press brake for sale leaves our production floor customized to your workshop standard:
| System Module | Standard Options | Advanced / Heavy-Duty Options |
|---|---|---|
| CNC Controller | Delem DA-66T (2D Graphical) | Delem DA-69T (3D Simulation), ESA S660W, Cybelec |
| Backgauge System | 4-Axis (X, R, Z1, Z2) | 6-Axis (X1, X2, R1, R2, Z1, Z2) for extreme taper bends |
| Tooling Package | Hardened 42CrMo European-style punches & dies | Custom gooseneck punches, acute dies, pneumatic hemming |
| Clamping Style | Manual quick-clamp mechanical system | Wila-style hydraulic or pneumatic one-touch clamping |
| Deflection Crowning | CNC motorized mechanical crowning | Dynamic hydraulic auto-crowning system |
3. Fast Engineering Turnaround Within 12 Hours
Once your parameters arrive, our in-house engineering team calculates the required tonnage, checks punch-to-die clearances, and models your cycle times. As an established 6 axis cnc press brake supplier, we return a complete quotation package to your inbox within 12 hours:
-
- Itemized Factory Quotation: Clear FOB, CIF, or DDP pricing with zero hidden handling costs.
- Detailed Technical Specification Sheet: Complete motor ratings, hydraulic flow volumes, daylight dimensions, and stroke parameters.
- 2D/3D Footprint Drawings: Exact foundation requirements, overall machine dimensions, and loading weight calculations for your shop floor.