
High-Precision Sheet Metal Machinery for Architectural & Construction Fabrication
Engineered for curtain wall contractors, structural builders, and decorative metal fabricators worldwide. Haden delivers heavy-duty, large-format sheet metal laser cutting machines, tandem CNC press brakes, high-speed V-groovers, and automated panel benders built to hold precise facade tolerances and protect pristine architectural finishes.
Ultra-Long Bed Processing
Continuous, high-accuracy cutting and tandem bending engineered for workpieces up to 12 meters.
Zero-Scratch Protection
Class-A architectural surface integrity for anodized aluminum, polished stainless steel, and pre-coated sheets.
Direct BIM & CAD Integration
Native STEP, DXF, and 3D architectural CAD file parsing directly to CNC controllers without manual unfolding errors.
Overcoming Core Facade Panel Manufacturing Challenges with Advanced Architectural Metalworking Solutions
Modern architectural building envelopes require flawless aesthetic surfaces, crisp corner reveals, and uncompromising dimensional accuracy. Fabricating oversized exterior cladding, perforated sunscreens, and structural subframes frequently pushes standard sheet metal equipment past its operational limits. Material springback, surface abrasions, thermal warpage, and angular deflection across long spans routinely compromise project schedules, drive up scrap rates, and complicate on-site installation.
Haden manufactures purpose-built architectural sheet metal machinery designed specifically to resolve these fabrication bottlenecks. By pairing stress-relieved structural machine beds with closed-loop CNC dynamic crowning, scratch-free tooling systems, and high-speed V-grooving technologies, Haden delivers reliable, repeatable processing performance for complex architectural geometries and premium decorative alloys.
Long-Span Panel Deflection
Extended facade cassettes and honeycomb panels develop substantial angular variation across 6m to 12m lengths due to machine bed deflection under heavy forming loads.
Real-time CNC dynamic hydraulic and mechanical crowning systems constantly adjust counter-deflection, maintaining uniform bend angles within ±0.5° across entire profiles.
Surface Tooling Abrasions
Mirror-finish stainless steel, pre-anodized aluminum, and brass cladding readily suffer die scuffs, contact galling, and protective film rupture during conventional forming.
Cushioned clamping tables on V-groovers paired with specialized non-marking polyurethane lower dies and roller-bearing tooling eliminate cosmetic defects completely.
Perforation Thermal Warpage
High-density decorative perforations concentrate cutting heat rapidly across thin panels, creating internal stress buildup, edge dross, and severe sheet warping.
High-dynamic sheet metal laser cutting machines with adaptive pulse control, high-pressure nitrogen assist gas, and intelligent nesting algorithms cut heat input and boost yield by 15%.
Cumulative Tolerance Stack
Inconsistent bend radiuses and frame deflection compound into significant cumulative errors, resulting in uneven facade joint reveals and expensive installation delays.
Heavy stress-relieved annealed frames combined with synchronized CNC V-grooving and bending control deliver sharp corner reveals and repeatable datum points.
Process Comparison: Conventional Fabrication vs. Haden Architectural Machinery Solutions
Evaluating technical performance benchmarks demonstrates how Haden equipment eliminates downstream installation friction while upholding tight sheet metal bending tolerance standards across diverse architectural alloys.
| Fabrication Parameter | Conventional Fabrication Method | Haden Machinery Architecture | Project-Level Advantage |
|---|---|---|---|
| Long-Bed Angle Uniformity | Manual mechanical shimming; angular drift up to ±2.0° over 6m spans | Automatic CNC dynamic crowning with multi-axis real-time compensation | Maintains ±0.5° across 12-meter profiles |
| Facade Corner Definition | Direct air bending with outer radius R = 1.5t to 2.5t (wide joint seams) | Precision pre-V-grooving before automated cassette folding | Ultra-sharp R < 0.5mm razor-edge aesthetics |
| Finished Cladding Integrity | Metallic die rubbing marks, scoring, and film tears on anodized panels | Polyurethane non-marking dies and pneumatic cushioned clamping | 100% scratch-free Class-A surface guarantee |
| Perforated Screen Flatness | Thermal curling and dross accumulation requiring manual post-grinding | High-frequency pulse laser cutting machines coupled with precision roller leveling | Zero dross edges and verified flat panel datums |
| Structural Plate Forming | Severe frame flex and dimensional deviation during thick plate forming | Thermally annealed 600°C stress-relieved solid steel monolithic frames | Geometric frame stability <0.015 mm/m |
Configure the Right Machinery for Architectural Metal Fabrication
Haden can configure laser cutting, bending, V-grooving, panel bending, leveling, and automated production equipment around large-format panels, facade components, structural metalwork, and other architectural fabrication requirements.
Architectural Metal Application Scenarios and Precision Forming Workflows
Modern architectural envelope fabrication requires stringent angular precision, pristine surface finishes, and direct translation from BIM models to shop floor machinery. Haden engineers dedicated sheet metal fabrication products designed for facade panel manufacturers, architectural metalwork job shops, and structural envelope contractors. Discover our proven production workflows across five core construction metalworking scenarios.
Curtain Wall & Cladding Cassette Fabrication
Precision curtain wall panel fabrication demands tight joint reveals, zero oil-canning, and razor-sharp returns. Direct air bending on thick architectural aluminum (AA3003, AA5052) or stainless steel cladding creates wide outer corner radii that compromise building aesthetics. Haden combines large-format fiber laser blanking with high-speed CNC V-grooving and synchronized press brake bending to produce crisp 90° cassette returns with exterior corner radii under 0.5 mm.
WF Standard Certified Manufacturing Workflow
Technical Process Thresholds
| Workpiece Alloy | Thickness Range | Angular Precision | Recommended Equipment |
|---|---|---|---|
| AA3003 / AA5052 Solid Aluminum | 2.0 mm – 4.0 mm | ±0.3° across 12 m | Haden CNC V-Groover + Tandem Press Brake |
| SUS 304 / 316 Architectural Stainless | 1.2 mm – 3.0 mm | ±0.25° continuous | Haden Dual-Pulse Laser + CNC Press Brake |
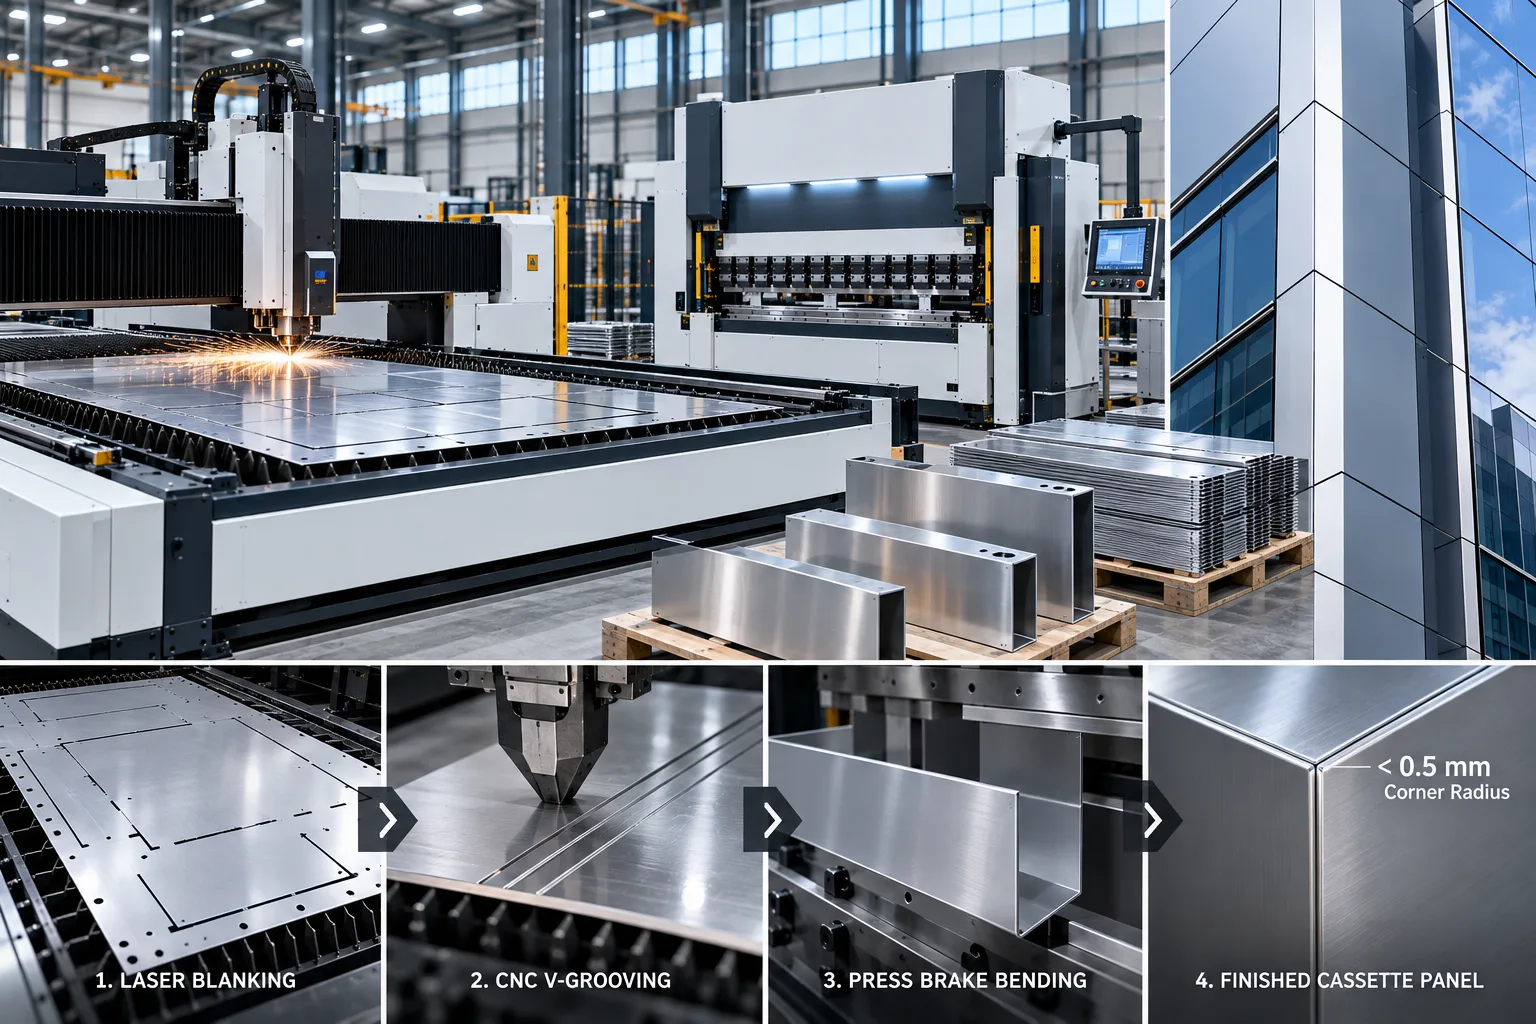
Curtain Wall Cassette Production Cell
- Haden FiberCut 12025: 12 m × 2.5 m large-format fiber laser blanking platform.
- Haden GroovTech 6000: High-speed vertical 4-axis CNC V-grooving center.
- Haden SynchroBrake Tandem: Synchronized 800T/8000mm dynamic crowning press brake.
Planning a Custom Architectural Metal Fabrication Line?
From V-grooving and precision bending to panel forming and automated production cells, Haden can configure machinery, tooling, material flow, and automation around your architectural components, production targets, and available factory space.
Dedicated Architectural Sheet Metal Machinery Matrix
Engineered specifically for exterior curtain wall panels, interior metal ceilings, and structural framework fabrication, Haden delivers heavy-duty forming, cutting, and grooving machinery. Every advanced laser cutting machine and forming system supports customized throat depths, extended stroke heights, and oversized tandem beds to meet demanding architectural specifications.
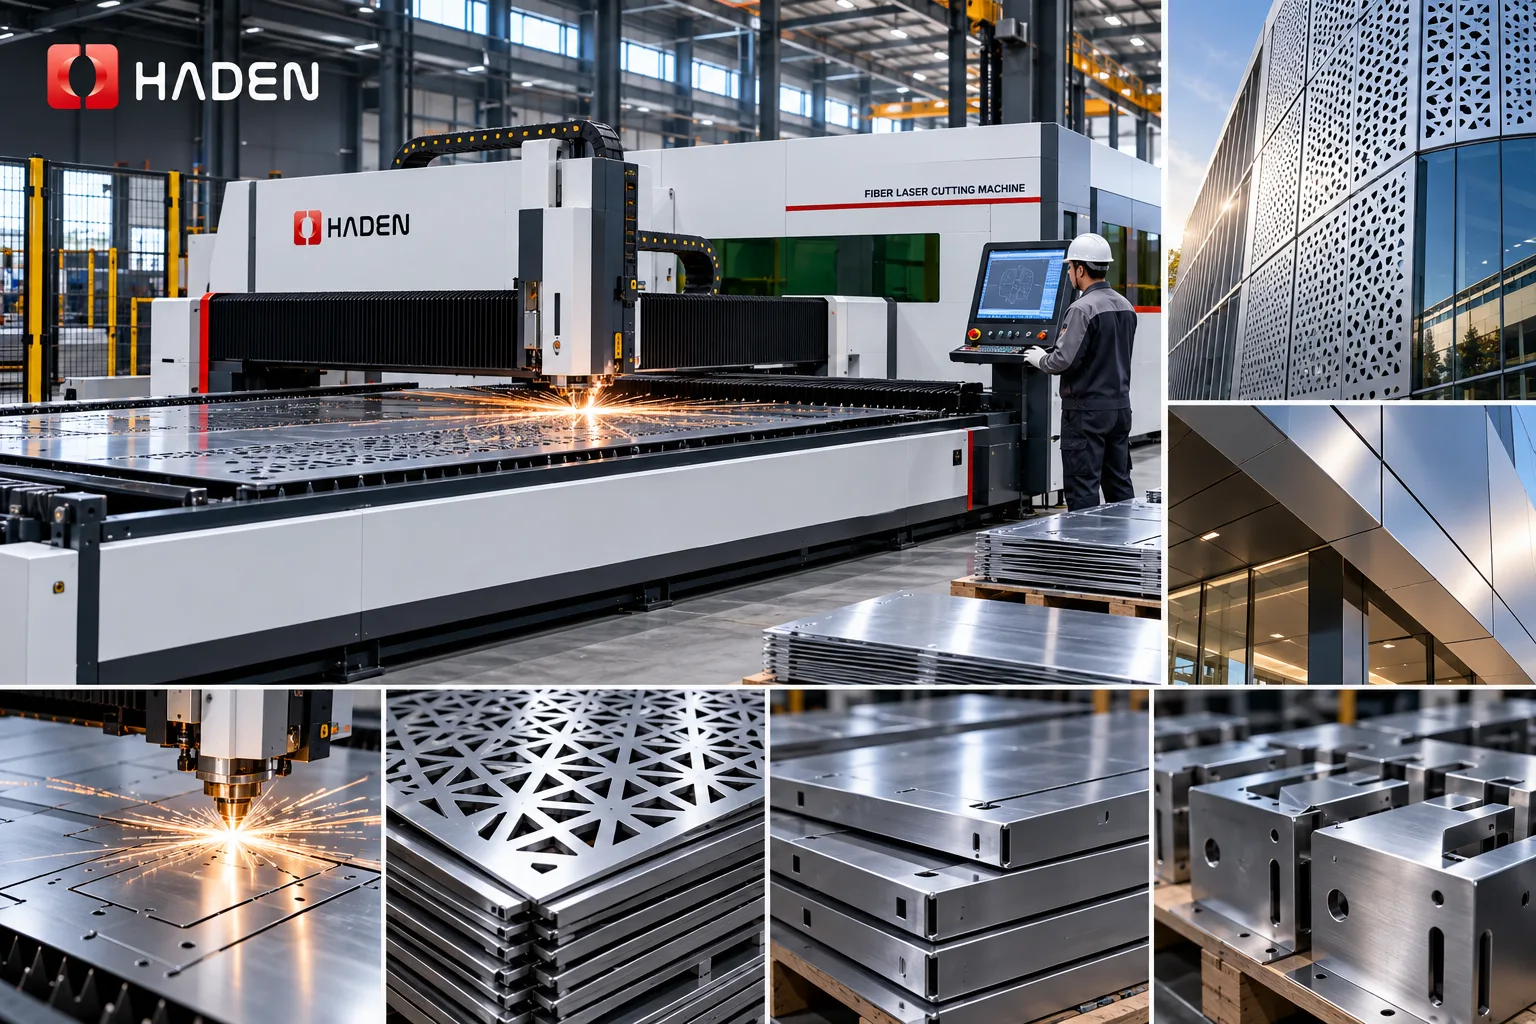
Large-Format Fiber Laser Cutting Machines
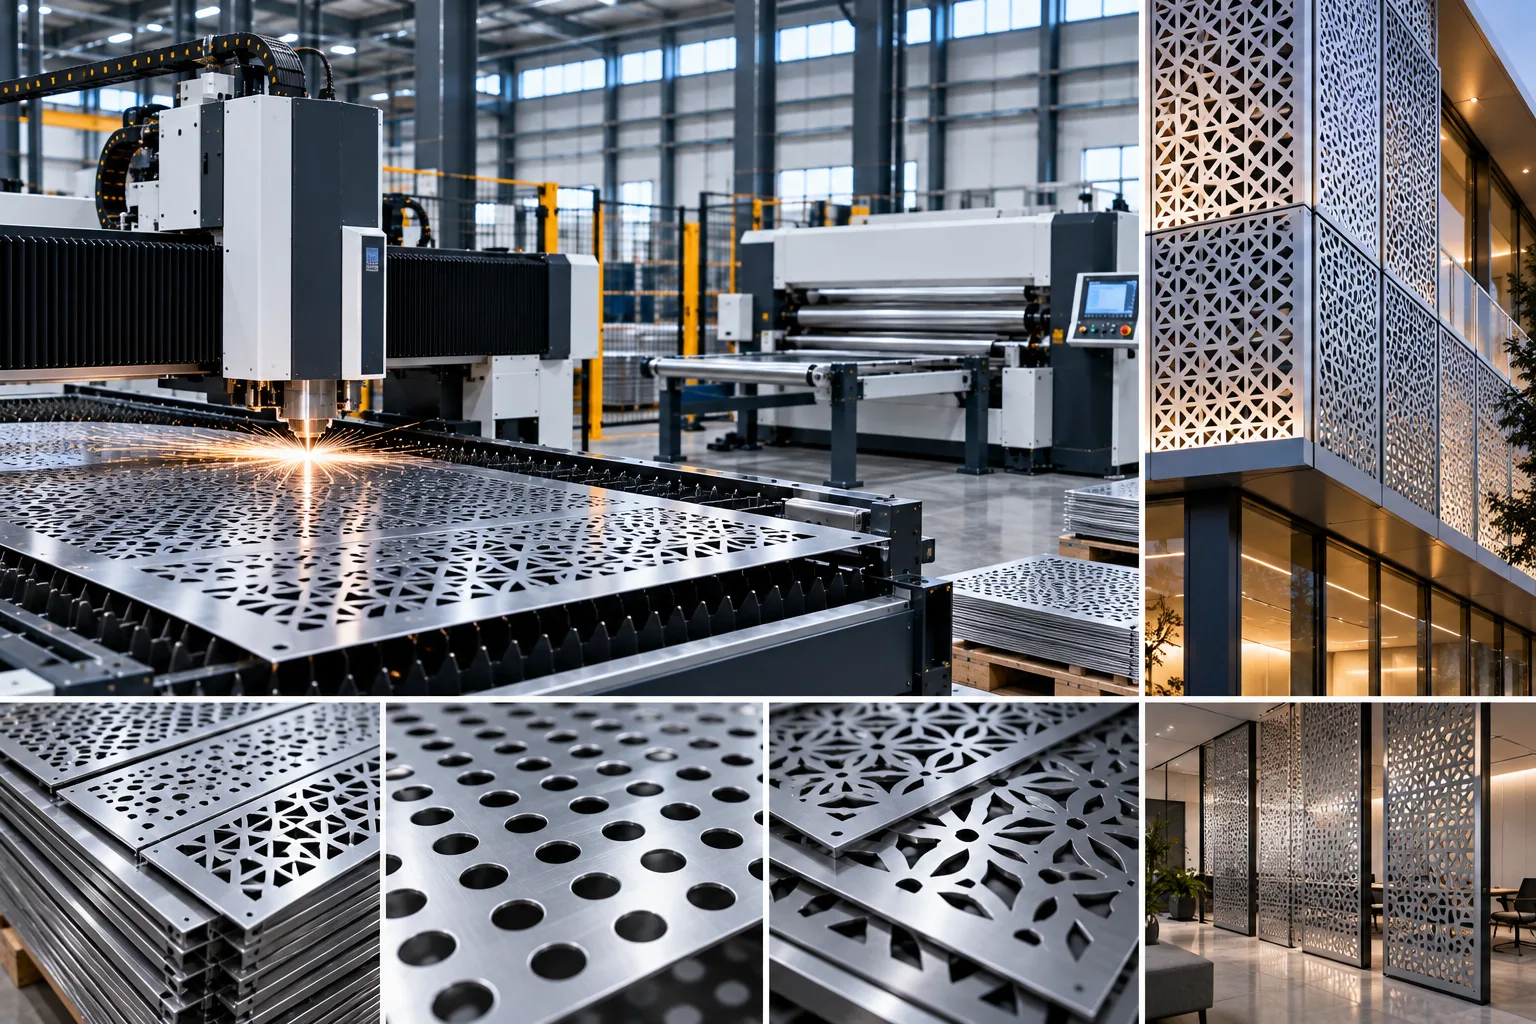
Engineered for single-pass cutting with dedicated sheet metal laser cutting machines, handling extra-long facade cassettes, structural curtain wall brackets, and intricate perforated decorative panels with anti-reflection optical protection.
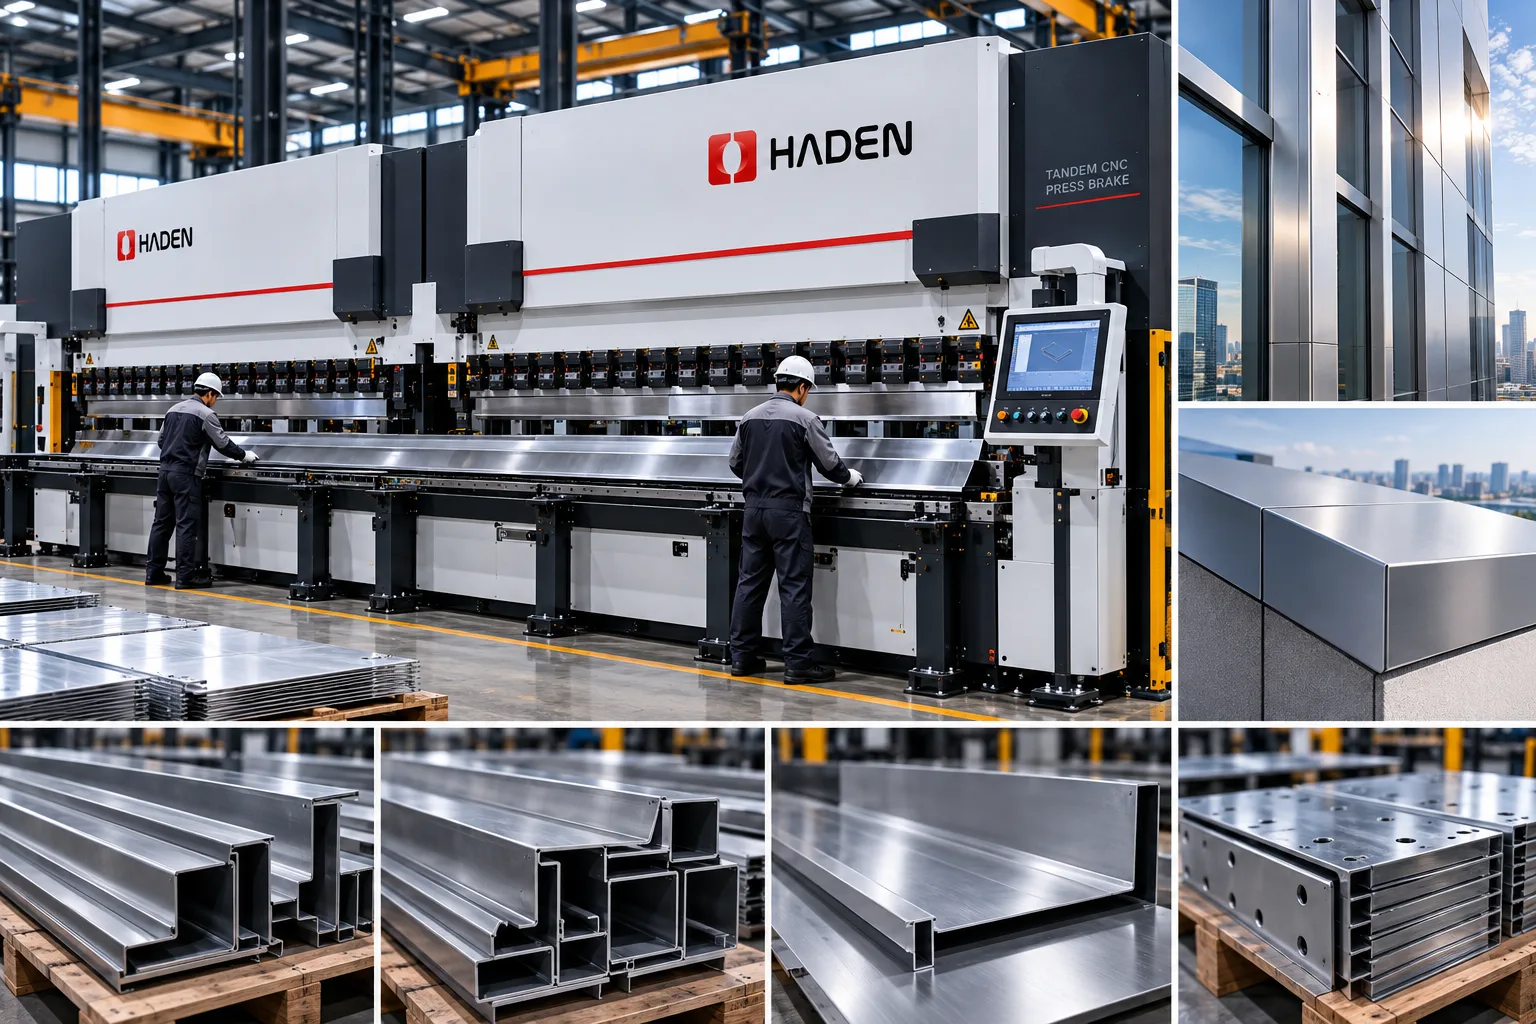
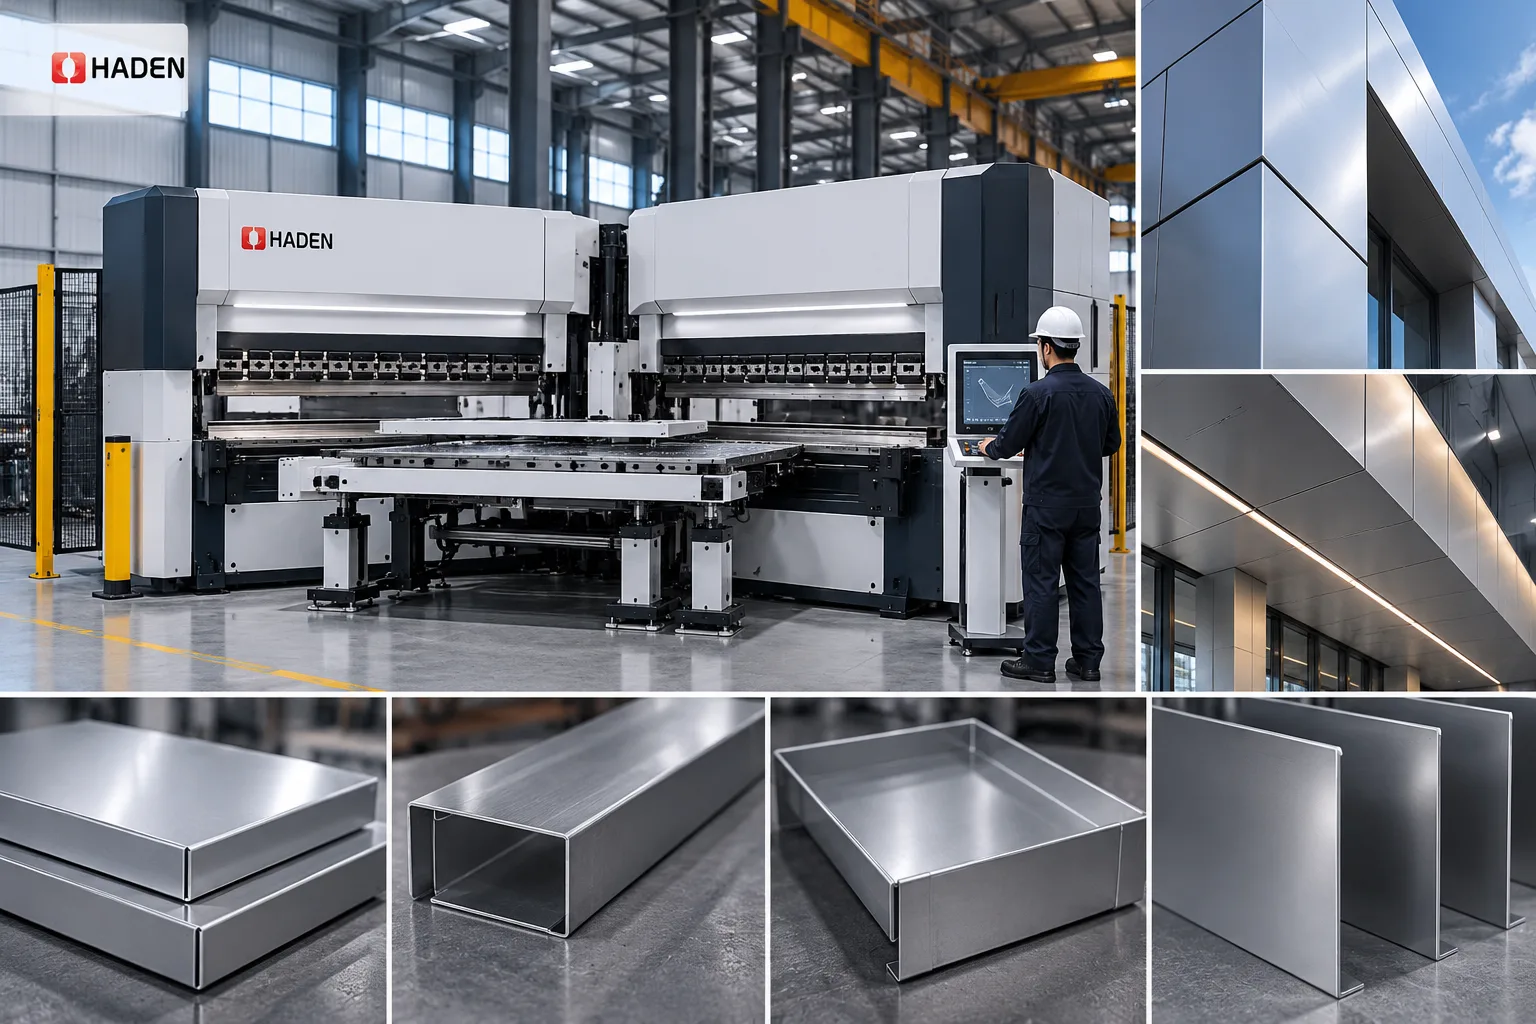
Tandem CNC Synchronized Press Brakes
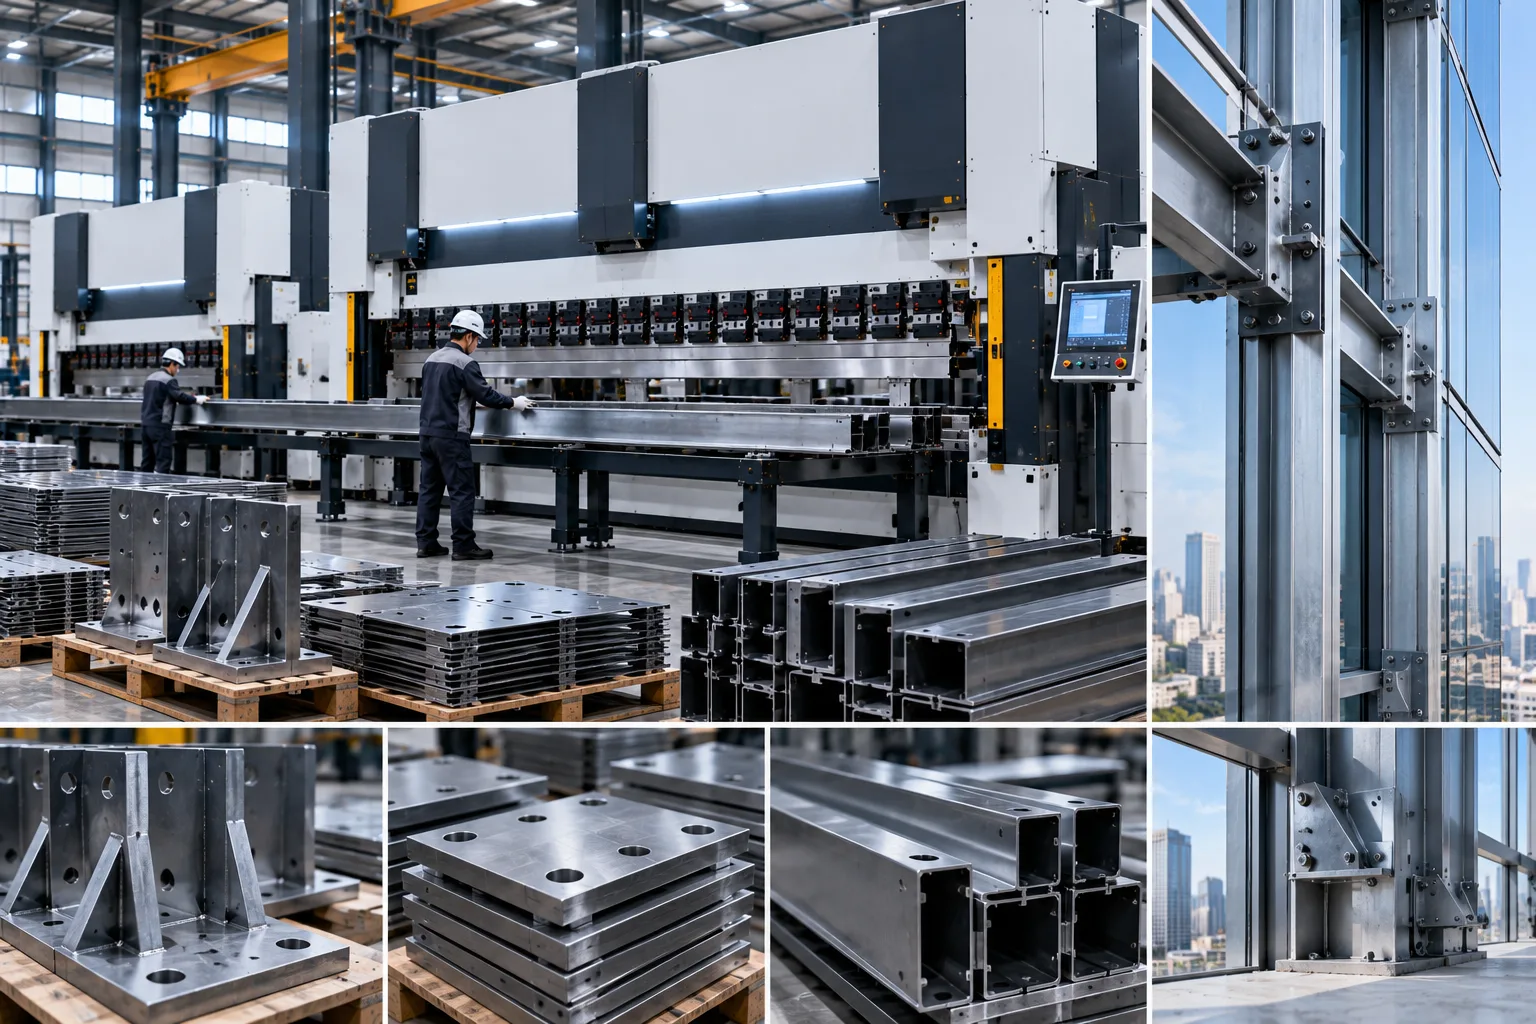
Bends continuous full-length curtain wall mullions, roof flashings, and heavy structural base plates with dynamic crowning compensation for uniform angles across the entire seam.
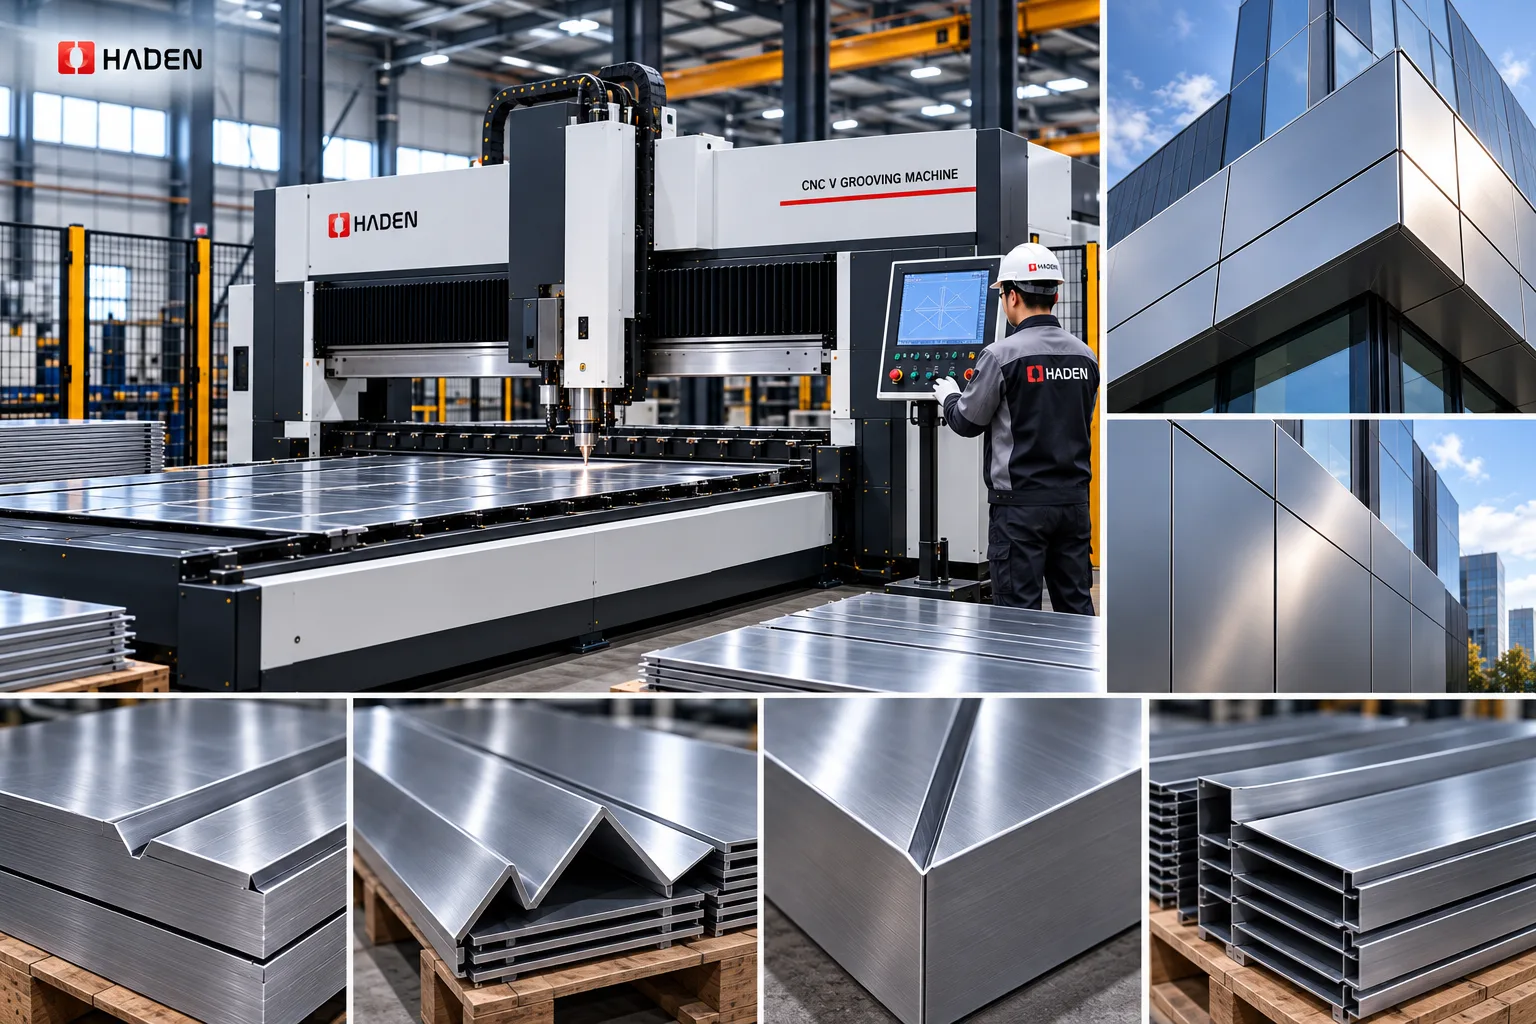
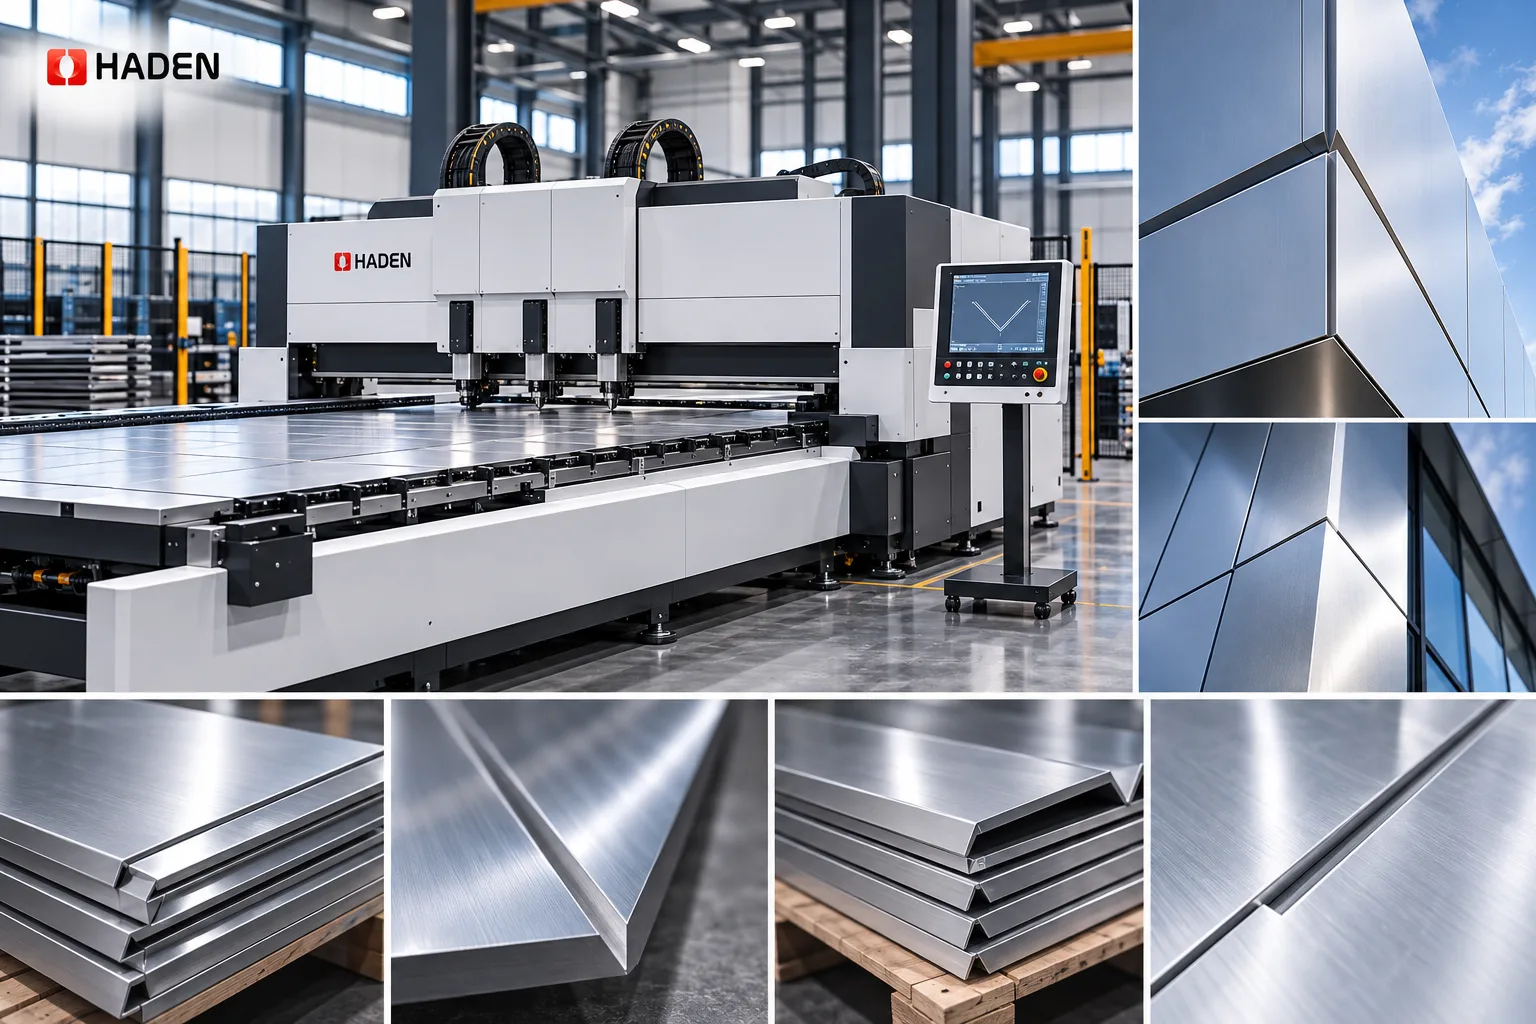
High-Speed CNC Facade V Grooving Machines
Pre-mills high-precision V-grooves into aluminum, stainless steel, and composite sheets prior to bending, producing ultra-sharp exterior corners and seamless architectural reveals.
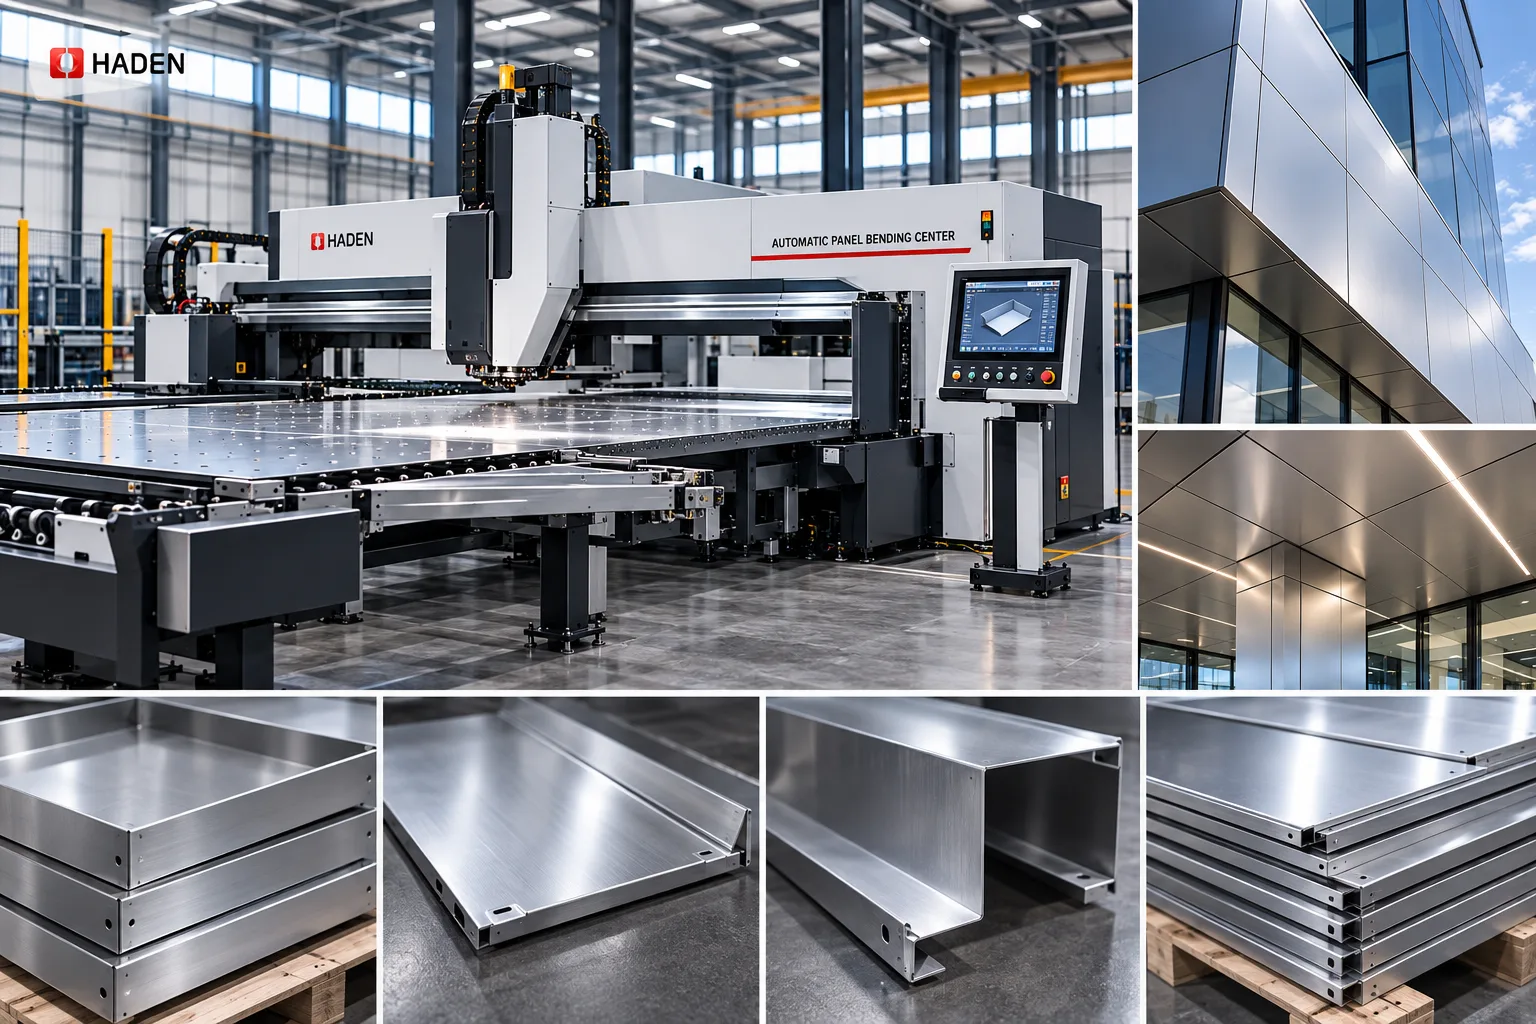
Intelligent Automatic Panel Bending Centers
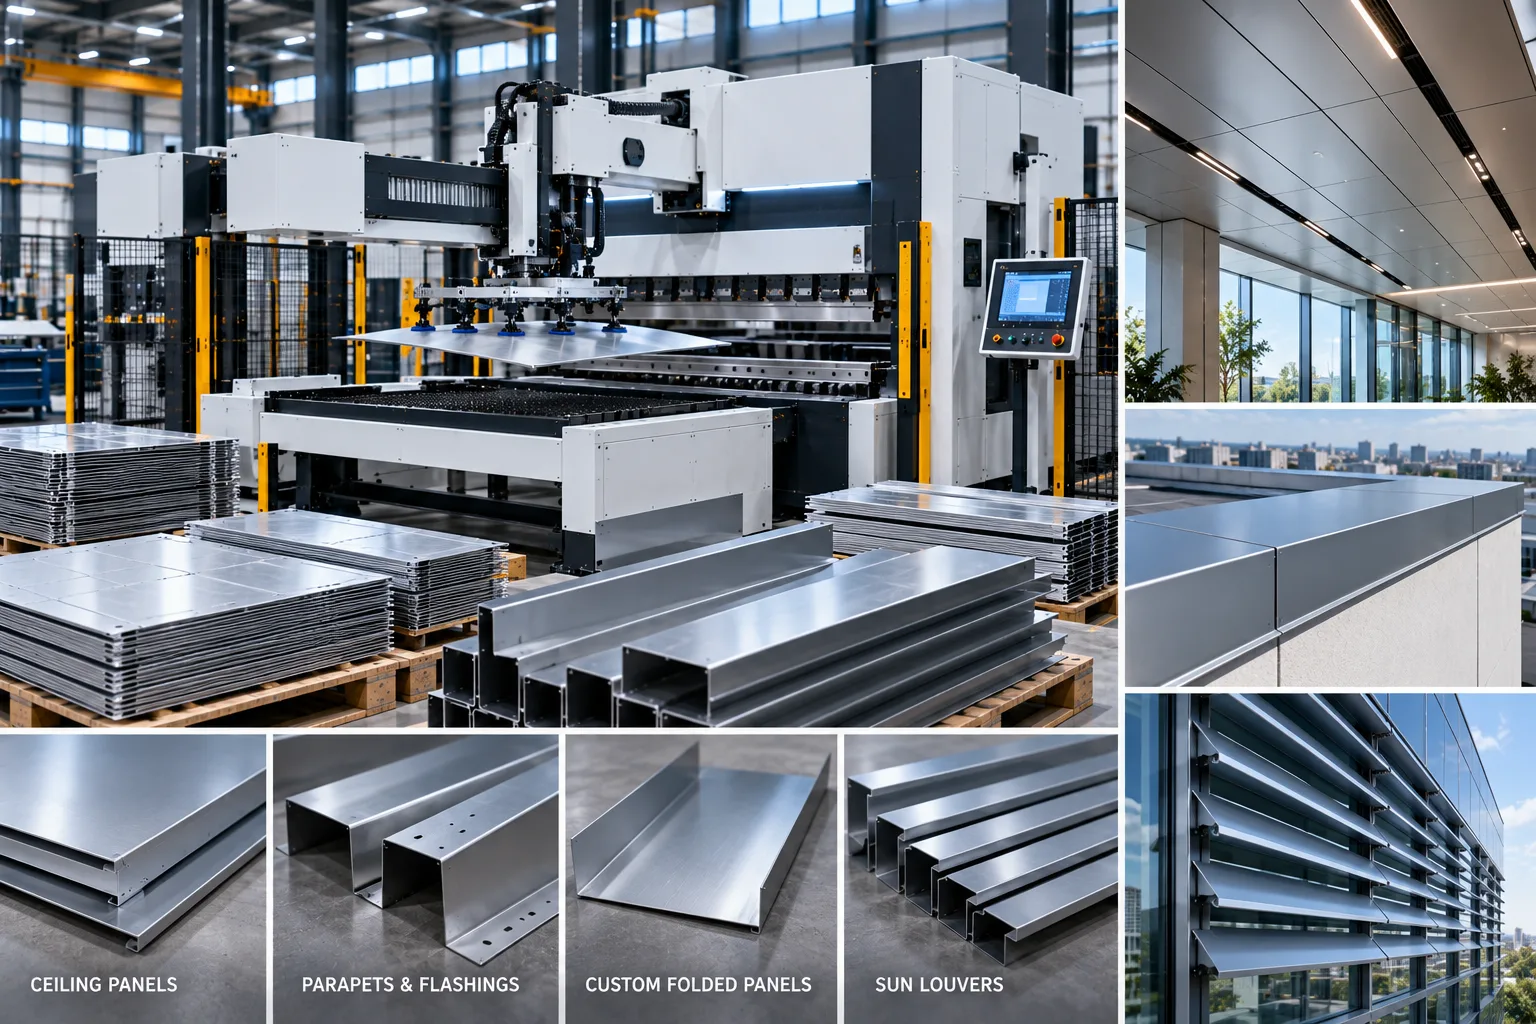
Automates multi-edge box folding, metal cassette forming, and ceiling tile fabrication with universal servo tooling, eliminating manual operator handling and setup downtime.
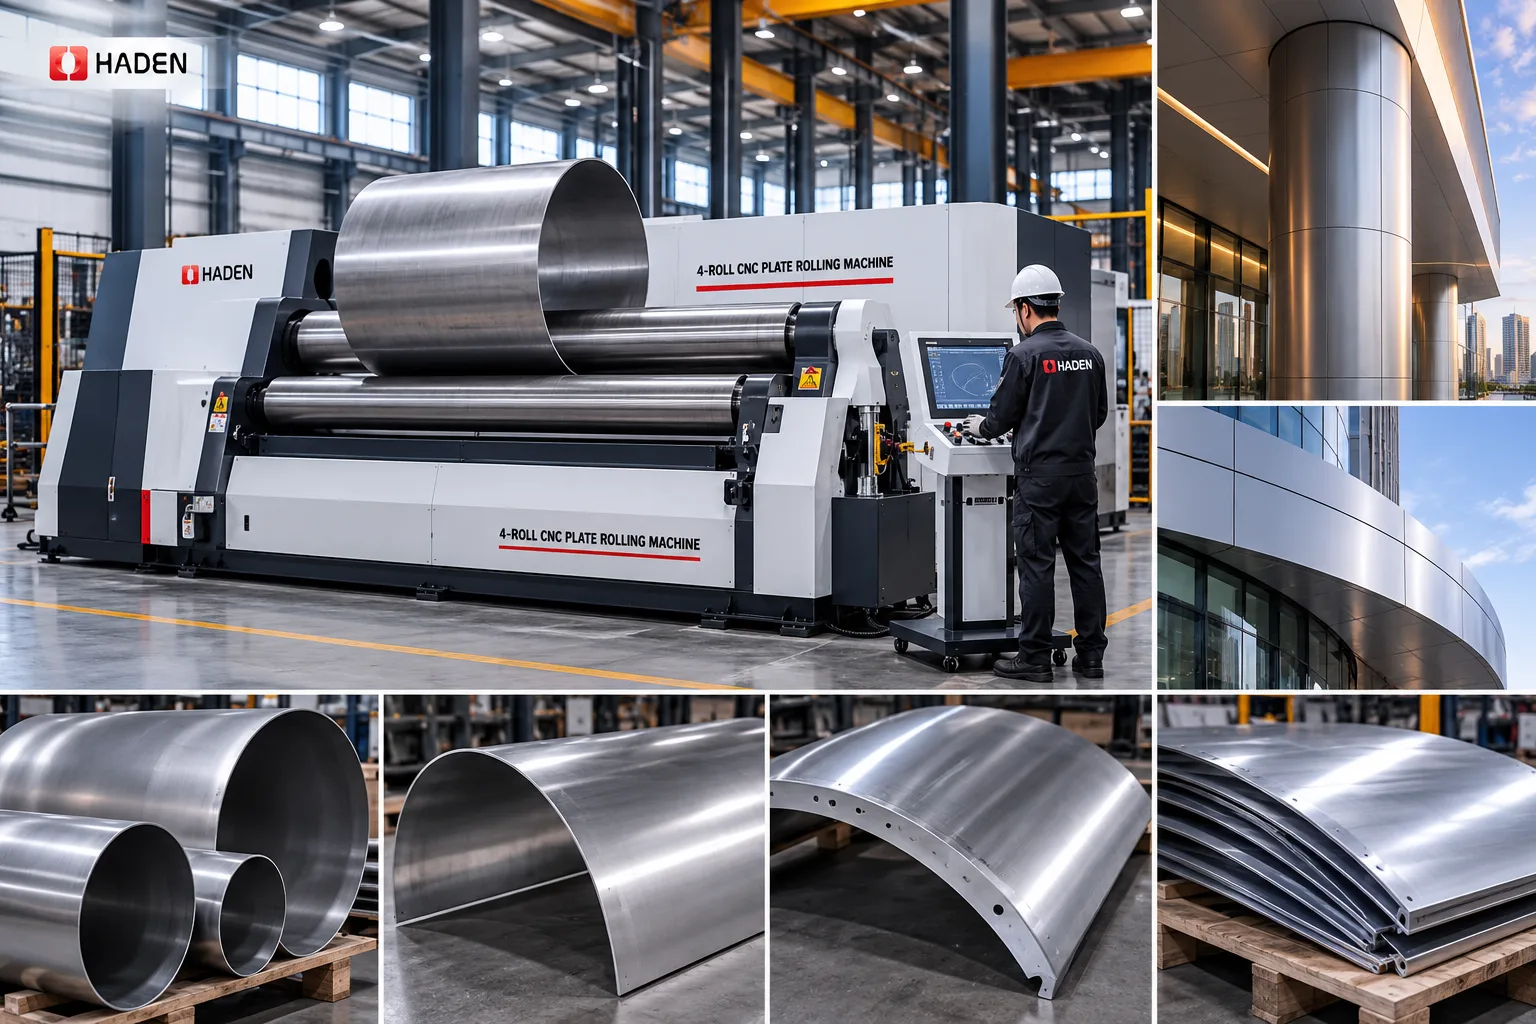
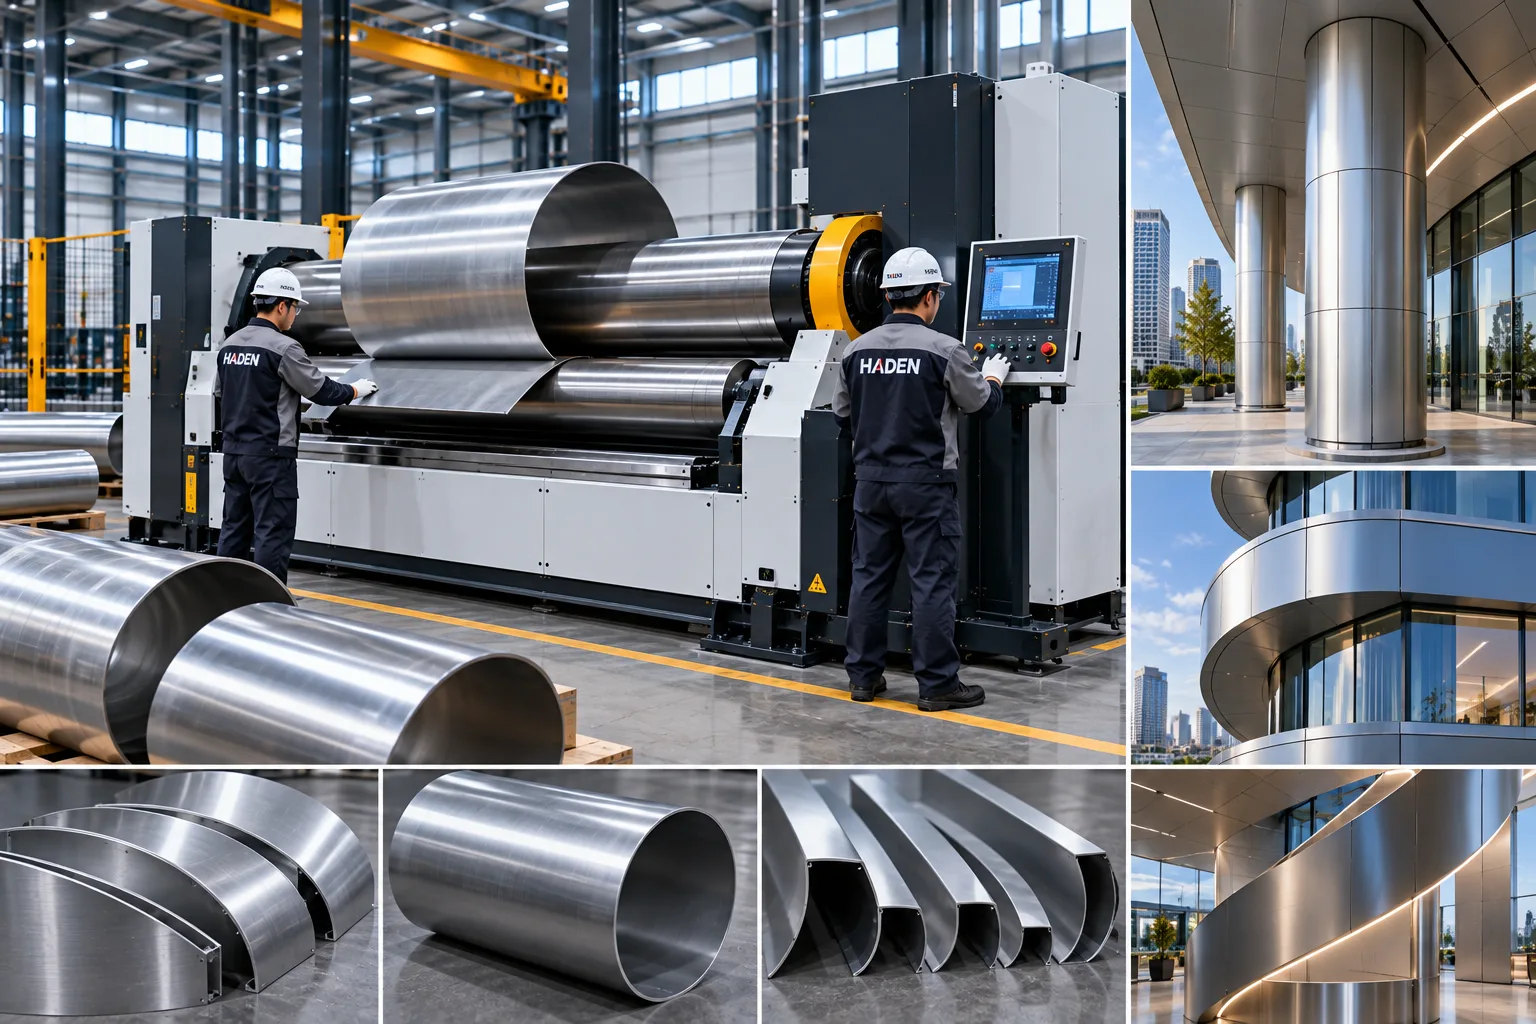
High-Precision 4-Roll CNC Plate Rolling Machines
Rolls cylindrical, elliptical, and variable-radius architectural arches with minimal unbent flat ends on aluminum solid sheet, composite panels, and stainless cladding.
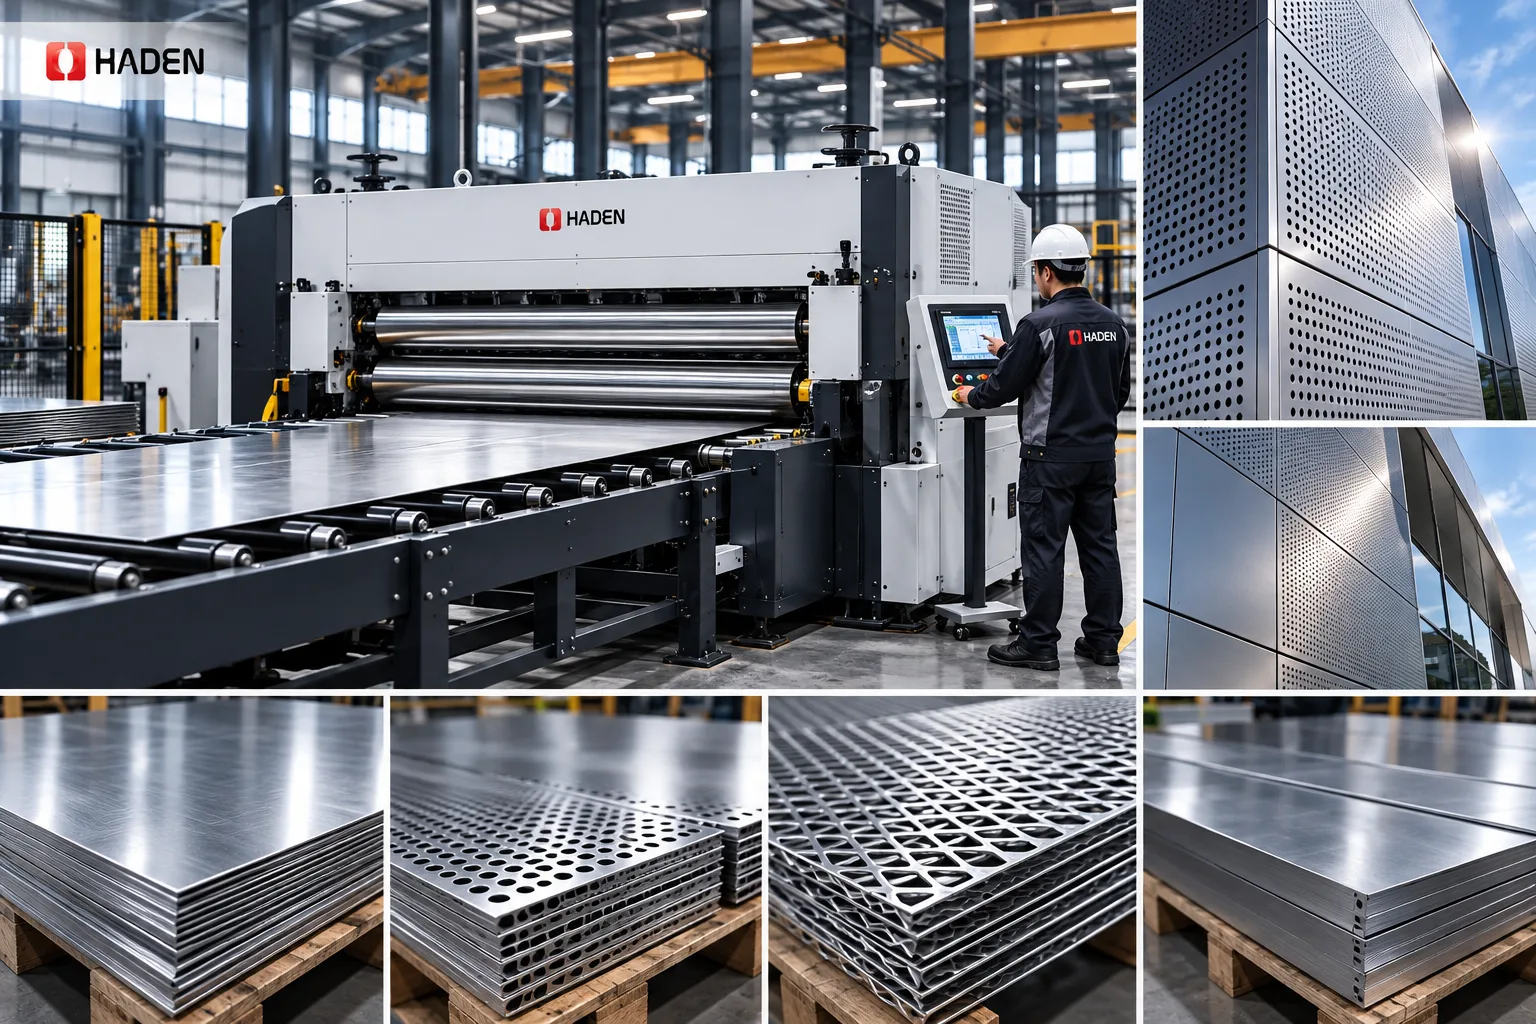
Precision Sheet & Plate Leveling Machines
Eliminates internal tension, edge waves, and thermal distortion across densely perforated facade screens, expanded mesh panels, and laser-processed architectural cladding.
Need a Non-Standard Machine or Tooling Configuration?
For oversized panels, long workpieces, special profiles, or surface-sensitive architectural components, Haden can evaluate customized machine dimensions, tooling, gauging, workpiece support, and material-handling configurations around your fabrication requirements.
Sharp Corner Facade Bending: The Engineering Synergy of CNC V-Grooving and Folding
Achieving monolithic shadow gaps, crisp cassette returns, and true 90-degree outer corners on modern exterior envelopes demands specialized fabrication. By pairing high-precision blanks from industrial laser cutting machines with CNC V-grooving technology and multi-axis press brakes, fabricators can eliminate wide bend radii, reduce forming tonnage by up to 60%, and deliver architectural metalwork of uncompromising quality.
Core Mechanics: Eliminating Wide Radii and Seam Reveals
Conventional air bending of 3.0mm to 4.0mm architectural sheet metal naturally yields an outside corner radius of R = 1.5t to 2.0t. On large exterior cladding panels and column enclosures, this standard radius creates wide, visibly soft transitions that interrupt clean sightlines and expose irregular shadow reveals between adjacent modules.
Precision V-grooving pre-cuts a controlled V-shaped profile along the designated bend axis, leaving a calibrated residual thickness (typically 0.3mm to 0.8mm depending on material grade). When formed on a press brake, the material folds neatly along the grooved seam, achieving an outside radius of R < 0.5mm for sharp, monolithic corners without structural tearing.
Micron-Level Depth Control and Surface Protection
Haden CNC V-grooving machines utilize dynamic hydraulic clamping tables coupled with high-resolution closed-loop linear encoders to maintain consistent cutter penetration across sheet spans up to 12 meters. This continuous depth tracking eliminates standard fabrication failures:
- • Burn-through and micro-fracturing: Uniform residual thickness prevents localized tensile failure during 90° to 135° cassette panel folding.
- • Groove depth deviation: Auto-leveling cutter carriages compensate for raw mill sheet thickness tolerances in real time.
- • Coating crazing: Reduced outer fiber elongation preserves PVDF coatings, coil anodizing, and protective films along the fold.
Material-Specific Grooving and Forming Parameters
Optimizing groove angle, tool geometry, and residual web thickness on blanks processed by sheet metal laser cutting machines ensures structural integrity across common architectural metals:
- Architectural Aluminum (1.5–4.0mm, 3003/5052): Recommended groove depth of 70%–85% of total sheet thickness with 90°–100° cutter profiles. High-speed carbide inserts prevent edge burring prior to folding.
- Stainless Steel Cladding (0.8–3.0mm, 304/316): Recommended groove depth of 60%–75% of thickness with 90°–135° angles. Controlled cutter feed rates manage work-hardening and heat buildup along the slot.
- Architectural Copper & Brass (0.8–3.0mm): Recommended groove depth of 65%–80% of thickness with 90° profile tooling and active chip evacuation to ensure flawless polished or patinated surfaces.
Performance Matrix: Direct Bending vs. Precision V-Groove Folding
| Engineering Metric | Standard Direct Bend | CNC Grooved & Folded |
|---|---|---|
| Outside Corner Radius (R) | 1.5t – 2.0t (R 4.5–8.0mm on thick stock) | R < 0.5mm (true sharp edge) |
| Visible Seam Reveal | 3.0mm – 6.0mm rounded gap | 0.5mm – 1.0mm hairline joint |
| Press Brake Tonnage Load | 100% nominal forming load | 40% – 60% force reduction |
| Angular Springback Variation | ±0.8° – ±1.5° across full sheet | ±0.2° – ±0.3° consistent tolerance |
| Tooling Life Expectancy | Standard cycle life (~50,000 hits) | Extended service (>200,000 hits) |
| Coated Surface Condition | Risk of coating crazing and die marks | Class-A architectural finish preserved |
Tonnage, Tooling, and Energy Efficiency Profile
Removing material along the neutral bending axis substantially lowers the plastic deformation resistance of the workpiece:
- → Reduced Machine Deflection: Lower forming pressure prevents bed and ram yaw on extra-long 6m to 12m press brakes.
- → Stable Bend Geometry: Minimal springback variation (±0.25°) guarantees flawless panel alignment across complex multi-panel elevations.
- → Lower Energy Consumption: Operating at 40%–50% nominal hydraulic or servo tonnage delivers measurable electrical savings per shift.
- → Tooling Longevity: Reduced contact pressure drastically cuts punch tip galling and die shoulder wear on mirror-finish stainless.
Strategic Advantages for Architectural Facade Fabricators
✓ Architectural Aesthetic Compliance
Deliver razor-sharp, monolithic facade transitions that meet strict architectural specifications for curtain walls, rainscreen cassettes, and decorative column covers without unsightly radius rounding.
✓ High-Speed Production Repeatability
Lower forming tonnage requirements and predictable residual material behavior widen forming process windows, driving up first-pass acceptance rates on high-volume commercial panel runs.
✓ Lower Production and Rework Costs
Eliminate costly manual post-bend grinding, corner welding, and repainting. Extended tooling lifespans and minimized machine strain significantly lower operating cost per square meter.
✓ Surface and Protective Film Integrity
Grooving from the reverse side prevents surface elongation on visible faces. Pre-applied protective laser films, anodized coatings, and PVDF paints remain completely intact throughout the fold cycle.
Integrated Haden CNC V-Grooving and Press Brake Ecosystem
Haden designs matched manufacturing systems that harmonize high-speed CNC horizontal and vertical V-groovers with heavy-duty tandem press brakes for unified architectural fabrication:
Closed-Loop Thickness Sensing
Real-time residual thickness probing across multi-meter sheets maintains depth accuracy within ±0.03mm, preventing panel burn-through, micro-fracturing, or bend line deviations.
Multi-Axis Dynamic Crowning
Electro-hydraulic CNC crowning integrated directly into the press brake controller ensures absolute angular uniformity within ±0.25° from end to end on 6m to 12m architectural panels.
Direct CAD/BIM File Interoperability
Directly import STEP, DXF, and IGES engineering files synchronized with framing profiles cut on tube laser cutting machines. Haden software automatically calculates grooving depth, sheet stretch factors, and multi-step bend sequences to eliminate operator trial-and-error.
Engineering Case: Supertall Commercial Tower Rainscreen Panels
Project Specifications
3.0mm solid architectural aluminum (5052-H32) cassette panels measuring 6,000mm × 1,400mm with 4-sided returns, requiring uniform 0.5mm outside bend radii and Class-1 anodized surface perfection.
Haden Equipment Solution
Haden High-Speed Vertical CNC V-Groover synchronized with an 8,000mm 400-Ton Tandem CNC Press Brake, running full production at 250+ oversized facade cassettes per week.
Quantified Production Results
- ✓ Outside corner radius reduced from 4.8mm to 0.45mm for razor-sharp facade reveals
- ✓ Bending force requirements decreased by 54%, eliminating bed crowning over-compensation
- ✓ Overall angular deviation maintained within ±0.2° across the entire 6,000mm panel length
- ✓ Zero micro-fracturing along bend axes; 100% first-pass qualification under ASTM E330 wind load testing
Discuss Your Architectural Sheet Metal Fabrication Project
Share your facade cassette, rainscreen, cladding, trim, or other architectural component drawings in DXF, STEP, or PDF format. Haden engineers can evaluate suitable cutting, V-grooving, bending, forming, tooling, and production configurations for your application.
Architectural Panels • V-Grooving & Bending • Custom Machine Configuration • Automation Planning
Integrated Coil-to-Panel Architectural Metal Production Workflow
From raw coil stock to jobsite-ready facade cassettes, Haden synchronizes every fabrication stage for tight structural tolerances and flawless surface quality.
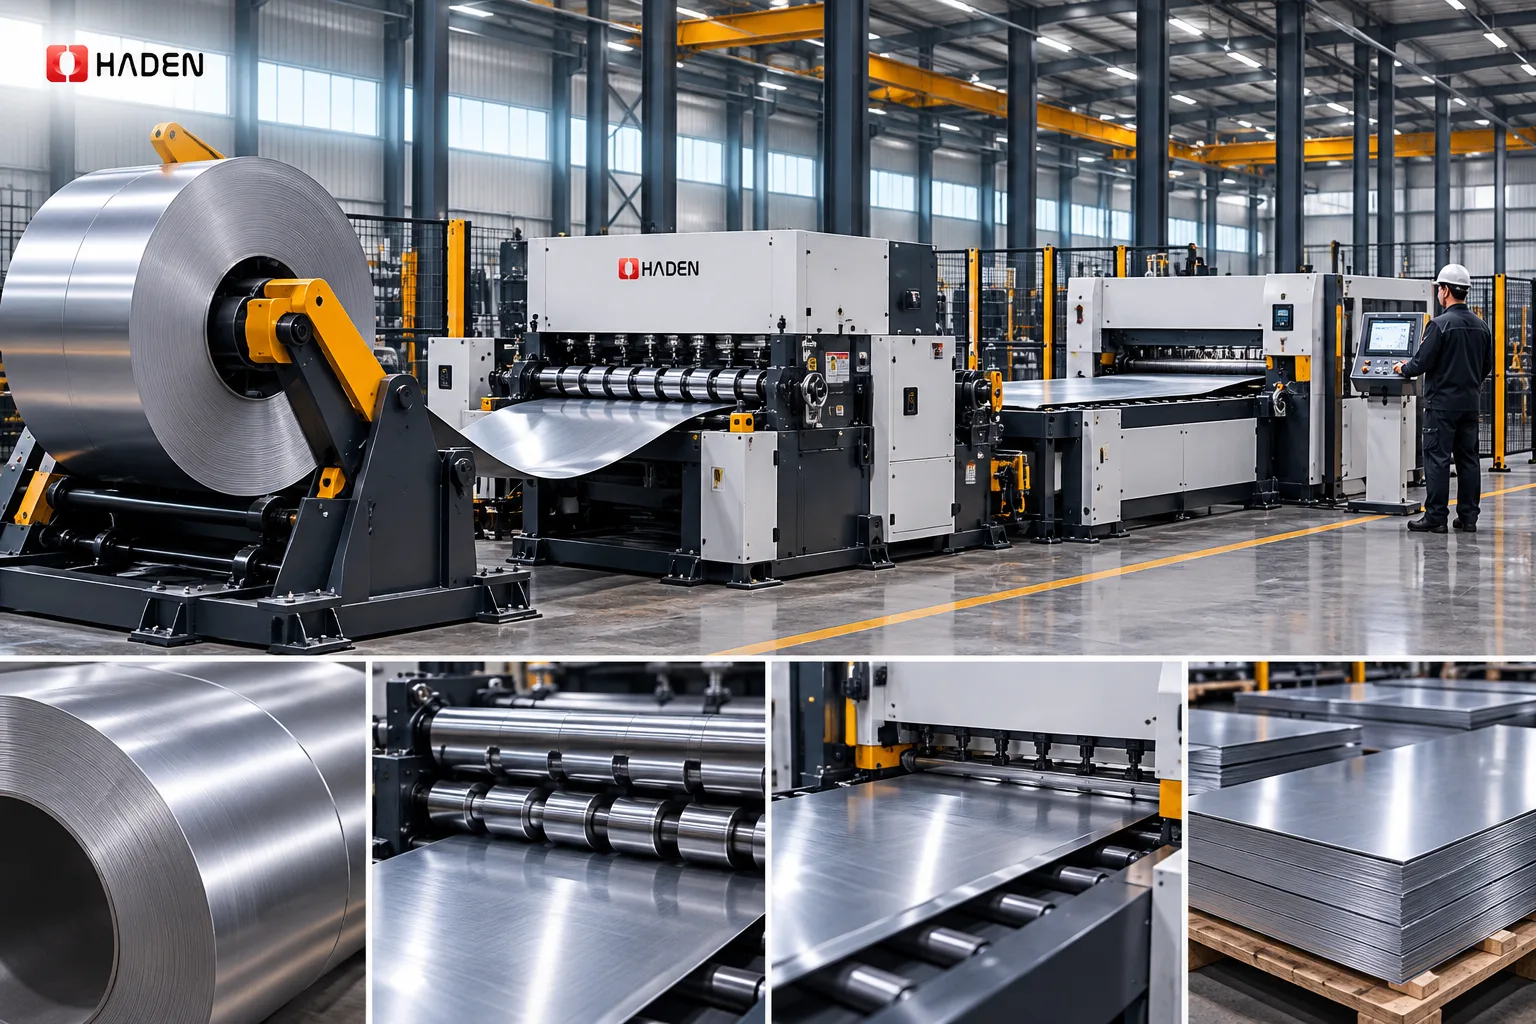
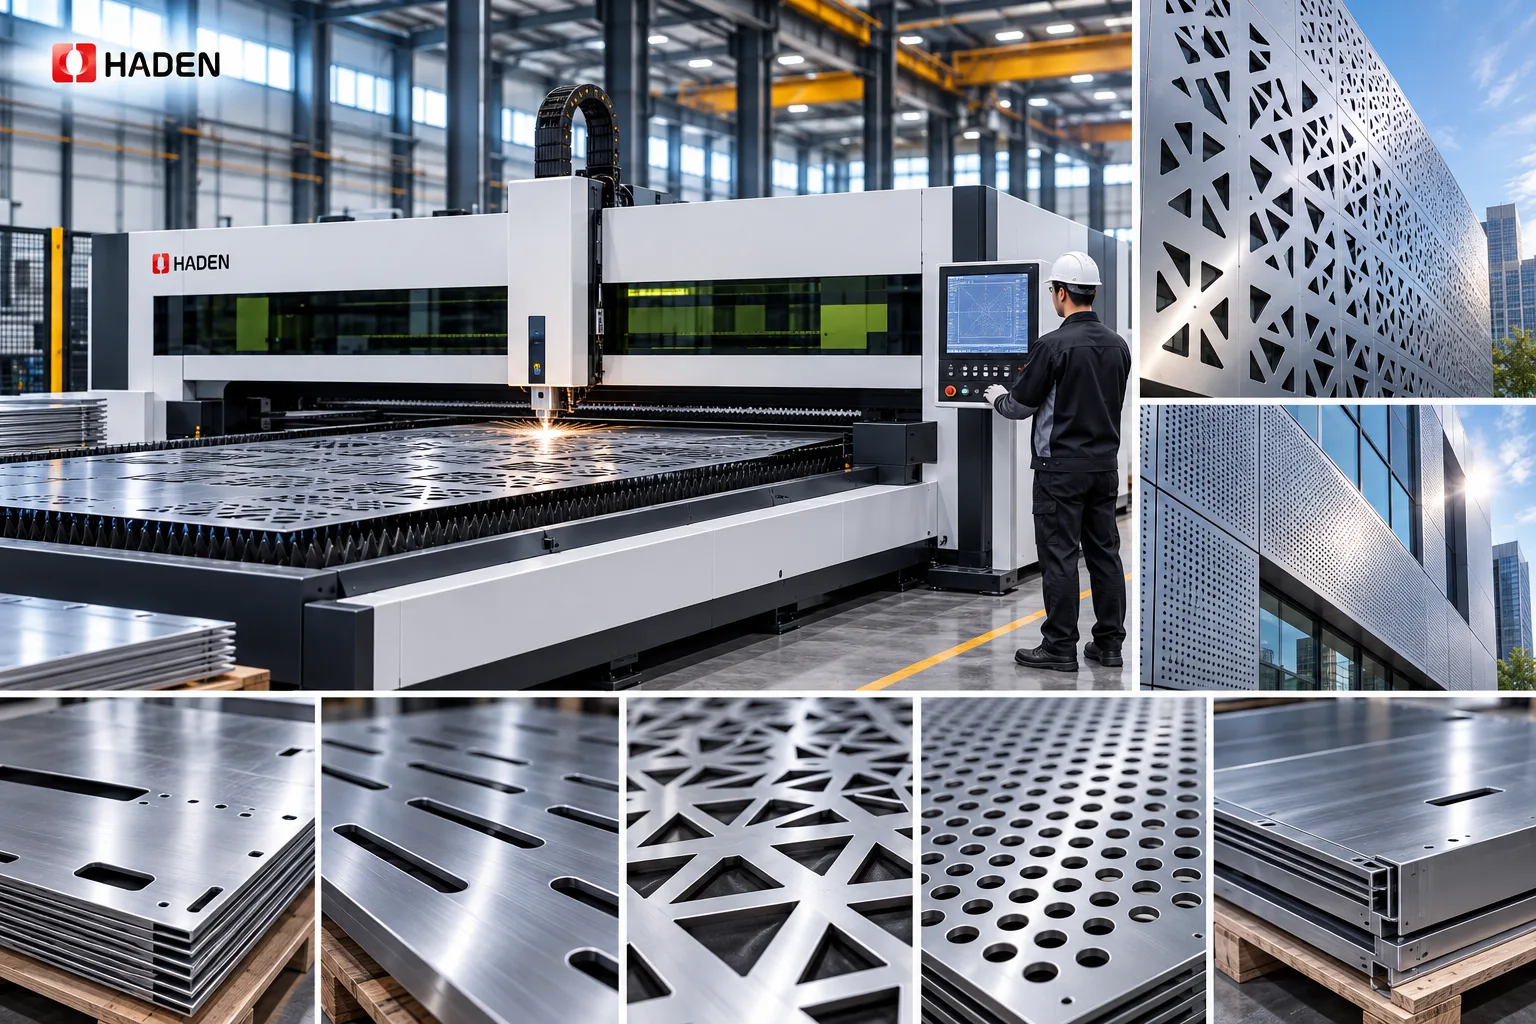
De-Coiling, Precision Leveling & Blanking
Relieve internal coil stress and achieve absolute sheet flatness before cutting. Haden servo blanking and precision leveling lines eliminate coil curvature, cross-bow, and edge-wave defects for seamless downstream processing with our automated coil-fed laser cutting machines.
Hydraulic high-capacity uncoiler with automated loop speed synchronization.
Multi-roller precision leveling bank with computerized cassette changeout.
Direct automated transfer into laser cutting cells or buffering stations.
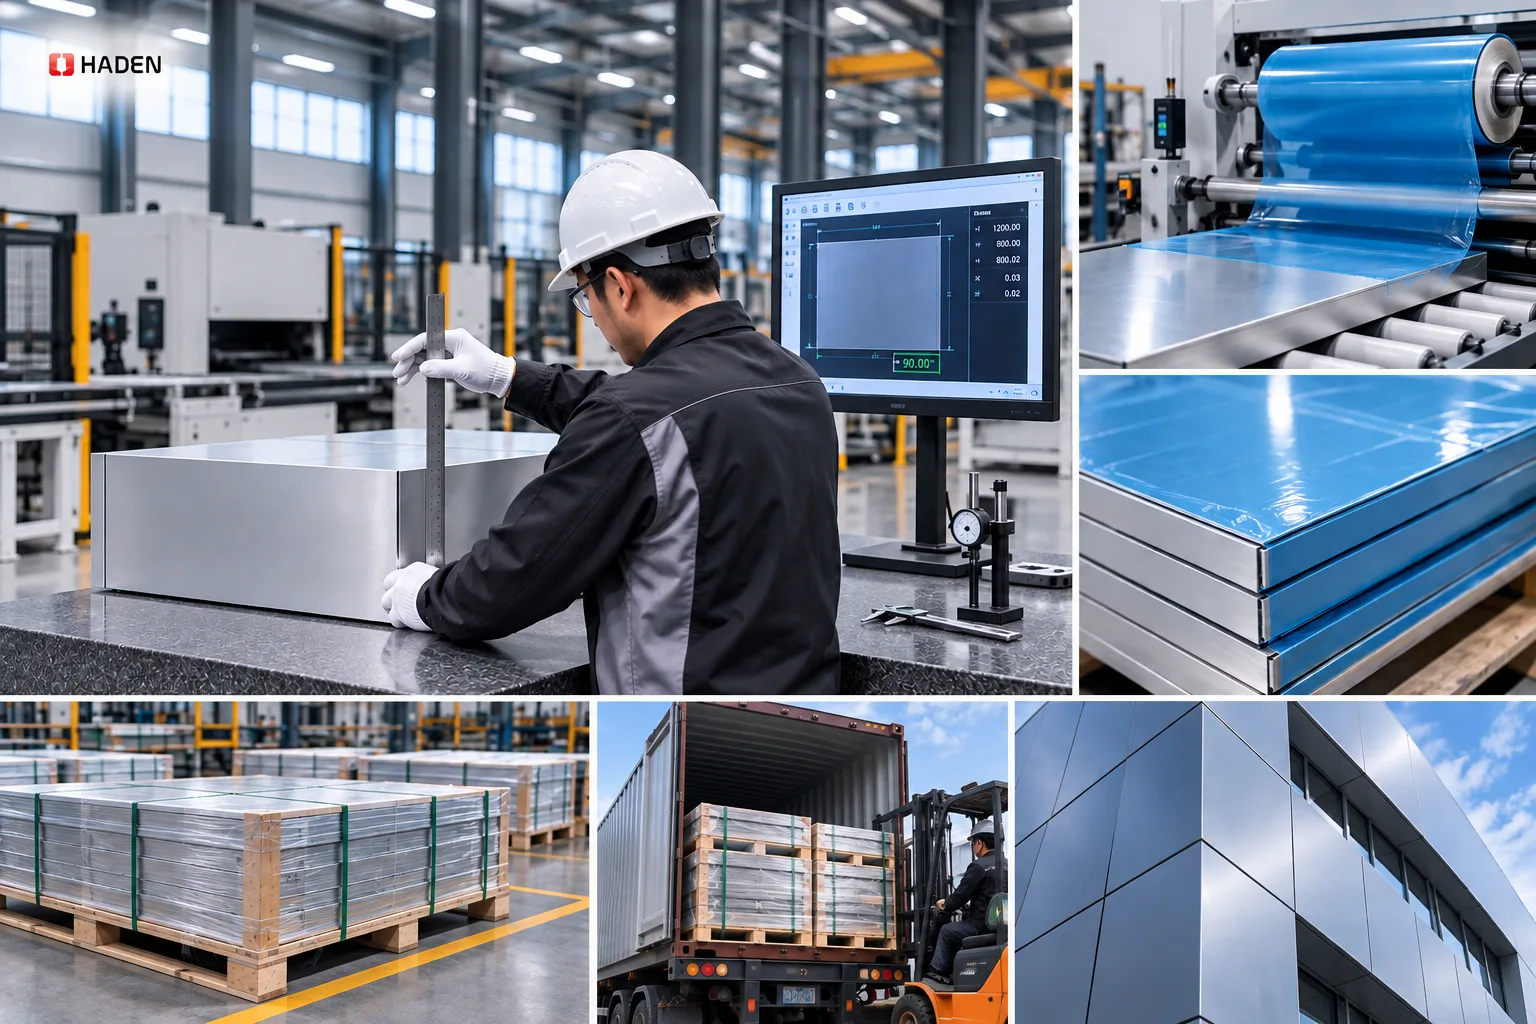
Turnkey Automated Flexible Sheet Metal Lines
Haden provides both standalone specialized CNC machine tools, including high-precision laser cutting machines, and fully integrated automated production cells engineered specifically for building envelope and architectural facade manufacturers worldwide.
Architectural Metal Material Processing Capabilities and Parameter Matrix
Explore precise engineering specifications across workable gauge thicknesses, specialized laser cutting machines, precision V-grooving depths, and CNC forming solutions for major architectural alloys. Engineered to eliminate surface defects, control material springback, and ensure seamless facade alignment.
| Material Type & Grade | Thickness Range | Cutting Method | Forming Process | Key Fabrication Advantages |
|---|---|---|---|---|
| Architectural Aluminum Alloys (1100, 3003, 5052, 6063 Series) | 1.0 mm – 6.0 mm (0.040" – 0.236") | High-Pressure Nitrogen Laser Cutting | Precision CNC V-Grooving + Urethane Die Bending | Eliminates micro-cracks before anodizing or PVDF coating; delivers zero tool scuffing on pre-finished panel faces. |
| Architectural Stainless Steel (AISI 304, 316, Mirror #8 & Hairline) | 0.8 mm – 4.0 mm (0.031" – 0.157") | Dual-Pulse Laser Vaporization with Film Preservation | Protective Film V-Groove + Roller-V Die Bending | Prevents laser protective film delamination and edge burn; produces crisp 90° razor edges with intact mirror finishes. |
| Weathering Steel Facades (Corten Steel A/B, ASTM A588 / A242) | 2.0 mm – 12.0 mm (0.078" – 0.472") | High-Wattage Fiber Laser Bevel Cutting (Up to ±45°) | Heavy-Tonnage Press Brake Forming with 42CrMo Hardened Tooling | Dross-free open-joint bevel preparation; dynamic crowning compensates for severe tensile yield springback. |
| Galvanized Structural Channels & Subframes (Q235B, S350GD, DX51D+Z) | 1.5 mm – 20.0 mm (0.059" – 0.787") | High-Speed Assist-Gas Laser Cutting (Nitrogen / Compressed Air) | Multi-Axis Tandem Synchronized Press Brake Bending | Maintains tight hole-to-bend pitch accuracy (±0.1 mm) across structural continuous profiles up to 12 meters. |
| Architectural Copper & Brass Cladding (C11000, C26000, Architectural Bronze) | 0.8 mm – 3.0 mm (0.031" – 0.118") | Anti-Reflective Fiber Laser Cutting with Optical Isolation | High-Speed Micro V-Groove + Elastic Urethane Tooling | Eliminates back-reflection beam damage; guarantees scratch-free, sharp cassette corners without edge wrinkling. |
Match Machine Parameters to Your Architectural Materials
Material type, thickness, surface condition, part geometry, and finishing requirements can all influence cutting, V-grooving, bending, and forming processes. Haden can help evaluate suitable machinery and process configurations for aluminum, stainless steel, coated sheet, and other architectural metal applications.
+ Automated Material Database Calibration
Haden CNC systems continuously adjust assist-gas pressures, dynamic focal lengths, and mechanical crowning tonnages based on alloy temper and thickness. Real-time feedback loops eliminate manual trial bends and scrap during alloy changeovers.
+ Zero-Scuff Surface Protection Technology
Integrated film-piercing laser modes and urethane-padded bending dies prevent heat scorching and mechanical die rubbing on mirror-polished stainless steel, prepainted stock handled by coil-fed laser cutting machines, and anodized architectural panels.
+ Wide Gauge & Extended Span Versatility
From ultra-thin 0.8 mm decorative copper sheets to heavy 20 mm structural baseplates, Haden machines deliver high dynamic rigidity, extended stroke depths, and tandem bending synchronization for oversized architectural assemblies.
+ International Building Code Compliance
Machined components consistently maintain tight geometric tolerances that satisfy ASTM E330 wind-load resistance and EN 13830 curtain walling standards, ensuring hassle-free installation on demanding global commercial jobsites.
Why Architectural Fabricators Choose Haden: Four Core Engineering Advantages
Engineered to meet demanding structural standards, Haden laser cutting machines and fabrication systems deliver continuous heavy-duty precision across facade panels, architectural framing, and bespoke metalwork.
Heavy-Duty Annealed Frames & Torsional Rigidity
Welded heavy steel plate structures undergo 600°C thermal stress-relief annealing and single-setup machining on a five-face gantry mill, preventing bed deflection over decades of high-tonnage runs.
Oversized Custom Machine Envelopes
Designed for large-scale curtain walls and long flashings, offering custom press brakes for construction with daylights to 1,200mm and sheet metal laser cutting machines with fiber tables up to 16m × 3.5m.
Seamless CAD/CAM/BIM System Interface
Directly import STEP, DXF, and IGES architectural models into the CNC controller to automate V-groove path plotting, bend sequencing, and flat blank calculations without manual re-drafting.
Global Application Engineering & Lifecycle Support
Ensure maximum CNC metal machinery reliability with factory-backed structural application support, hands-on operator training, and rapid 48-hour global spare part dispatch.
Engineered for Demanding Structural Tolerances and Continuous Output
Haden unifies robust mechanical construction, precision tube laser cutting machines, and closed-loop hydraulic crowning to keep architectural fabrication plants operating with high repeatability and zero unplanned downtime.
Global Architectural Landmark Case Studies & Client Verifications
Discover how tier-1 facade contractors and architectural metal fabricators leverage Haden high-precision laser cutting machines, V-grooving, and bending machinery to deliver complex building envelopes worldwide.
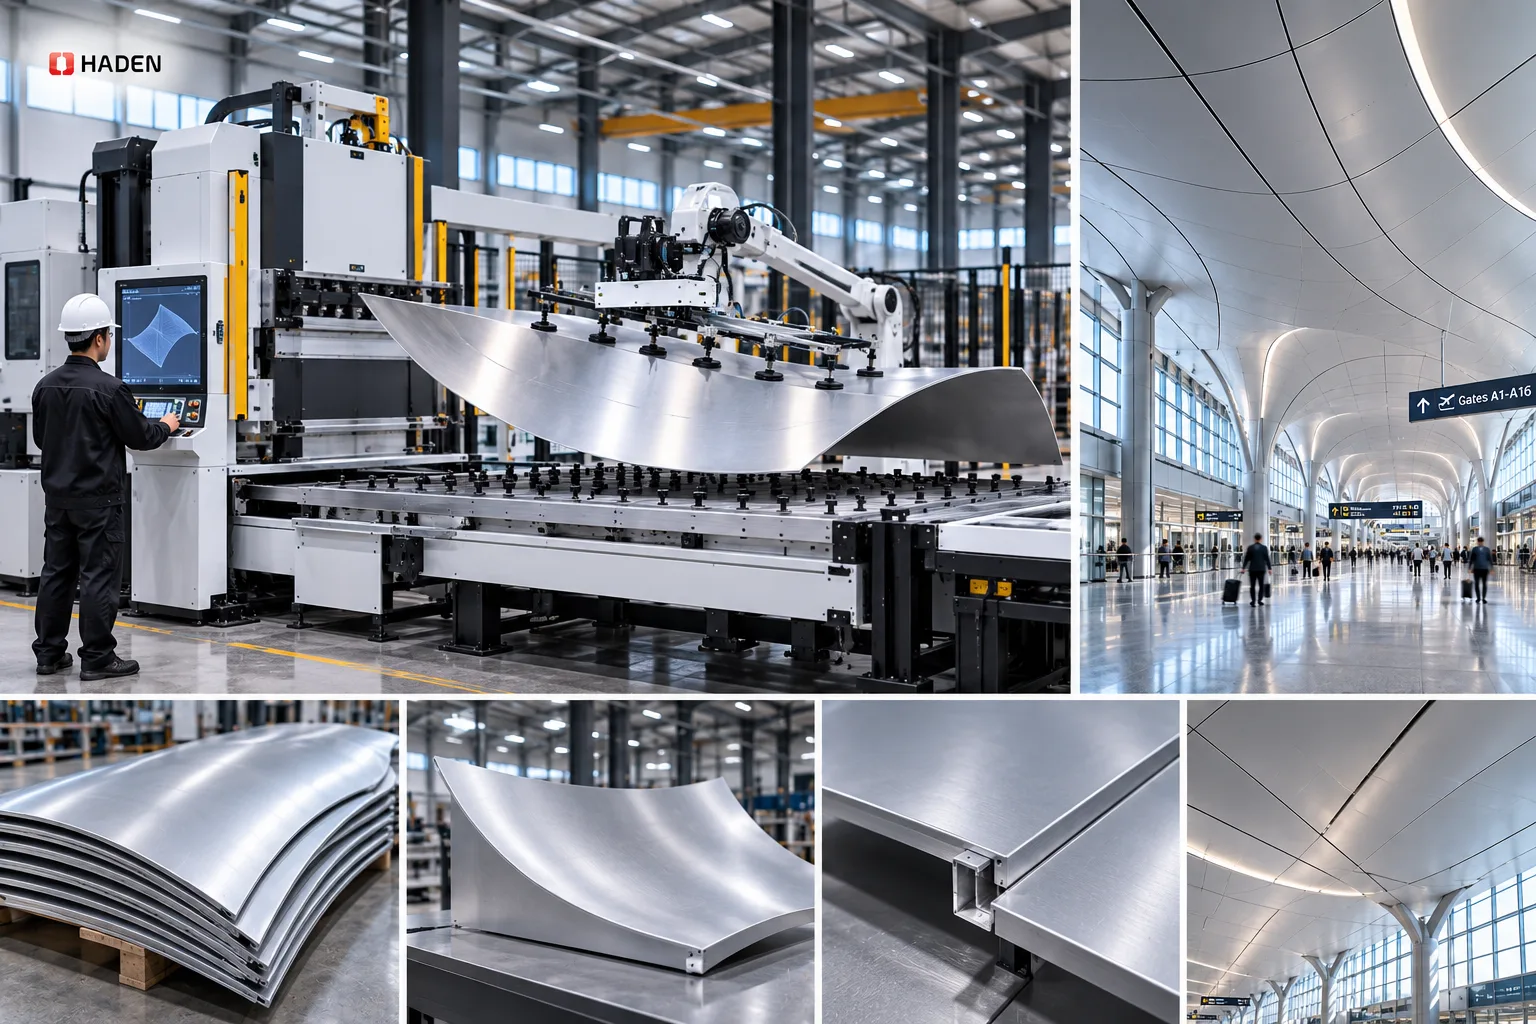
International Airport Terminal Hyperbolic Ceiling Production
DEPLOYED MACHINERY CONFIGURATION
Haden 6025 Large-Bed Fiber Laser + Automatic Panel Bending Center
VERIFIED PRODUCTION OUTCOMES
- • Delivered 140,000 m² of perforated double-curved architectural ceiling cassettes
- • Sustained daily output exceeding 1,200 m² with scrap rates below 0.2%
- • Improved joint seam uniformity by 30% compared to conventional press brakes
High-dynamic sheet metal laser cutting machines eliminated heat distortion across complex acoustic perforation patterns, while automated panel folding formed 3D cassette profiles without tool-change bottlenecks.
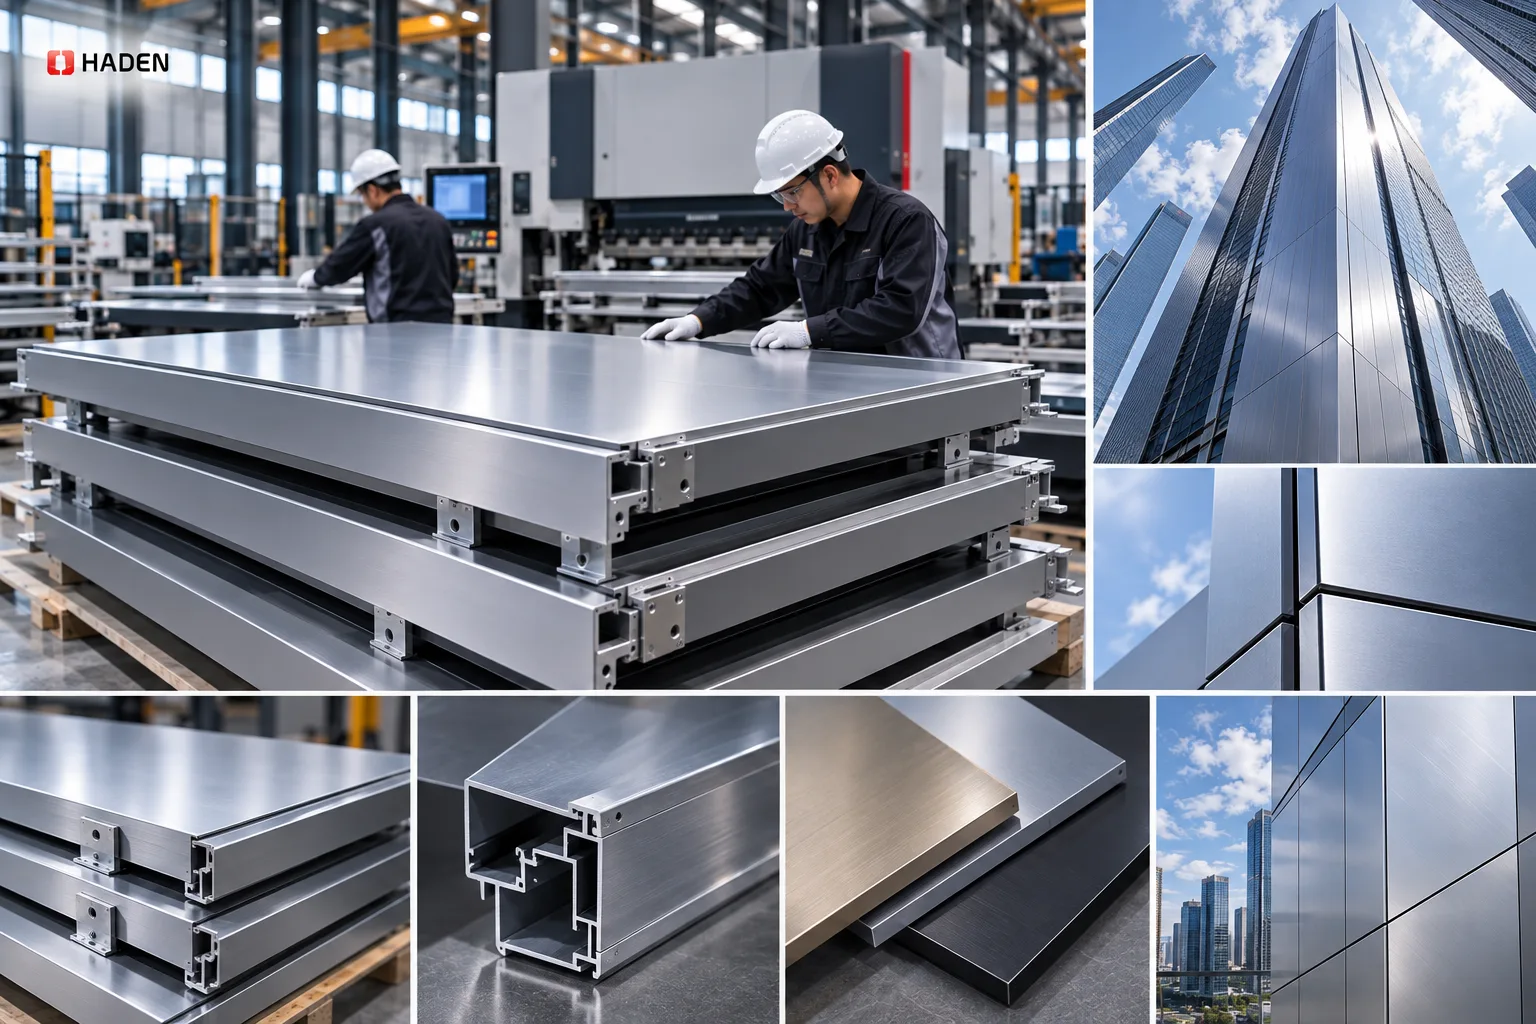
Supertall Commercial Tower Anodized Cladding Cassette System
DEPLOYED MACHINERY CONFIGURATION
Haden Vertical CNC V-Groover + 8000 mm 600T Tandem Press Brake
VERIFIED PRODUCTION OUTCOMES
- • Fabricated 6-meter anodized aluminum exterior panels with zero corner crazing
- • Passed ASTM E283 air leakage and ASTM E331 water penetration tests on first trial
- • Maintained ±0.3° angular accuracy across full panel spans via dynamic crowning
Synchronized V-grooving lowered bending resistance by 50%, completely avoiding anodized surface fracture while delivering crisp, ultra-narrow 90° shadow-line joints for the skyscraper facade.
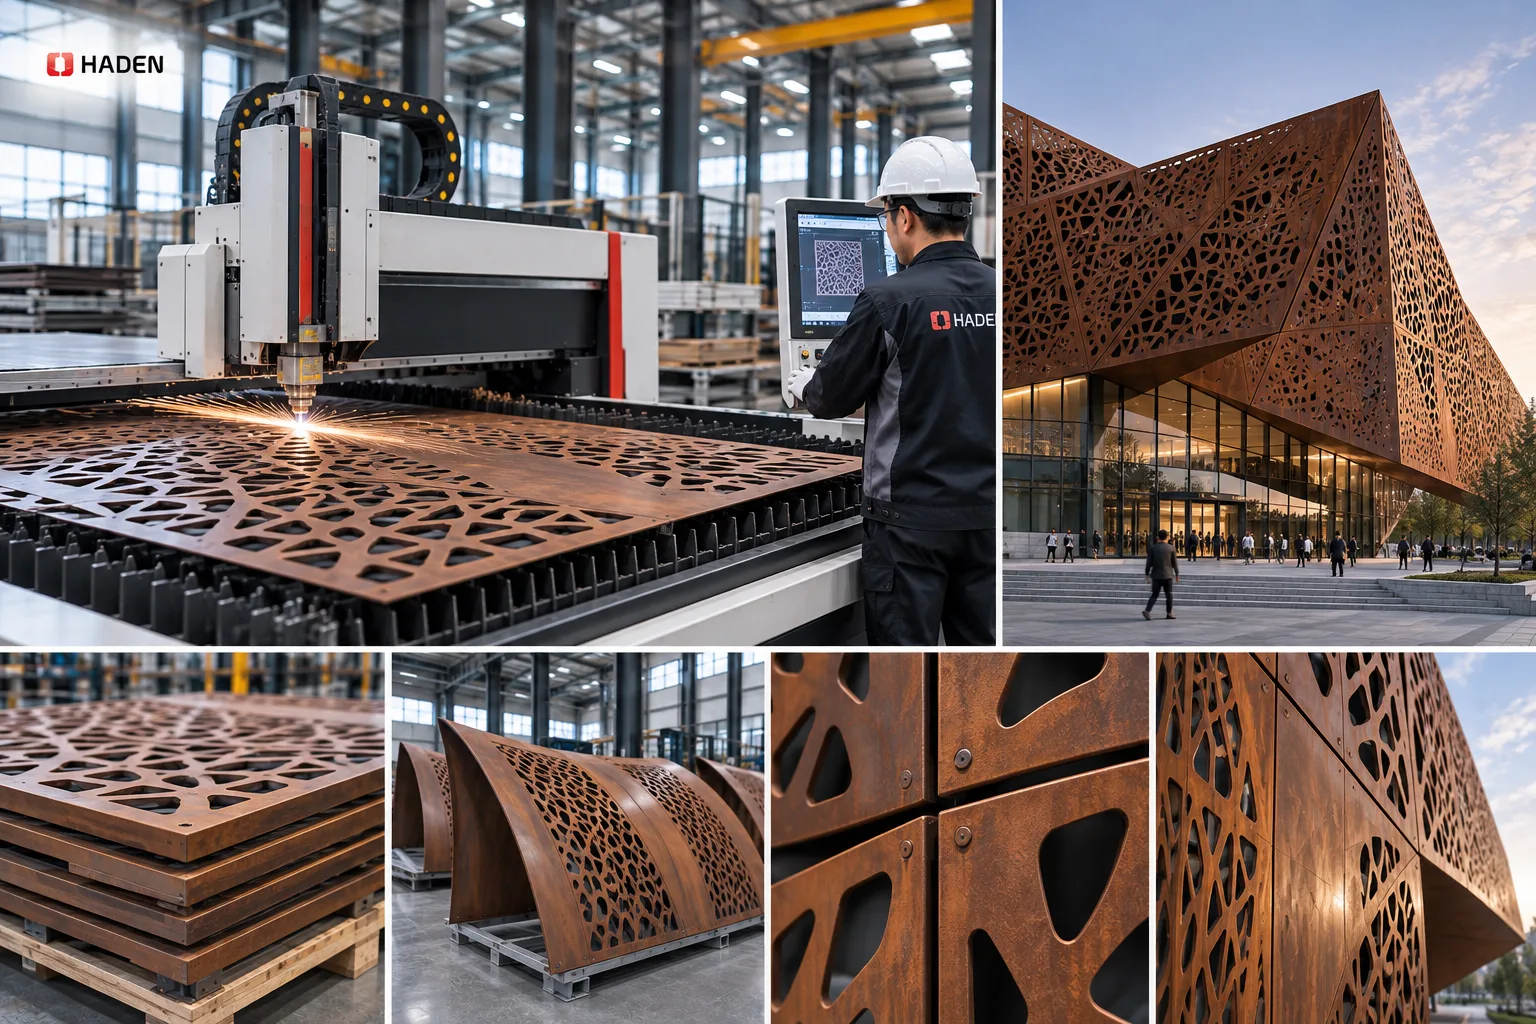
Civic Cultural Center Parametric Corten Steel Facade
DEPLOYED MACHINERY CONFIGURATION
Haden 12 kW High-Power Fiber Laser + Precision 4-Roll Plate Rolling Machine
VERIFIED PRODUCTION OUTCOMES
- • Processed over 45,000 parametric perforations with 100% dross-free, clean edge finish
- • Formed variable-radius weathering steel fins with virtually zero unbent flat ends
- • Boosted plate material utilization by 18.5% through intelligent common-line nesting
High-pressure sheet and tube laser cutting machines preserved the chemical integrity of weathering steel edges, while 4-roll planetary bending ensured consistent radial curvature without secondary surface rework.
Explore Sheet Metal Machinery Applications in Architectural Fabrication
Explore how laser cutting, bending, V-grooving, panel forming, plate rolling, and leveling equipment can be configured for facade panels, cladding systems, structural metalwork, decorative components, and other architectural fabrication applications.
Why Global Architectural Fabricators Trust Haden Equipment
Average machine uptime in commercial facade production facilities
Rapid international dispatch for critical technical support and tooling
Direct CAD/BIM model unfolding with zero manual programming error
Stress-relieved annealed frames ensuring lifelong geometric precision
Architectural Sheet Metal Fabrication Equipment: Technical FAQ
Fabricating high-performance architectural facades, aluminum curtain wall cassettes, structural brackets, and decorative perforated metal panels requires uncompromising precision, tight bend tolerances, and complete surface protection. Review our engineering guide addressing kinematics, CNC crowning systems, scratch-free forming, and custom machine configurations.
Why is CNC V-grooving recommended before bending architectural aluminum and stainless facade panels?
Direct air bending on a conventional press brake naturally produces an outer bend radius proportional to the material thickness (R = 1.5t to 2.2t). On heavy 3.0mm to 4.0mm solid aluminum cladding or 2.0mm architectural stainless steel, direct forming creates wide, rounded corners that produce visible joint reveals, optical distortions, and uneven shadow lines across building envelopes.
High-speed CNC V-grooving cuts a micro-precision relief channel along the fold datum before bending, leaving a strictly controlled residual web thickness (typically 0.6mm to 1.0mm). This delivers measurable structural and aesthetic advantages:
- Sharp Corner Radii: Produces an outside radius of R < 0.5mm, achieving seamless 90° cassette edges and flush joints specified in modern architectural envelopes.
- 40% to 60% Tonnage Reduction: Relieving material mass along the bend line dramatically lowers the required press brake tonnage, minimizing machine frame deflection and tool wear.
- Crack & Crazing Prevention: Reduces outer tensile strain during bending, preventing surface micro-fissures and coating discoloration on PVDF-painted aluminum, anodized sheets, and architectural brass.
How do tandem CNC press brakes maintain uniform bend angles across 8-meter to 12-meter architectural profiles?
Architectural curtain wall mullions, roof flashings, fascia gutters, and structural supports often require continuous lengths of 8 to 12 meters. Bending these extended profiles on conventional uncompensated equipment causes angular canoe deflection, resulting in open angles along the center and tight angles at the ends due to machine side-frame deflection and bed deformation under load.
Haden tandem synchronized press brake systems resolve angular variance across extra-long parts through an integrated multi-tier control setup:
Dynamic CNC Crowning
Multi-point CNC dynamic mechanical wave crowning automatically calculates elastic bed deflection based on material yield strength, sheet thickness, and tonnage, applying real-time micro-curve compensation along the lower beam.
EtherCAT High-Speed Synchronization
High-resolution optical linear encoders mounted on decoupled side frames monitor the Y1/Y2/Y3/Y4 ram axes, synchronizing dual hydraulic circuits through electro-proportional valves with millisecond response times.
This electro-hydraulic coordination holds angle tolerances within ±0.3° across the entire profile length, eliminating manual post-forming adjustments during curtain wall framing installation.
How do fiber laser cutting systems prevent protective film burning on mirror stainless steel and coated aluminum?
Architectural metal panels often carry laser-grade PE, PVC, or fiber-protective films to safeguard hairline, No.4, mirror (No.8), or pre-anodized finishes during handling. Conventional single-pass laser cutting frequently leads to film bubble formation, edge carbonization, and adhesive melting, resulting in burnt edges and labor-intensive manual cleaning.
Haden high-performance sheet metal laser cutting machines incorporate an automated two-stage film-evaporation cutting process developed for architectural materials:
- Stage 1 - Low-Power Film Slitting: A high-frequency, defocused laser beam scans the cutting contour first, vaporizing a narrow channel through the protective film without transferring excess heat into the underlying metallic substrate.
- Stage 2 - High-Pressure Nitrogen Cutting: The cutting head instantly follows with ultra-pure nitrogen assist gas (18 to 25 bar), cleanly ejecting molten metal to create an oxide-free, burr-free edge while keeping the adjacent protective film firmly bonded.
This method allows facade sheets to proceed directly from laser cutting into CNC grooving and folding stations with flawless surface finishes and intact film coverage.
How should architectural fabricators choose between an Automatic Panel Bender and a CNC Tandem Press Brake?
Both machine types are core assets in architectural sheet metal production, but each addresses distinct component geometries, material gauges, and batch volumes:
| Selection Criteria | Automatic CNC Panel Bender | Tandem CNC Press Brake System |
|---|---|---|
| Target Workpieces | Standard ceiling tiles, 4-sided cassette pans, elevator door panels, acoustic baffles | Continuous mullions, heavy structural brackets, oversized roof flashings, perimeter fascias |
| Working Envelope | Up to 2500mm × 1500mm; thicknesses up to 3.0mm Al / 2.0mm Steel | Lengths from 4000mm to 12000mm+; thicknesses up to 20mm plate |
| Forming Speed & Cycle | Universal folding blades: 4-sided panel completed in 20–35 seconds with zero setup changes | Standard stroke cycling; suited for sequential deep bends and custom multi-step profiles |
| Operator Intervention | Single operator loading or continuous automated robotic integration | 1 to 2 operators assisted by automated sheet followers for wide, heavy parts |
Engineering Recommendation: Facilities producing high volumes of standardized cassettes and metal ceiling systems gain the shortest payback with Haden Automatic Panel Benders, while contractors manufacturing long structural profiles, custom flashings, and heavy brackets should select Haden Synchronized Tandem Press Brakes.
Can Haden customize machine throat depth, daylight opening, and non-marking tooling for complex architectural profiles?
Yes. Architectural components routinely exceed the dimensional clearances of standard sheet metal machinery. Deep cassette returns, narrow internal channels, and oversized exterior parapets require custom machine geometry to prevent sheet collisions with the upper beam or side housings.
Haden provides engineered-to-order machine customizations and specialized tooling for facade and interior manufacturers, including:
- Extended Daylight & Deep Throats: Open daylight heights up to 1200mm and throat depths exceeding 1000mm to accommodate deep returns and complex box shapes.
- Scratch-Free Tooling Packages: Precision-ground 42CrMo punches paired with polyurethane lower die inserts and roller-bearing V-dies, eliminating tooling drag marks on painted and polished surfaces.
- Extra-Large Cutting Formats: Large-format laser cutting machines built with table sizes up to 16m × 3.5m and multi-zone partitioned exhaust systems for oversized screen and cladding production.
Haden application specialists evaluate your DXF and STEP component files to run collision analyses, tonnage calculations, and bend simulations prior to equipment fabrication, supporting both solid panel forming and hollow structural profiles processed on high-performance tube laser cutting machines.
Discuss Your Architectural Sheet Metal Manufacturing Project with Haden
Share your architectural components, materials, drawings, and production requirements. Haden engineers can help evaluate suitable cutting, bending, V-grooving, panel forming, rolling, leveling, and automation configurations for your fabrication project.
Parts & Drawings
Component drawings, CAD files, dimensions, profiles, or representative architectural parts.
Materials & Processes
Material type, thickness range, surface requirements, and cutting, grooving, bending, or forming processes.
Production Requirements
Production volume, process flow, automation targets, and available factory space.