
Sheet Metal Machinery Case Studies Across Real Manufacturing Applications
Explore Haden machinery projects across cutting, bending, rolling, leveling, and automated production applications. See how equipment configurations are matched to different materials, part geometries, production requirements, and factory workflows, including custom automated sheet metal production lines .
Project Coverage
Sheet, tube, and coil-fed laser cutting applications
Press brake, panel bending, and robotic forming projects
Plate rolling, shearing, and V-grooving applications
Integrated lines, material handling, and custom workflows
Sheet Metal Machinery Projects Across Global Applications
Explore representative Haden machinery applications across cutting, bending, rolling, forming, and automated production. Filter projects by equipment category and industry, then contact our team to request additional technical information relevant to your production requirements.
Customer identities, facility images, and confidential production information are not displayed publicly. Additional project information can be discussed based on the scope and confidentiality requirements of each reference.
Showing 12 representative applications
Detailed project information is available upon request.
HVAC Ductwork Laser Cutting
EuropeLaser cutting configuration for galvanized and stainless steel duct components requiring flexible profiling and consistent cut quality.
Electrical Enclosure Panel Bending
Southeast AsiaCNC bending configuration for enclosure panels requiring multiple bends, repeatable positioning, and controlled forming sequences.
Automotive Aluminum Component Forming
North AmericaFlexible panel bending application for aluminum components requiring controlled forming sequences and repeatable production.
Pressure Vessel Shell Rolling
Middle EastHeavy plate rolling configuration for cylindrical vessel components requiring edge pre-bending and controlled forming of thick plate.
Architectural Stainless Steel Fabrication
EuropeIntegrated cutting and forming application for architectural stainless panels requiring controlled processing and protected surface finishes.
Integrated Coil-Fed Laser Blanking Line
South AmericaIntegrated coil processing configuration combining material feeding, leveling, laser blanking, and downstream production handling.
Commercial Kitchen Equipment Bending
Western EuropeFlexible bending application for stainless foodservice equipment requiring multiple part geometries and frequent production changes.
HVAC Flange & Duct Forming
Northern EuropePress brake configuration for galvanized duct components requiring repeatable flange positioning and controlled sheet handling.
Switchgear Panel Precision Cutting
East AsiaLaser cutting application for switchgear and enclosure panels with dense apertures, cutouts, and varied component geometries.
Agricultural Equipment Plate Rolling
Latin AmericaPlate rolling application for structural agricultural components, cylindrical parts, and variable-geometry formed sections.
Automotive Panel Forming & Hemming
GermanyPrecision press brake application for automotive sheet components requiring controlled bending and protection of finished surfaces.
Robotic Power Cabinet Bending Cell
North AmericaAutomated bending cell integrating material handling, robotic loading, flexible panel forming, and downstream part handling.
No Matching Applications Found
Try another category or contact Haden for project references related to your application.
Looking for a Case Similar to Your Production Requirement?
Tell us your material, part dimensions, process requirements, production volume, and target equipment. Our team can discuss relevant application references and available technical details while respecting customer confidentiality.
Flagship Turnkey Engineering Project Deep Dives
Examine how Haden engineers overcome complex sheet metal forming, heavy plate rolling, and advanced laser cutting machines integration challenges worldwide. Each deep dive explores initial operational bottlenecks, customized machine architectures, closed-loop CNC compensation algorithms, and verified production yield improvements across demanding manufacturing sectors.
Automated Commercial Kitchen Equipment Flexible Bending Line Case Review
A leading European commercial refrigeration and catering equipment manufacturer required high-precision, scratch-free sheet forming for sanitary AISI 304 and AISI 316 stainless steel panels. Their previous workflow relied on multiple conventional hydraulic press brakes, generating severe tooling scuff marks on #4 brushed aesthetic surfaces and requiring 20- to 30-minute manual tool reconfigurations between small-batch part geometries.
Haden deployed a fully automated turnkey panel bending cell integrated with dual-pallet vacuum de-stacking, automated part centering, and real-time optical sheet thickness compensation. The servo-electric universal bending blades execute continuous positive and negative bends without dedicated die changeovers, safeguarding architectural surface integrity and slashing batch transition downtime.
Technical Implementation Highlights
- Closed-Loop Thickness Sensing: High-resolution optical sensors measure sheet gauge variations on the fly, auto-adjusting stroke depths to eliminate angle drift.
- Multi-Axis Robotic Rotator: Seamlessly maneuvers complex 2500 mm x 1250 mm wrapper panels through multi-sided reverse flanges in a single continuous clamp cycle.
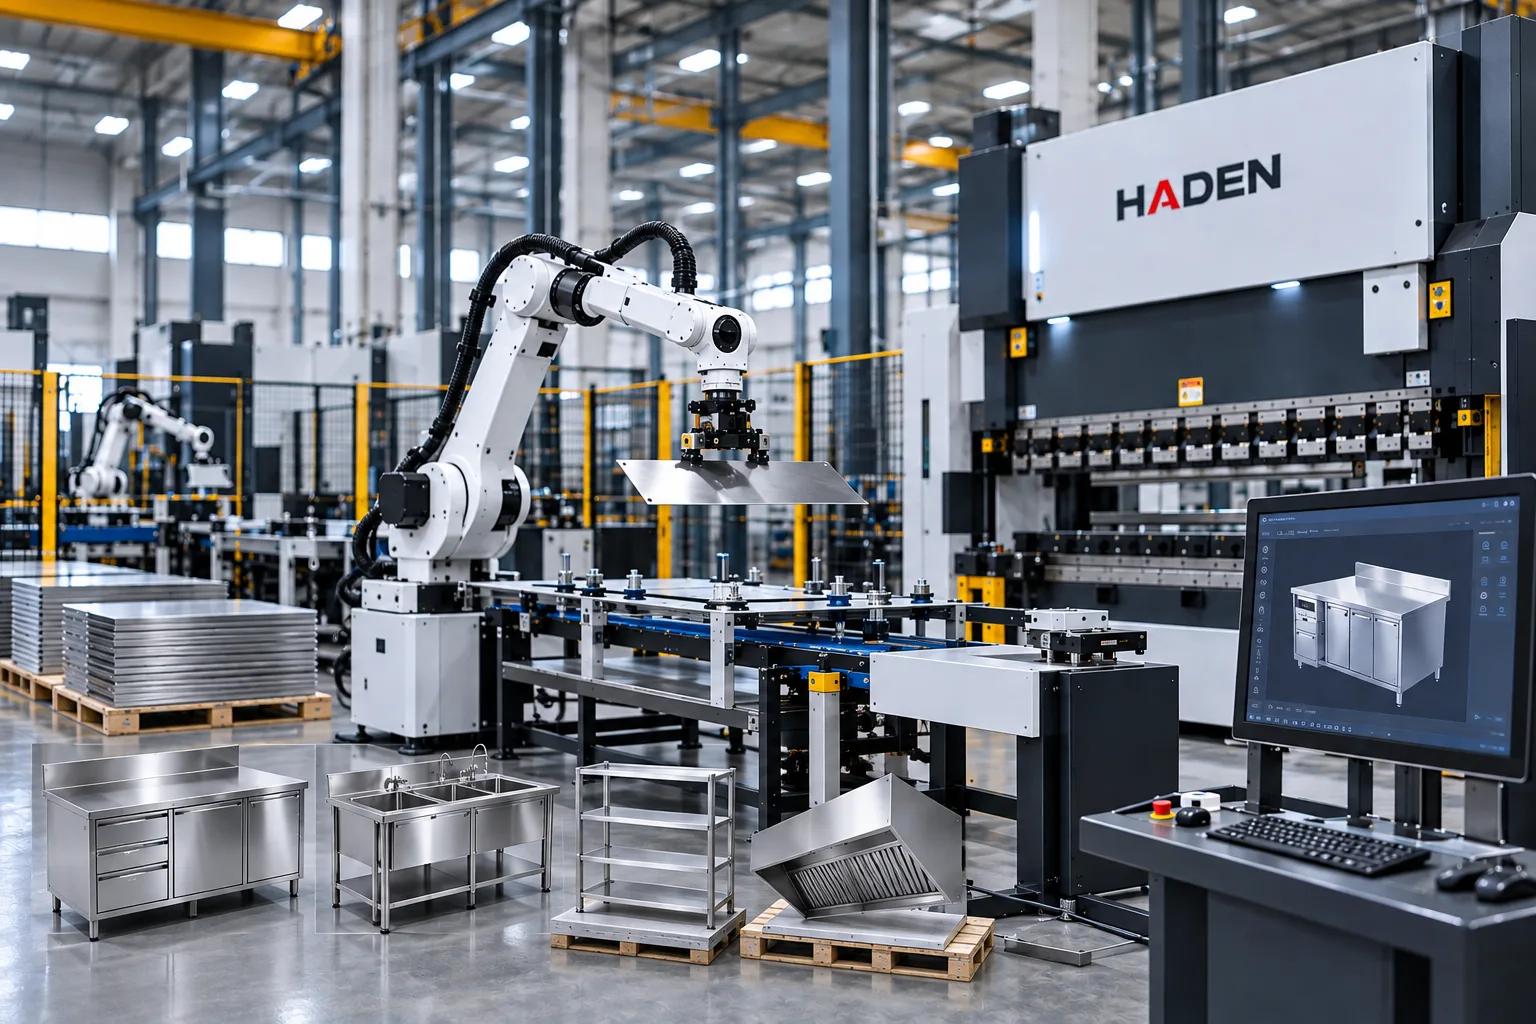
Commissioned: Frankfurt, Germany | Material: 1.2–2.0mm AISI 304 Stainless

Commissioned: Jubail, Saudi Arabia | Material: 65–80mm SA516 Gr 70 Heavy Boiler Plate
Heavy Duty Petrochemical Pressure Vessel Plate Rolling Engineering Analysis
A major Middle Eastern process equipment manufacturer faced excessive straight unbent flat edges and barrel-shaped shell distortion when rolling high-tensile SA516 Grade 70 boiler plate up to 80 mm in thickness. Excessive roll deflection during conventional symmetric 3-roll bending necessitated costly secondary press-brake edge pre-crimping and labor-intensive manual edge grinding before longitudinal seam submerged-arc welding (SAW).
Haden designed and delivered a high-capacity 3,000-ton hydraulic 4-roll CNC plate rolling machine equipped with dynamic hydraulic roll crowning compensation and proportional electro-hydraulic roll tilt synchronization. By securing the plate between the top and bottom pinch rolls, the system pre-bends leading and trailing edges in a single continuous pass, eliminating plate slippage and preserving tight circular geometry.
Structural & Hydraulic Engineering Highlights
- Planetary Swing Arm Roll Guides: Delivers superior mechanical leverage closer to the roll center, enabling tighter cylinder diameters without frame deflection.
- Overhead Hydraulic Shell Support: Fully synchronized top crane support sustains shells up to 4,500 mm in diameter, preventing gravitational ovalization during rolling.
Integrated Power Distribution Cabinet Coil-Fed Laser Bending System Study
A high-capacity North American industrial enclosure manufacturer was constrained by excessive sheet metal off-cut scrap and intermediate work-in-progress (WIP) buffers between shearing stations and manual press brakes. Fabricating modular NEMA 4X power distribution cabinets demanded high-density ventilation cutouts, exact knockouts, and rapid multi-bend profiles on galvanized steel, shifting legacy processes toward automated sheet metal laser cutting machines.
Haden engineered a comprehensive continuous turnkey production line integrating a decoiler, precision 19-roll leveling machine, dynamic coil-fed laser cutting machines, and automated tandem servo press brake cells. Proprietary nesting software optimizes full coil width with continuous common-line cutting, removing skeleton scrap and staging finished blanks directly into bending grippers.
Automation Workflow Integration
- On-The-Fly Dynamic Fiber Laser Piercing: The laser cutting head tracks continuous strip movement without stopping material feed, reducing thermal distortion across thin sheet profiles.
- 6-Axis Synchronized Transfer Robot: Executes direct blank transfer from the laser unloader table to the tandem CNC press brake backgauge without manual pallet staging.
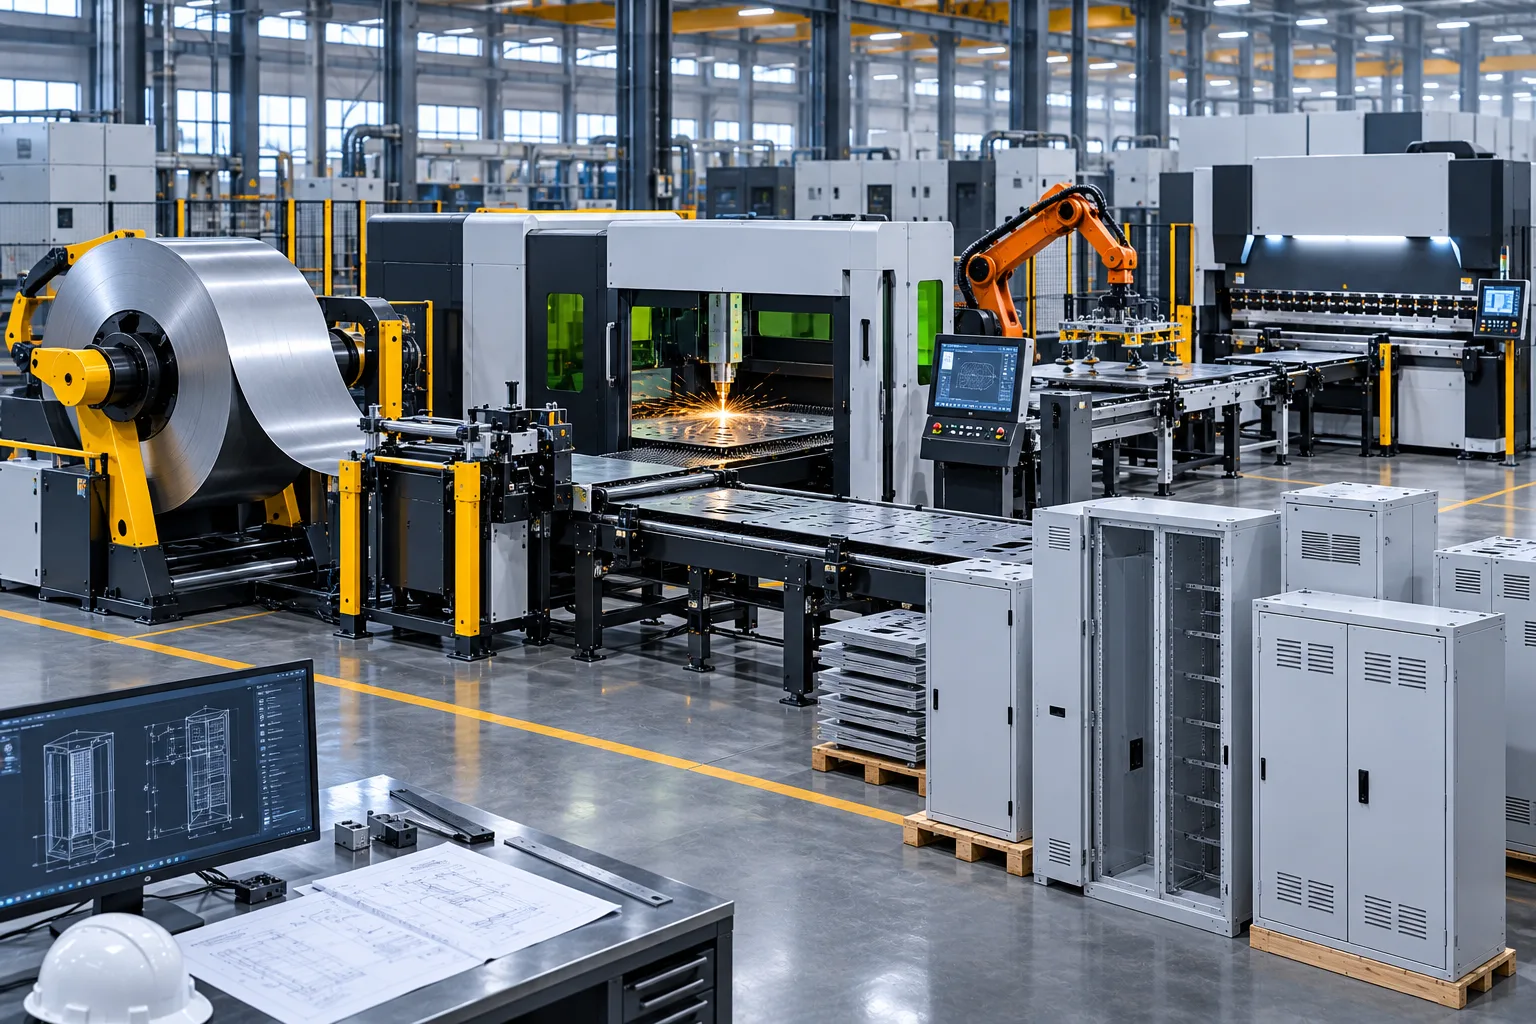
Commissioned: Monterrey, Mexico | Material: 1.5–3.0mm Galvanized Coil
Parametric Performance Comparison and Quality Verification Metrics
The table below highlights audited manufacturing data collected across these three flagship turnkey projects during rigorous Factory Acceptance Testing (FAT) and continuous multi-shift production at customer facilities.
| Project Application | Processed Workpiece Material | Haden Machine Configuration | Dimensional Tolerance | Cycle Time Reduction | Scrap Rate Impact | Verified ROI Period |
|---|---|---|---|---|---|---|
| Commercial Kitchen Panels | AISI 304 / 316 Stainless (1.2–2.0 mm) | Servo Flexible Panel Bender + De-Stacker | ±0.05 mm / ±0.2° | 79.4% Reduction | Reduced from 4.2% to 0.08% | 9.4 Months |
| Petrochemical Pressure Shells | SA516 Gr 70 Boiler Plate (Up to 80 mm) | 4-Roll 3,000-Ton CNC Plate Rolling Machine | ±0.50 mm (Roundness) | 55.0% Reduction | Reduced from 6.5% to 0.30% | 11.8 Months |
| Modular Electrical Enclosures | Galvanized Coil Strip (1.5–3.0 mm) | Coil-Fed Fiber Laser + Tandem Press Brake | ±0.08 mm (Hole Spacing) | 62.5% Reduction | Reduced from 18.0% to 6.4% | 8.2 Months |
Industry-Specific Sheet Metal Fabrication Transformation Hub
Off-the-shelf metalworking machinery frequently falls short when confronted with specialized metallurgical behaviors, strict surface finish requirements, and narrow dimensional tolerances. Haden designs and commissions application-dedicated fabrication lines calibrated to overcome unique manufacturing bottlenecks—from high-velocity galvanized duct seaming to zero-scratch mirror-finish architectural grooving.
Our multi-axis fiber lasers, servo-electric panel benders, synchronous CNC press brakes, and roll forming lines integrate custom tooling packages and real-time springback compensation algorithms. Review the field-proven deployments below to see how our sector-engineered installations shorten cycle times, eliminate manual rework, and secure measurable ROI across demanding manufacturing environments.
Solving Micro-Cracking, Tooling Marring, and Springback at Production Speed
Forming diverse alloy families demands closed-loop pressure monitoring, scratch-free sheet handling, and dynamic material thickness compensation. Haden application engineering integrates custom backgauge kinematics, specialized urethane tooling, automated brush support tables, and high-frequency servo drives directly into your production line.
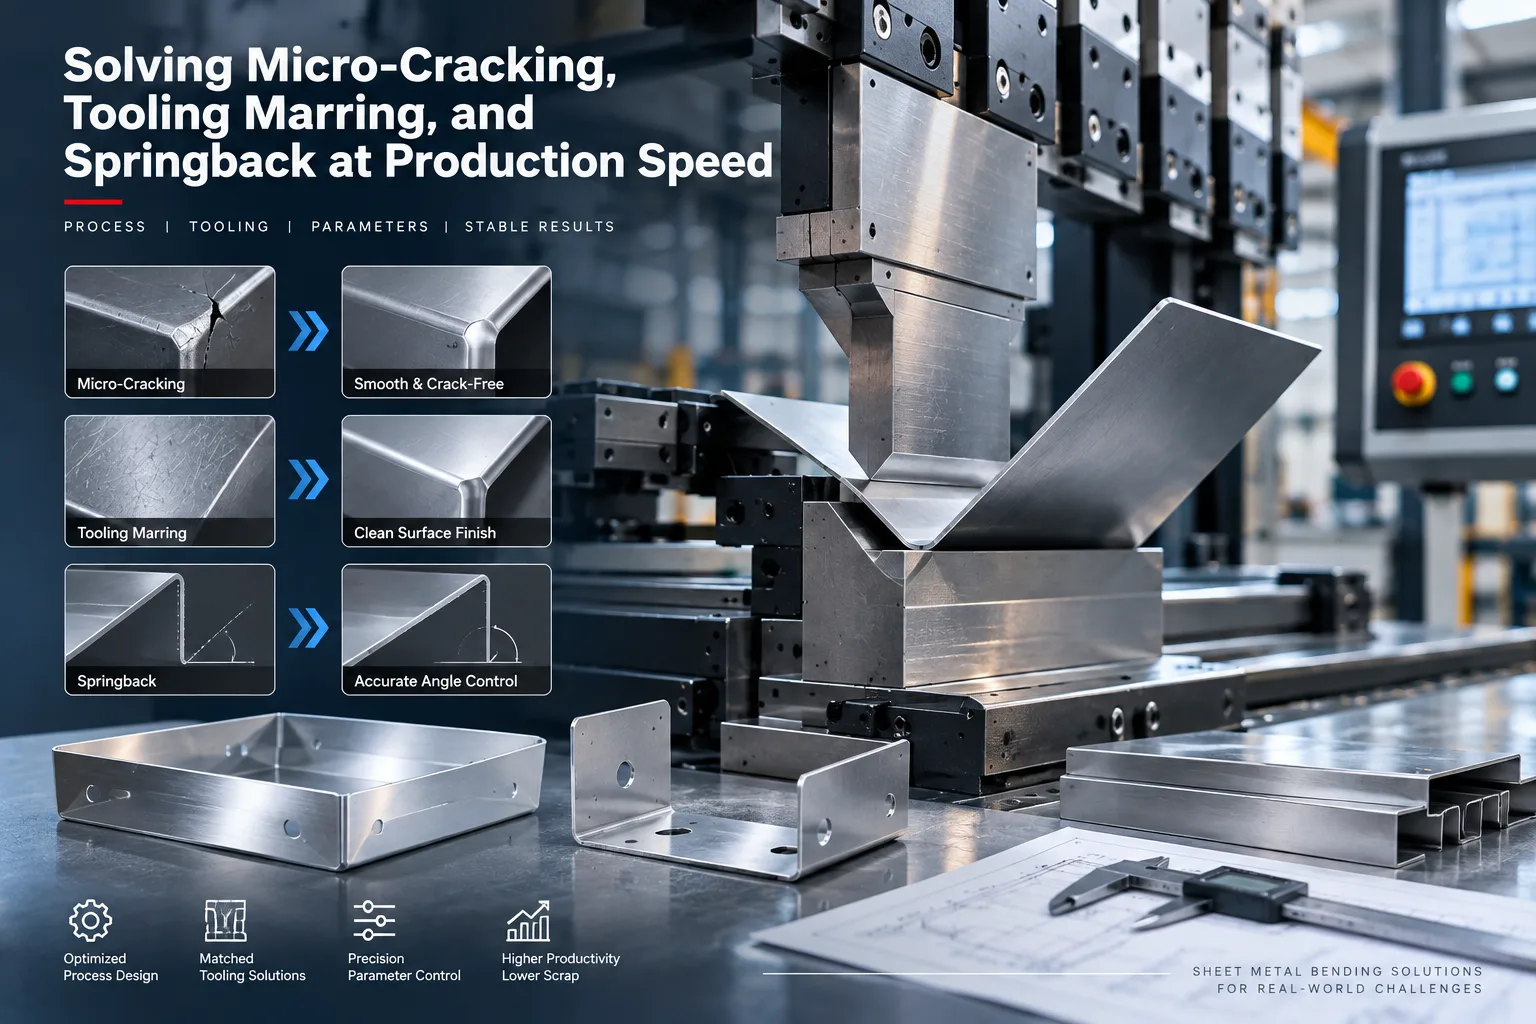
HVAC & Environmental Ductwork: High-Speed Flange and Lock Forming
Commercial HVAC fabrication demands continuous high-volume blanking, seam locking, and TDF/TDC flange forming without peeling protective zinc coatings or warping thin-gauge galvanized sheets.
High-Speed Pittsburgh Lock Forming: Eliminates seam separation under high static operating pressures up to 2,500 Pa during airtight duct certification.
Anti-Flaking Chrome Roll Dies: Micro-polished 40Cr tooling rollers prevent zinc spangle delamination and micro-fractures across Z275 galvanized coils.
Automated Duct Coil Lines: Integrated decoiling, leveling, beading, punching, and flanging achieve 18-second cycle times per complete duct section.
Electrical Enclosures & Server Racks: Scratch-Free Hemming and Panel Bending
Precision server racks, IT chassis, and NEMA-rated electrical enclosures require tight geometric orthogonality, multi-bend returns, and zero surface indentation on pre-painted or electro-galvanized sheets.
Servo-Electric Multilateral Bending: Universal tooling forms positive, negative, and return bends in a single continuous cycle without mechanical setup changes.
Safe-Edge Dutch Hemming: High-tonnage controlled flattening produces burr-free perimeter returns for uncompromised IP65 and NEMA enclosure gasket sealing.
Scratch-Free Brush Feed Tables: High-density nylon brush tables and vacuum positioners eliminate friction abrasions across pre-coated sheet stock.
Automotive Structural Components: High-Strength Steel and Aluminum Forming
Forming automotive crossmembers, EV battery housing trays, and chassis subframes in ultra-high-strength steel (UHSS) and 6000-series aluminum requires high tonnage combined with dynamic springback compensation.
Real-Time Laser Angle Correction: Optical sensors measure live material springback during ram stroke, automatically adjusting penetration depth on 980+ MPa steels.
Controlled Strain-Rate Forming: Variable-speed hydraulic kinematics prevent tensile shear tearing and grain boundary micro-cracks in 5052 and 6061 aluminum.
Heavy-Duty CNC Crowning: 800-ton synchronous tandem systems maintain full-bed deflection control within 0.02 mm/m for accurate robot welding assembly.
Architectural Metalwork: Mirror-Finish Stainless Steel V-Grooving & Bending
Luxury curtain walls, elevator cabs, and decorative entrance portals fabricated from #8 mirror-finish stainless or PVD-coated sheets require sharp zero-radius bend lines without tensile strain marks or surface cracking.
High-Precision CNC V-Grooving: Cuts precise micro-grooves along bend axes to achieve sharp 90-degree internal radii without surface stress whitening.
Anti-Marking Urethane Tooling: Elastomeric non-metallic die inserts eliminate tooling galling and pressure marks on titanium-plated and mirror surfaces.
Synchronized Sheet Followers: CNC-controlled heavy panel supports eliminate operator back-bend deformities on oversized 4-meter decorative cladding sheets.
Parametric Performance Across Dedicated Industrial Applications
Review comparative technical criteria, operational thresholds, and verified field performance data achieved by Haden customized machinery lines.
| Sector Application | Target Alloys | Key Technical Bottleneck | Haden Equipment Solution | Factory Yield Improvement |
|---|---|---|---|---|
| HVAC Ductwork | DX51D Galvanized (0.6–1.2 mm) | Zinc coating flaking & slow lock forming | Auto Duct Line V with Chrome Dies | +42% Line Output / 0% Rusting |
| Electrical Enclosures | SPCC, SECC, AL5052 (1.0–2.0 mm) | Multiple tool changes & surface scratching | Servo Flexible Panel Bender | -65% Cycle Time / Zero Rework |
| Automotive Structural | DP780, DP980, 6061-T6 (1.5–4.0 mm) | Extreme elastic springback variation | CNC Press Brake with Laser Angle Check | Angle Accuracy within ±0.2° |
| Architectural Metalwork | AISI 304/316 #8 Mirror (1.2–3.0 mm) | Die marking and radius deformation | CNC V-Groover & Polyurethane Tools | 100% Defect-Free Visual Finish |
Need to Evaluate a Material or Forming Application?
Share your part drawings, material specifications, thickness, tolerances, and production requirements. Haden engineers can evaluate the forming process, machine capacity, tooling requirements, and suitable equipment configuration for your application.
Quantifiable ROI & Production Performance Metrics
Engineered precision and integrated CNC automation deliver measurable operational gains. Review verified field data documenting sheet material yield increases, fabrication cycle time reductions, and accelerated capital payback timelines across global Haden installations utilizing industrial laser cutting machines.
Average sheet utilization increase achieved through dynamic multi-part geometric nesting algorithms.
Fabrication throughput acceleration powered by synchronized high-speed servo ram and backgauge systems.
First-pass defect rate maintained using closed-loop laser angle detection and dynamic springback compensation.
Average capital equipment amortization timeline driven by substantial labor and unit-cost savings.
Real-Time Manufacturing Telemetry
Haden CNC systems continuously stream operational telemetry, OEE benchmarks, and tooling wear analytics directly to plant MES environments to eliminate downtime and production bottlenecks.

Advanced Nesting Yield
Automated multi-part geometric nesting minimizes edge margins and maximizes raw stock efficiency across high-output sheet metal laser cutting machines.
Automated Servo Motion
Synchronized multi-axis direct-drive servo control accelerates ram positioning and backgauge indexing, drastically cutting non-productive stroke transit.
Dynamic Laser Angle Correction
Non-contact optical laser sensors evaluate material grain direction and thermal variance in real time, executing micro-adjustments during the bending stroke.
Cost-Per-Part Optimization
Automated material handling and rapid setup sequencing reduce dedicated operator labor requirements and electrical energy draw per finished component.
Production Audit: Conventional Equipment vs. Haden Automated Cell
Comparative performance audit based on an annual throughput of 100,000 structural components processed on versatile sheet and tube laser cutting machines.
| Operational Metric | Standard Equipment | Haden Automated System | Net Advantage |
|---|---|---|---|
| Material Sheet Yield | 74.5% Average Yield | 92.4% Optimized Yield | +17.9% Material Savings |
| Cycle Time per Part | 48.0 Seconds | 26.5 Seconds | 44.8% Faster Throughput |
| First-Pass Scrap Rate | 3.50% Run Average | 0.18% Laser Corrected | 94.8% Scrap Reduction |
| Direct Cost Per Part | $4.65 / Component | 2.58 / Component | $2.07 Savings / Part |
| Capital Amortization Period | 28 - 36 Months | 9.4 Months Mean | 68% Faster Payback |
Evaluate the Right Production Line for Your Capacity Goals
Share your part drawings, material and thickness ranges, target output, and current production process. Haden engineers can evaluate equipment configuration, automation requirements, production capacity, and key investment considerations for your project.
From Blueprint to Serial Production: End-to-End Machinery Implementation Workflow
Deploying high-performance sheet metal machinery requires structured engineering governance at every milestone. Haden executes a proven five-phase implementation framework designed to eliminate commissioning risks, verify microscopic geometric tolerances, and ensure turnkey automation integration for manufacturing plants worldwide.
Blueprint Feasibility & Prototype Sampling
Rigorous 3D CAD/CAM review, finite element analysis, and physical test processing on high-precision laser cutting machines to evaluate springback, thermal impact, and cycle times.
Custom Assembly & Robotic Automation
Stress-relieved frame machining, electro-hydraulic servo synchronization, custom tooling packages, and communication interface setup for tube laser cutting machines and robotic load/unload cells.
Factory Acceptance Testing (FAT)
Continuous 100-workpiece pilot production run under full load. Verification of laser angle measurement, dynamic deflection compensation, and thermal stability.
Global Rigging & On-Site Calibration
Vapor-barrier export crating, international logistics management, professional plant positioning, dual-axis optical leveling, and electrical/pneumatic integration.
Certified Operator Training & Support
Hands-on CNC programming instruction, safety protocol onboarding, preventative maintenance schedules, encrypted IoT diagnostics, and regional spare parts coverage.

De-Risking Capital Machinery Deployments Through Controlled Quality Gates
Industrial metal fabrication equipment represents a high-stakes capital commitment where unaddressed calibration errors, material springback discrepancies, or communication bottlenecks directly cause production downtime. Haden engineers eliminate deployment uncertainty by establishing empirical baseline benchmarks before a machine ever leaves our production floor.
From extended throat depths and customized daylight openings to turnkey integration with advanced sheet metal laser cutting machines, enterprise MES systems, and multi-axis loading robots, each machine configuration undergoes finite element stress analysis. Every electrical enclosure, hydraulic manifold, and optical safety interlock strictly adheres to global CE, UL, and ISO 12100 machinery safety directives.
Pre-Delivery Quality Verification Gate
Full-speed kinematic cycling with synchronized multi-axis servo validation, logging angular repeatability and dynamic crowning compensation across real workpieces.
Post-Commissioning Operational Continuity
Factory-integrated IoT edge gateways monitor proportional valve response curves, oil degradation, and backgauge alignment to automate preventative service triggers.
Turnkey Implementation and Milestone Verification Matrix
The following standard quality gates define accountability, compliance criteria, and formal engineering documentation delivered to client teams at every deployment milestone.
| Milestone Phase | Engineering Activities | Technical Validation Standard | Customer Deliverables |
|---|---|---|---|
| Phase 1: Feasibility | 3D CAD analysis, dynamic stress modeling, blank nesting, sample cutting on high-tensile alloys. | ISO 2768-m geometric tolerance and surface roughness Ra ≤ 1.6 μm. | Feasibility audit report, cycle time calculations, verified physical prototype specimens. |
| Phase 2: Customization | Custom bed machining, tooling geometry matching, safety light curtain integration, PLC coding. | EN 60204-1 electrical safety compliance & ISO 13849 PL-e safety architecture. | Custom electrical schematics, foundation drawings, and automation I/O map. |
| Phase 3: Factory Acceptance | 100-part continuous production cycle, thermal stability logging, full load dynamic bending. | Statistical process capability Cpk ≥ 1.33 across all critical dimensional axes. | FAT certificate, video validation record, calibration report, release for shipping. |
| Phase 4: Site Commissioning | Rigging, dual-axis electronic leveling, fluid charging, multi-axis zero calibration, utility hookup. | Optical bed parallelism ≤ 0.02 mm/m, ram positioning repeatability ±0.005 mm. | On-site acceptance protocol (SAT), installation inspection report, sign-off log. |
| Phase 5: Production Handover | Classroom and hands-on CNC training, routine maintenance guidance, cloud telemetry integration. | Operator qualification exam, ISO 9001 preventative maintenance audit check. | Certified operator diplomas, multi-language maintenance manuals, spare parts catalog. |
CNC Programming & Operational Certification
Structured modular training covering offline CAD/CAM nesting, dynamic bend sequencing, crash avoidance parameters, and real-time adaptive angle compensation.
- Multi-Language Operational Documentation
- Hands-on Tooling Setup & Calibration Drills
Predictive Telemetry & Remote Diagnostics
Edge-connected IoT telemetry continuously tracks proportional servo response, hydraulic temperature profiles, and optical encoder drift to prevent unplanned downtime.
- 24/7 Secure Encrypted Remote Diagnostics
- Condition-Based Maintenance Alerts
Strategic Spare Parts Hubs & Rapid Dispatch
Original replacement parts including high-precision linear encoders, CNC controllers, servo drives, and hydraulic seals are maintained in regional hubs for rapid delivery.
- Guaranteed 48-Hour Core Spares Dispatch
- Certified Field Service Engineering Support
Global Factory Customer Testimonials & Field Proof
Explore verified shop-floor performance data, equipment evaluations, and production audits from Haden engineering partners across Europe, Asia, and the Americas.
Tier 1 Enclosure Fabrication Plant
Production Review: CNC Electro-Hydraulic Press Brakes
"Switching to Haden electro-hydraulic press brakes reduced tooling setup downtime by 42%. The dynamic CNC crowning and real-time laser angle tracking maintain tight ±0.3° angular consistency across high-volume stainless electrical enclosures runs."
Electrical Switchgear Manufacturing
Automated Flexible Panel Bending Center
"Operating in continuous tropical shifts, our Haden flexible panel bending cell eliminated manual operator re-fixturing. We produce complex modular control cabinets with zero surface scratching on pre-coated galvanized sheet."
Heavy Agricultural Machinery
Heavy 4-Roll Plate Bending & Rolling System
"Over 4,500 annual running hours rolling 50mm high-yield structural plate, Haden heavy-duty plate rolling machines demonstrated zero cylinder deflection. Commissioning support and remote diagnostics were outstanding."
Rigorous Factory Acceptance Testing for Mission-Critical Machinery
Every Haden cutting, bending, grooving, and rolling system—including turnkey automated sheet metal production lines—undergoes multi-axis laser interferometry calibration, continuous 100-workpiece test runs, and optical cut-edge audits prior to worldwide dispatch.
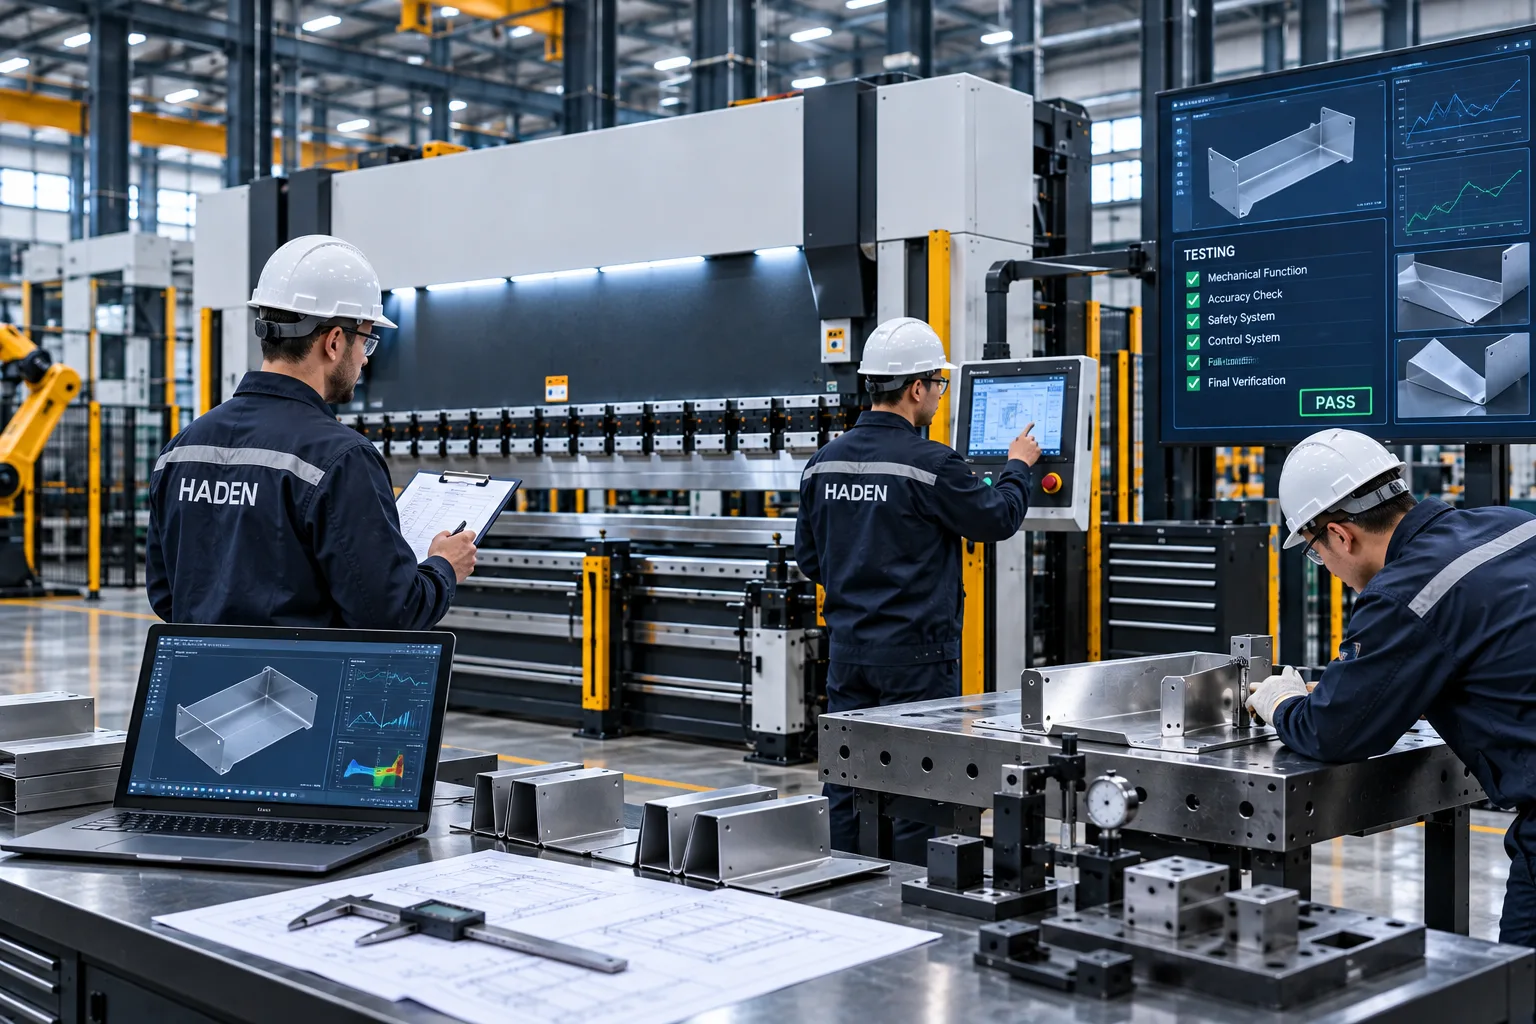
International Safety Certifications & Regulatory Compliance
Engineered and independently certified to meet the world's most demanding industrial fabrication directives.
ISO 9001:2015
Quality Management
CE Machinery
2006/42/EC Safety
UL & CSA
Electrical Systems
TÜV Rheinland
Functional Safety
IEC 60204-1
Industrial Controls
NEMA & IP54
Cabinet Ingress Rated
Sheet Metal Machinery Deployment & Commissioning FAQ
Transitioning from initial engineering drawings to reliable factory-floor production demands meticulous machine planning, strict tolerance verification, and dependable delivery milestones. Here, Haden application engineers address crucial questions regarding material feasibility testing, international commissioning timelines, custom footprint integration, and lifecycle maintenance support.
Project Timelines & Commissioning Deliverables
Standard execution benchmarks comparing standalone CNC machinery with fully automated turnkey metalworking cells.
| Implementation Milestone | Standard CNC Machinery | Custom Turnkey Production Lines | Core Engineering Deliverable |
|---|---|---|---|
| Pre-Engineering Feasibility & Prototyping | 24–48 Hours (CAD/CAM Analysis) | 3–5 Business Days (Physical Sample Runs) | Detailed Tolerance & Takt-Time Feasibility Report |
| Machine Assembly & FAT Validation | 4–6 Weeks (Modular Stock: 10–15 Days) | 10–14 Weeks (Tailored Tooling & Robotics) | 100-Part Continuous Run Pre-Acceptance Protocol |
| On-Site Rigging, Alignment & Setup | 2–3 Days per Unit | 7–12 Days (Full Line Handshake & Commissioning) | Laser Interferometer Geometric Calibration Certificate |
| Operator & Maintenance Certification | 2 Days Classroom & Hands-On Training | 5 Days Comprehensive Multi-Tier Training | Certified Machine Operator & Safety Competency Signoff |
01
How does Haden validate pre-sales feasibility for specialty alloys, high-tensile sheet, and non-standard geometries?
How does Haden validate pre-sales feasibility for specialty alloys, high-tensile sheet, and non-standard geometries?
Before finalizing any equipment proposal, the Haden Application Engineering Team executes rigorous physical trial cut, notch, and bend sequences using your specific material lots. When fabricating challenging grades like Hardox 450/500, high-yield structural plate (Strenx 700), or mirror-polished stainless steel, nominal formulas rarely reflect true material springback, grain direction variability, or coating sensitivities.
Active Springback Compensation Analysis
We measure accurate neutral axis shift factors (κ-factor) and configure real-time dynamic laser angle correction curves for CNC press brakes and automated panel benders.
Cut-Edge Heat-Affected Zone Profiling
Fiber laser cutting trials evaluate micro-burr formation, dross adhesion, and assist gas optimization (N₂/O₂/Air) to guarantee taper-free vertical edges within ±0.05 mm.
Each pre-sales validation package includes optical cross-section micrographs, required tonnage graphs, optimal tooling geometry blueprints, and certified cycle-time benchmarks.
02
What are standard machinery manufacturing lead times and Factory Acceptance Testing (FAT) protocols?
What are standard machinery manufacturing lead times and Factory Acceptance Testing (FAT) protocols?
Haden operates structured production workflows backed by strict quality gate checkpoints. Build schedules depend on machine class and custom automation requirements:
- •Standard CNC Press Brakes & Fiber Laser Cutters: 30 to 45 business days. Quick-ship modular stock units and dual-purpose sheet and tube laser cutting machines can be prepared and dispatched in 10 to 15 business days.
- •Flexible Panel Benders & Plate Rolling Systems: 60 to 75 business days, utilizing engineered plate rolling and forming solutions , custom universal bending blade manufacturing, and material manipulation units.
- •Turnkey Coil-Fed Lines & Robotic Automation Cells: 90 to 120 business days covering total hardware integration, automated robotic panel bending cells , and multi-station synchronization.
Before crating, every machine undergoes a strict 48-hour continuous Factory Acceptance Test (FAT). Clients may inspect runs on-site at our manufacturing plant or witness live high-definition multi-angle streams complete with real-time CMM dimensional validation.
03
How does Haden support on-site international installation, machine calibration, and operator training?
How does Haden support on-site international installation, machine calibration, and operator training?
Haden deploys certified field service engineers directly to your plant globally. Our standardized commissioning workflow ensures rapid, error-free integration:
Rigging & Foundations
Foundation leveling validation, vibration-damped anchoring, and integration with plant pneumatic, hydraulic, and electrical grids.
Optical Alignment
Renishaw laser interferometer calibration verifying linear positioning and backgauge repeatability within ±0.01 mm.
Operational Handoff
Structured training covering CNC programming, 3D CAD/CAM nesting software, safety interlocking, and daily inspection protocols.
All documentation is provided in English, Spanish, German, French, or Arabic, complete with electrical schematics, hydraulic routing charts, and 3D exploded spare parts catalogs.
04
Can Haden equipment adapt to limited shop floor layouts and interface with existing robotic automation cells?
Can Haden equipment adapt to limited shop floor layouts and interface with existing robotic automation cells?
Yes. Over 60% of Haden automated turnkey installations involve non-standard layout footprints, crane interference constraints, or integration with existing upstream/downstream automation. Our custom engineering capabilities include:
- •Frame & Enclosure Customization: Extended throat depths, increased open daylight heights, and low-profile backgauge enclosures tailored for tight factory corridors.
- •Open Industrial Protocols: Native support for OPC UA, Profinet, EtherCAT, and Modbus TCP for seamless bi-directional ERP/MES production tracking and remote telemetry.
- •Robotic Handshake Architecture: Standardized software and hardware interfaces for 6-axis articulated robots (Fanuc, KUKA, Yaskawa, ABB), facilitating automated sheet feeding, re-gripping, and part sorting.
05
What wear parts supply guarantees, preventive maintenance programs, and remote IoT diagnostics does Haden provide?
What wear parts supply guarantees, preventive maintenance programs, and remote IoT diagnostics does Haden provide?
To ensure maximum operational uptime, Haden backs every installation with comprehensive lifecycle service protocols and dependable global spare parts inventory:
Direct Wear Parts Distribution
Critical consumables—including fiber laser optical lenses, cutting nozzles, ceramic rings, hydraulic seals, proportional valves, and hardened 42CrMo bending tooling—are stocked in regional hubs for 24-to-48-hour emergency dispatch.
Haden Edge IoT Diagnostics
Encrypted telemetry monitors servo thermals, proportional valve response speeds, and vibration frequencies. Our engineering center identifies component wear patterns to resolve anomalies before unexpected downtime occurs.
We provide lifetime remote software and firmware updates, cloud configuration backups, and a guaranteed minimum 15-year parts availability commitment from the date of commissioning.
Facing a specific metal forming or precision cutting challenge?
Submit your component CAD files (.DXF, .DWG, or .STEP) directly to our senior application team. We will provide a thorough manufacturing feasibility analysis, machine configuration recommendations, and production cycle-time estimates within 24 hours.
Feasibility Analysis Turnaround
< 24 Hours
Global Installation Footprint
50+ Countries
Discuss Your Sheet Metal Machinery Project with Haden Engineering
Share your part drawings, materials, thickness ranges, production targets, and process requirements. Haden engineers can evaluate the application and recommend a suitable machine configuration, tooling approach, automation level, and production solution.
Review Your Parts & Production Requirements
We review your drawings, materials, thickness ranges, part dimensions, tolerances, production volumes, and current manufacturing process to understand the application.
Evaluate Machine, Tooling & Automation
Based on your process requirements, our team evaluates machine capacity, tooling requirements, material handling, automation, and production-line configuration.
Develop a Project-Specific Equipment Proposal
We can prepare a recommended equipment configuration and discuss technical specifications, optional automation, project scope, and commercial requirements with your team.
What You Can Send Us
Project Confidentiality
Technical drawings and project information are handled as confidential business information. NDA arrangements can be discussed when required for your project.
Request a Technical Proposal
Tell us about your parts, materials, production requirements, and target equipment. Upload drawings or CAD files if available to help our engineers evaluate the right machinery configuration for your project.
Application Review
Machine selection based on your material, parts, and process.
Confidential Project Handling
NDA arrangements can be discussed for sensitive project information.
Custom Configuration
Evaluate machine capacity, tooling, automation, and line integration.
Production-Line Planning
Support for standalone machines and integrated automated solutions.