
Industrial Coil Processing Solutions & Automated Blanking Lines
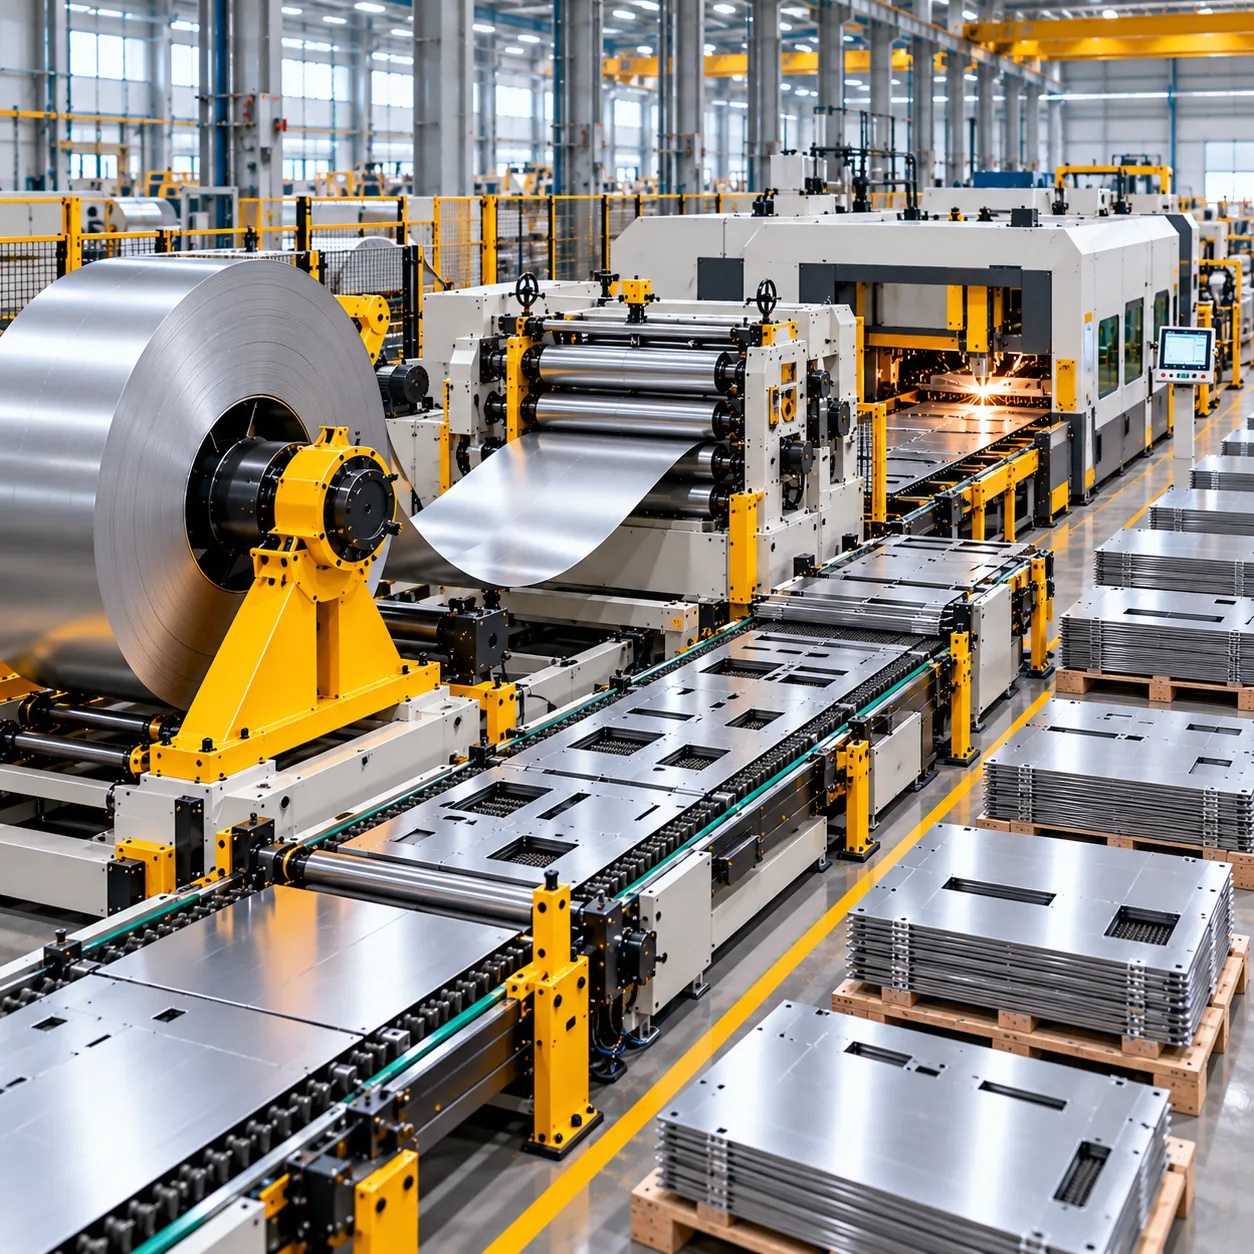
Seamlessly integrate heavy-duty uncoiling, multi-roller precision leveling, continuous servo loop feeding, and synchronized coil-fed laser cutting machines or shearing systems to maximize material utilization and eliminate secondary operations.
Continuous nesting eliminates standard sheet end-trim scrap.
Multi-roller leveling completely relieves coil memory and internal stress.
Direct-from-coil feed removes repetitive manual sheet loading delays.
Custom configurations for laser blanking, cut-to-length, and stamping feeds.
Quantifiable Efficiency & Material Savings Metrics
Haden automated coil-fed laser cutting machines and coil processing lines unify decoiling, precision leveling, and continuous on-the-fly blanking to eliminate material waste, accelerate part throughput, and reduce per-part fabrication costs.
Continuous nesting across virtual sheet lengths eliminates standard pre-cut sheet end-drops and off-cut waste.
Precision multi-roller leveling neutralizes coil set, crossbow, and internal residual stresses across the entire web.
Direct coil blanking eliminates standalone sheet shearing, manual pallet handling, and intermediate blank staging.
Engineered for cold-rolled carbon steel, high-tensile alloys, stainless steel, galvanized sheet, and aluminum coils.
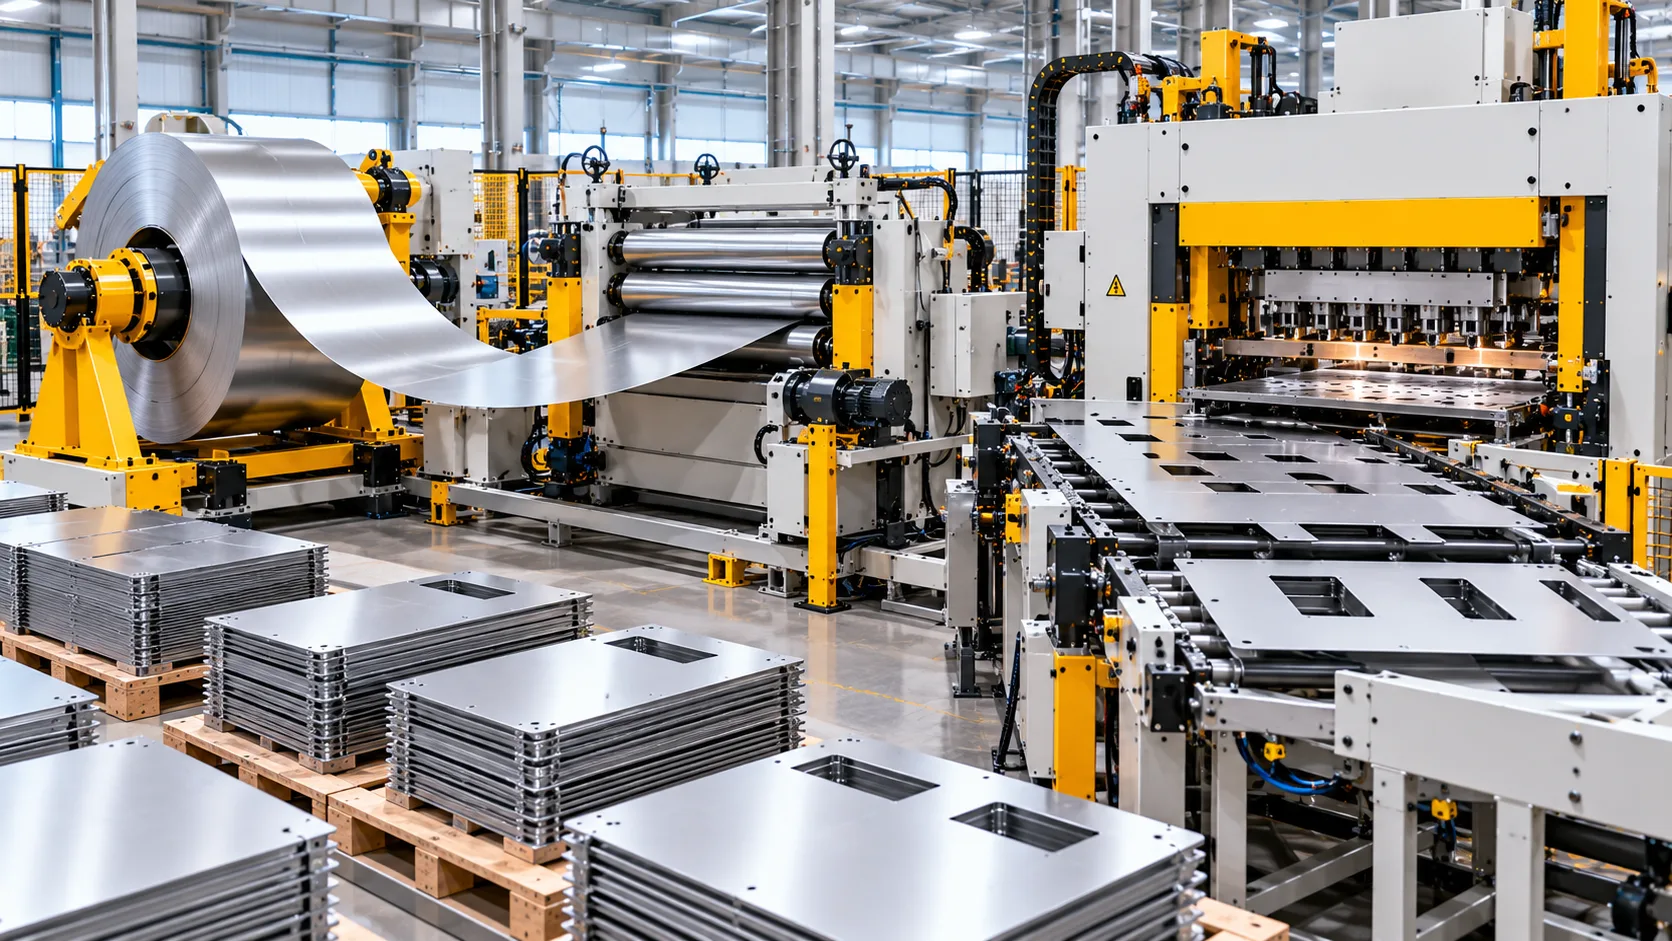
Engineered to Solve Core Sheet Fabrication Bottlenecks
Haden coil processing systems replace fragmented shearing, handling, and single-sheet laser cutting with an integrated continuous line. By synchronizing heavy-duty decoiling, high-precision leveling, and automated cutting, your facility achieves peak output with minimal scrap.
Continuous Common-Line Dynamic Nesting
Removes length constraints and sheet edge margins, allowing extra-long components and mixed-part nests across an unbroken strip.
Residual Stress Relief & Extreme Flatness
Multi-roller alternating bending eliminates inner material stresses, preventing thermal distortion during high-speed cutting and forming.
Lean Floor Logistics & Labor Elimination
Replaces bulky sheet inventory staging with compact master coil storage, transitioning directly from coil to sorted finished blanks.
End-to-End Coil Processing Solutions and Integrated Line Architectures
Modern metal fabrication demands continuous automated throughput, superior blank flatness, and agile production flexibility. Haden engineers heavy-duty coil processing solutions that convert raw metal coils into high-precision, stress-free blanks in a single integrated workflow. By synchronizing automated uncoiling, multi-roller precision leveling, closed-loop servo feeding, and continuous fiber laser or mechanical blanking, our automated coil processing line configurations eliminate manual sheet handling, dramatically reduce edge scrap, and deliver measurable operating cost advantages.
Continuous Coil-Fed Fiber Laser Cutting Lines
The continuous coil-fed laser cutting machines combine the material cost advantages of raw coil stock with the extreme flexibility of advanced laser cutting machines . Strip feeds continuously from the decoiler through an advanced multi-roller precision leveler directly into an enclosed dynamic cutting zone. By utilizing advanced continuous nesting software across infinite strip lengths, manufacturers produce complex geometric blanks and variable part families without dedicated stamping dies or standard sheet length restrictions.
Maximized Material Yield
Continuous strip nesting removes fixed sheet border margins, boosting raw material utilization up to 92%+ and drastically minimizing skeleton scrap.
Zero Hard Tooling Costs
Direct digital CAD/CAM processing eliminates custom blanking die fabrication, multi-week tooling lead times, and costly die warehouse storage.
Synchronized Flying Blanking
Dynamic dual-cutting bridge architecture enables high-speed profiling while the material advances smoothly without surface scratch marks.
Automated Part Sorting
Integrated overhead Cartesian or robotic sorting gantries pick finished components on the fly, stacking them neatly by recipe onto designated pallets.
Core Line Modules
- Decoiler System: Hydraulic expansion mandrel (5 to 25 Ton payload)
- Precision Leveling: 19-roller micro-gap leveling cassette with anti-camber control
- Laser Power: 3 kW to 20 kW high-brightness industrial fiber sources
- Thickness Capacity: 0.5 mm – 6.0 mm (Carbon steel, stainless steel, aluminum)
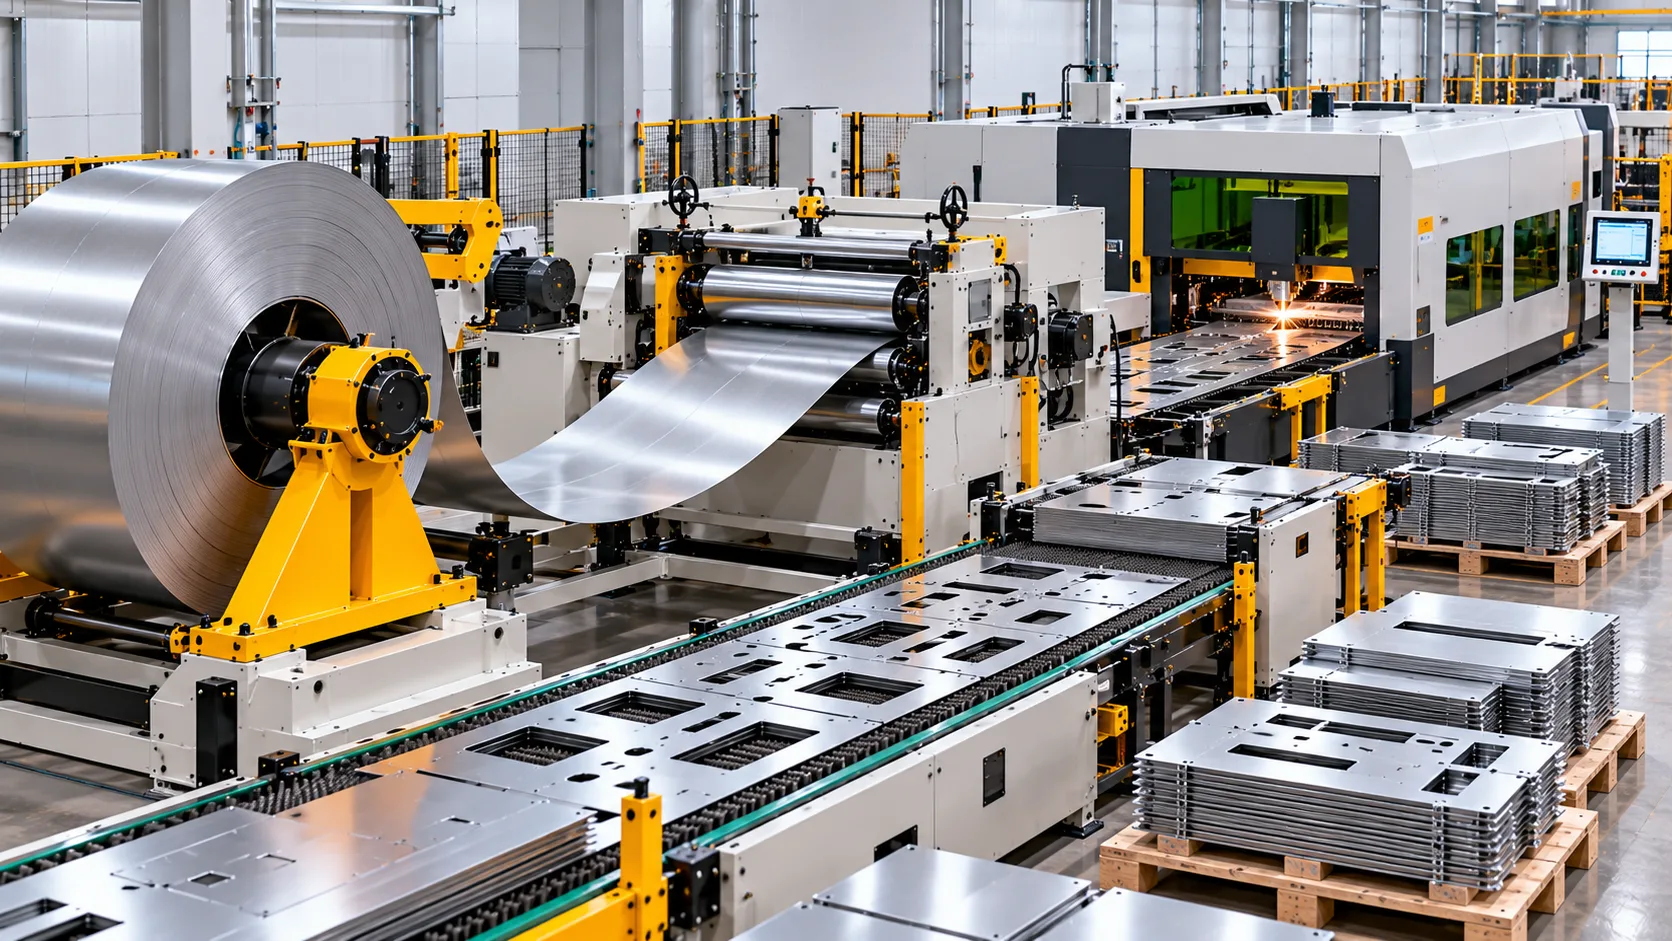
Ideal for tier suppliers and fabricators managing diverse component variants, rapid engineering change orders, and extra-long structural sheet blanks exceeding the bed dimensions of traditional sheet metal laser cutting machines .
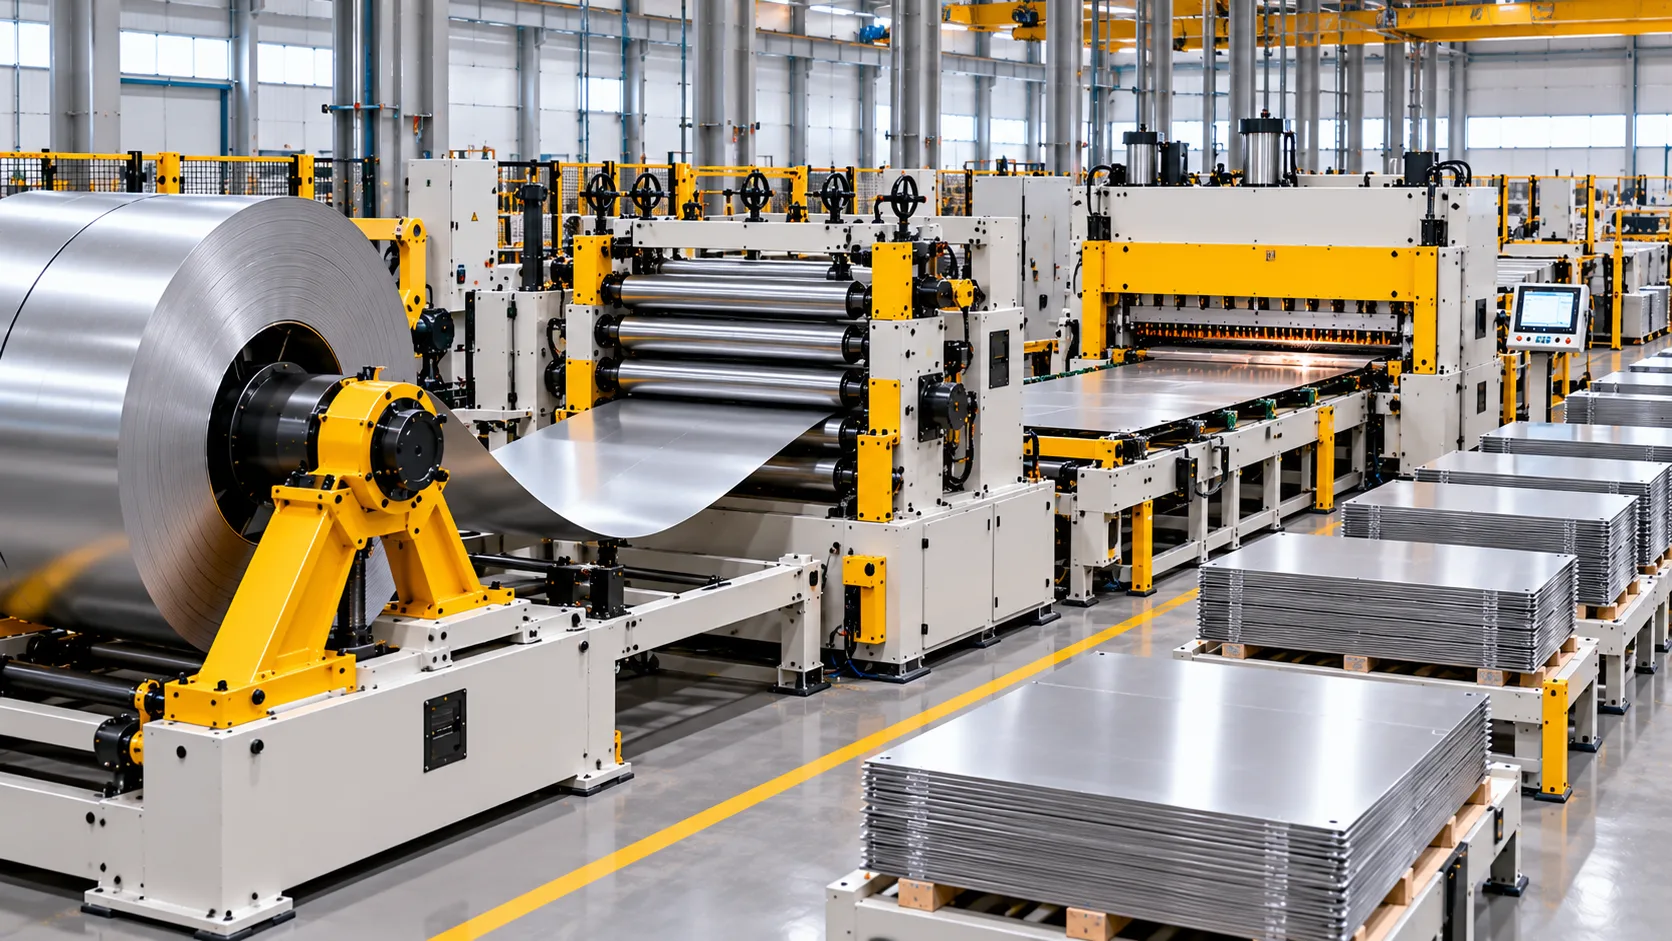

Engineering Architecture & System Selection Matrix
Compare key operational criteria across our primary coil processing system architectures to identify the optimum balance of part geometry flexibility, tooling investment, and line throughput.
| System Architecture | Blank Geometry Flexibility | Tooling & Die Costs | Thickness Range | Production Throughput | Primary Industrial Use |
|---|---|---|---|---|---|
| Coil-Fed Laser Cutting Line | Maximum (Infinite contour profiles & nested parts) | Zero Die Investment (CAD/CAM Driven) | 0.5 mm – 6.0 mm | Moderate to High (Continuous dynamic cutting) | High-mix parts, prototypes, custom enclosures, EV components |
| Cut-to-Length (CTL) Line | Standard Rectangles & Trapezoids | Low (Standard shear blades) | 0.5 mm – 16.0 mm | Ultra-High (Up to 60 m/min continuous) | Steel service centers, HVAC ductwork, commercial refrigeration |
| Automated Press Feed Line | Dedicated Die Profile (High Repetition) | High (Hard stamping & progressive dies) | 0.8 mm – 12.0 mm | Mass Production (Up to 120 SPM) | Automotive OEM stamping, chassis brackets, motor stampings |
Configure a Custom Coil Processing Line for Your Facility
Every manufacturing facility operates under unique material constraints, floor space boundaries, and production quotas. Haden provides complete engineering support, including 3D plant layout simulation, material flow analysis, and tailored equipment integration to ensure maximum output and fast capital payback.
Core Engineering Mechanics and Precision Leveling Process
Eliminating severe residual stress, coil memory, crossbow, and edge wave defects requires an advanced, multi-stage mechanical transformation. Haden coil processing solutions integrate a four-stage strip stabilization workflow to transform raw master coils into mirror-flat, stress-relieved strip substrates engineered for high-speed coil-fed laser cutting machines and heavy-duty progressive die stamping.
Elastoplastic Reverse Bending: The Science of Residual Stress Relief
Master coils produced at steel rolling mills carry steep internal stress gradients generated by uneven thermal cooling, winding tension profiles, and cold-reduction forces. When processed without multi-roller corrective leveling, these locked-in stresses release unpredictably during downstream shearing, punching, or fiber laser blanking, causing instant sheet warping, springback distortion, and automated production stoppages.
The Haden precision leveling system subjects the strip to a continuous series of alternating plastic-elastic reverse bends. By driving outer strip fibers past their yield threshold by 70% to 85% with decreasing deflection amplitudes toward the exit, our levelers equalize internal fiber lengths, reset crystalline structural memory, and deliver permanent flatness across the entire strip width.
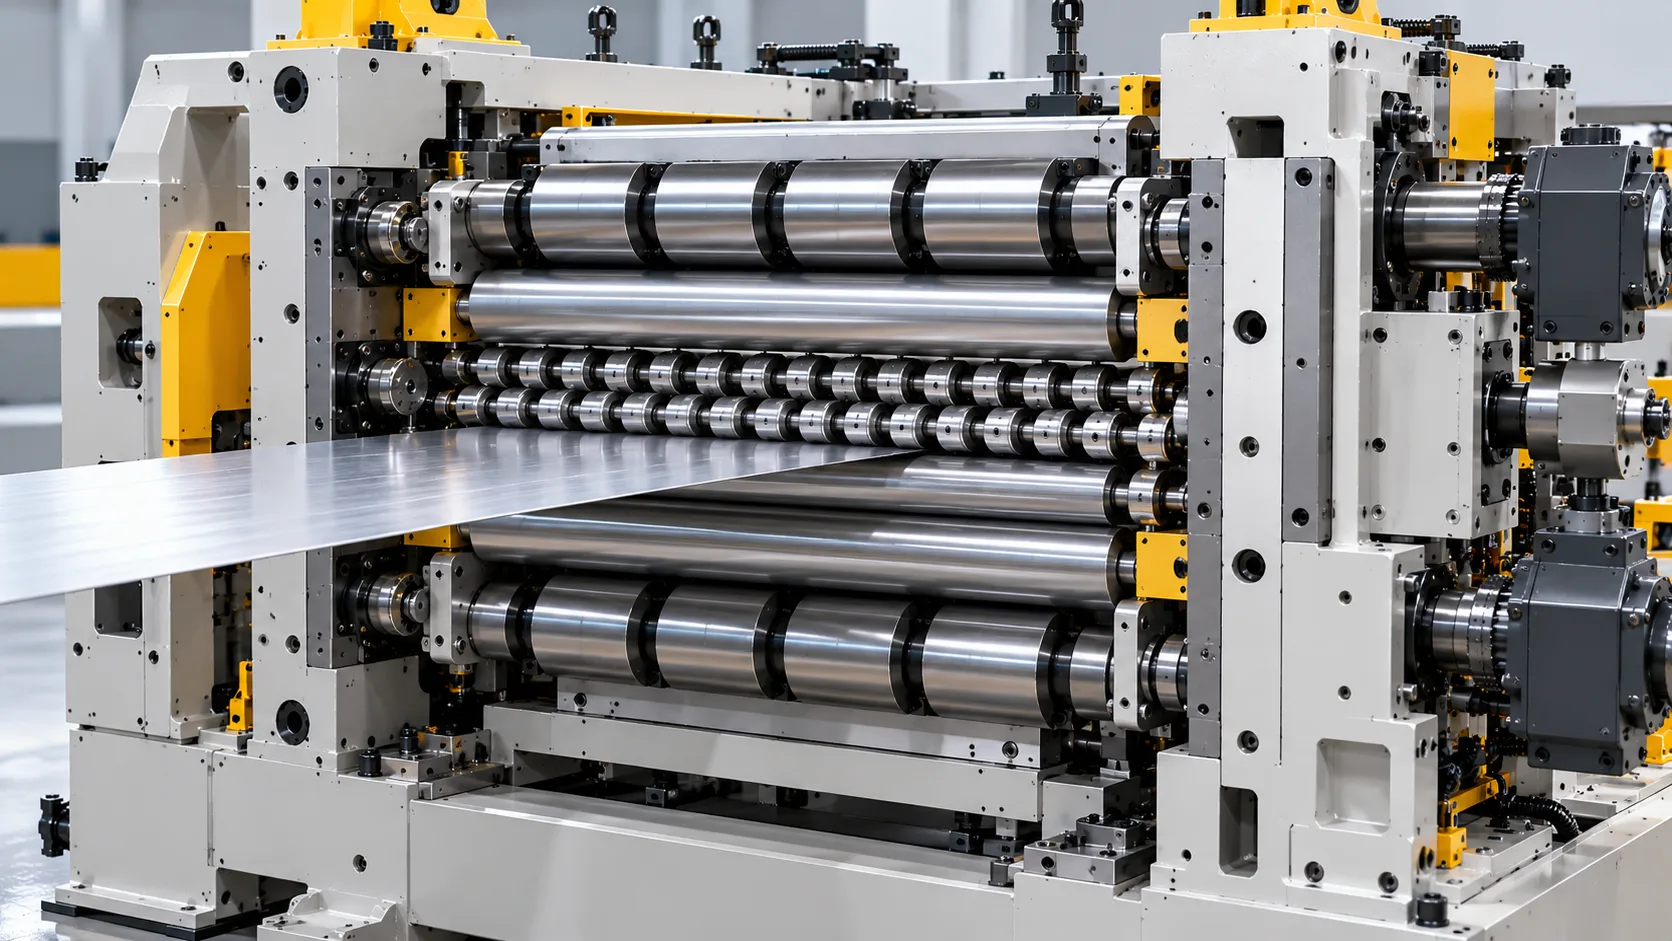
Four-Stage Precision Strip Stabilization Process
A synchronized, fully automated material path engineered to transition raw coil stock into perfectly indexed, dimensionally stable, burr-free blanks.
Intelligent Decoiling & Constant Back-Tension
Heavy-duty hydraulic expansion mandrels securely grip coil internal diameters up to 30 metric tons. Proportional disc braking units and closed-loop load cells maintain steady web back-tension, eliminating strip sagging, uncoiler slippage, and surface scratching during rapid acceleration cycles.
- Hydraulic peeler table & motorized snubber roll
- Automatic strip centering with optical edge sensors
Multi-Roller Reverse Bending Leveling
Coil material passes through 19 to 23 micro-adjustable alloy steel work rolls supported by dense multi-tier backup bearings. Independent servo-driven wedge adjustment applies precise roll plunge profiles to eliminate coil set, crossbow, center buckles, and edge waves.
- Four-high and six-high leveler cassette configurations
- Independently motorized backup roller bank control
Optical Loop Buffering & Tension Isolation
A deep storage loop pit or horizontal overhead loop bridge cleanly decouples upstream continuous uncoiling from downstream high-speed pulsed indexing. Non-contact ultrasonic arrays continuously monitor loop geometry to ensure shock-free speed synchronization.
- Zero tensile drag during servo blanking acceleration
- Scratch-free pneumatic support cascade rollers
Synchronized Dynamic Servo Blanking
High-torque AC servo direct-drive feeder rolls with hard-chrome anti-slip surfaces feed leveled material directly into continuous fiber laser cutting chambers or hydraulic shears, maintaining positioning repeatability within ±0.05 mm at continuous line speeds.
- Feed length positioning accuracy within ±0.05 mm
- Burr-free synchronized shearing and automated stacking
Comparative Engineering Analysis: Standard Straighteners vs. Haden Precision Levelers
Technical distinctions between basic uncoiler straighteners and advanced multi-roller elastoplastic leveling systems.
| Process Parameter | Conventional 7-Roll Straightener | Haden 19–23 Roll Precision Leveler | Operational Impact |
|---|---|---|---|
| Roll Topology & Quantity | 5 to 7 large-diameter unsupported rolls | 19 to 23 micro-diameter backed-up rolls | Higher roll density generates tight alternating reverse bends required for core yield penetration. |
| Residual Stress Removal | Partial (removes only gross coil curvature) | Complete (eliminates internal tension gradients) | Prevents post-cut thermal distortion, sheet warping, and weld seam misalignment. |
| Crown & Edge Wave Correction | Not possible (rigid single-piece roll shafts) | Individual motorized backup roller adjustment | Allows targeted zone stretching to flatten tight strip centers or wavy coil edges. |
| Surface Protection Grade | Standard ground steel (prone to roll markings) | Hard-chrome plated / mirror-finish (Ra ≤ 0.2 μm) | Completely safe for bright-annealed stainless, pre-painted sheet, and architectural aluminum. |
| Feed Positioning Repeatability | ±0.30 mm to ±0.50 mm | ±0.05 mm via closed-loop encoder feedback | Guarantees tight blank squareness, precise sheet indexing, and reliable die operation. |
Precision Leveling Engineering Specifications
Explore the core mechanical assemblies driving Haden continuous coil processing systems.
Work Roll Construction
Machined from premium vacuum-degassed 100Cr6 forged alloy tool steel, induction hardened to 60–62 HRC, cryogenically stabilized, and micro-ground to sub-micron concentricity tolerances.
6-High Configuration
Intermediate roller cassettes eliminate contact shadowing and cross-hatch marks on sensitive automotive Class-A panels, polished stainless steel, and anodized aluminum coils.
Rapid Cassette Exchange
An automated hydraulic quick-change rail carriage enables full cassette swap-outs within 8 to 12 minutes for rapid alloy changeovers and offline maintenance routines.
Engineered for Heavy-Duty Industrial Coil Processing Applications
From 0.5 mm light-gauge appliance alloys to 25.0 mm heavy-plate structural steel, Haden precision leveling mechanics ensure dependable strip stability, zero springback, and maximum raw material utilization for global manufacturing lines.
In-House Coil Processing vs. Conventional Flat Sheet Blanking
High-volume metal fabricators face relentless margin pressure from raw material markups, scrap loss, and manual staging bottlenecks. Transitioning from pre-cut sheet bundles to an integrated Haden in-house coil processing line fundamentally reshapes production economics. By purchasing master coils directly from primary mills, nesting parts without fixed sheet length boundaries, and running continuous uncoiling lines, industrial manufacturers achieve verifiable cost reductions on every metric ton processed.
Bypass steel service center processing premiums and protective pallet surcharges by procuring raw master coils directly from mills and tier-one distributors.
Continuous nesting across virtually infinite strip lengths removes leading and trailing remnant scrap inherent to fixed standard sheet blanks.
A single continuous coil staging sequence replaces repetitive sheet de-stacking, crane transfers, shuttle table cycles, and manual skeleton clear-outs.
High-throughput stamping, automotive stamping, and HVAC fabrication operations typically recover total line investment within the first year of operation.
Comprehensive Manufacturing Comparison Matrix
Side-by-side technical and economic evaluation: traditional standalone flatbed cutting vs. automated continuous coil processing.
| Operational Dimension | Conventional Flat Sheet Blanking | Haden In-House Coil Processing | Economic Impact |
|---|---|---|---|
| Raw Material Procurement | Purchasing pre-cut flat sheets carries middleman toll slitting, custom packaging, and freight handling markups ($40–$120/ton extra). | Direct purchasing of master coils from steel mills at baseline commercial commodity and contract price brackets. | 5% to 15% lower cost/ton |
| Nesting & Scrap Yield | Constrained by fixed sheet dimensions (e.g., 5×10 ft or 6×12 ft). Boundary clamps and remnant drops limit net yield to 75%–82%. | Borderless continuous nesting with dynamic servo feeding. Common-line cutting across virtual infinite strips yields 88%–95%. | +10% to +18% scrap reclamation |
| Handling & Labor Cycles | Frequent crane rigging, vacuum pallet de-stacking, shuttle table staging, and continuous manual skeleton scrap sorting. | Single coil loading (up to 35 tons) provides hours of fully autonomous, unattended continuous uncoiling and blanking. | -40% direct operator hours |
| Part Flatness & Internal Stress | Residual stresses stored in commercial sheets release during thermal laser cutting, causing edge curl and laser nozzle collisions. | Integrated 19-to-23-roller precision levelers eliminate coil memory, center buckle, and edge wave under hydraulic back-up control. | Zero secondary flattening needed |
| Floor Space & Warehousing | Dozens of sheet pallet variations and lengths occupy hundreds of square meters of floor space and heavy cantilever racking. | High-density vertical or saddle coil storage. Produce any custom blank geometry on demand from standard master coil widths. | -60% storage footprint |
| Production Lead Time | Dependent on outside service center fulfillment times for custom-cut sheet sizes, risking project downtime and expediting fees. | Instant order execution. High-speed NC servo feeders and continuous blanking units process new production jobs on demand. | Immediate production turnaround |
Master Coil Procurement & Margin Reclamation
Purchasing pre-cut flat sheet inventory transfers essential operating margin to intermediary metal processors. Steel service centers add surcharges for decoiling, rough slitting, protective banding, custom pallets, and multi-leg trucking. Over an annual operating cycle, these compounding markups add $60,000 to over $300,000 in unrecoverable overhead for every 1,500 metric tons of processed carbon steel, stainless steel, or aluminum.
- ✓ Direct Primary Mill Purchasing: Secure raw structural steel, galvanized coil, and aluminum at primary tier-one volume pricing tiers.
- ✓ Price Volatility Protection: Buffer raw master coils in-house, shielding plant operations from short-term sheet distribution spot price spikes.
- ✓ Packaging Cost Elimination: Eliminate thousands of single-use wooden skids, steel straps, plastic stretch wrapping, and waste disposal fees.
Continuous Dynamic Nesting & Scrap Elimination
Standard flatbed CNC cutting systems force nested CAD geometry into fixed rectangular boundaries, creating unusable offcut skeletons. In contrast, Haden coil-fed laser cutting machines establish a continuous, virtually endless sheet format. By interleaving parts across the uncoiling axis with common-line cutting strategies, production engineers eliminate clamp scrap, end-of-sheet drops, and leading margins.
- ✓ Zero End-of-Sheet Skeleton Waste: Feed continuous strip stock seamlessly without losing 150–300 mm offcut tails on every cycle.
- ✓ Extra-Long Seamless Components: Blank components exceeding 4,000 mm in a single uninterrupted pass, eliminating secondary welding.
- ✓ High-Density Interlocking Layouts: Nest complex, asymmetrical automotive brackets, enclosure panels, and duct components with near-zero gap.
Continuous Autonomous Workflow & Labor Savings
Sheet-fed laser cutting systems and mechanical punch presses require constant labor intervention: pallet staging, suction de-stacker cycles, micro-joint tab break-out, and scrap disposal. A fully automated Haden decoiling, leveling, and blanking line shifts sheet metal production toward uninterrupted lights-out manufacturing with minimal operator intervention.
- ✓ Long-Run Unattended Operation: A single 20-to-30-ton coil delivers 6 to 10 hours of continuous automated blanking and sorting.
- ✓ Streamlined Internal Logistics: Consolidate up to 40 daily forklift pallet transport runs into just 1 or 2 high-capacity coil transfers.
- ✓ Enhanced Operator Ergonomics: Automated hydraulic coil loading cars and motorized threading tables minimize manual handling risks.
Stress-Free Leveling & Quality Consistency
Internal mechanical stresses trapped inside standard commercially leveled sheets release during thermal laser cutting or heavy stamping, resulting in heat warping, springback variance, and cutting head collisions. Haden integrates multi-roller precision leveling cassettes that subject the material to calculated alternating reverse bending, neutralizing residual stress before cutting.
- ✓ Micron Flatness Tolerances: Consistently achieve precision flatness within ±0.1 mm per linear meter across high-tensile steels.
- ✓ Zero Laser Head Collisions: Stress-relieved material stays completely flat under thermal cut paths, protecting high-value optical cutting heads.
- ✓ Downstream Bending Uniformity: Uniform mechanical yield profile guarantees repeatable press brake angles and reliable robotic welding fit-up.
Engineered for Continuous Heavy-Duty Industrial Output
Haden coil blanking lines seamlessly synchronize hydraulic uncoilers, 4-high or 6-high precision roller levelers, loop pit buffers, high-speed servo feeders, and continuous fiber laser cutting or mechanical shear modules. Every installation is engineered around your plant layout, material grades, and throughput goals.
Annual In-House Coil Blanking Savings Estimator
Calculate your estimated annual material and toll processing savings by transitioning from sheet blanks to master coils.
Cost Model Baseline Assumptions:
• Estimated third-party toll processing & blanking premium: $80 / metric ton.
• Scrap yield improvement: 9% net material reclamation via continuous dynamic nesting.
• Benchmark raw steel master coil price: $850 / metric ton.
Request a Custom Coil Processing Line Layout & Engineering Proposal
Share your material grades, strip thickness range, coil weights, target blank dimensions, and production requirements. Haden application engineers will review your application and develop a coil processing line configuration around your material flow, equipment requirements, and available floor space.
Dedicated Coil Processing Solutions Across Demanding Production Scenarios
High-throughput manufacturers face continuous pressure to accelerate blanking cycle times, eliminate raw material scrap, and process high-tensile alloys without dimensional distortion. Haden engineered coil processing solutions transform continuous master coils into stress-relieved, precision-cut workpieces optimized for demanding high-volume manufacturing environments.
By transitioning from pre-cut sheet handling to synchronized automated coil lines, industrial fabricators routinely achieve up to 92% to 95% material utilization and complete springback control. Explore our field-proven production line configurations across four major industrial sectors below.
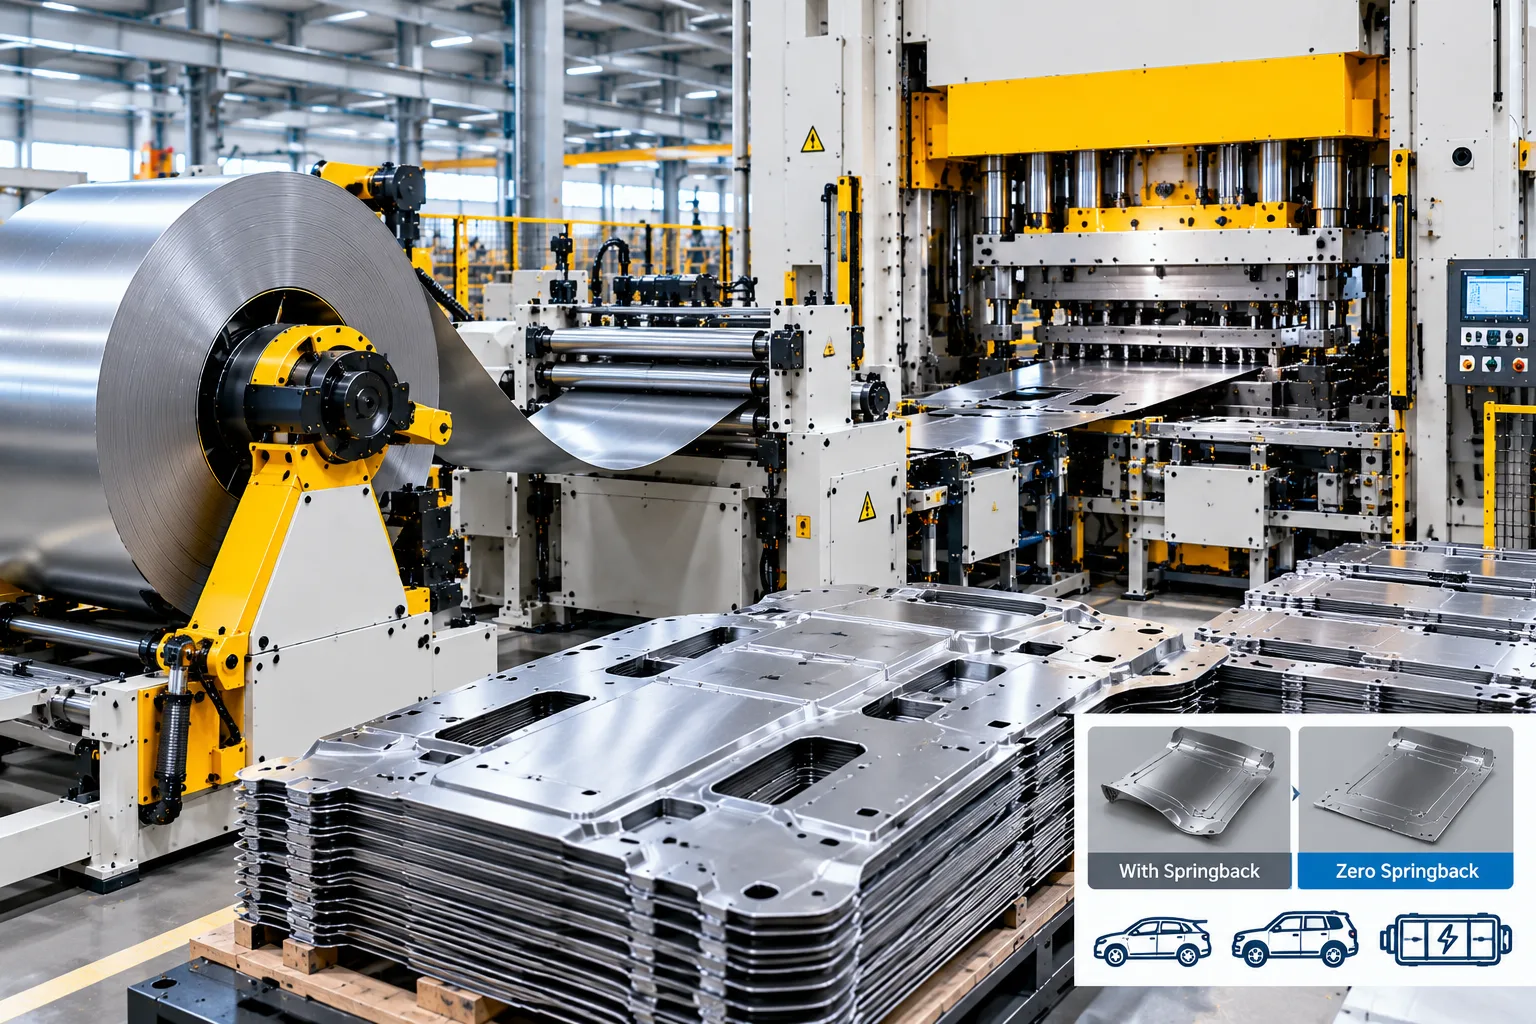
High-Strength Steel Blanking with Zero Springback for Automotive and EV Platforms
Electric vehicle battery pack trays, structural cross members, chassis sub-frames, and pillar reinforcements require advanced high-strength steels (AHSS) and structural aluminum alloys. Haden automotive coil blanking systems integrate 19-to-23-roll precision levelers that apply controlled alternating plastic bending, neutralizing coil memory and cross-bow before subsequent stamping or laser processing.
DP600 / DP980, 5000 & 6000 Series Al
±0.1 mm per Linear Meter
- ✓ Tooling-Free Laser Blanking: Continuous coil-fed sheet metal laser cutting machines process complex nested profiles without costly progressive blanking die lead times.
- ✓ Residual Stress Elimination: Multi-roller hydraulic cassette leveling prevents post-cut edge curling during automated robotic welding assemblies.
- ✓ High-Speed Non-Scratch Stacking: Synchronized magnetic and pneumatic drop-stackers organize delicate aluminum blanks without surface impingement.

Technical Line Configurations Across Specialized Coil Processing Sectors
Match your plant's product mix with engineered uncoiling, precision leveling, and continuous blanking capabilities.
| Industry Sector | Target Materials | Thickness Band | Leveling Roll Qty | Primary Blanking Method | Scrap Waste Reduction |
|---|---|---|---|---|---|
| Automotive & EV | AHSS, DP600/980, 6000-Series Al | 0.8 mm – 3.2 mm | 19 – 23 Rolls | Continuous Laser / Servo Press | 12% – 18% |
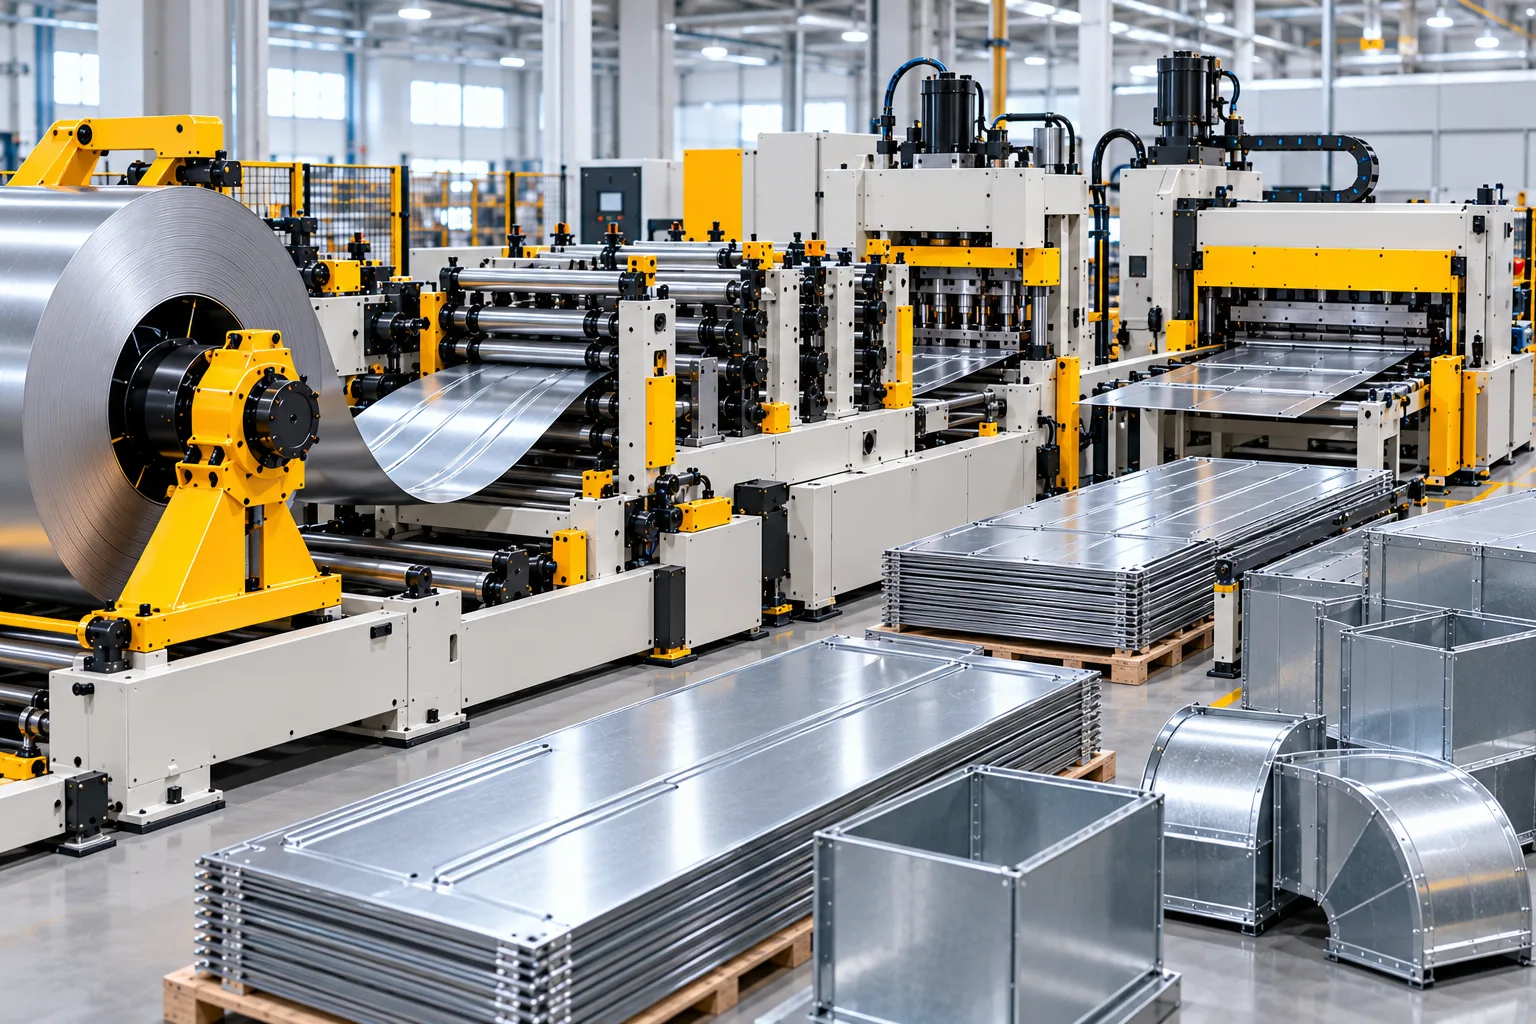
| HVAC Ductwork | G60 / G90 Galvanized Steel | 0.5 mm – 1.5 mm | 7 – 11 Rolls | Rotary Beader + Flying Shear | 8% – 14% |
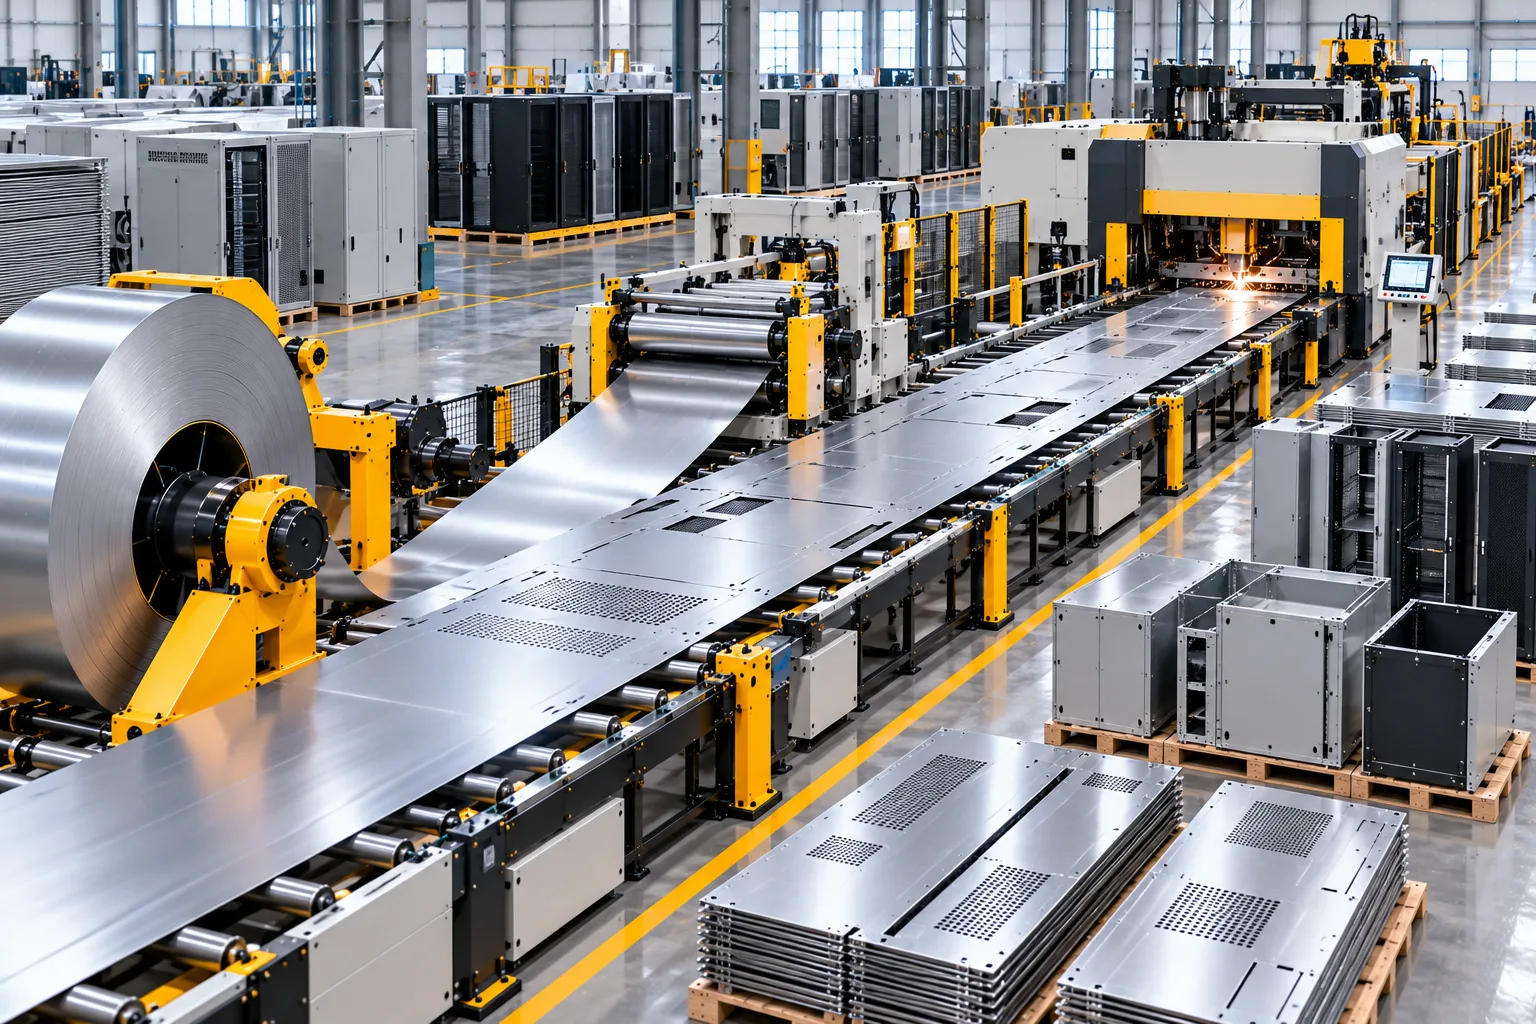
| Electrical Enclosures | CR4, SECC, Stainless 304 | 1.0 mm – 3.0 mm | 15 – 19 Rolls | Continuous Coil Laser Blanking | 14% – 22% |
| Appliances & Facades | Pre-painted, Brushed 316, Al | 0.6 mm – 2.5 mm | 19 – 21 Micro-Rolls | Precision Shear + Film Lamination | 10% – 16% |
Modular Line Topologies Engineered for Specific Factory Layouts
Every Haden coil processing line is modularized to match factory floor footprint, coil weight limitations, and target shift throughput.
Compact 3-in-1 Uncoiler-Leveler-Feeder Lines
Integrates decoiler, high-precision straightener, and NC servo feeder onto a rigid, unified mono-block frame. Drastically reduces factory footprint by eliminating deep pit buffers, making it ideal for space-constrained stamping plants.
Continuous Loop Coil Laser Blanking
Combines dynamic optical strip tracking with multi-head fiber laser cells. Delivers non-stop decoiling and continuous flying laser cutting, executing complex nested programs across virtually infinite strip lengths.
Heavy-Gauge Precision Cut-to-Length Systems
Engineered for plate thicknesses up to 25.0 mm with dual hydraulic wedge back-tension units and 4-high or 6-high cassette leveler drives. Guarantees true square cuts and mirror flatness across structural master coils.
Coil Processing Line Specifications & Sizing Guide
Compare standardized operational parameters across three specialized Haden machinery classes. Determine the optimal processing envelope, leveling capability, and speed profile for your facility, including automated setups paired with advanced laser cutting machines.
Light-Gauge Blanking & Laser Lines
Designed for rapid sheet processing, continuous blanking, and seamless integration with coil-fed laser cutting machines.
Automotive stampings, HVAC ducts, and precision enclosures fabricated via sheet metal laser cutting machines.
Medium-Plate Precision CTL Lines
Engineered for high-yield flat sheets, structural strip leveling, and precise dimensional shearing.
Heavy equipment frames, agricultural tooling, and industrial trailers.
Heavy-Duty Plate Processing Systems
Built to flatten extreme high-tensile hot-rolled steel plates and heavy uncoiled sheet slabs.
Shipbuilding plates, bridge girders, pressure vessels, and structural steel.
Standard Engineering Sizing Matrix
Haden Line Calibration Index| Technical Parameter | Class I: Light Gauge | Class II: Medium Plate | Class III: Heavy Plate |
|---|---|---|---|
| Strip Width Capacity | 600 mm – 1,600 mm | 1,000 mm – 2,000 mm | 1,200 mm – 2,500 mm |
| Maximum Coil Weight | 10 – 15 Metric Tons | 20 – 30 Metric Tons | 30 – 40 Metric Tons |
| Yield Strength Range (Re) | Up to 550 MPa | Up to 700 MPa | Up to 950 MPa (Dual Drive) |
| Leveling Roll Diameters | Ø 35 mm – Ø 50 mm | Ø 70 mm – Ø 120 mm | Ø 140 mm – Ø 220 mm |
| Length Cutting Precision | ± 0.15 mm / m | ± 0.30 mm / m | ± 0.50 mm / m |
| Shear Execution Type | High-Speed Rotary / Flying Laser | Hydraulic Guillotine / Bow-Tie | Hydraulic Heavy-Duty Stationary |
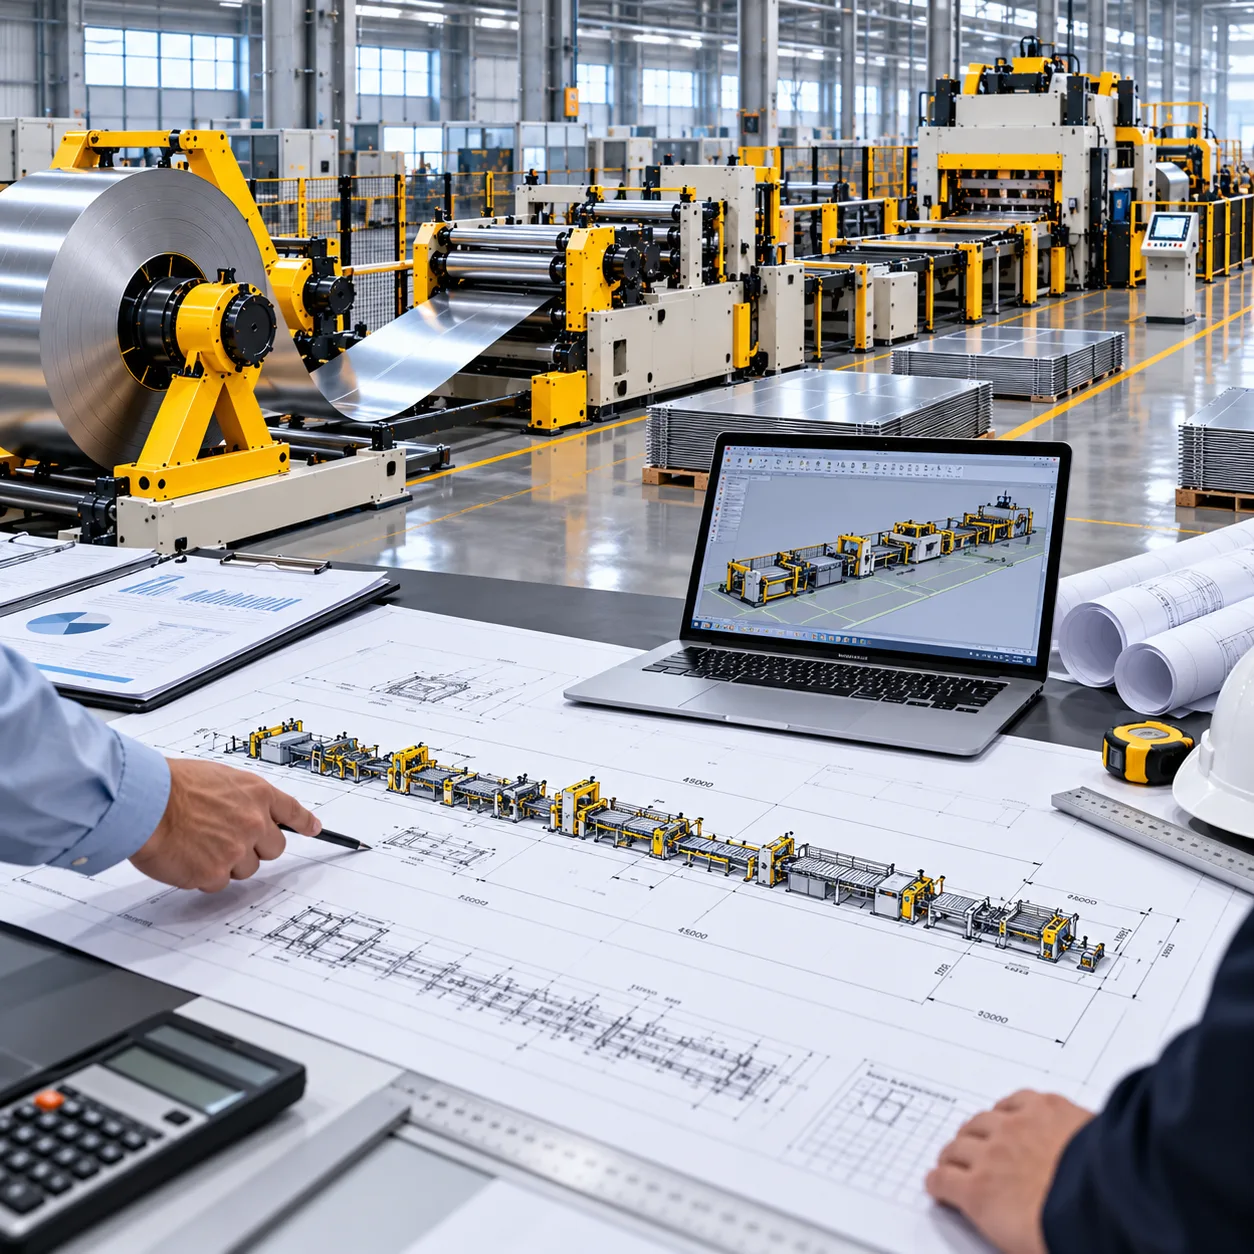
Engineering Resources for Line Sizing & Facility Planning
Access engineering guidance for equipment layout, utility planning, foundation requirements, and coil handling space. For project-specific dimensions and CAD integration, our application engineering team can review your material, production, and facility requirements.
Technical Insights and Coil Processing Frequently Asked Questions
Transitioning from discrete flat sheet manufacturing to automated coil processing lines introduces critical engineering considerations across residual stress mitigation, continuous nesting on high-performance laser cutting machines, rapid coil staging, and facility floor optimization. Below are detailed, engineering-backed explanations addressing the primary technical questions encountered by plant managers, manufacturing engineers, and production executives.
Core Engineering Principles
Eliminating mechanical memory and latent lattice stresses requires precise multi-axis deformation. Haden automated coil processing systems stabilize master coils into dead-flat strip for high-tolerance continuous downstream blanking, punching, and forming.
Plastic-Elastic Alternating Bending
Graduated multi-roller arrays elongate strip outer fibers past the material yield point to neutralize internal cross-section tension.
Continuous Dynamic Synchronization
Non-contact optical and ultrasonic looping pits buffer uncoiler payout velocities with pulsed servo feeding or on-the-fly laser heads.
Compact Monobloc Integration
Space-saving 3-in-1 line architectures merge heavy uncoiling, precision flattening, and NC feeding on a single rigid base.
Standard uncoiler straighteners typically feature 5 to 7 large-diameter rolls designed solely to remove basic coil curvature (coil set) so material can enter downstream dies without mechanical jamming. However, these basic straighteners do not alter internal strain differentials across the sheet cross-section, leaving severe residual stresses such as edge waves, center buckle, and longitudinal camber intact. When parts cut from un-leveled coil undergo secondary fiber laser cutting, CNC press brake bending, or robotic welding, these latent stresses release unpredictably, causing severe thermal distortion, angular springback variation, and dimensional rejections.
Haden high-precision coil leveling machines integrate 19 to 23 micro-adjustable rolls supported by multi-segment adjustable backup roller flights. By subjecting the material strip to calculated, decreasing alternating reverse bends, the machine stretches outer fibers beyond their yield point (typically 70% to 80% plastic deformation on entry, diminishing to pure elastic recovery at the exit). This homogeneous stress redistribution eliminates material memory, delivers flatness tolerances down to ±0.1 mm/m, and guarantees consistent dimensional stability during subsequent cutting and forming operations.
Configure a Coil Processing Line Around Your Production
Tell us what you need to process. Haden application engineers can review your requirements and help define the appropriate line configuration, equipment scope, and facility layout.
Tell Us About Your Application
A few basic details are enough to start. Our engineering team can follow up for additional technical information if needed.
Start With the Application. We’ll Work Through the Details.
You do not need a complete machine specification before contacting us. Basic information about your material, parts, and production goals is enough for an initial engineering review.
Line Configuration
Match uncoiling, leveling, feeding, cutting, and automation equipment to your application.
Facility Layout
Review equipment footprint, coil loading access, material flow, operator space, and downstream integration.
Technical Scope
Define the preliminary machine configuration, utilities, integration requirements, and project scope.
If you already have drawings, material specifications, or a production-line concept, you can send them after the initial inquiry.
Explore Engineering CapabilitiesShare Your Application
Tell us what material and products you need to process.
Engineering Review
We review the process requirements and suitable line architecture.
Configure the Solution
Develop the equipment scope, layout, and project proposal.