
Precision Leveling & Cut-to-Length Lines
Integrated coil processing lines combining uncoiling, precision leveling, servo feeding, cut-to-length shearing, and automated stacking. Configure material thickness, strip width, line speed, cutting method, and handling automation around your production requirements and downstream laser cutting machines .
Configurable for thin sheet, high-strength steel, and heavier coil-processing applications.
Line speed can be configured around material, feeding, shearing, and stacking requirements.
Servo-controlled feeding supports repeatable sheet-length positioning across continuous production.
Material guidance and line alignment support consistent sheet squareness for downstream fabrication.
Available processing ranges, line speeds, and accuracy depend on material properties, coil dimensions, and line configuration.
End-to-End Coil Processing Workflow and Core Station Engineering
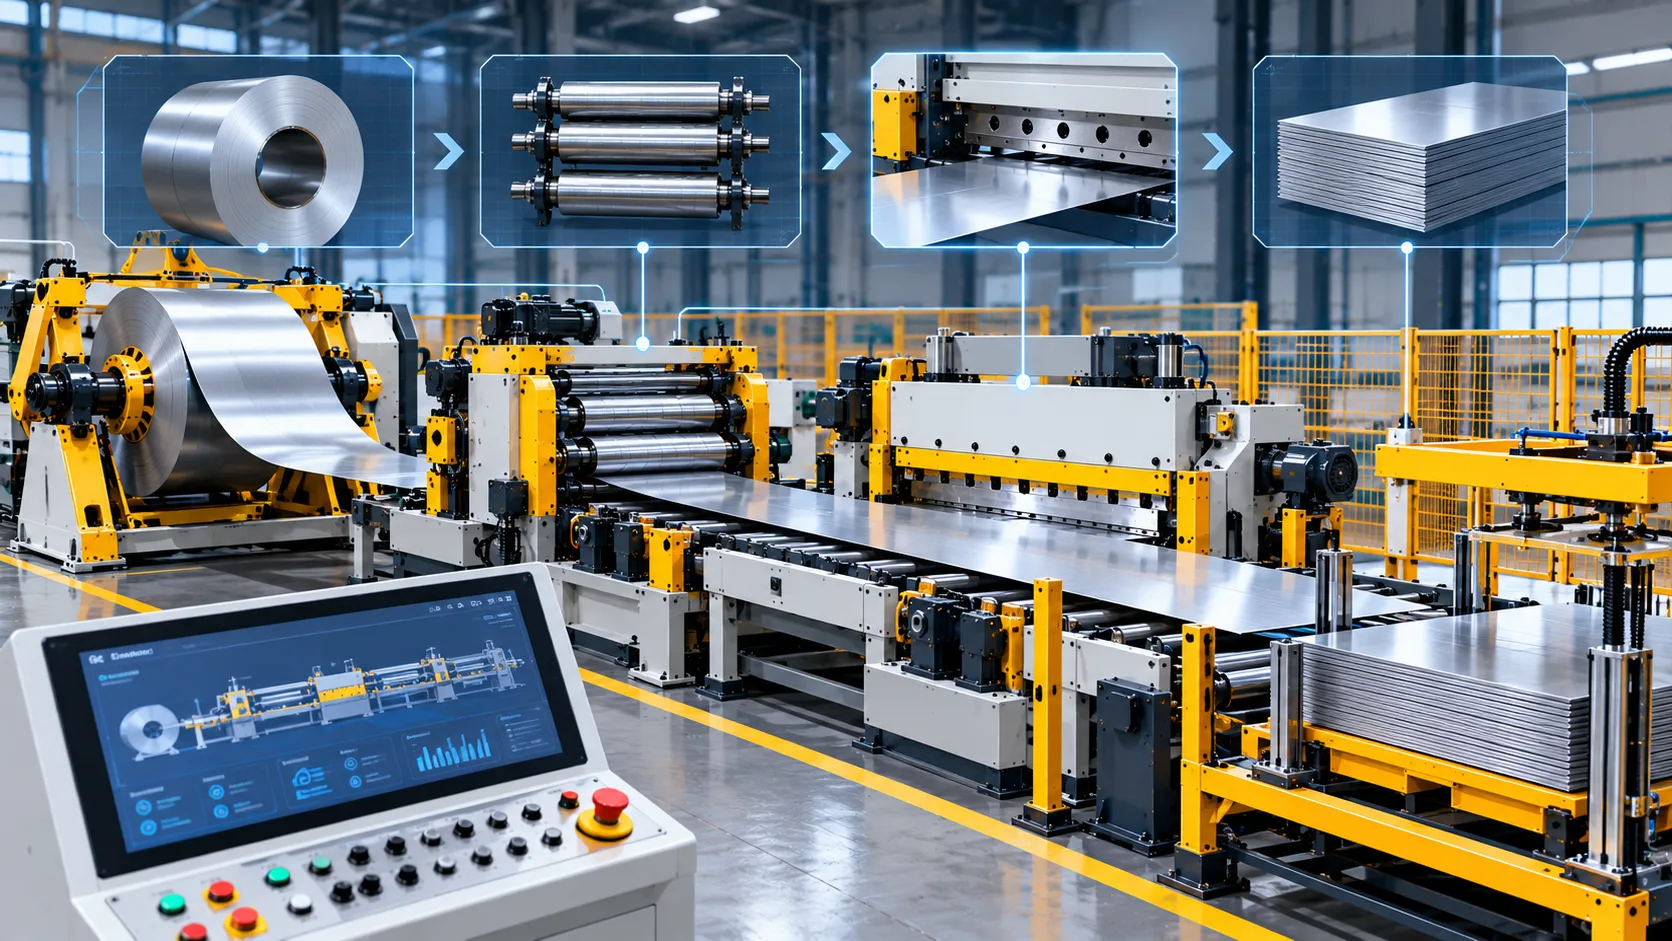
Transforming raw master coils into laser-flat, stress-free sheet blanks requires exact mechanical synchronization, continuous back-tension control, and closed-loop servo feedback. Haden engineers robust heavy-duty automation across every machine station. Explore how our integrated uncoiler leveler shear stacker workflow eliminates residual stresses, shields sensitive cosmetic surfaces, and delivers precise cut-to-length accuracy—complementing high-yield coil-fed laser cutting machines for structural plate, automotive high-strength alloys, and surface-critical aluminum.
Coil Staging, Loading, and Mandrel Decoiling Unit
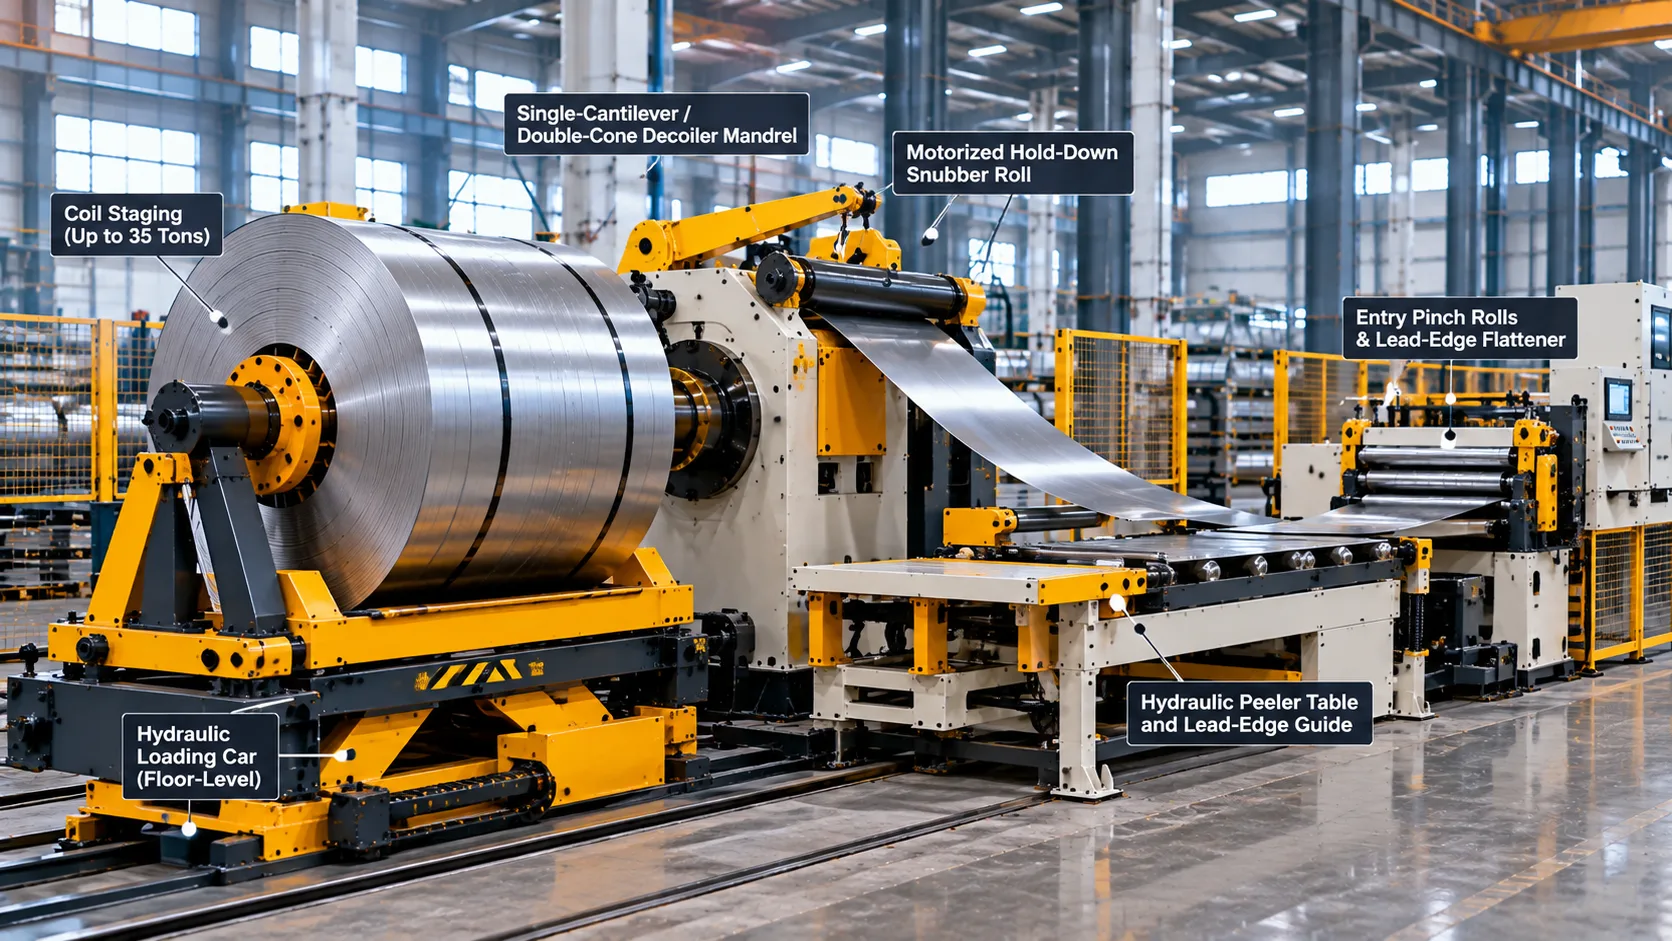
The entry station secures heavy coil staging without scuffing outer wraps. A floor-level hydraulic loading car positions coils up to 35 metric tons directly onto single-cantilever or double-cone decoiler mandrels. A motorized hold-down snubber roll applies regulated radial pressure to prevent coil clock-springing during strap removal, while the hydraulic peeler table and lead-edge flattener automatically guide heavy strip into downstream pinch rolls.
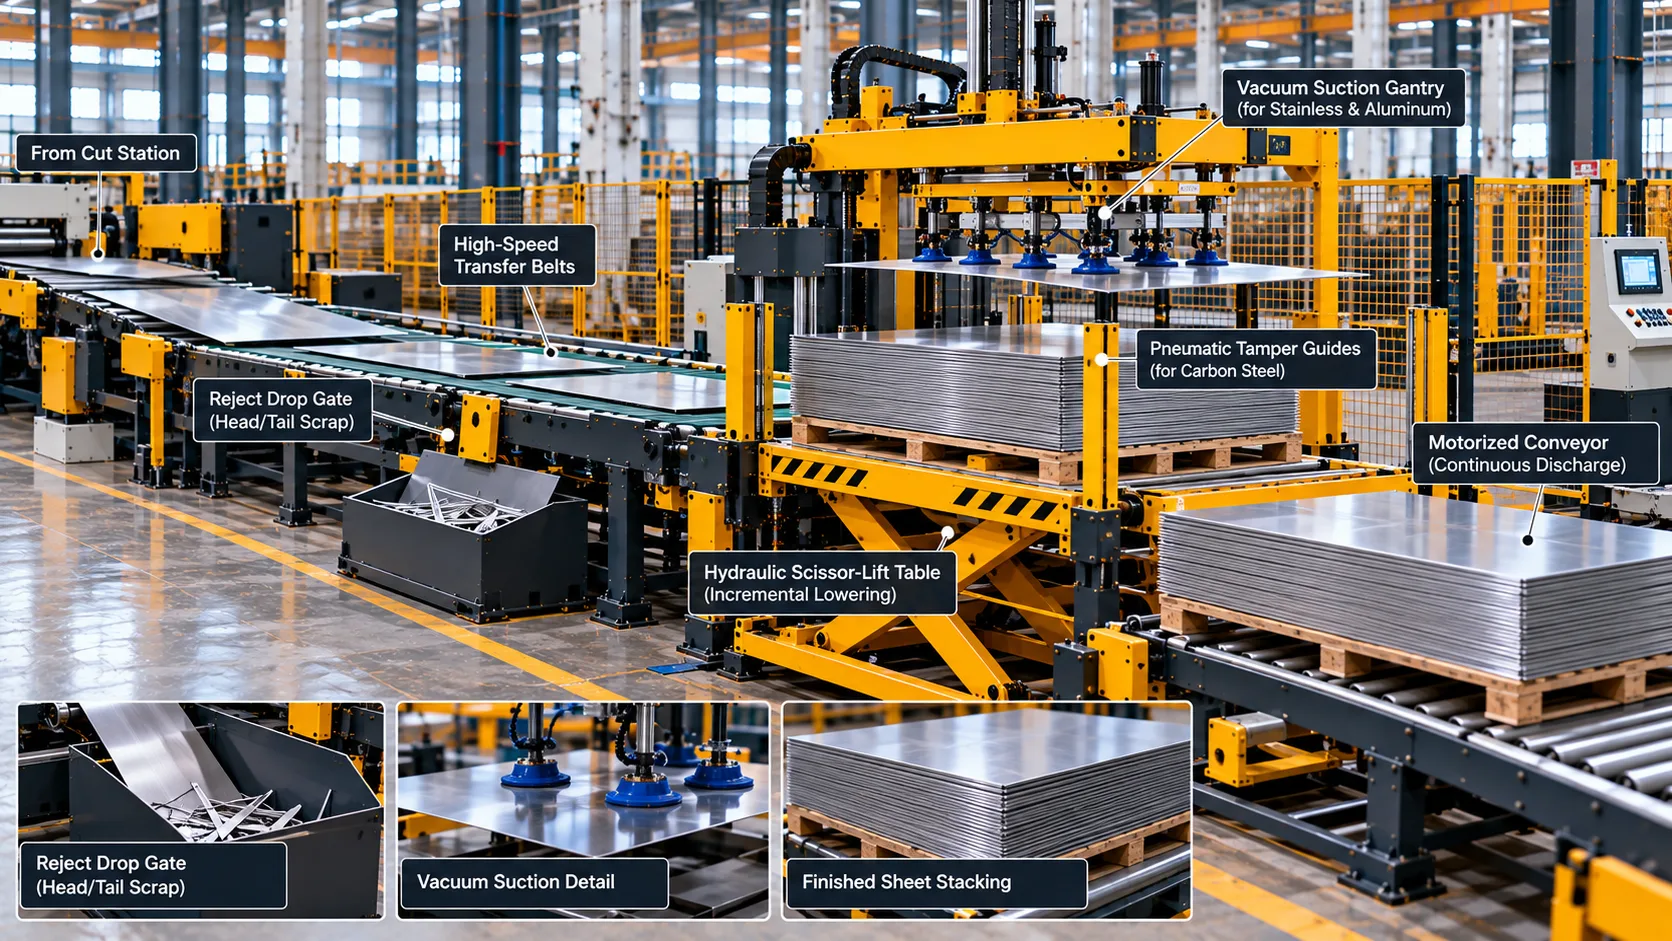
Synchronized Mechanical Engineering Across Stations
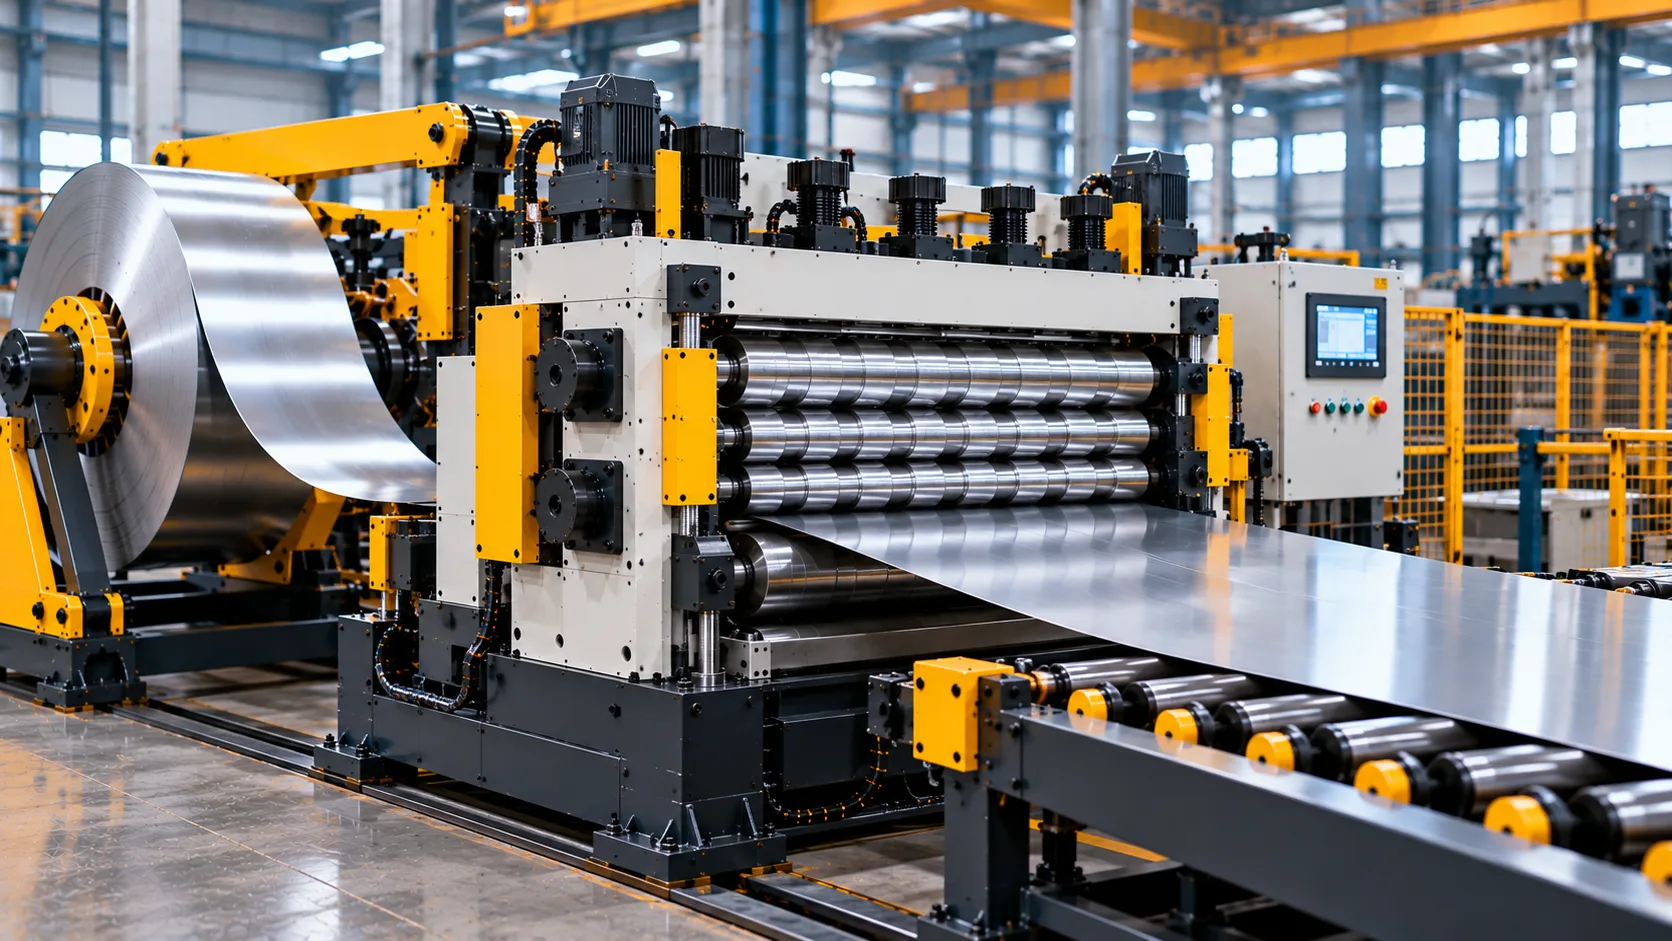
The structural efficiency of an automated cut to length line relies on tight mechanical and electronic synchronization across every module. As master coils unwind, varying coil diameters create continuous shifts in rotational inertia. Haden incorporates proportional hydraulic back-tension controls that communicate directly with the precision leveler drive. This dynamic balance prevents strip slippage, maintains roll traction, and avoids inter-station stretching that could compromise gauge uniformity.
- 1 Continuous Tension Feedback: Load-cell tension bridles coordinate with regenerative drives to eliminate coil cinching and loose outer wraps.
- 2 Dynamic Loop Cushioning: Variable-speed inverter controls maintain optimal loop geometry, dampening shock pulses during shear cycles.
- 3 Synchronized Acceleration Curves: Programmed S-curve velocity profiles eliminate roll skid marks when servo feed rolls index sensitive strip stock.
Integrated Surface Protection and Scratch Prevention
Automotive exterior skins, architectural stainless steel, and pre-painted appliance panels demand complete surface integrity. Throughout each station of the Haden uncoiler leveler shear stacker line, metal-to-metal rubbing on cosmetic faces is systematically eliminated through specialized contact materials, air flotation, and non-contact transfer engineering.
- • Polyurethane and Chromed Surfaces: Deflector and pinch rolls feature mirror-polished hard chrome or vulcanized 90-durometer polyurethane coatings.
- • Air-Cushioned Transfer Tables: Pneumatic air tables float sheet undersides across the looping pit and shearing transition zones to prevent abrasion.
- • Overhead Vacuum Stacking: High-volume vacuum suction cups gently handle individual sheets from the top side, eliminating edge scraping common in drop-box systems.
Station Architecture and Technical Performance Matrix
A structured engineering overview of sub-assemblies, control mechanisms, and performance ratings across the five line stations.
| Station Name | Core Mechanical Sub-Assemblies | Control & Sensor Logic | Operational Range | Surface Protection Measure |
|---|---|---|---|---|
| 01. Decoiling Unit | Floor car, expanding mandrel, snubber roll, peeler blade | Hydraulic proportional back-pressure valve | Coils up to 35 tons; 508–610 mm ID | Segmented rubber mandrel sleeves |
| 02. Precision Leveler | 4-high / 6-high cassette, intermediate & backup rolls | Closed-loop servo gap regulation via linear encoders | 0.3 mm – 25.0 mm strip thickness | Automated cassette extraction & roll cleaning |
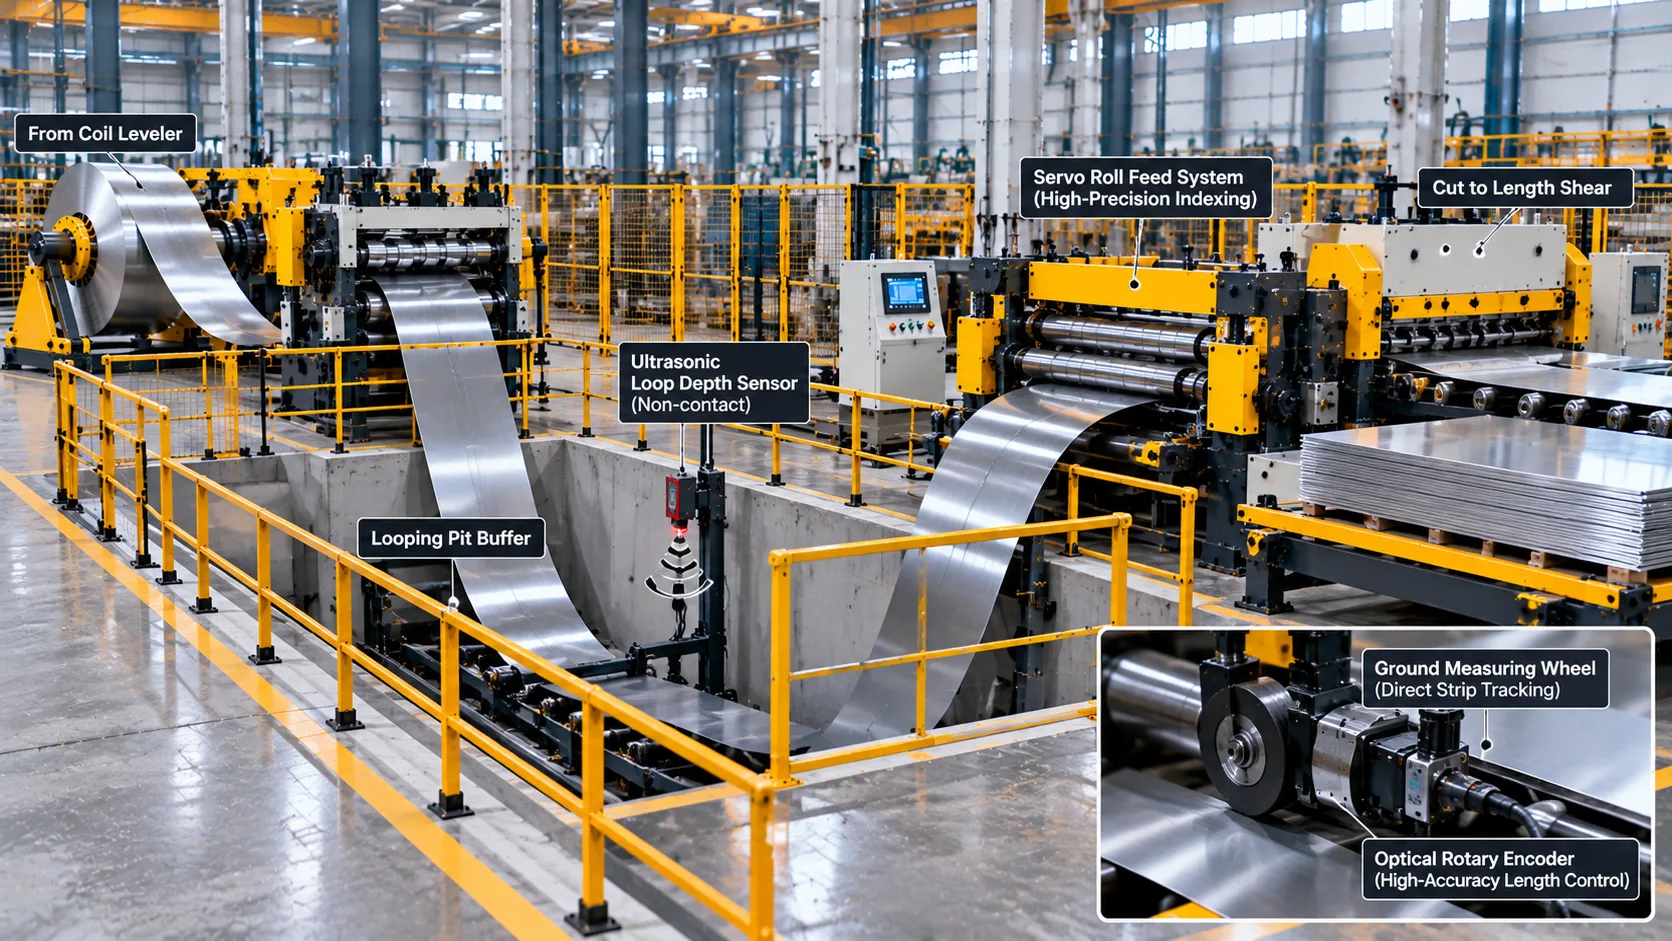
| 03. Looping & Feeding | Looping pit, side guide centering, dual servo feed rolls | Ultrasonic pit sonar + optical measuring wheel | Feed speed up to 100 m/min | Polyurethane roll covers & air-cushion tables |
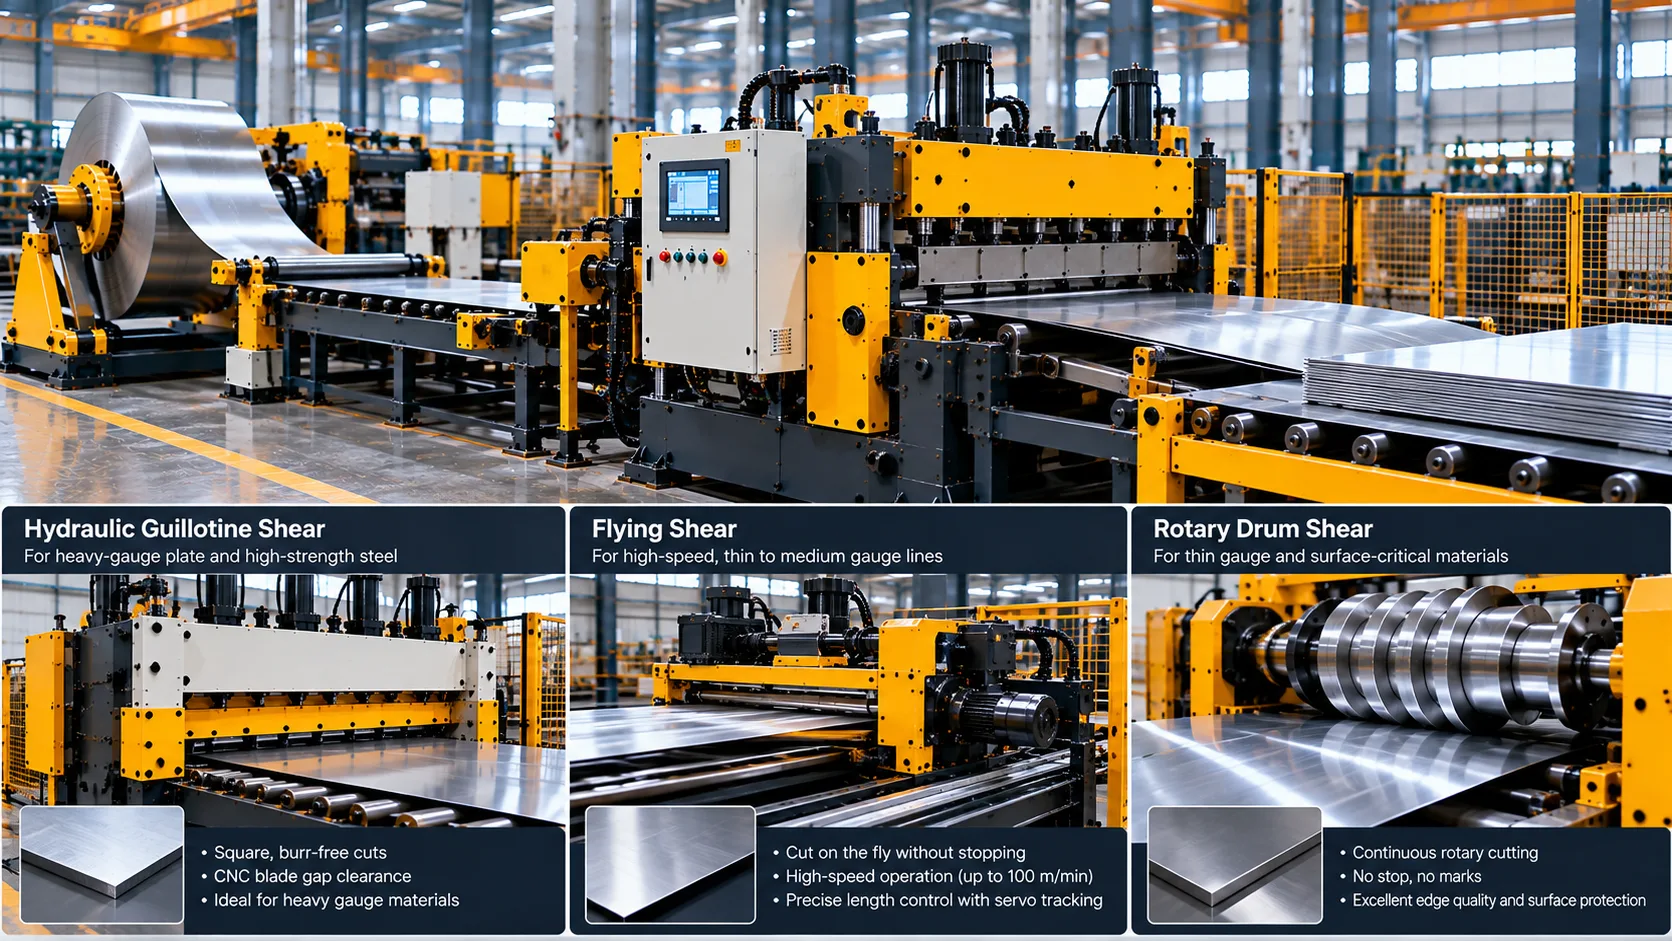
| 04. Shearing System | Hydraulic guillotine, flying shear carriage, or rotary drum | Motorized CNC blade gap & rake angle automation | Lengths 200 mm to 12,000 mm | Synchronized velocity matching during cut |
| 05. Automated Stacker | Pneumatic drop, overhead vacuum/magnetic, scissor lift | Dual photo-eye edge squaring & weight cells | Packs up to 10,000 kg per bay | Top-side suction arms & soft-side bumpers |
Configure Your Tailored Coil Processing Workflow
Every metal alloy, gauge range, and daily tonnage target requires an engineered match of uncoilers, levelers, shears, and automated stackers. Let Haden application engineers evaluate your coil specifications to configure an optimized turnkey layout for your shop floor.
Modular Line Configurations and Model Selection Matrix
Optimizing metal coil leveling and shearing requires an exact mechanical match between raw material yield strength, gauge range, strip width, and target throughput. Haden builds modular cut to length lines configured specifically to balance capital investment with operational velocity. Whether processing ultra-thin surface-critical appliance sheets or heavy structural carbon steel plates, our standardized machine frames and interchangeable sub-assemblies deliver high mechanical rigidity, zero strip damage, and tight length tolerances.
Explore our four core production line architectures below. Each configuration integrates closed-loop hydraulic roll positioning, synchronized servo roll feeding, dynamic stress-relieving multi-roll levelers, and automated stacking cells tailored to high-demand fabrication environments.
Light Gauge High-Speed Cut to Length Line
Engineered for toll processors, electrical enclosure builders, and appliance manufacturers requiring rapid processing of cold-rolled steel, galvanized coils, prepainted sheets, and surface-sensitive stainless steel. This high-velocity line configuration integrates a deep looping pit accumulator with micro-diameter 6-high leveler rolls to eliminate work-roll print marks and neutralize residual edge wave or center buckle.
The high-response AC servo feed mechanism synchronizes with a high-cycling pneumatic or hydraulic stop-and-go shear. Advanced air-cushion flapper or drop stackers prevent friction scratches on critical face finishes like mirror No. 4 and BA stainless, ensuring laser-ready flat blanks directly off the stacking table for downstream processing on sheet metal laser cutting machines.
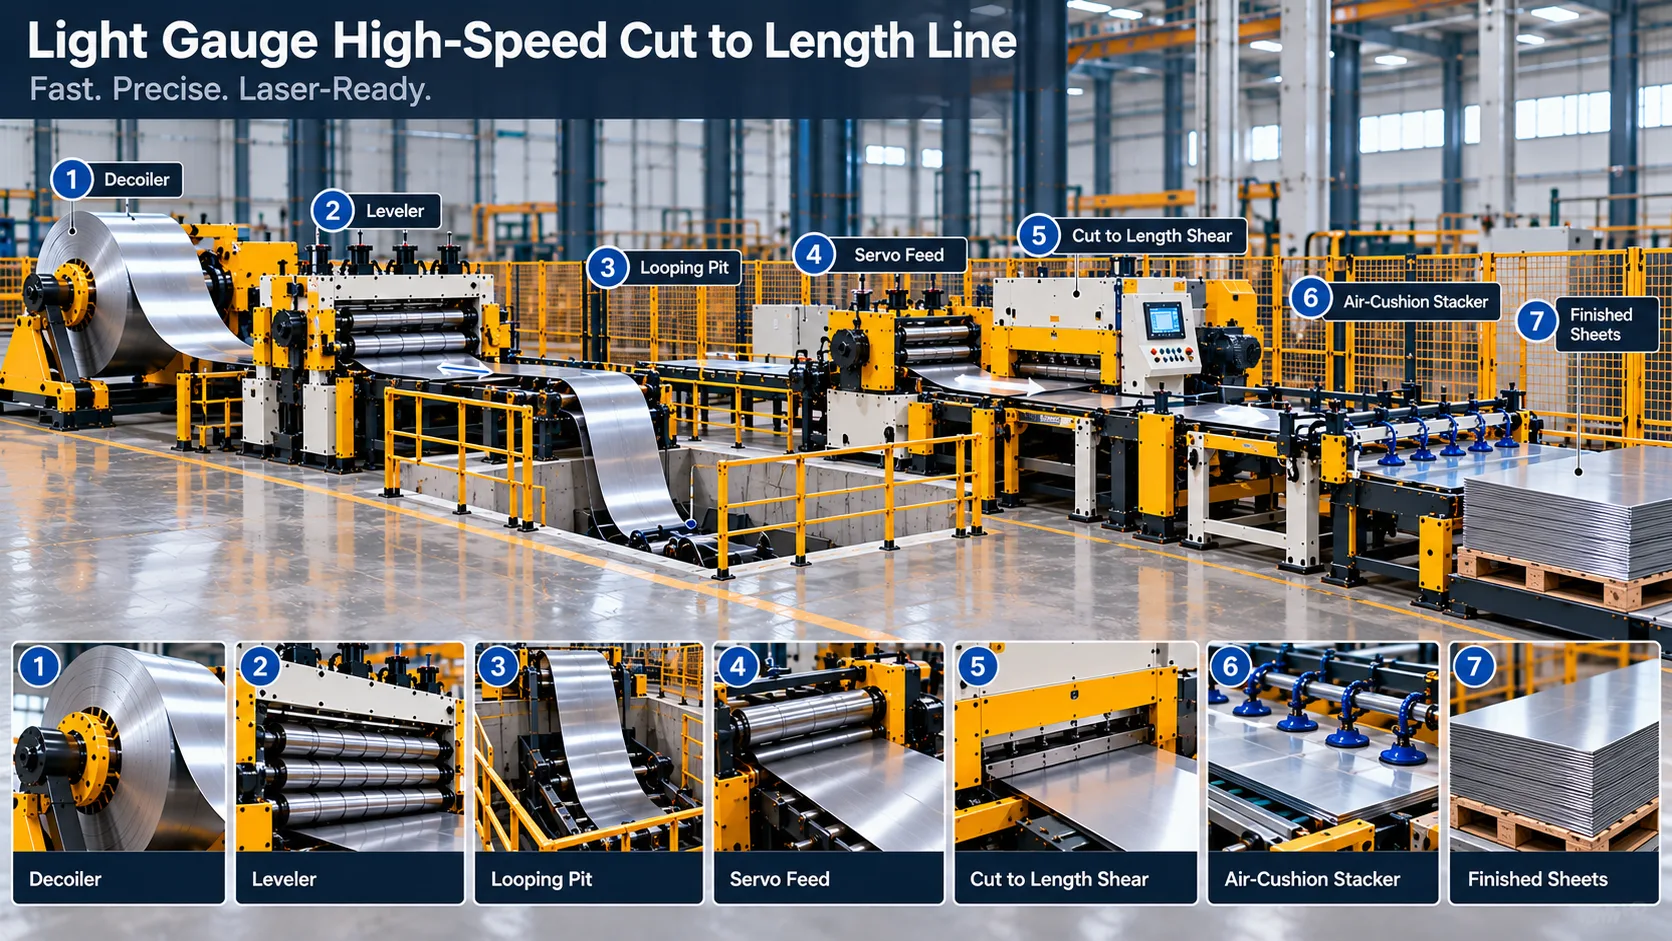
Core Station Highlights
- Cantilever uncoiler with hydraulic expansion & snubber roll
- 19 to 23 roll 6-high cassette leveler with intermediate backup rolls
- Dual-motor servo roll feeder with non-marking polyurethane wrap
- Pneumatic flapper stacker with scissor lift and side discharge
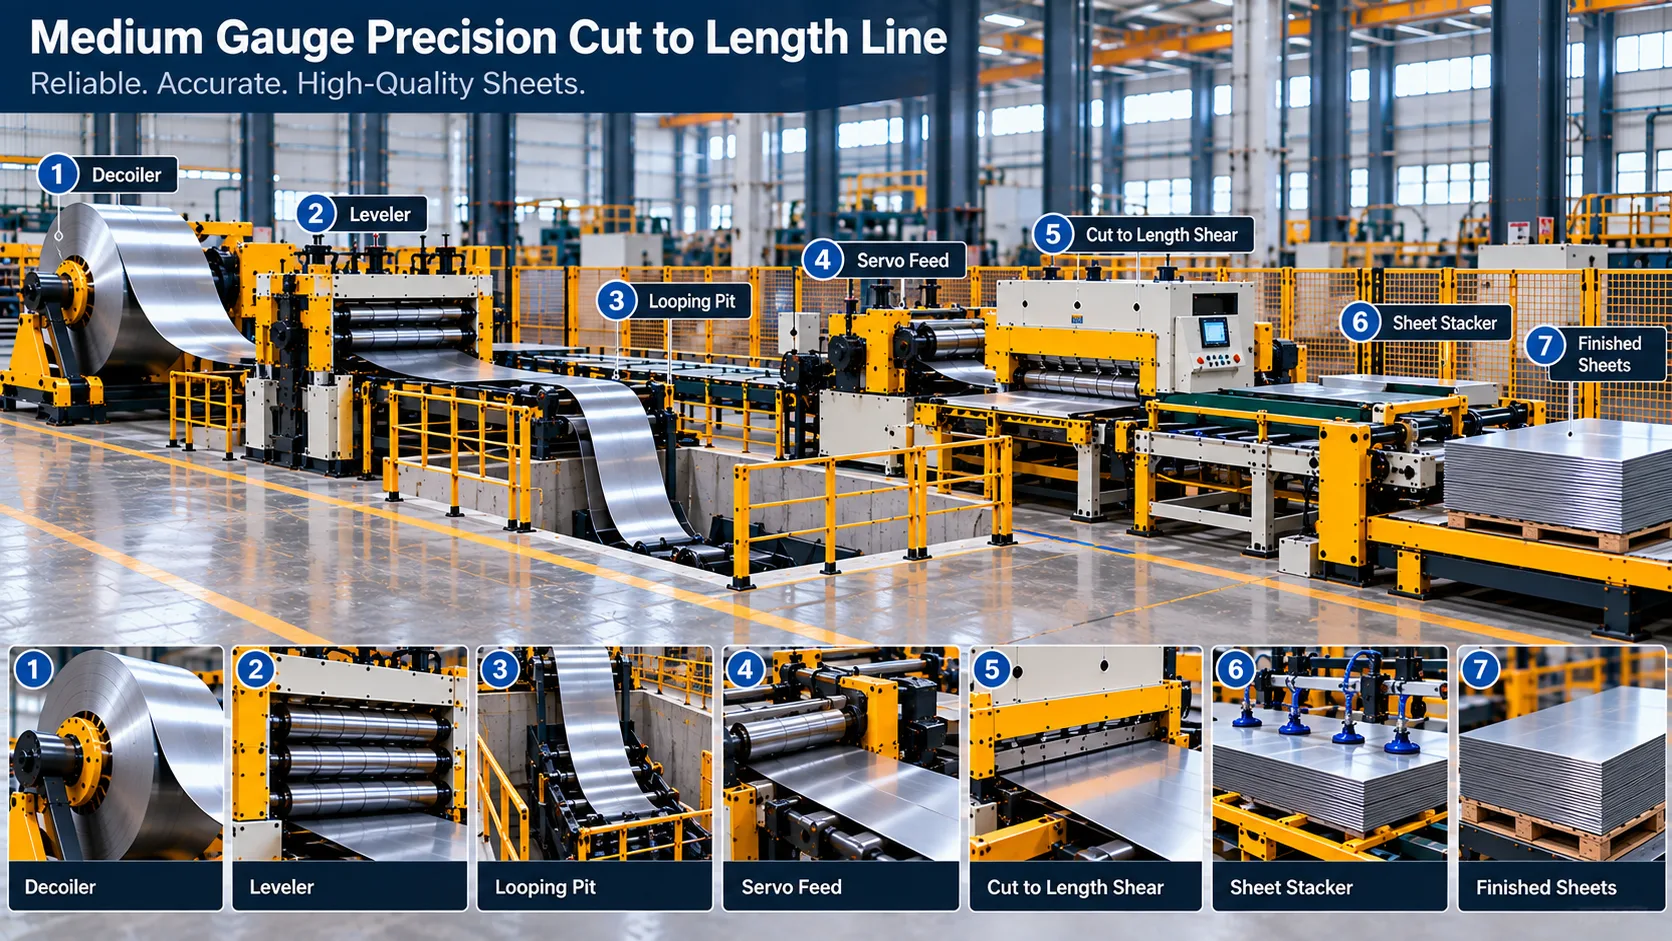
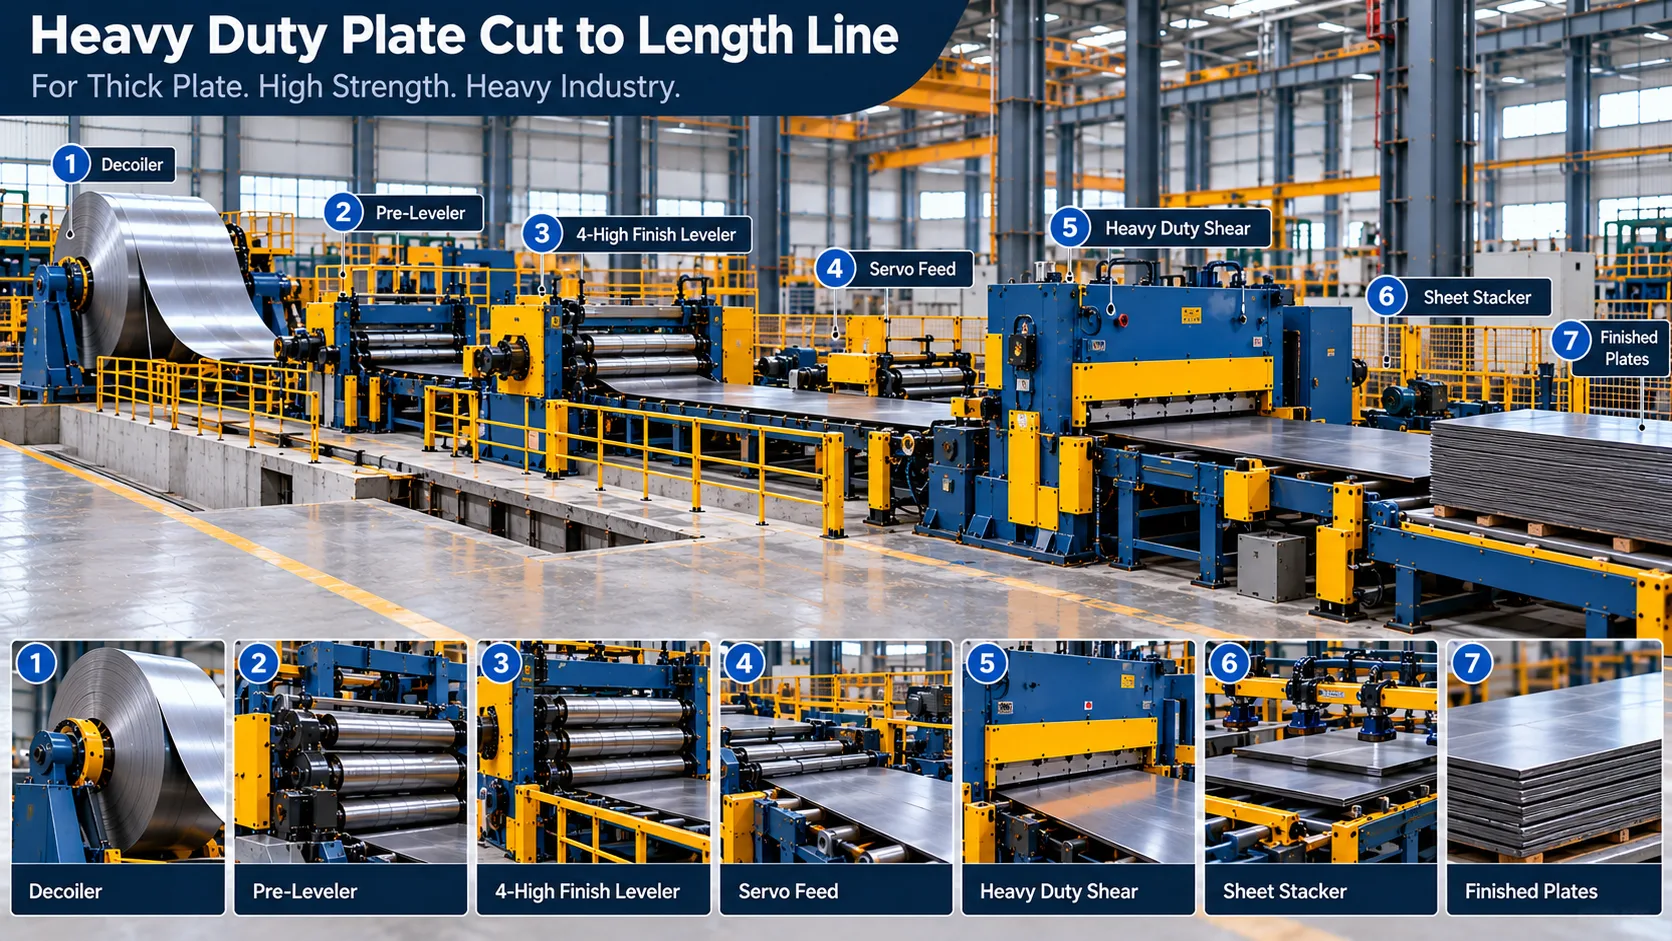
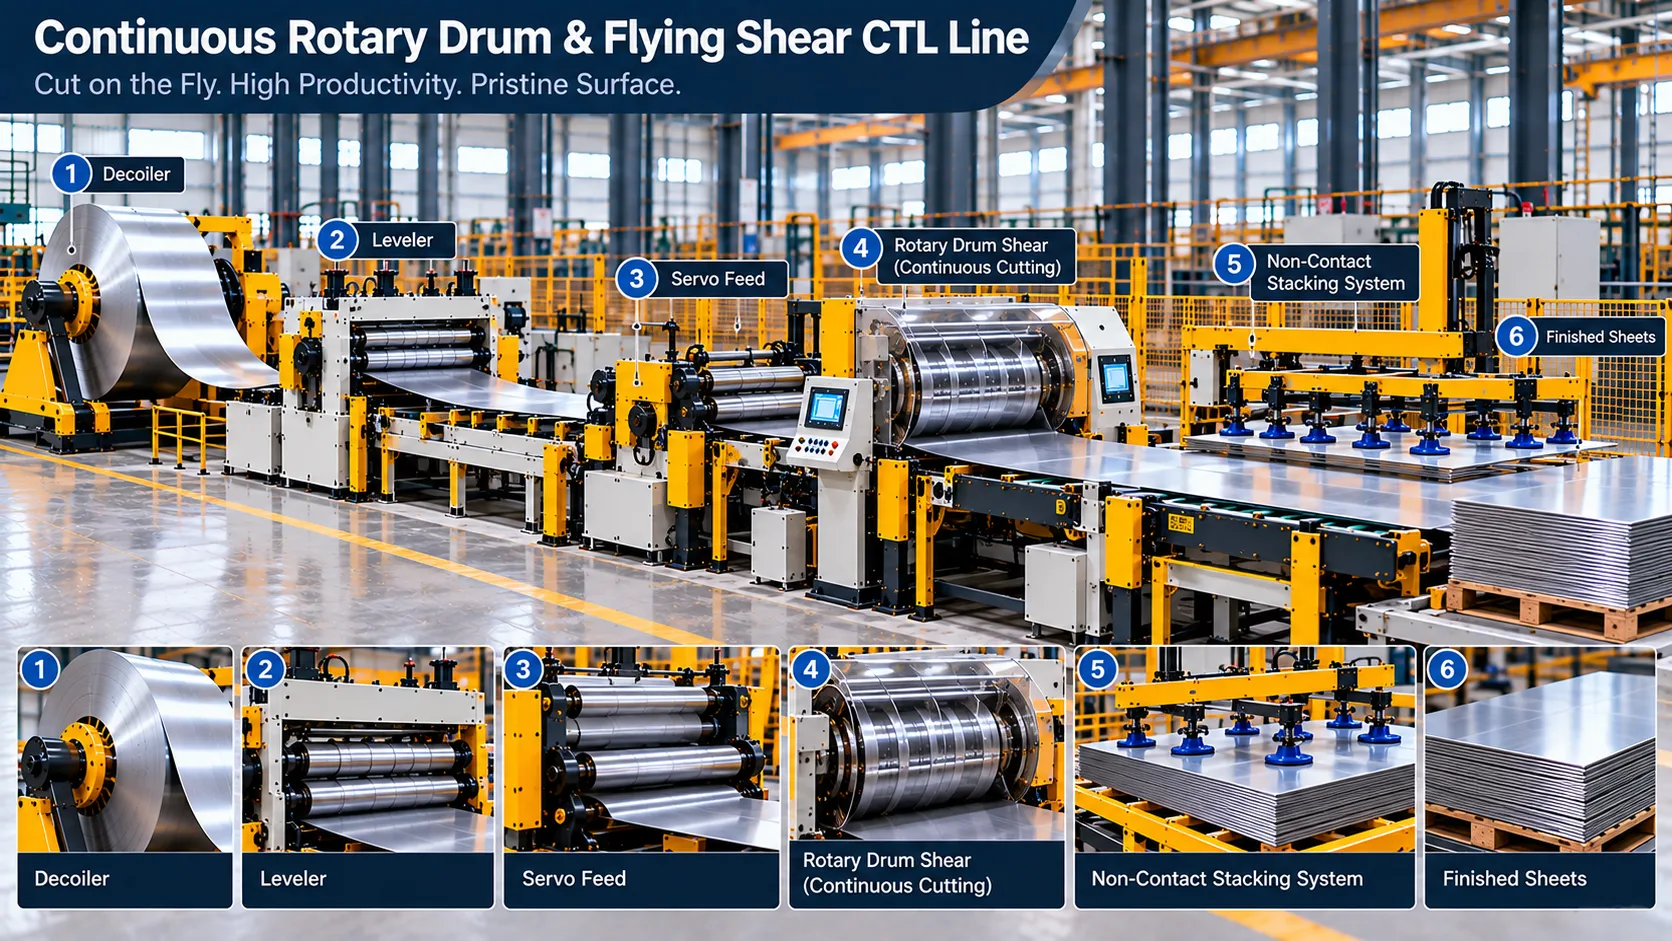
Model Selection Matrix & Technical Capabilities
Compare key mechanical specifications across standard Haden cut to length machine classifications to determine the optimal configuration for your material mix.
| Line Series | Thickness Range | Strip Width | Leveler Rollers | Shearing Architecture | Max Velocity | Primary Materials |
|---|---|---|---|---|---|---|
| CTL-Light-100 | 0.3 – 3.0 mm | 600 – 1600 mm | 19–23 Rolls (6-High) | Servo Stop Shear / Flying Shear | Up to 100 m/min | CR, GI, Stainless 2B/BA, Aluminum |
| CTL-Med-060 | 2.0 – 8.0 mm | 800 – 2000 mm | 15–19 Rolls (4-High / 6-High) | Eccentric Mechanical / Hydraulic Gate | Up to 60 m/min | HRPO, Structural Steel, Automotive AHSS |
| CTL-Heavy-035 | 6.0 – 25.0 mm | 1000 – 2500 mm | Pre-Leveler + 11–13 Rolls (4-High) | Heavy Hydraulic Guillotine with Rake Control | Up to 35 m/min | Hot Rolled Carbon, Heavy Plate, Q355–Q690 |
| CTL-Rotary-120 | 0.4 – 4.0 mm | 800 – 1800 mm | 21–25 Rolls (6-High Micro-Gap) | Continuous Synchronized Rotary Drum | Up to 120 m/min | Mirror Stainless, Painted Coil, Architectural |
* Note: Custom widths up to 2800 mm and specialized coil weights up to 40 tons are engineered upon request. All Haden systems comply with CE and ISO9001 quality and safety standards.
Request Custom Engineering ReviewCore Engineering Advantages and Sheet Flatness Control
Engineered for demanding coil service centers and Tier-1 manufacturing plants, Haden leveling and cut-to-length lines neutralize deep residual stress, safeguard sensitive decorative finishes, and maintain dead-flat tolerances compliant with stringent international flatness standards.
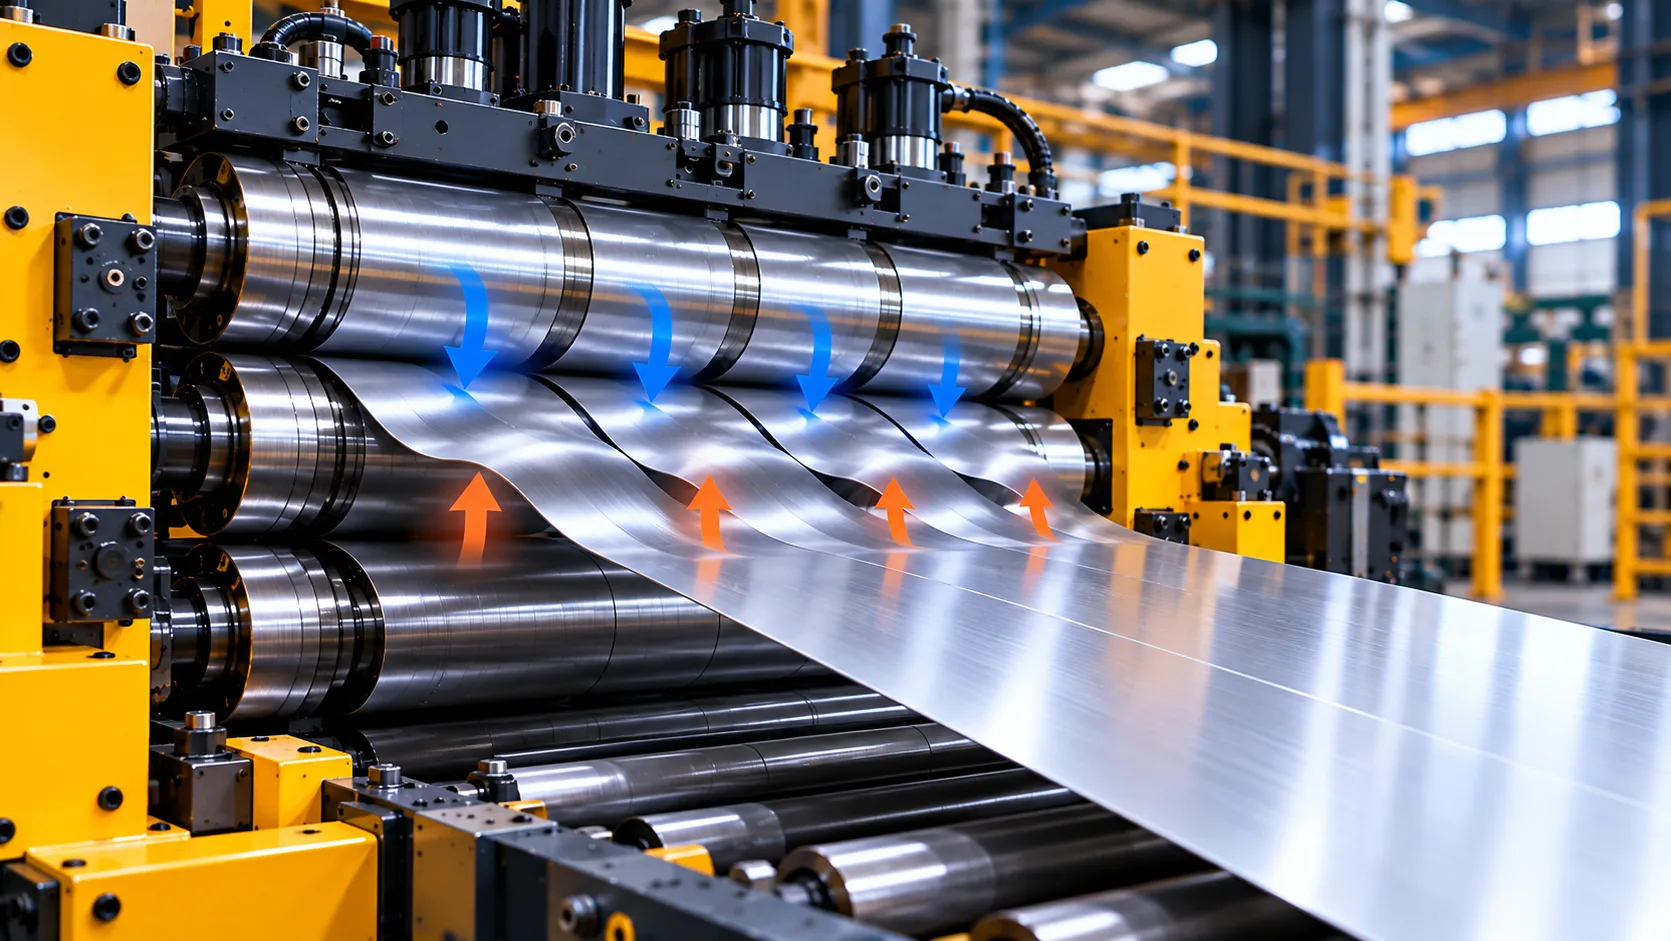
Precision Residual Stress Relief Dynamics
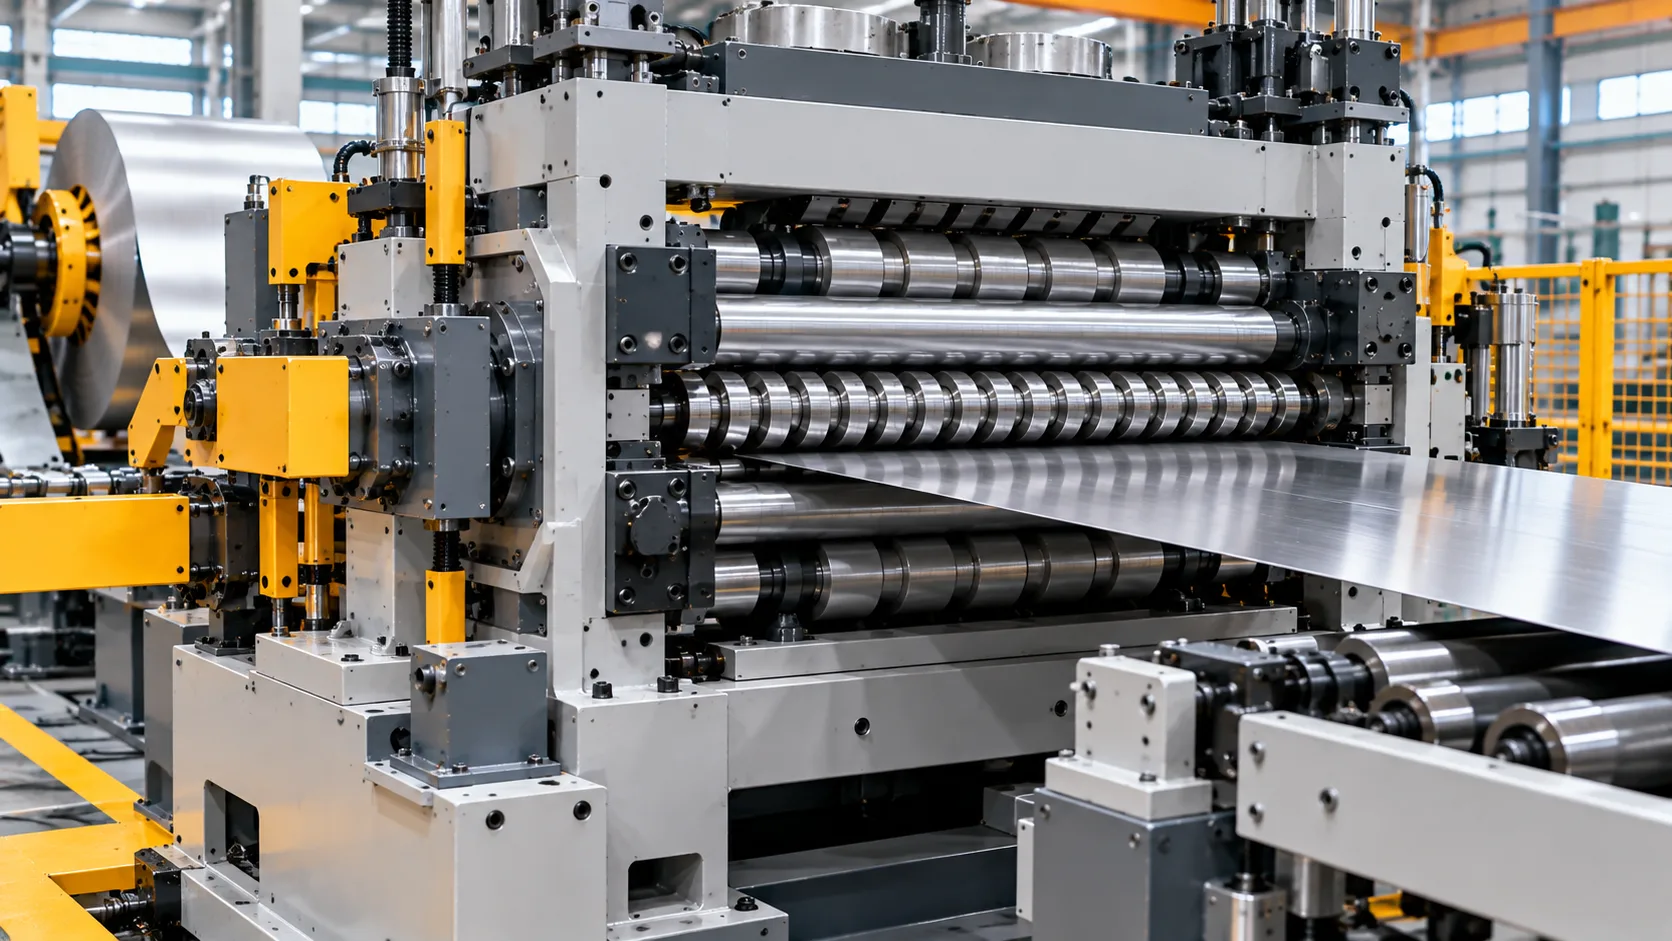
Through controlled alternating plastic-elastic deformation across multi-roll clusters, our levelers systematically erase longitudinal coil set, cross bow, center buckles, and edge waves. Neutralizing latent stress prevents sheet spring-back, thermal distortion, and costly cutting nozzle collisions during downstream processing on industrial laser cutting machines.
- • Eliminates coil memory across high-strength structural grades and standard carbon steels
- • Multi-point backup roll cassettes deliver localized crown and tilt micro-adjustments
- • Guarantees fiber-laser cutting stability without edge uplift or thermal bowing
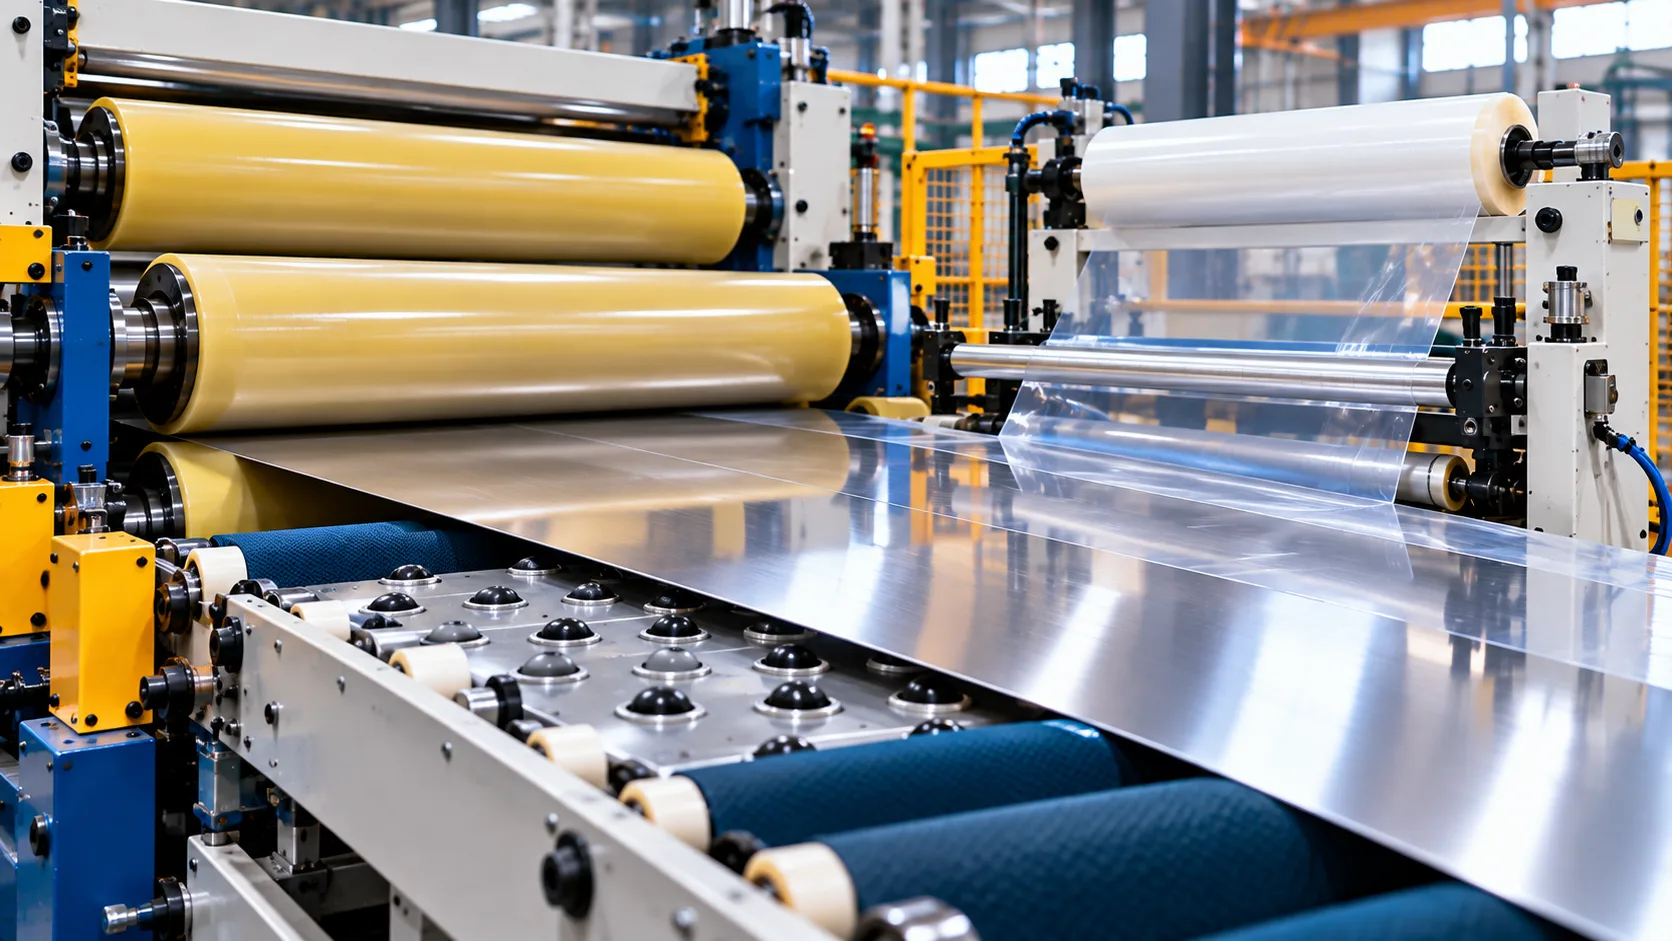
Scratch-Free Surface Protection Systems
Processing polished stainless steel, automotive aluminum, and pre-painted architectural coils requires zero surface compromise. Haden integrates vulcanized polyurethane rolls, non-marking transfer belts, pneumatic air-cushion tables, and optional online protective film applicators to safeguard critical finishes.
- • Specialty treated and coated roll surfaces prevent roll pickup, scuffing, and metal imprint
- • Non-contact air float tables and synchronized side dampening eliminate transfer dragging
- • Automated magnetic or vacuum drop stackers stack finished sheets without corner impact
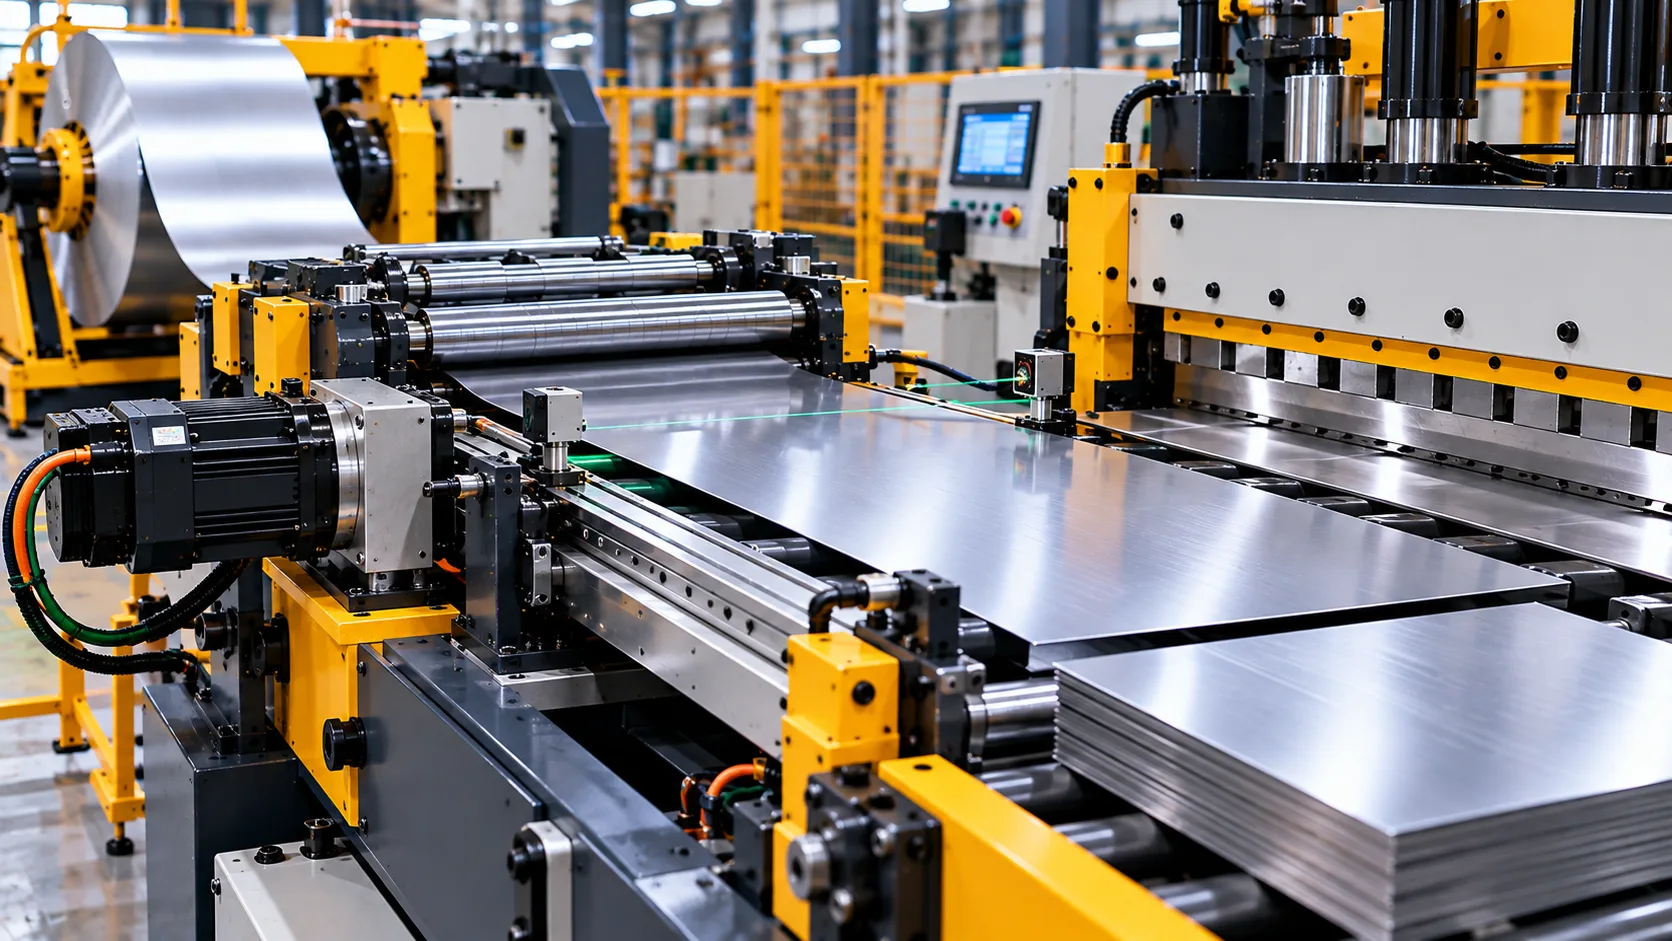
Closed-Loop Servo Length & Squareness Control
Driven by high-torque AC servomotors and optical rotary encoders, our precision roll feeds work in tandem with rigid side-centering tracks and high-rigidity shears. This closed-loop design delivers length tolerances within ±0.1 mm and diagonal tolerances within ±0.5 mm, even at line speeds up to 100 m/min.
- • Real-time encoder feedback compensates dynamically for material slip and acceleration inertia
- • Rigid guillotine, flying, or rotary shearing mechanisms produce clean, burr-free perpendicular cuts
- • Strict diagonal squareness control ensures seamless robotic press-brake and panel-bender feeding
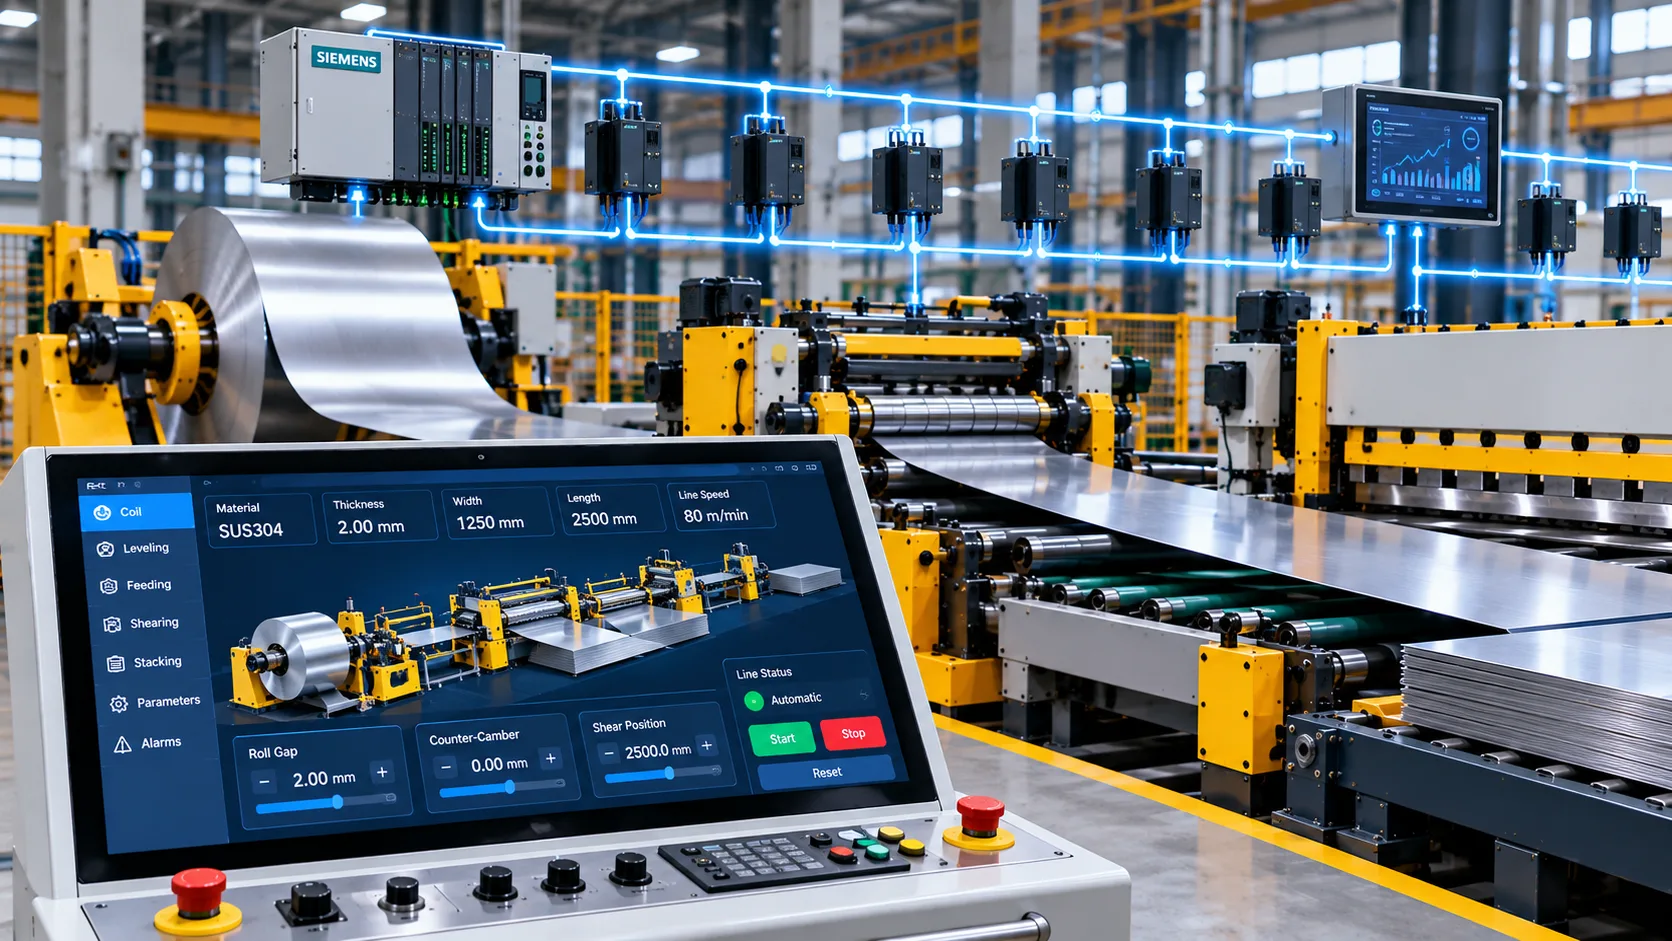
Industry 4.0 Smart CNC Bus Architecture
Centralized Siemens or Beckhoff industrial control architectures automate every phase of the leveling cycle. Operators select material grade, coil thickness, and target dimensions on an intuitive HMI, triggering automated motorized roll-gap positioning, hydraulic counter-camber curves, and synchronized shear cycles.
- • Comprehensive recipe management system slashes tooling and job changeover times to under 5 minutes
- • Automated motorized gap and roll-tilt positioning driven by precision hydraulic-wedge servos
- • Industrial Ethernet, OPC-UA, and cloud telemetry provide live line diagnostics and MES tracking
Why Precision Flatness Dictates Downstream Profitability
Unrelieved stresses in coiled strip create latent defects that surface only when sheets are subjected to intense thermal or mechanical work downstream. During multi-kilowatt processing on sheet metal laser cutting machines, residual tension causes severed cutouts to snap upward, precipitating costly laser head crashes, machine downtime, and scrapped blanks. In automated stamping dies and robotic welding fixtures, uneven curvature produces dimensional drift, irregular seam gaps, and tool binding.
Haden leveling and cut-to-length lines satisfy demanding European flatness norms (EN 10051) and strict ASTM standards. By combining optimized roll geometry, rigid multi-point support cassettes, and responsive servo feeds, Haden supplies blanks that load smoothly, cut cleanly, and seamlessly integrate with continuous coil-fed laser cutting machines and forming presses across carbon steels, stainless grades, and advanced high-strength alloys.
Cut-to-Length Line Specifications & Capacity Matrix
Operational specifications across Haden standard and heavy-gauge cut-to-length processing lines. Built for tight tolerance control and residual stress relief across cold-rolled, stainless, aluminum, and advanced high-strength steels optimized for high-performance laser cutting machines.
Precision Flatness Control for Advanced High-Strength Alloys
Haden cut-to-length lines combine closed-loop hydraulic roll bending, multi-flight back-up cassettes, and high-dynamic servo shears. Each system relieves internal material stress while delivering optical-grade surface protection and accurate squareness for downstream sheet metal laser cutting machines and stamping.
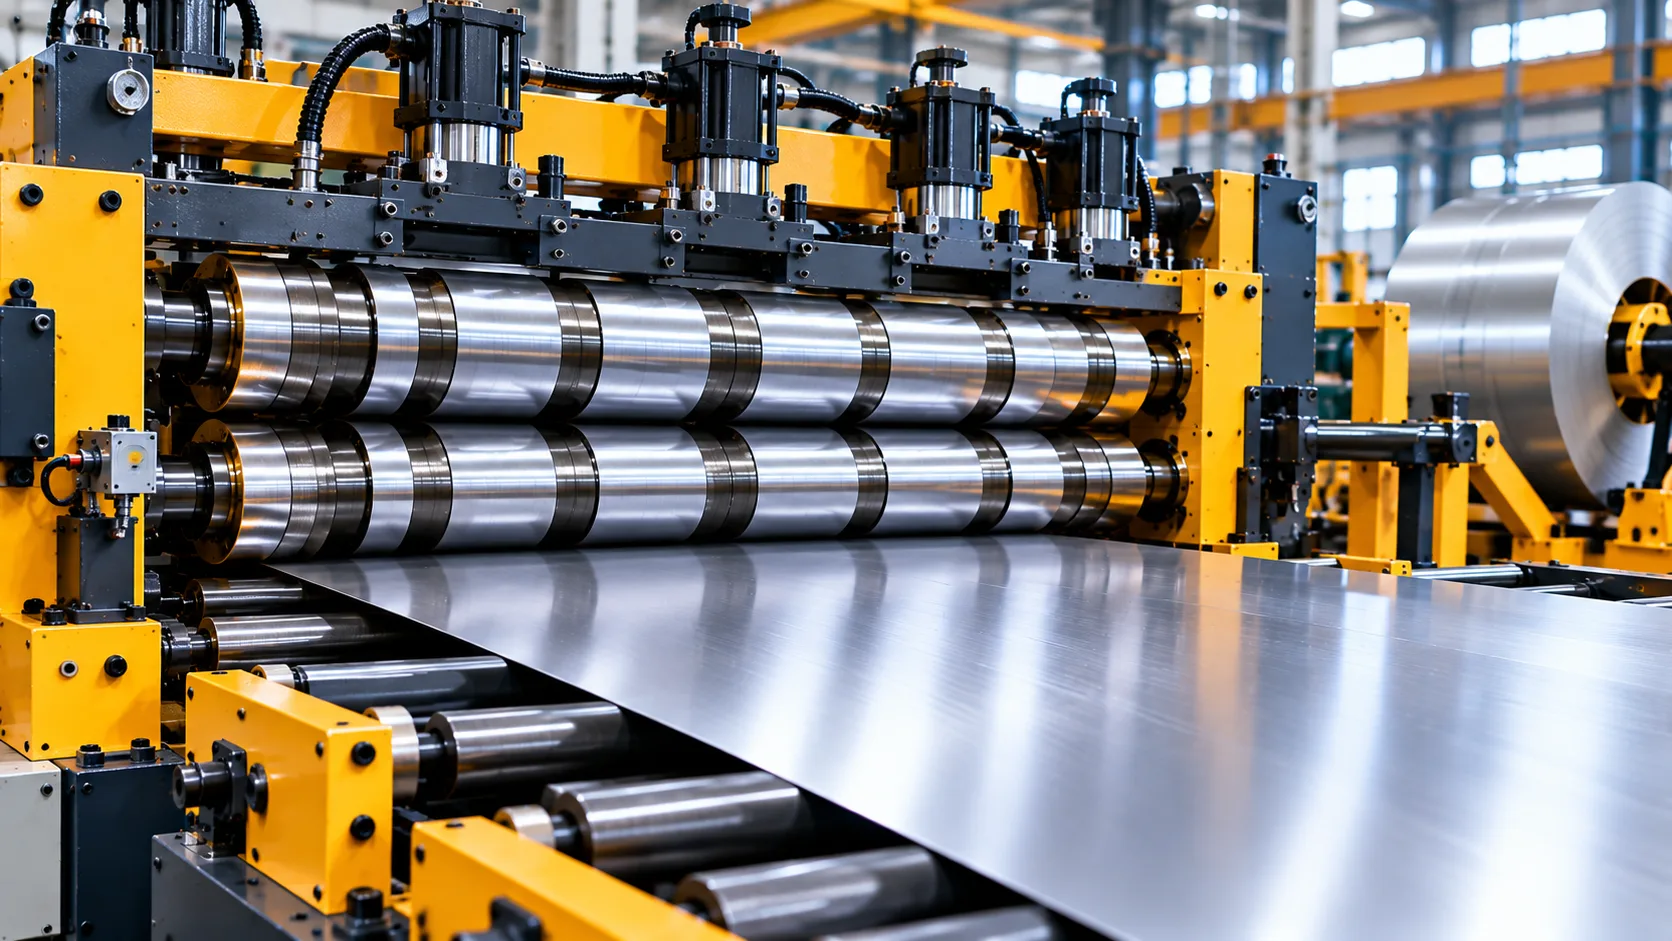
Gauge Classification Matrix
Engineering comparison across standard CTL line configurations
| Parameter / Specification | Light-Gauge Precision Line 0.3 – 3.0 mm range | Medium-Gauge Standard Line Most Popular 1.5 – 8.0 mm range | Heavy-Plate / AHSS Line 4.0 – 25.0 mm range |
|---|---|---|---|
| 1. Dimensional & Material Capacity | |||
| Strip Thickness Capacity | 0.3 mm – 3.0 mm | 1.5 mm – 8.0 mm | 4.0 mm – 25.0 mm |
| Strip Width Range | 600 mm – 1,600 mm | 800 mm – 2,000 mm | 1,000 mm – 2,500 mm |
| Maximum Coil Payload | 15 Metric Tons | 25 Metric Tons | Up to 35 Metric Tons |
| Material Compatibility | Cold-rolled, Aluminum alloys, 2B/BA Stainless steel | Hot-rolled, Pickled & Oiled, Galvanized, Stainless steel | High-strength carbon steel, AHSS, Wear-resistant plate |
| Max Material Yield Strength | ≤ 450 MPa | ≤ 650 MPa | ≤ 1,200 MPa |
| 2. Leveling & Shearing Performance | |||
| Leveler Design & Work Rolls | 6-Hi Cassette / 21 Rolls (Ø40 mm) | 4-Hi or 6-Hi / 19 Rolls (Ø70 mm) | 4-Hi Heavy / 13–15 Rolls (Ø130–180 mm) |
| Maximum Operating Speed | Up to 100 m/min | Up to 80 m/min | Up to 45 m/min |
| Cut Length Range | 300 mm – 4,000 mm | 500 mm – 8,000 mm | 1,000 mm – 16,000 mm |
| Length Cutting Tolerance | ±0.15 mm (at 2,000 mm) | ±0.25 mm (at 3,000 mm) | ±0.50 mm (at 6,000 mm) |
| Diagonal Squareness Tolerance | ±0.25 mm/m | ±0.35 mm/m | ±0.50 mm/m |
| 3. Automation, Power & Line Footprint | |||
| Installed Electrical Power | ~160 kW – 220 kW | ~280 kW – 380 kW | ~450 kW – 650 kW |
| Hydraulic System Pressure | 14 MPa (Proportional) | 16 MPa (Servo-assisted) | 21 MPa (High-flow servo) |
| Automation & PLC Platform | Siemens S7-1500 / Allen-Bradley | Siemens S7-1500F / Allen-Bradley | Siemens S7-1500F Redundant |
| Estimated Line Footprint | 28 m (L) × 7.5 m (W) | 36 m (L) × 9.5 m (W) | 48 m (L) × 12.0 m (W) |
Integrated Upstream & Downstream Options
Tailor material handling ergonomics, strip edge conditioning, and automatic stacking throughput to your facility workflow.
Side Trimmer & Scrap Chopper
Dual rotary side-trimming heads with motorized width setup and heavy-duty dual-rotor scrap choppers for burr-free edges.
- Motorized width positioning
- Integrated scrap chute evacuation
Protective Film Applicator
Synchronized top-and-bottom PVC/PE film lamination with automatic tension brakes and bubble-free pinch roll stations.
- Single or double-sided coating
- Zero-scratch protective feed
Dual-Station Auto Stacker
Air-flotation, vacuum, or electromagnetic stacking beds engineered for non-stop pallet exchange and automated bundle squaring.
- Non-stop continuous stacking
- Scissor lift motorized discharge
Auto Coil Prep & Loading
Heavy-duty coil staging cars, hydraulic de-banders, peeler knives, and automated paper winders to minimize changeover downtime.
- Fast-cycle coil staging
- Optoelectronic strip centering
Need a Non-Standard Coil Capacity or High-Strength Material Configuration?
Share your coil weight, strip width, thickness range, material strength, line speed, and downstream process. Haden application engineers can evaluate a custom cut-to-length configuration for heavy coils, extra-wide strip, high-strength materials, and integration with coil-fed laser cutting systems.
Send your material and production parameters for an application-specific engineering review.
Industrial Applications & Material Capabilities for Cut to Length Lines
Modern metal fabrication requires unyielding geometric flatness, precise dimensional squareness, and complete elimination of internal residual stresses. Haden leveling and cut to length lines are engineered to process high-yield and surface-sensitive metal alloys across diverse manufacturing environments—from high-throughput master coil service centers to tight-tolerance automotive and appliance blanking cells.
Steel Service Centers & Toll Processors
Engineered for continuous multi-shift production processing diverse carbon steel, galvanized, and stainless master coils. Integrated with rapid hydraulic mandrel expansion, automated coil-car positioning, dynamic recipe selection, and automated bundle strapping systems to maximize daily metric tonnage.
Technical Processing Capabilities
- Target Materials: Hot-rolled, cold-rolled, pickled & oiled, galvanized coils
- Throughput Speeds: Continuous line velocity up to 80–100 m/min
- Core Advantage: Rapid sub-5-minute coil changeover and motorized roll-gap setup
Automotive Stamping & Body Panels
Delivers ultra-precise blanks tailored for high-speed progressive dies, transfer presses, and tandem stamping lines. Maintains strict diagonal squareness tolerances within ±0.3 mm while neutralizing trapped inter-laminar stresses across advanced dual-phase (DP) and aluminum structural grades.
Technical Processing Capabilities
- Target Materials: DP600, DP800, DP980, 5000/6000 series aluminum alloys
- Leveling Architecture: 6-high cassette leveler with intermediate anti-fluting rolls
- Core Advantage: Eliminates blank edge curl to prevent stamping die damage
Home Appliances & Precision Metal Fabrication
Configured specifically for scratch-free, mirror-finish stainless and pre-painted steel sheets used in home appliances, refrigerator panels, washing machines, and architectural HVAC cabinetry. Utilizes micro-ground chrome rolls, non-marking vacuum stackers, and synchronous protective film lamination.
Technical Processing Capabilities
- Target Materials: SUS304/430 (2B/BA/No.4), pre-coated VCM/PCM steel
- Surface Safeguards: Air-cushion floatation table and inline top/bottom PVC filmer
- Core Advantage: Zero roll imprint shadows, surface indentation, or edge burrs
Architectural Facades & Metal Curtain Walls
Processes wide-format aluminum, copper, and composite coils up to 2,000 mm in width. Provides thorough internal stress relief to eliminate visual oil-canning, edge waviness, and distortion across large-format exterior cladding cassettes and perforated architectural ceiling tiles.
Technical Processing Capabilities
- Target Materials: AL3003, AL5005, anodized & PVDF-coated coils
- Flatness Compliance: Exceeds ASTM A480, ASTM A568, and EN 10131 flatness standards
- Core Advantage: Uniform cross-width leveling tension across extra-wide sheets
Heavy Machinery & Yellow Goods
Engineered for high-tonnage uncoiling, heavy leveling, and shearing of structural steel plates from 6.0 mm up to 25.0 mm thick. Heavy box-frame levelers with rigid hydraulic backup roll assemblies impart deep plastic deformation to eliminate material memory before thermal cutting.
Technical Processing Capabilities
- Target Materials: Q355B, Q690D, ASTM A572 Grade 50, abrasion-resistant steels
- Shear Configuration: Heavy-duty hydraulic guillotine shear with hydraulic blade gap adjustment
- Core Advantage: Zero thermal distortion or plate lift during processing on sheet metal laser cutting machines and plasma cutters
Electrical Enclosures & Data Center Racks
Delivers highly consistent, dead-flat sheets vital for automated CNC punch presses, robotic panel benders, and laser welding cells. Prevents seam gaps, dimensional distortion, and assembly misalignment in precision modular server cabinets and switchgear enclosures.
Technical Processing Capabilities
- Target Materials: Electro-galvanized (SECC), hot-dip galvanized (SGCC), SPCC, AL5052
- Length & Squareness: Length accuracy within ±0.1 mm; diagonal squareness within ±0.3 mm/m
- Core Advantage: Seamless feeding for lights-out robotic bending and laser welding lines
Eliminating Residual Stresses Across High-Yield & Structural Alloys
When metal coils are wound under tension at the mill, unbalanced internal stress fields become trapped within the cross-section. Without precise alternating elastoplastic reverse bending, subsequent thermal cutting releases these stresses, resulting in severe sheet distortion, edge lifting, and collisions on high-speed laser cutting machines.
Multi-flight back-up roll adjustment eliminates longitudinal coil set, cross-bow, and center buckle.
Guarantees zero plate pop-up during high-speed fiber laser, plasma, or punch cutting.
Haden electro-hydraulic servo leveling systems calculate yield point profiles dynamically, automatically setting roll penetration depths and crowning based on real-time material thickness, width, and alloy yield strength parameters.
Material Processing Compatibility Matrix
Evaluate how Haden leveling and cut to length lines resolve specific metallurgical challenges across primary alloy families.
| Material Grade Group | Gauge Range (mm) | Primary Processing Challenge | Engineered Machine Solution | Downstream Readiness |
|---|---|---|---|---|
| Mild Carbon Steel Q235B, ASTM A36, SPCC, S235JR | 0.5 – 25.0 mm | Coil set, center buckle, mill scale abrasiveness | 4-High heavy-roll leveler with 60 HRC induction-hardened rollers & inline scale wiper | General Stamping & Welding |
| Advanced High-Strength Steel DP600, DP980, Q690D, Strenx | 1.0 – 12.0 mm | High elastic springback, extreme yield resistance | High-torque individual roll drive with compact roll diameters & multi-point hydraulic backup blocks | Automotive Chassis & Cranes |
| Cosmetic Stainless Steel SUS304, SUS316L, SUS430 2B/BA/No.4 | 0.3 – 4.0 mm | Surface scratching, roller shadow marks, work hardening | 6-High intermediate roll design with hard chrome plating & automated inline PVC film applicator | Kitchenware & Architecture |
| Aluminum Alloys AL1060, AL3003, AL5052-H32, AL6061 | 0.4 – 8.0 mm | Low elastic modulus, surface galling, sheet slippage | High-precision rotary shear, air-flotation support conveyors, non-marking vacuum stacker | Curtain Walls & Transport |
| Pre-Painted & Galvanized PPGI, PPGL, HDG DX51D, Galvalume | 0.3 – 2.5 mm | Coating delamination, micro-cracking, zinc pickup | Polyurethane-jacketed pinch rolls and non-contact optical loop tension control system | HVAC & Exterior Enclosures |
Need a Leveling Configuration for Specialized or High-Strength Alloys?
Share your material grade, yield strength, thickness range, strip width, and target flatness. Haden application engineers can evaluate suitable leveling capacity, roll diameter, roll pitch, backup configuration, and machine setup for your material and production requirements.
Cut to Length Line Selection Guide & Technical Investment Framework
Make confident capital equipment decisions by balancing roll mechanics, shearing velocities, and facility dynamics. Along with continuous solutions like coil-fed-laser-cutting-machines, Haden engineers custom coil processing equipment engineered for long-term operational ROI.
Mechanical Selection Criteria & Engineering Trade-Offs
Leveler Roll Diameter & Work Roll Count Matching
Achieving total plastic deformation and residual stress elimination depends on precisely matching work roll diameter and center-to-center pitch to your material's maximum yield strength and gauge spectrum.
- High-strength advanced steels (DP600–DP980, Q550–Q690) require compact roll diameters (40–65 mm) and 19–23 work rolls to generate required reverse-bending force.
- Medium-gauge structural and stainless grades (2.0–8.0 mm) utilize 80–120 mm rolls with 4-high or 6-high cassette configurations to maintain roll parallelism.
- Heavy plate fabrication (6.0–25.0 mm) mandates large-diameter rolls (150–220+ mm) coupled with heavy-duty motorized backup bearings to resist deflection.
- Light-gauge aluminum and pre-painted stock (0.3–1.5 mm) require close roll pitch and intermediate rolls to prevent stripe marks and center buckling.
Shearing Mechanism & Speed Cycle Evaluation
Selecting the ideal cutoff method requires evaluating initial capital cost against continuous line velocity, blade life, and finished edge tolerance.
- Hydraulic Stop-to-Cut Guillotine Shear: Economical entry cost and exceptional cutting force for heavy plate up to 25 mm; relies on a looping pit or feed-stop cycle.
- Servo-Driven Flying Shear: Synchronous tracking cut without strip hesitation; accelerates output for light-to-medium gauges while safeguarding strip surface integrity.
- High-Speed Rotary Drum Shear: Continuous rotary motion delivering up to 100 m/min continuous throughput; zero stop marks, making it essential for mirror stainless and automotive outer panels.
Automated Sheet Stacking & Material Handling Systems
Stacking configurations must match continuous processing throughput while preventing cosmetic scratches, corner burrs, or bundle misalignment.
- Drop-Style Air Cushion & Flapper Stackers: Cost-effective and durable for standard hot-rolled and structural sheet fabrication with side tamping arms.
- Automated Vacuum or Magnetic Crane Stackers: Non-contact sheet handling ideal for polished aluminum, brass, galvanized, and stainless steel sheets.
- Continuous Dual-Station Turnstile Stackers: Enable non-stop production during full bundle discharge and automatic pallet replacement for high-tonnage service centers.
Facility Engineering, Infrastructure & Footprint Planning
Foundation, Looping Pit, & Electrical Load Calculation
Proper site preparation ensures equipment longevity, vibration isolation, and efficient coil transport logistics before commissioning.
- Looping Pit Dimensions: Depth of 1.5–3.5 meters planned according to line acceleration rates, strip thickness, and buffer volume requirements.
- Overhead Crane Capacity: Minimum 15–35 ton crane rating with coil lifters to support continuous master coil replenishment and staging.
- Reinforced Foundation Slabs: 400–600 mm isolated concrete slab with dynamic load ratings of 30–60 kN/m² to support heavy leveler clamping pressures.
- Connected Electrical Load: Plan for 120–350 kW depending on leveler drive power, hydraulic pump stations, and high-frequency servo feeder capacities.
- Pneumatics & Hydraulics: Centralized hydraulic power units operating at 210–280 bar with continuous fluid cooling and filtered pneumatic feeds.
Rapid Tooling Setup & Automated Recipe Management
Haden cut to length lines utilize centralized CNC recipe storage, allowing operators to execute fast parameter recall across varying coil batches.
- Master Coil Changeover: 12–20 minutes via hydraulic loading cars, auto-centering mandrels, and motorized coil peeler tables.
- Leveler Roll Gap Adjustment: Motorized wedge adjustment completes multi-axis positioning in under 60 seconds with digital readout feedback.
- Sheet Length Adjustment: Instantaneous length preset from HMI touchscreens with closed-loop optical encoder verification.
- Comprehensive Recipe Loading: Instant parameter configuration for yield strength, roll bend crown, back-tension, and stacking programs.
Factory Automation & MES Industry 4.0 Integration
Engineered with open architecture communication protocols, our CTL lines connect seamlessly with upstream logistics, downstream packaging, and automated laser-cutting-machines.
- In-Line Surface Protection: Automated protective film applicators (PE/PVC) and paper interleave decoilers integrated prior to leveling.
- Edge Trimming & Scrap Balling: Integrated rotary side trimmers with dual-spindle scrap choppers for exact strip width sizing.
- Smart MES Communication: OPC UA, PROFINET, and Ethernet/IP protocols support real-time OEE reporting and coil batch tracking.
- Predictive Remote Diagnostics: Built-in IIoT modules for cloud-based monitoring of bearing temperatures, vibration, and hydraulic status.
Key Operational Benchmarks & Tolerances
Gauge Capability
From sensitive aluminum to high-tensile plate
Max Line Velocity
Continuous rotary drum & flying shear throughput
Length Accuracy
High-resolution closed-loop servo feed system
Diagonal Squareness
Zero edge camber for downstream sheet-metal-laser-cutting-machines
Cut to Length Line Investment Planning Checklist
Define Baseline Coil Specifications & Material Spectrum
Quantify maximum coil outer diameter, inner bore (508/610 mm), strip width, maximum tonnages, and yield strength limits (N/mm²).
Analyze Surface Sensitivity & Cosmetic Finish Requirements
Determine whether intermediate 6-high rolls, polyurethane-coated feed rolls, or non-contact vacuum stackers are required for sensitive alloys.
Audit Plant Layout, Crane Clearances, and Pit Feasibility
Review available bay length (35–90 m), hook height clearances, underground utility locations, and foundation soil bearing capacities.
Balance Shearing Method Against Throughput & Capital Budget
Compare stop-shear, servo flying shear, and rotary drum systems to identify the optimal balance of upfront cost and production capacity.
Identify In-Line Processing & Downstream Packaging Needs
Evaluate requirements for edge trimming, protective film lamination, automatic sheet weighing, strapping, and bundle wrapping integration.
Verify Lifecycle Support, Spare Roll Cassettes & Service SLA
Ensure quick availability of replacement backup bearings, precision-ground rolls, and dedicated field engineering support from Haden.
Standard Haden CTL Line Configurations Matrix
| Line Configuration | Thickness Range | Max Line Speed | Target Industrial Applications |
|---|---|---|---|
| Light-Gauge High-Speed Line | 0.3–3.0 mm | 80–100 m/min | Appliance white goods, electronics, architectural cladding, pre-painted coils |
| Medium-Gauge Precision Line | 2.0–8.0 mm | 40–60 m/min | Automotive chassis components, laser-cutting blanks, steel service centers |
| Heavy-Duty Plate CTL Line | 6.0–25.0 mm | 20–40 m/min | Heavy machinery, shipbuilding, structural steel, bridge & container fabrication |
| Rotary / Flying Shear Continuous Line | 0.8–6.0 mm | 60–100 m/min | Mirror-finish stainless steel, aerospace aluminum, high-output blanking centers |
Request a Tailored Line Layout & Project Cost Evaluation
Share your coil specifications, production targets, and available workshop space. Haden application engineers can evaluate a suitable cut-to-length line configuration, equipment layout, production workflow, and budgetary quotation based on your project requirements.
Key Specifications for Custom Line Evaluation
Providing these parameters helps our engineering team recommend a more application-specific line configuration.
Frequently Asked Questions About Leveling and Cut-to-Length Lines
Review technical guidelines, operational specifications, and capital procurement criteria for high-capacity coil processing lines. Whether you are upgrading an existing sheet leveling line or configuring a new high-speed cut-to-length installation, our engineering team addresses critical performance, metallurgy, and integration questions below.
How do I select between 4-High and 6-High precision leveler configurations?
Choosing between a 4-High and a 6-High precision leveler depends on raw material thickness, tensile strength, and critical surface finish requirements:
- 4-High Levelers: Built with work rolls supported directly by adjustable back-up roller flights. This delivers maximum mechanical rigidity, making it the industry standard for medium-to-heavy gauge carbon steels, structural plate, and hot-rolled coils where slight back-up roll witness lines are acceptable.
- 6-High Levelers: Feature an intermediate roll bank positioned between the slender work rolls and the back-up flights. This intermediate layer eliminates shadow marks, roll pickup, and localized deflection. It is indispensable for surface-critical materials such as mirror-finish stainless steel, automotive Class-A exposed panels, bright aluminum alloys, and prepainted coils.
Haden also designs quick-change roll cassette systems, allowing toll processors to alternate between dedicated 4-High and 6-High cassettes within 15 minutes on the same production line.
How does the line eliminate residual stress and prevent warping in high-strength steels?
Processing advanced high-strength steels (AHSS, Domex, Q550, Q690) requires deep plastic deformation to neutralize locked-in coil tension that causes thermal springback during fabrication on laser cutting machines:
- Controlled Elastic-Plastic Alternating Bending: The entry work rolls subject the incoming strip to 75%–85% plastic deformation, eliminating internal stress memory across the material fibers. Subsequent rolls gradually reduce intermesh depth toward zero at the exit, leaving the sheet completely stable.
- Closed-Loop Hydraulic Back-Up Crowning: Multi-station motorized hydraulic flight wedges independently adjust individual work roll segments across the full web width, correcting center buckles and edge waves.
- Prestressed Cast-Steel Frame Rigidity: Extra-rigid housings and oversized alloy roll journals counteract extreme separating forces, ensuring zero frame deflection during continuous high-tensile leveling.
What is the typical changeover time for different strip thicknesses, widths, and lengths?
Haden cut-to-length lines feature automated recipe recall and motorized positioning systems to minimize changeover downtime:
- Automated CNC Recipe Recall (< 1 Minute): Material parameters (strip thickness, yield strength, target length, roll intermesh, and side guide positions) load directly from the touchscreen database.
- Hydraulic Coil Staging & Threading (3 to 5 Minutes): Dual-speed hydraulic coil loading cars with laser auto-centering, motorized uncoiler mandrel expansion, and hydraulic peeler tables feed new coils without overhead crane delays.
- Motorized Stacker Pocket Setup (< 2 Minutes): Automated drop stackers, side tampers, and magnetic or vacuum overhead arms adjust along servo-driven linear rails to match the target blank size.
Total typical line changeover between master coils is completed in 4 to 7 minutes, maximizing overall equipment effectiveness (OEE) for high-mix service centers.
What are the standard equipment lead times, FAT protocols, and on-site commissioning procedures?
We maintain rigorous project milestone tracking, full-scale factory verification, and structured on-site commissioning:
- Manufacturing Lead Time: Standard configuration lines ship in 14 to 18 weeks; custom heavy-duty plate lines and high-speed rotary shear lines require 20 to 26 weeks.
- Factory Acceptance Testing (FAT): Prior to shipping, the entire line is mechanically assembled, dry-cycled, and tested under load using client-supplied coil samples to verify leveling accuracy, cut length tolerances, and diagonal squareness.
- On-Site Installation & Commissioning: Haden field service engineers oversee foundation setting, precision laser alignment, hydraulic flushing, electrical tie-ins, and operator training during an efficient 10 to 18 business day commissioning window.
Can Haden cut-to-length lines integrate with plant MES, automated packaging, and robotic cells?
Yes. All Haden systems utilize open-architecture automation built for complete Industry 4.0 factory integration:
- MES & ERP Connectivity: Standard industrial Ethernet interfaces (OPC-UA, PROFINET, Modbus-TCP) provide live production tracking, scrap logging, automated job dispatching, and remote diagnostics.
- Automated Packaging Line Handshake: Direct signal and physical integration with automatic strapping machines, paper/protective film applicators, VCI sheet dispensers, and motorized pallet turntables.
- Downstream Blanking & Storage Links: Exit runout conveyors can link directly to automated storage and retrieval systems (ASRS), integrated sheet metal laser cutting machines, or robotic destacking cells.
What technical parameters drive cut-to-length line pricing and capital investment?
Total equipment investment is governed by four primary engineering and production capacity criteria:
- Material Thickness & Coil Width: Heavy plate lines (up to 25 mm) require reinforced machine housings and high-tonnage hydraulics, while light gauge systems (0.3–3.0 mm) focus on high-precision roll geometries.
- Shear Type & Line Speed: Start-stop hydraulic guillotine shears provide a cost-effective solution for standard volumes. Servo flying shears and continuous rotary shears command higher investment but eliminate surface marking and double continuous throughput.
- Leveler Precision Level: 6-High configurations with motorized hydraulic roll cassettes cost more than baseline 4-High units but are required for scratch-sensitive and high-tensile alloys.
- Stacking Automation: Manual or pneumatic drop tables represent the base tier, whereas non-marking electromagnetic and vacuum gantry stackers deliver high-speed, unmanned blank handling.
Need a Custom Parameter Evaluation?
Our line architects evaluate your material yield curves, strip widths, daily throughput targets, and workshop layout to engineer a high-yield, cost-effective coil processing line.
Standard Precision Benchmarks
Leveling Precision Troubleshooting & Defect Correction Guide
Delivering laser-flat, stress-relieved sheet metal requires understanding incoming coil shape defects and applying targeted mechanical roll forces. Use this reference matrix to identify strip shape irregularities and apply corrective adjustments during coil processing.
| Coil Defect Condition | Underlying Stress Cause | Leveler Mechanical Adjustment | Downstream Production Impact |
|---|---|---|---|
| Coil Set (Longitudinal Curvature) | Differential fiber length between upper and lower strip surfaces induced during tight coil winding and cooling. | Increase entry work roll intermesh to force deeper plastic bending; set exit work roll gap to exact material gauge. | Prevents feed jams in punch presses and progressive stamping dies. |
| Cross Bow (Transverse Curvature) | Transverse internal stresses created by uneven cooling or cold reduction rolling in the master coil. | Adjust intermediate roll tilt or raise center back-up roll flights to reverse lateral crown stress. | Guarantees precise root gap alignment for automated seam welding. |
| Edge Waves (One or Both Edges) | Strip edges are longer than the center cross-section due to uneven rolling mill draft across the strip width. | Apply positive center back-up roll crowning to extend center fibers until they match the elongated edge fibers. | Eliminates visible oil canning on architectural facade panels. |
| Center Buckle (Oil Canning / Pockets) | The center fibers of the strip are longer than the outer edge fibers across the transverse plane. | Depress the outer back-up roll flights to stretch the edge fibers, balancing length across the full sheet width. | Prevents cutting head collision issues on automated coil-fed laser cutting machines caused by sheet thermal uplift. |
Configure Your Cut-to-Length Line & Request a Project Proposal
Share your coil specifications, production targets, and application requirements. Haden application engineers can evaluate a suitable leveling, feeding, shearing, stacking, and automation configuration for your coil processing project.
What Our Engineering Team Can Review
Material & Capacity Evaluation
Review material grade, yield strength, thickness, coil width, coil weight, and target production output.
Line Configuration & Layout
Evaluate uncoiling, leveling, servo feeding, shearing, stacking, material flow, and available workshop space.
Production Workflow Integration
Review integration with downstream cutting, forming, material handling, and automated production processes.
Discuss Your CTL Project
Planning a new coil processing line or upgrading an existing system? Share your production requirements with our application team for a configuration review.
Contact Application EngineersRequest Line Configuration & Quotation
Provide your key coil and production parameters for an application-specific cut-to-length line recommendation.