
Coil-Fed Laser Cutting Machines for Continuous Sheet Metal Blanking
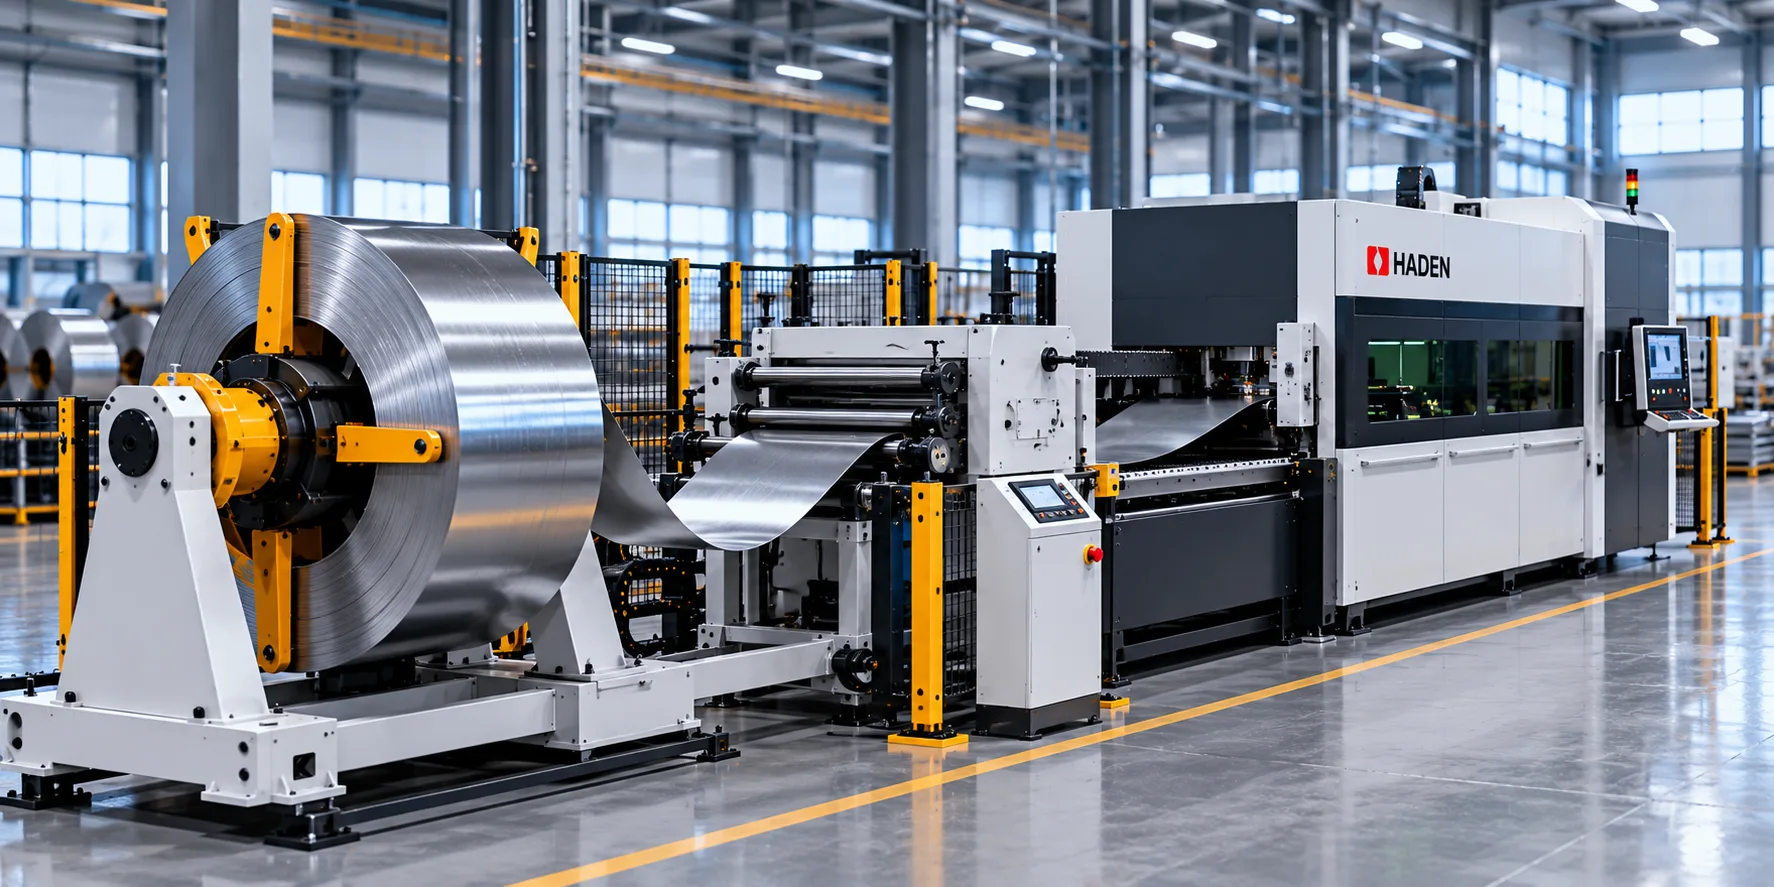
Integrate coil uncoiling, precision leveling, fiber laser cutting, and automated material handling into a continuous production line. Haden coil-fed laser cutting systems support flexible blank geometries and help streamline high-volume sheet metal processing.
Integrated uncoiling and leveling
Flexible cutting from digital part files
Configurable blank sorting and stacking
Applications: Automotive blanks · HVAC components · Appliance panels · Electrical enclosures · Industrial sheet metal fabrication
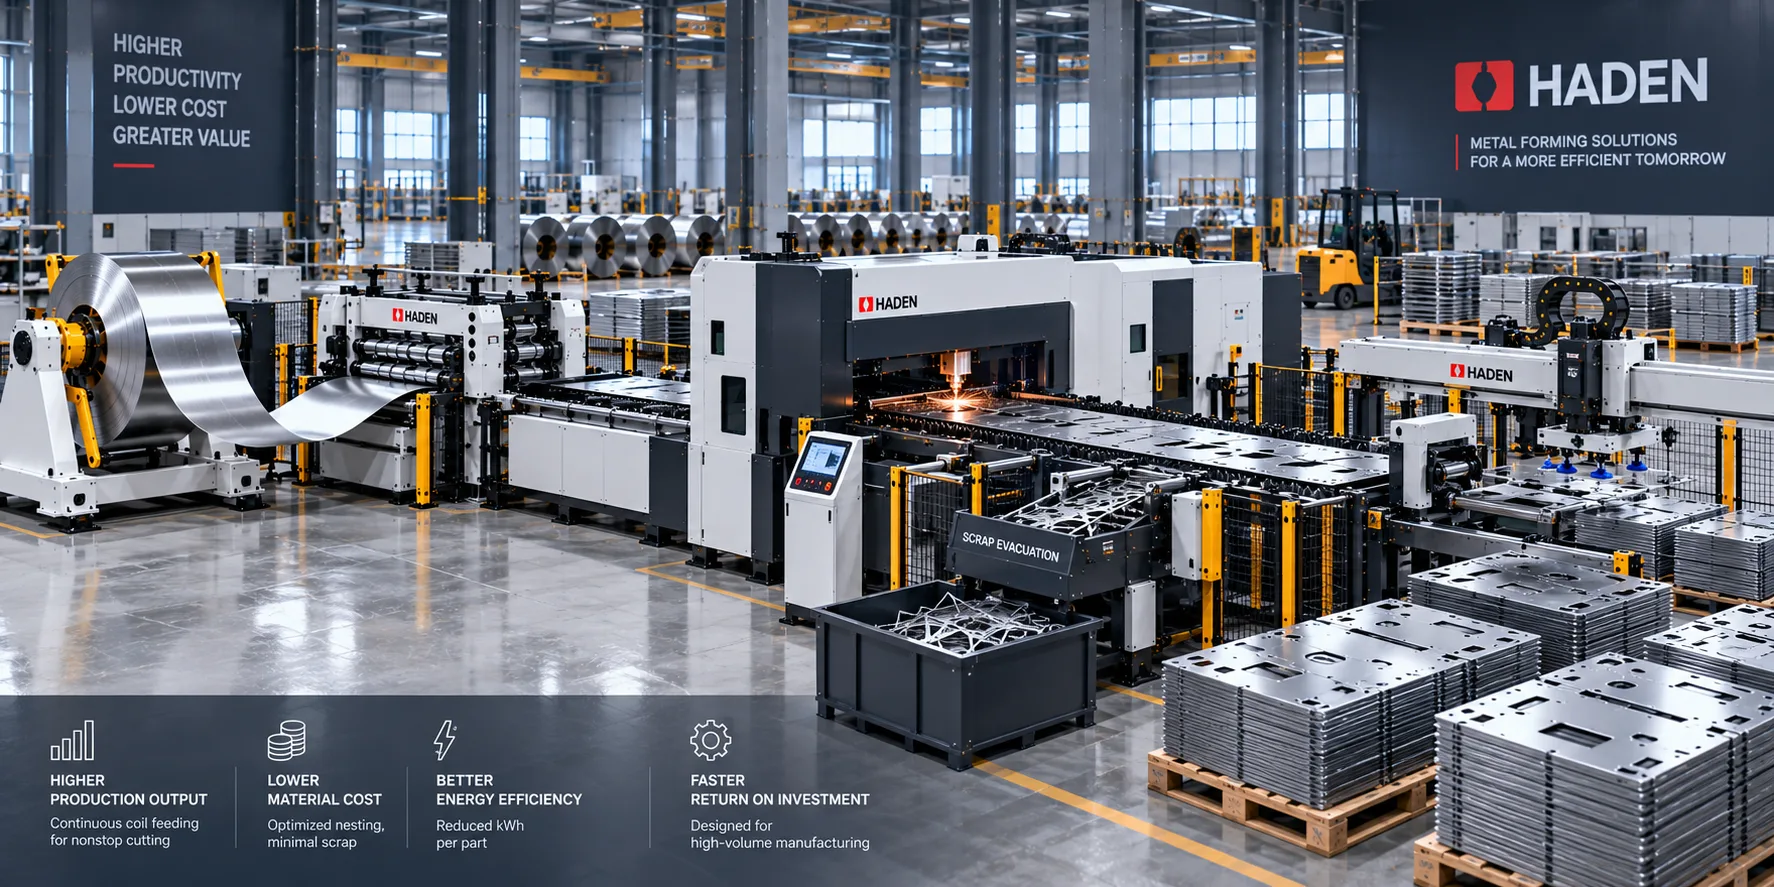
Fully Automated Integrated Coil Laser Cutting Production Line Workflow
High-throughput industrial stamping and sheet metal fabrication demand continuous material flow without the throughput bottlenecks of discrete flat-sheet loading. Expanding beyond conventional laser cutting machines, the Haden uncoiling leveling laser cutting system unifies raw master coil decoiling, multi-roller internal stress relief, high-speed dynamic continuous cutting, and automated blank sorting into a synchronized, closed-loop CNC production line. By transforming coiled steel into precision-cut parts in a single non-stop sequence, manufacturers bypass pre-blanking shear lines, cut scrap rates, and minimize material handling footprint.
Heavy-Duty Hydraulic Uncoiling
Dual-wedge hydraulic expansion mandrels securely handle 5 to 20 metric ton coils, paired with automated coil car staging and optical strip edge-centering.
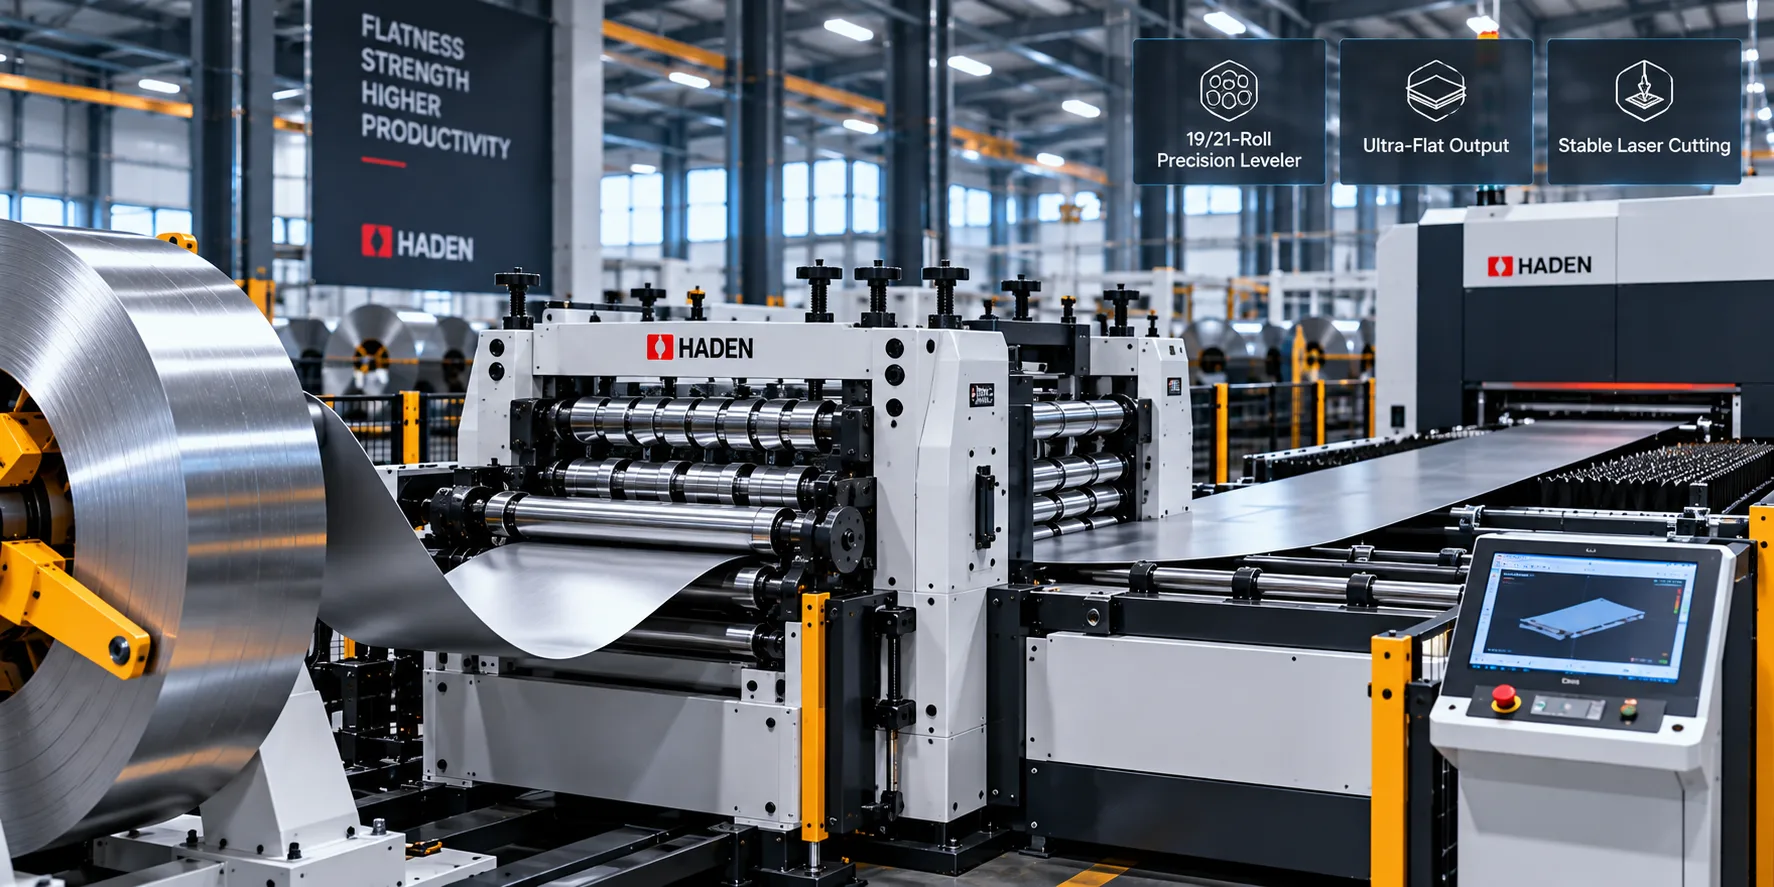
High-Precision Roller Leveling
Four-high, multi-roll precision straighteners eliminate coil set, coil cross-bow, and residual internal stress to secure true zero-gap laser focal consistency.
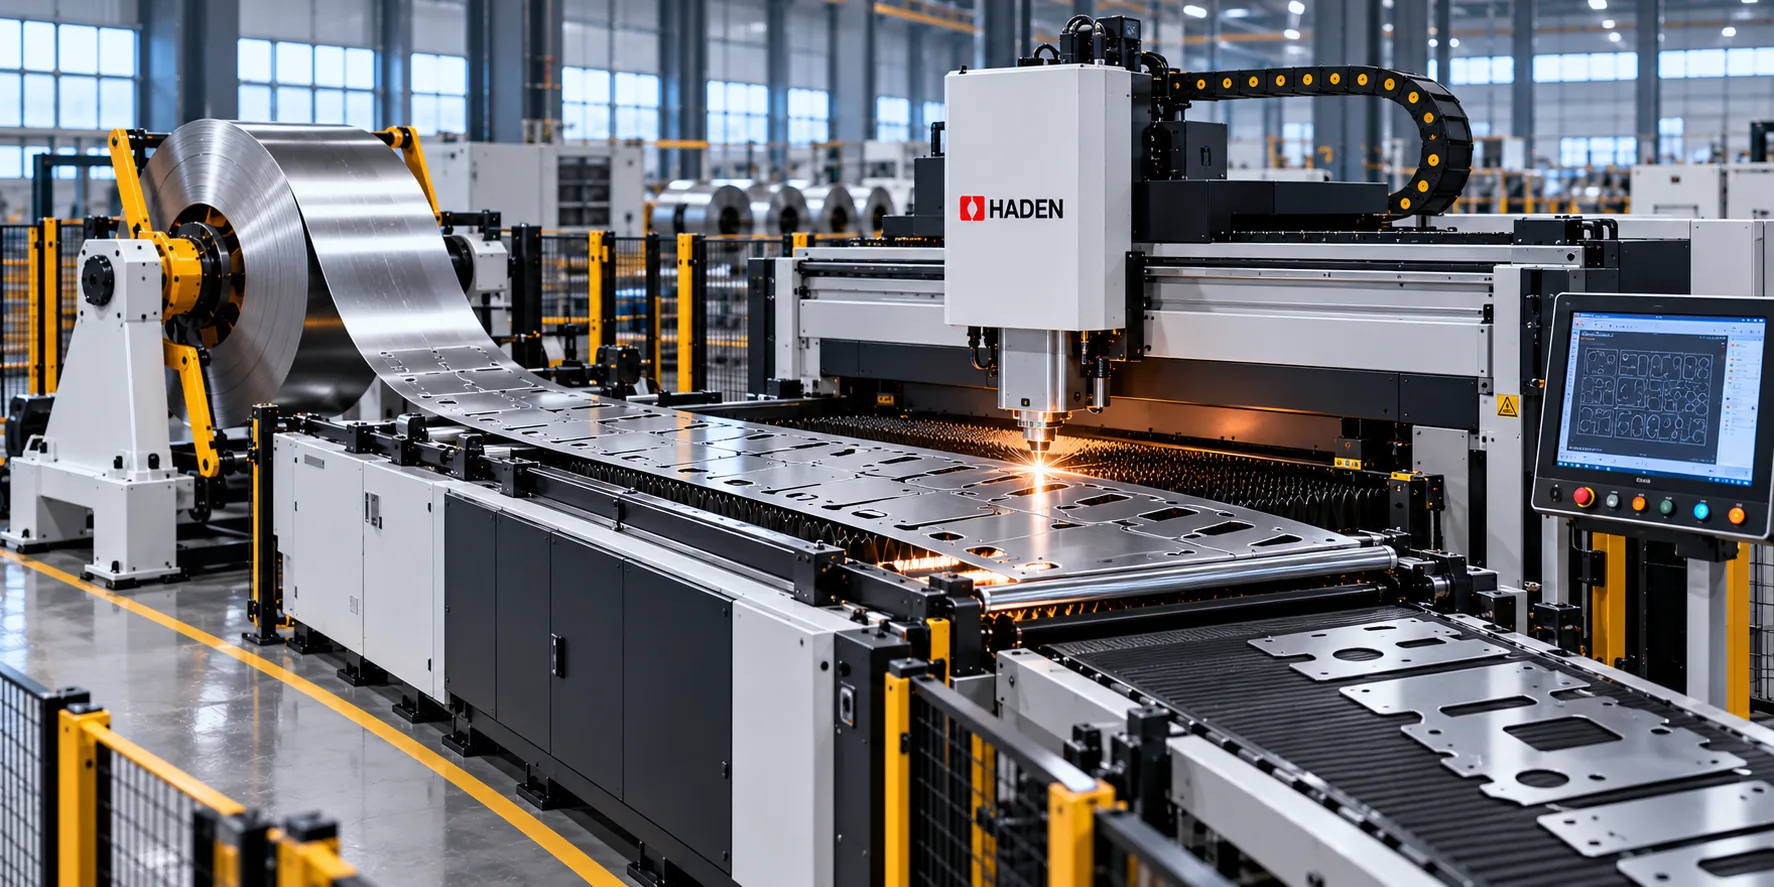
Continuous Dynamic Laser Cutting
Synchronized linear-motor gantries and traveling slat beds execute continuous dynamic cutting, fly-cutting, and common-line nesting across continuous strip runs.
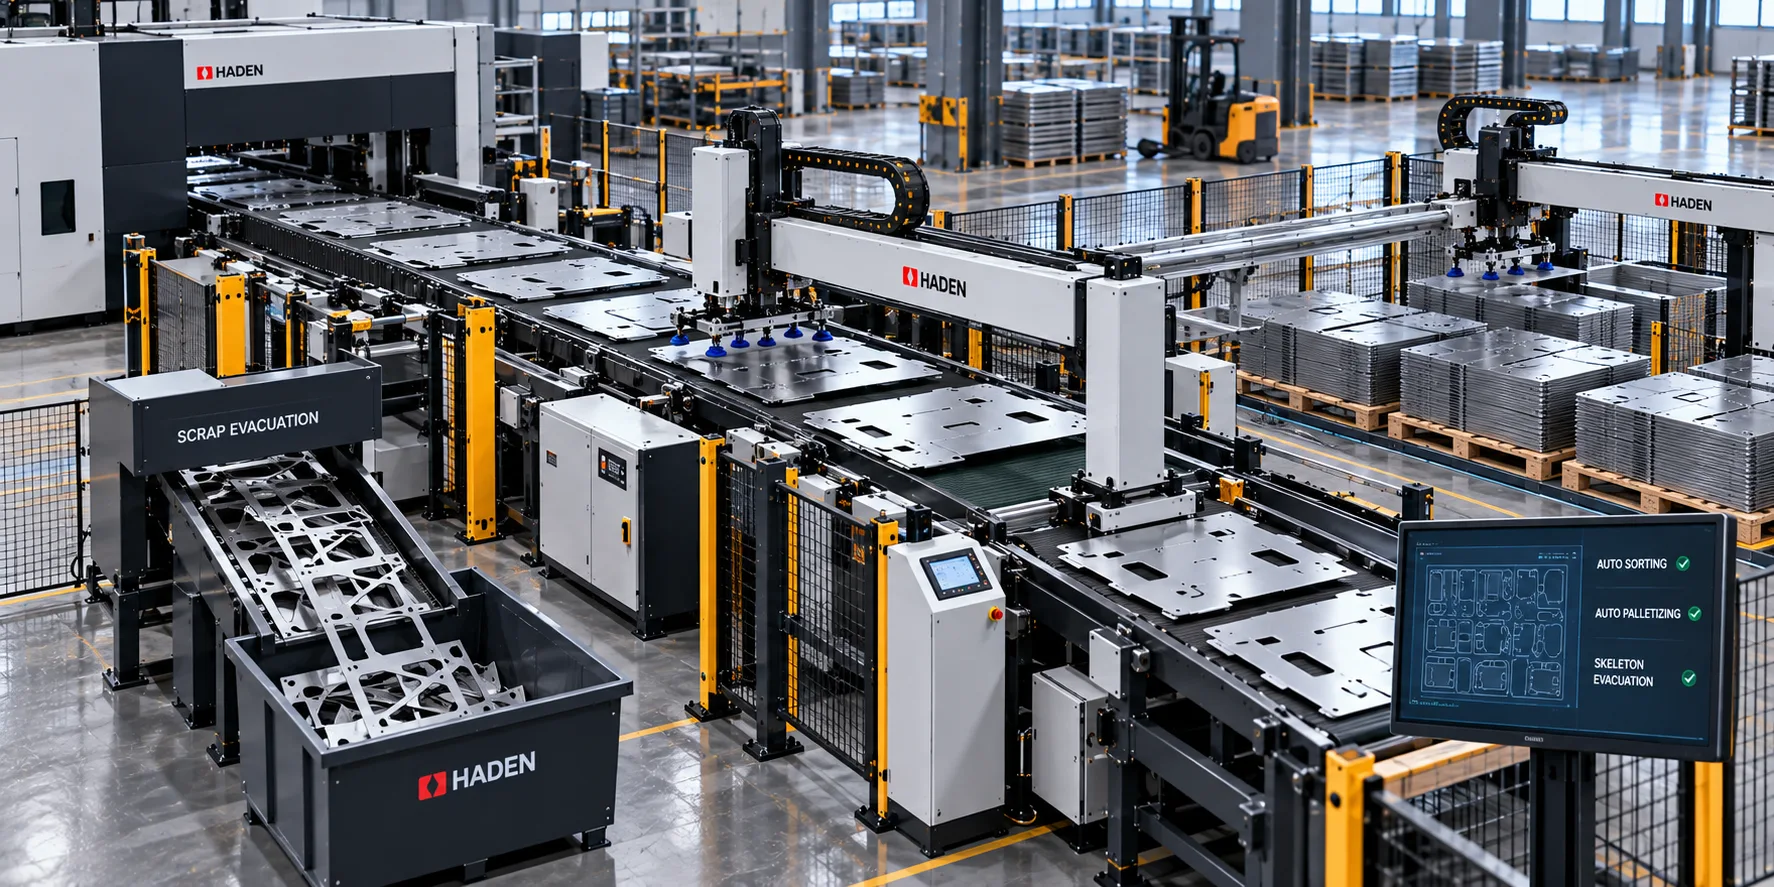
Automated Sorting & Stacking
Robotic vacuum gantries, vision-guided sorting conveyors, and scrap segment choppers automatically palletize finished blanks and evacuate metal skeletal scrap.
Automated Coil Feeding with Precision Photoelectric Centering
The automated coil feeding phase establishes uninterrupted strip flow for the entire downstream blanking cell. Heavy-duty hydraulic loading cars transfer coils directly onto dual-cone or cantilevered expanding mandrels, maintaining steady back-tension across carbon steel, stainless steel, galvanized sheet, and aluminum alloys.
- Hydraulic Hold-Down Arm & Snubber: Prevents violent outer-wrap expansion during coil banding release and strip lead-in.
- Motorized Peeler Blade & Pinch Rolls: Delivers hands-free strip threading directly into the primary leveling assembly.
- Regenerative Servo Tension Control: Eliminates strip sagging, chatter, and surface scratching under high-speed feed cycles.
Haden Centralized Closed-Loop Line Control
Every module in the Haden coil-fed laser cutting line is integrated via a high-speed industrial EtherCAT communications bus. This delivers microsecond-level synchronization among decoiler back-tension, leveler roll positioning, dynamic continuous laser cutting interpolation, and outfeed sorting.
Endless Strip Nesting Engine
Industrial nesting software compiles continuous strip cutting programs, interlocking components past conventional sheet length limits to reach 92% to 96% raw material utilization.
Dynamic Feed Synchronizer
Real-time optical sensors and high-resolution servo encoders dynamically modulate leveling roll gaps and feed rates according to real-time strip thickness and coil diameter changes.
Rapid Coil Changeover Staging
Motorized dual-station loading cars prep the subsequent master coil while cutting continues on the active strip, shrinking end-to-end setup and changeover windows to under 8 minutes.
MES / ERP Factory Integration
Built-in OPC-UA and industrial Ethernet protocols export live production volume, material yield statistics, and preventative maintenance diagnostics straight to plant execution software.
Coil vs. Sheet Laser Cutting: Material Utilization & Cost Reduction
Transitioning from standard pre-cut sheet metal to an automated coil-fed laser blanking line delivers decisive operational and financial gains for high-throughput manufacturing. By unifying heavy-duty uncoiling, precision multi-roller leveling, and high-speed CNC laser cutting machines into a single automated process, fabricators eliminate standalone shearing operations, minimize scrap margins, and dramatically accelerate capital payback timelines.
Endless Boundary Common-Line Nesting
Conventional flatbed sheet metal laser cutting machines are constrained by fixed sheet lengths (such as 3,000 mm or 4,000 mm), generating recurring skeleton waste at every perimeter. Haden continuous coil laser blanking lines operate along an uninterrupted X-axis, enabling tight part interlocking and head-to-tail common-line nesting across continuous strip lengths.
- 90% to 96% material utilization efficiency
- Eliminates leading and trailing end-of-sheet drops
- Dynamic nesting across irregular part geometries
Elimination of Intermediate Shearing Lines
Feeding raw coils directly into the laser cell bypasses standalone cut-to-length shearing lines, secondary crane transport, and staging storage buffers. By integrating de-coiling, level-flattening, dynamic laser cutting, and parts sorting into one automated production footprint, shop floor space requirements drop by more than 40%.
- Zero secondary handling damage or transfer labor
- Purchasing advantage through raw master coil procurement
- Consolidated footprint with streamlined work-in-progress flow
Tooling-Free Flexible Blanking
Mechanical stamping lines demand dedicated hard dies that require weeks of tooling lead times and thousands of dollars in fabrication and sharpening costs. Haden coil-fed fiber laser cutting systems execute design revisions directly from CAD/CAM nesting files, enabling instantaneous program changeovers without tooling depreciation.
- Zero die tooling costs and zero die storage requirements
- Instant changeover between varied part runs and geometries
- Elimination of massive pre-stamped inventory holding costs
Interactive Material Savings & ROI Simulator
Quantify the annual cost reductions and capital payback timeline achieved by converting raw coil stock directly into finished laser-cut blanks versus standard pre-cut sheet processing.
Engineered for High-Volume Production and Accelerated ROI
For automotive tier-one suppliers, HVAC ducting fabricators, and contract metal forming facilities utilizing high-precision press brakes, raw material purchasing represents 60% to 75% of total manufacturing cost. Haden coil-fed laser cutting machines transform shop-floor economics by feeding continuous metal coils directly through dynamic optical cutting heads, bypassing pre-cut sheets and repetitive material loading cycles.
Intelligent nesting algorithms synchronize with heavy-duty roller levelers to maintain precise focal consistency across carbon steel, stainless steel, and aluminum coils. By removing geometric boundary constraints and supporting nonstop continuous cutting, Haden lines minimize skeleton scrap, reduce kilowatt-hour consumption per part, and sustain high output across three-shift industrial operations.
| Evaluation Metric | Standard Pre-Cut Sheet Laser Cutting | Haden Coil-Fed Laser Blanking Line |
|---|---|---|
| Average Scrap Margin | 15% – 25% (Edge clamping margins & end drop-offs) | 4% – 8% (Continuous boundaryless nesting) |
| Pre-Processing Requirements | Requires separate cut-to-length shearing lines | Zero; Direct decoiler-to-cutting head feed |
| Raw Material Purchase Cost | Higher premium per ton for packaged sheet blanks | Lower raw master coil commodity pricing |
| Material Loading Downtime | Pallet shuttle exchange cycle required every sheet (60–90s) | Non-stop uncoiling feeding for continuous hours |
| Floor Space & Staging Footprint | Extensive multi-bay sheet pallet racks and forklifts | High-density coil staging and integrated line footprint |
Coil-Fed Fiber Laser Cutter Series & Technical Specifications
Discover the high-efficiency lineup of Haden coil-fed laser cutting machines and turnkey blanking lines. By integrating automated hydraulic decoiling, high-precision roll leveling, dynamic continuous fiber laser cutting, and synchronized parts sorting into a single continuous workflow, these production lines eliminate sheet pre-cutting and drastically reduce scrap. Compare our standard, dual-head, and heavy-duty models to match your coil width, material thickness, and production throughput targets.
Standard Single-Head Continuous Laser Blanking Line
Engineered for rapid precision blanking in HVAC duct manufacturing, electrical enclosure fabrication, and commercial appliance production. Unlike traditional standalone sheet metal laser cutting machines, this compact line pairs high-speed dynamic acceleration with synchronized uncoiling and precision leveling, processing coil widths up to 1,500 mm with exceptional edge squareness and zero material distortion.
Core Advantage: Bypasses independent sheet shearing machines, enabling continuous coil nesting that boosts raw material utilization up to 94% across standard multi-shift operations.
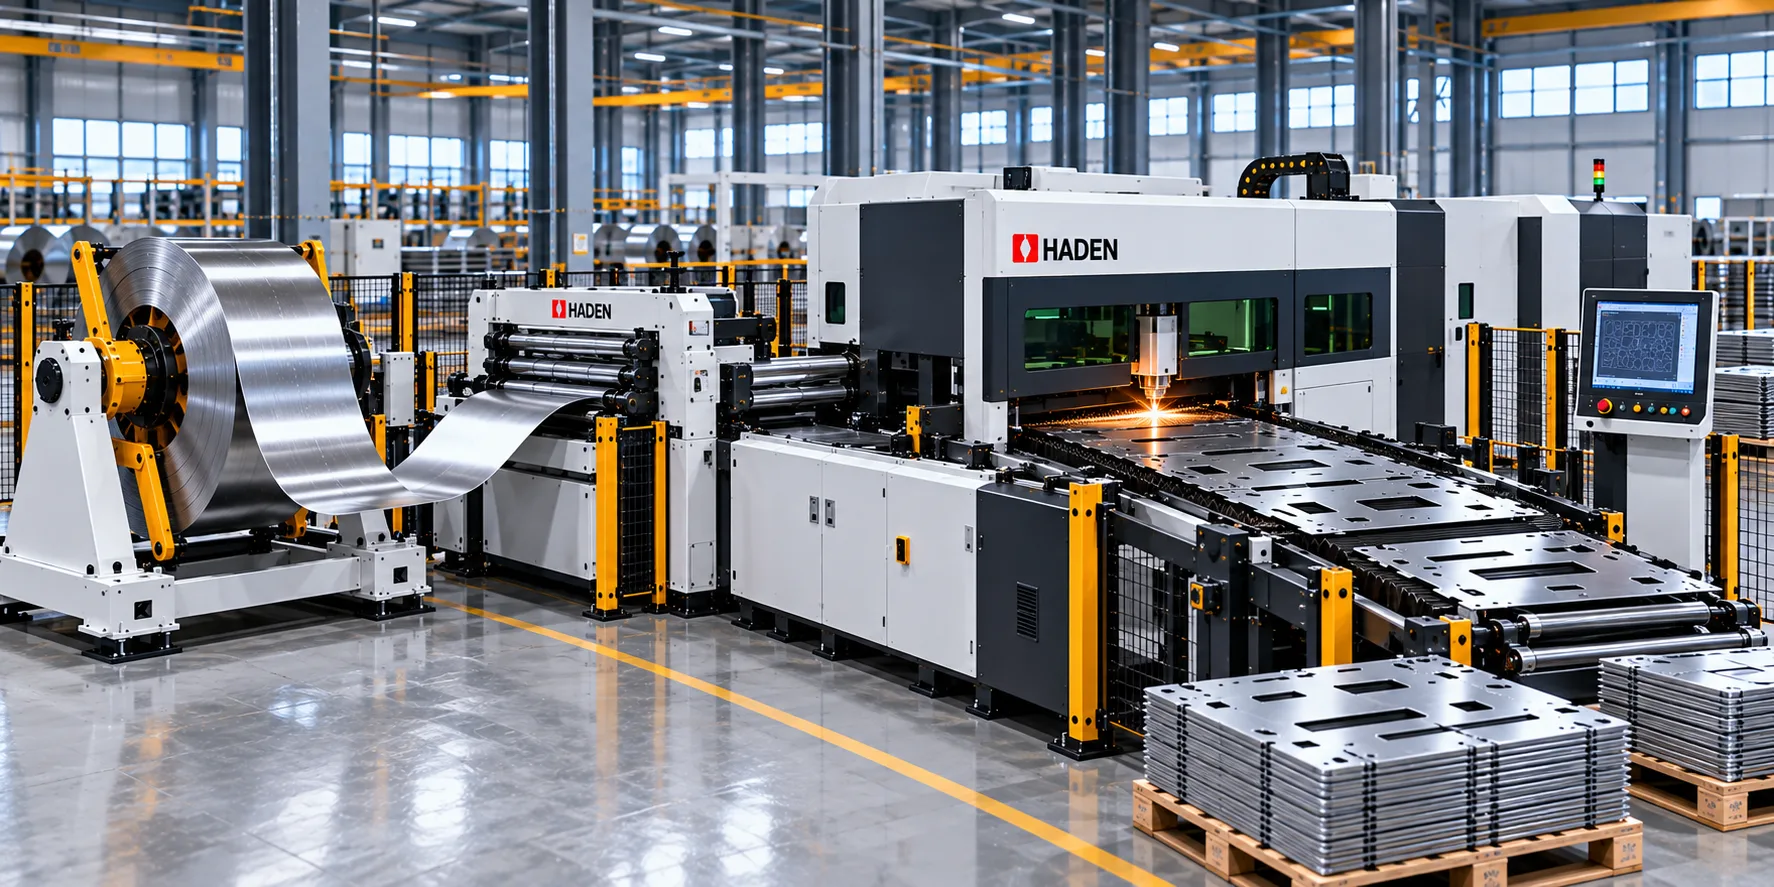
19-Roll Precision Leveler
Eliminates coil set and internal residual stress for optimal focal consistency.
Dynamic Cutting Head
Auto-focus fiber laser head with real-time dynamic obstacle avoidance.
Hydraulic Decoiler
Heavy-duty expandable mandrel supporting up to 10-ton master coils.
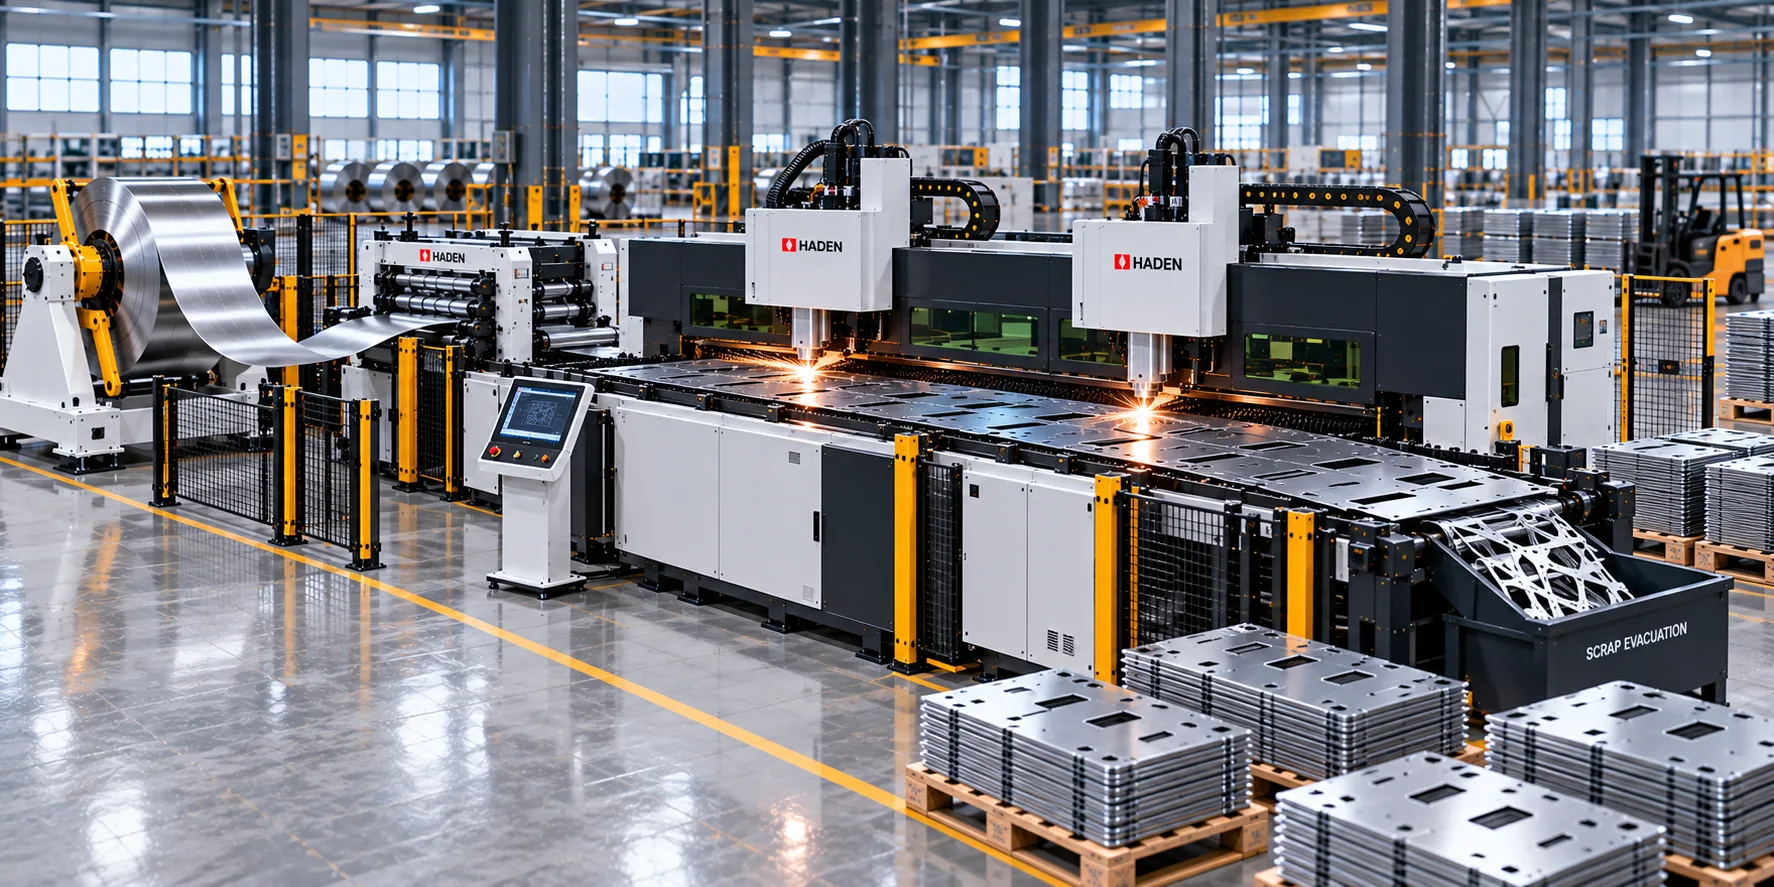
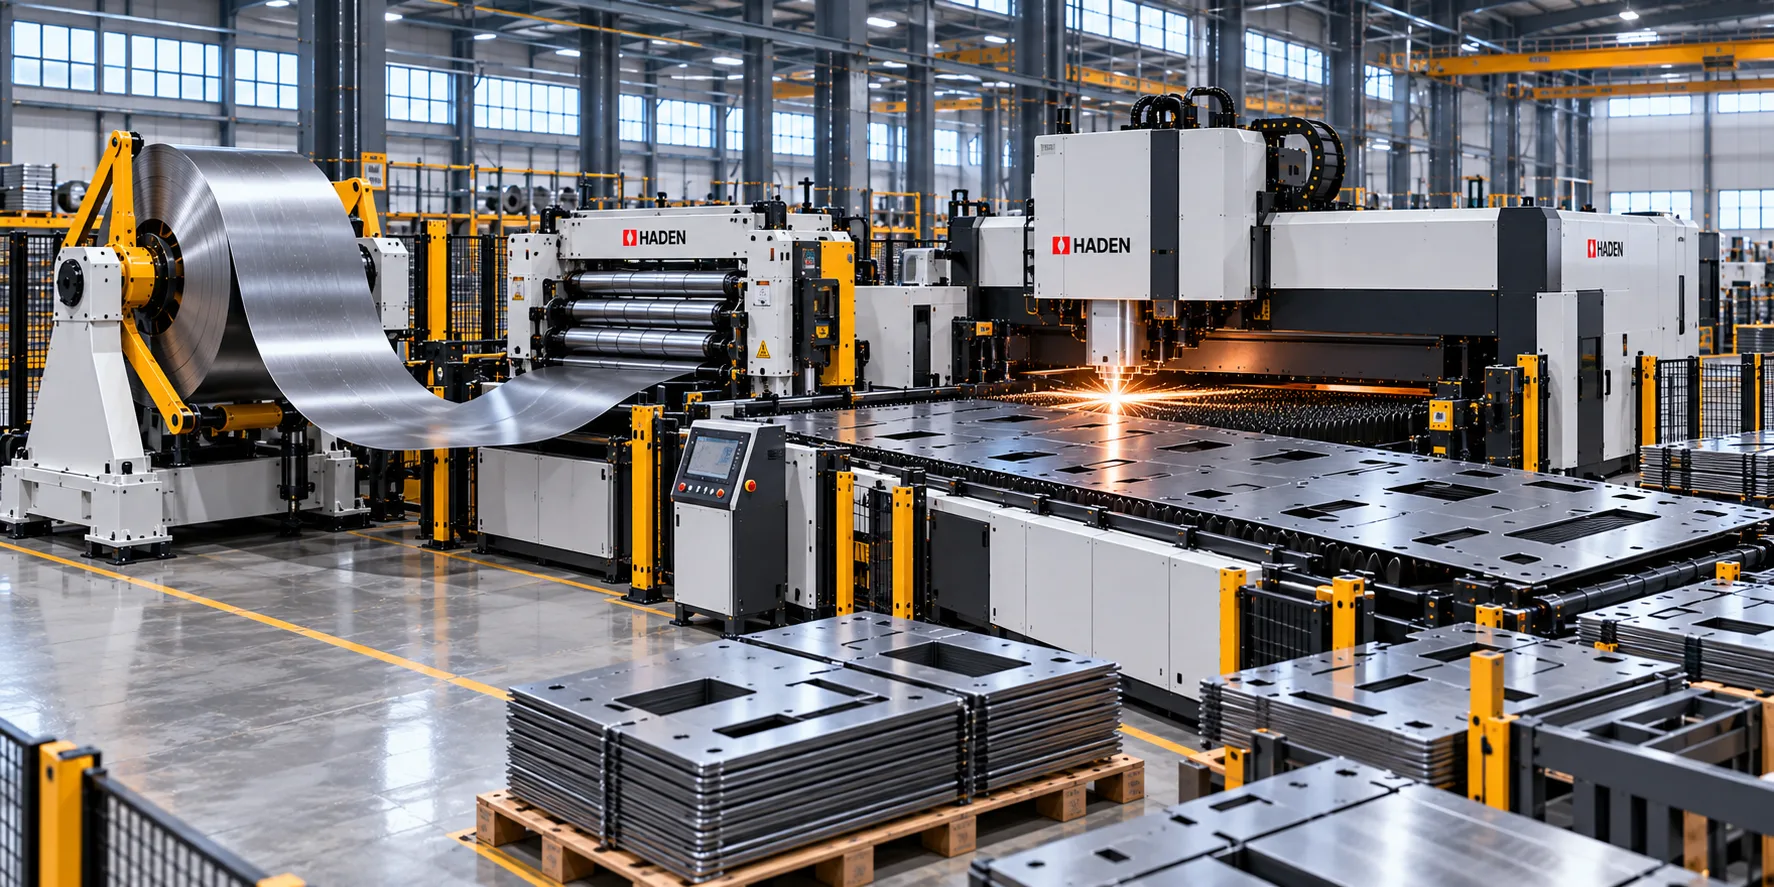
Technical Parameter Specification Matrix
Compare essential engineering metrics across our primary industrial coil-fed laser cutting configurations.
| Specification Parameter | Standard (CL-1500S) | Dual-Head (CL-1600D PRO) | Heavy-Duty (CL-2000H MAX) |
|---|---|---|---|
| Applicable Coil Width | 500 mm – 1,500 mm | 600 mm – 1,600 mm | 800 mm – 2,000 mm |
| Thickness Capacity (Carbon Steel) | 0.5 mm – 3.2 mm | 0.6 mm – 4.0 mm | 1.0 mm – 6.0 mm |
| Thickness Capacity (Stainless / Aluminum) | 0.5 mm – 2.5 mm | 0.6 mm – 3.0 mm | 1.0 mm – 5.0 mm |
| Fiber Laser Power Selection | 3 kW / 4 kW / 6 kW | 6 kW + 6 kW / 12 kW Dual | 12 kW / 15 kW / 20 kW |
| Maximum Coil Weight | 5 Tons / 10 Tons | 10 Tons / 15 Tons | 15 Tons / 20 Tons |
| Positioning Accuracy (X/Y) | ±0.03 mm/m | ±0.03 mm/m | ±0.05 mm/m |
| Repeatability Accuracy | ±0.02 mm | ±0.02 mm | ±0.03 mm |
| Max Cutting Acceleration | 1.5 G | 2.0 G (Per Gantry) | 1.2 G |
| Leveling Roller Configuration | 19 Multi-Roll Precision Unit | 21 High-Precision Rollers | Heavy Hydraulic Cassette Unit |
| Central CNC Architecture | Closed-Loop EtherCAT Bus | Multi-Axis Dual Synchronized CNC | Closed-Loop EtherCAT Heavy CNC |
Built Around Your Coil-Fed Production Requirements
Haden configures coil-fed laser cutting lines with suitable fiber laser sources, rigid machine structures, precision motion systems, and integrated material handling. Component selection and line configuration are reviewed against your material specifications, blank dimensions, production targets, and available floor space.
Laser Blanking Line vs. Traditional Stamping Press
High-tonnage stamping presses historically dominated high-volume blanking. However, shortening product lifecycles, tighter inventory targets, and demand for rapid prototyping have shifted the manufacturing benchmark. An industrial coil fed laser cutting machine, alongside advanced continuous laser cutting machines, introduces flexible moldless cutting directly from mother coils—eliminating multi-week die fabrication cycles, physical tool storage, and costly changeover delays.
Haden Coil Laser Blanking Line
Zero Tooling Overhead & Immediate Ramp-Up
Imports CAD/CAM DXF and STEP files directly into the CNC nested program with zero die machining expenditure. Transition from engineering sign-off to full-speed production in hours rather than months.
Agile Engineering Changes & Rapid Revisions
Executes instant geometric revisions, pilot prototypes, and multi-part batch interleaving on the fly without scrapping physical die blocks, reworking EDM inserts, or paying expensive setup penalties.
Complex Profile & Common-Line Continuous Nesting
Delivers intricate contours, curved automotive blanks, and shared-edge cutting along continuous uncoiled strip lengths, maximizing raw material utilization up to 90% to 96%.
Low Maintenance, Vibration-Free & Quiet Operation
Non-contact solid-state fiber laser blanking eliminates punch sharpening downtime, hydraulic fluid leaks, and heavy structural ground impact, maintaining factory sound levels comfortably below 75 dBA.
Traditional Mechanical Stamping Press Line
Massive Tooling Capital & Multi-Month Lead Times
Demands dedicated progressive or transfer stamping dies costing $40,000 to over $200,000 per part number, tied to lengthy 8 to 16 week design, machining, and tryout lead times.
Costly Design Freezes & Inflexible Tool Re-cuts
Engineering changes require extensive tool rework, welding, CNC re-milling, or complete die replacement, driving up prototype costs and stalling critical time-to-market.
High Web Scrap & Rigid Pitch Constraints
Constrained by fixed progression pitches, carrier strips, and edge allowances, locking manufacturing into persistent raw coil scrap losses typically averaging 18% to 30%.
Intensive Tool Maintenance & Heavy Storage Racks
Requires overhead bridge cranes, expansive floor space for heavy die racking, continuous mechanical lubrication, and recurring punch/die blade re-grinding schedules.
Operational Parameter Comparison Matrix
Comparing total cost of ownership across a laser blanking line vs traditional stamping press highlights distinct operational advantages in tooling amortization, changeover flexibility, energy efficiency, and floor space utilization.
| Operational Metric | Haden Coil Laser Blanking Line | Traditional Mechanical Stamping Press |
|---|---|---|
| Upfront Tooling Investment | $0 (100% Software-Driven DXF/G-Code) | $40,000 – $200,000+ per individual SKU |
| Production Ramp-Up Time | Immediate CAD-to-Cut (< 30 Minutes) | 8 to 16 Weeks (Die Design, Tooling, & Tryout) |
| Average Job Changeover | Under 2 Minutes (Digital Program Call-Up) | 45 to 120 Minutes (Heavy Crane Die Rigging) |
| Material Scrap Ratio | 4% – 10% (Endless Continuous Nesting) | 18% – 30% (Carrier Strips, Webbing, & Trims) |
| Floor Space & Die Inventory | Compact footprint; zero die storage footprint | Massive warehouse space required for die racks |
| Blank Edge Quality & Stress | Burr-free, smooth edge with zero tool contact stress | Shear burrs require frequent tool re-sharpening |
Transitioning Your Workshop to Tool-Free Laser Blanking
Haden application engineers assist sheet metal fabricators and Tier-1 stampers in evaluating part-level cost conversions across our automated manufacturing products. Eliminate heavy tooling overhead, shorten prototype lead times, and optimize production agility with our continuous coil laser cutting solutions.
- Comprehensive ROI audit comparing hard progressive dies versus laser nesting
- Integrated line design covering uncoiling, precision leveling, high-speed sheet metal laser cutting machines, and stacking
- Application validation and test cutting on your specific carbon steel, stainless, or aluminum coils
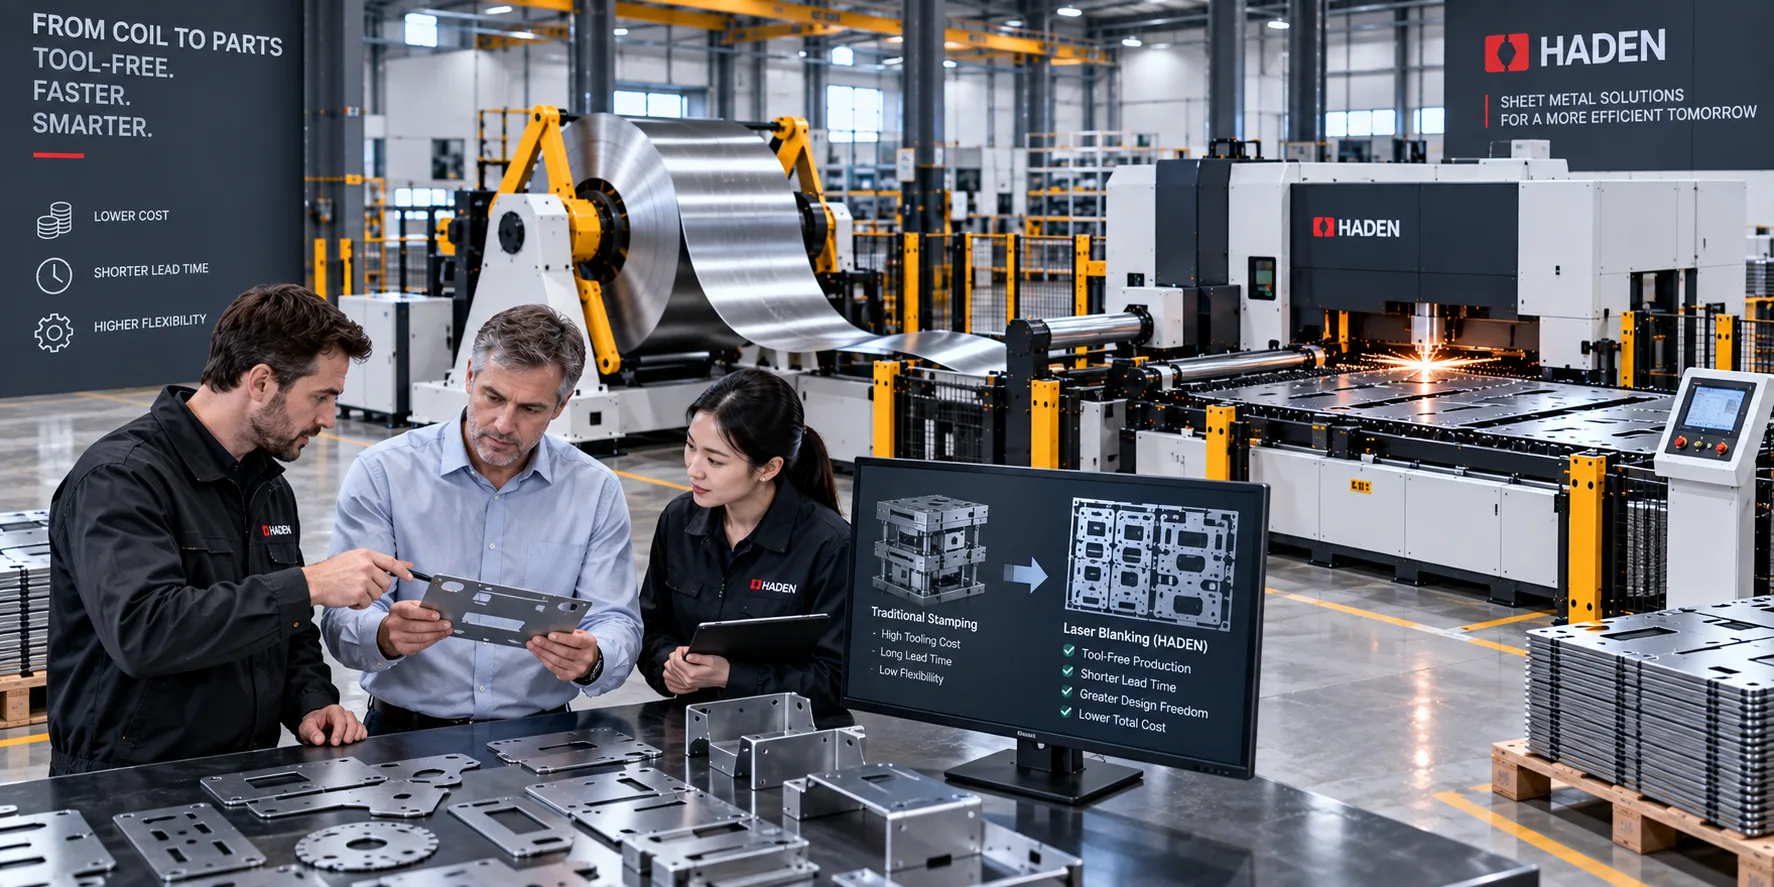
Industrial Coil Fed Laser Cutting Applications & Custom Blanking Solutions
Continuous coil fed laser cutting machines fundamentally transform high-volume sheet metal processing by removing standard sheet length limits and eliminating hard stamping tooling constraints. Haden engineers turnkey, high-speed automated coil blanking lines specifically configured to satisfy rigorous dimensional tolerances, pristine edge quality standards, and rapid takt-time demands across modern industrial production facilities.
From high-strength advanced automotive steels to mirror-finish stainless steel for commercial appliances, our integrated decoiling, precision multi-roll leveling, and dynamic continuous laser cutting architectures maintain uncompromised blank flatnesses, eliminate surface abrasions, and consistently achieve material utilization rates exceeding 95%.
Automotive & Tier Suppliers
Automotive coil laser blanking supports flexible production of body-in-white components, exterior closures, and electric vehicle battery enclosure blanks, including parts that require frequent design revisions.
Production Bottlenecks
- •Stamping die costs and long tooling lead times when part designs change.
- •Material scrap from complex blank contours and inefficient nesting.
Haden Custom Solution
- ✓Die-Free Flexibility: Digital cutting programs support part revisions without dedicated blanking dies.
- ✓Optimized Nesting: Part layouts can be arranged to improve coil utilization and reduce offcuts.
Door inners, chassis pillars, structural crossmembers, EV tray blanks
HVAC & Ductwork
HVAC manufacturers and sheet metal fabrication shops process variable-size duct wraps, transition sections, elbows, and ventilation fittings from galvanized and other sheet metal coils.
Production Bottlenecks
- •Fixed-size sheet preparation can create offcuts and additional handling steps.
- •Cut-edge quality and thermal effects can complicate downstream forming.
Haden Custom Solution
- ✓Continuous Coil Processing: Integrated uncoiling and leveling feed material into the laser cutting line.
- ✓Flexible Part Nesting: Digital cutting layouts accommodate varying duct dimensions and fitting geometries.
Rectangular duct wraps, spiral fittings, transition elbows, damper frames
Kitchenware & Appliances
Food service equipment and appliance manufacturers process stainless steel, aluminum, and coated sheet materials for refrigerators, cooktops, ovens, and sink components.
Production Bottlenecks
- •Surface scratches and roller marks during material transfer and processing.
- •Cut-edge burrs that can affect subsequent bending and forming operations.
Haden Custom Solution
- ✓Surface-Conscious Handling: Suitable roller and support configurations can be selected for sensitive sheet finishes.
- ✓Process-Specific Cutting: Assist gas and cutting parameters are selected according to material and edge-quality requirements.
Refrigerator door skins, cooktop panels, range hood housings, sink blanks
Enclosures & Steel Doors
Electrical enclosure, server rack, and commercial steel door manufacturers require flexible cutting of panels, openings, mounting holes, and exterior profiles.
Production Bottlenecks
- •Punch tooling changes and maintenance when producing varied panel designs.
- •Work-in-process buildup between cut-to-length, punching, and sorting operations.
Haden Custom Solution
- ✓Integrated Profile Cutting: Laser programs combine perimeter cutting with holes, slots, and other panel features.
- ✓Configurable Automation: Sorting and stacking options can be integrated according to part geometry and production flow.
Distribution cabinet wrappers, perforated chassis subpanels, fire door skins
Configure a Coil-Fed Laser Blanking Line for Your Plant
Share your material grades, coil dimensions, blank drawings, production targets, and available floor space. Haden can review your application requirements and discuss suitable uncoiling, leveling, laser cutting, and automated handling configurations for a custom production line.
Coil-Fed Laser Cutting Machine Frequently Asked Questions
Clear technical guidance on coil thickness capacity, continuous laser blanking operations, maintenance cycles, and line investment metrics.
Engineering & Line Consultation
Configuring the right uncoiler weight rating, precision roller straightener, and fiber laser source depends on strip yield strength and daily output quotas. Haden application specialists deliver end-to-end line evaluation from foundation loads to cycle-time simulation.
Operational Performance Summary
Industrial manufacturers upgrading from precut flat sheets to continuous coil blanking consistently hit lower costs per piece and higher throughput.
What raw materials and coil thickness ranges can this system process?
Haden coil-fed laser cutting machines are engineered to process standard commercial rolled metals straight from master coils. Standard production lines handle strip gauges from 0.5 mm to 3.2 mm at high cutting speeds, while reinforced heavy-duty systems cut plate up to 6.0 mm.
- Mild & Carbon Steel: Cold-rolled and pickled hot-rolled coils from 0.5 mm to 6.0 mm for automotive stampings, brackets, and structural framing.
- Stainless Steel (304, 316, 430): Coils from 0.5 mm to 3.0 mm processed with high-pressure nitrogen for scale-free edges on appliances and food service equipment.
- Galvanized & Pre-Coated Steel: From 0.6 mm to 2.5 mm, widely used for HVAC spiral/rectangular ductwork, cable trays, and electrical enclosures without zinc coating peel.
- Aluminum Alloys (3000, 5000, 6000 Series): From 0.8 mm to 3.0 mm, equipped with anti-reflective optical monitoring and oil-film compensation.
The sweet spot for return on investment sits between 0.8 mm and 2.5 mm, where continuous fiber laser blanking matches progressive stamping line speeds while removing all hard-tooling and die-storage expenses.
How does the precision leveling system guarantee laser focal stability and cut consistency?
Raw coiled strip retains coil set, crossbow, and residual rolling stress. If uncoiled directly into a cutting chamber without thorough leveling, the strip will buckle or flutter, causing nozzle collisions, dross formation, and unstable focus control.
Haden integrates a high-precision multi-roll leveler featuring 19 to 23 micro-alloy straightening rolls backed by multi-group adjustable support blocks. This setup eliminates sheet stress in three coordinated stages:
- Progressive Reverse Bending: Subjecting the metal strip to alternating plastic-elastic deformation that neutralizes internal stress and flattens coil curves.
- Strict Flatness Control: Delivering strip flatness within ±0.5 mm per square meter across the active laser cutting bed.
- High-Frequency Height Following: The cutting head's capacitive sensor detects subtle dynamic surface shifts at millisecond speeds, maintaining a constant nozzle standoff distance during high-acceleration motion.
This combination prevents edge dross, protects optical nozzles, and keeps dimensional tolerances tight across uninterrupted production runs.
What floor space, pit, and foundation requirements apply compared to flatbed laser systems?
Unlike clusters of individual flatbed sheet metal laser cutting machines that demand wide aisles and intermediate pallet racks, a coil-fed laser line operates on an organized in-line footprint, delivering cleaner material flow and reduced work-in-progress inventory.
| Evaluation Criteria | Haden Coil-Fed Laser Blanking Line | Multiple Flatbed Lasers + Cut-to-Length Line |
|---|---|---|
| Overall Footprint | Linear layout: approx. 20m – 30m length × 4.5m – 6.5m width | Scattered layout: multiple 9m × 6m laser cells plus sheet warehousing |
| Floor Space Savings | Saves 35% – 50% by eliminating intermediate sheet staging | Requires extensive transit aisles for constant forklift pallet runs |
| Foundation Engineering | Standard reinforced concrete slab (300 mm–400 mm); no deep pits needed | Multiple standard slabs with separate heavy scrap bin staging zones |
| Crane & Handling Loads | Single overhead crane load per 10–20 ton master coil | Continuous bundle moves, crane transfers, and pallet unbundling |
Haden supplies complete civil engineering blueprints, including dynamic anchorage and electrical channel layouts, well ahead of delivery to ensure quick, smooth installation.
How long does a coil changeover take when switching material types or widths?
Coil laser blanking lines are built for flexible, high-mix production. With automated loading accessories, a full changeover between coil gauges or strip widths takes under 10 to 15 minutes.
- Pre-Loading Coil Loading Car: The next coil is staged and auto-centered on the loading car while the previous coil is still cutting, minimizing uncoiler downtime.
- Hydraulic Peeler & Pinch Infeed: The hydraulic peeler arm and snubber roll flatten and thread the strip lead directly into the leveler rolls with no manual handling.
- CNC Parameter Recipe Recall: Choosing a new program automatically adjusts leveler roll gaps, side guides, feed speed, focal position, and assist gas pressure from saved memory.
Compared to mechanical stamping presses or dedicated lines requiring secondary operations on CNC hydraulic press brakes, coil-fed laser blanking turns product changeovers into a quick digital switch.
How are cut parts separated from scrap skeletons during continuous cutting?
Continuous coil laser blanking moves parts along a synchronous conveyor system instead of holding them in fixed sheet skeletons. Parts and waste are separated systematically through multiple automated discharge stations:
This automated sorting approach enables dependable, continuous operation from raw uncoiled strip to neatly palletized parts.
Plan a Coil-Fed Laser Blanking Line Around Your Production Goals
Work with Haden to review your coil material, strip dimensions, blank geometry, target output, and factory layout. We can discuss an integrated line combining uncoiling, coil leveling machines , laser cutting, and automated material handling based on your application requirements.
Application-Based Line Configuration
Review coil width, thickness, material grade, part drawings, production targets, and available floor space to identify suitable equipment configurations.
Material Utilization & Workflow Review
Discuss nesting options, material handling, and downstream processing requirements to support your production planning.
Integration & Technical Support Discussion
Review installation conditions, commissioning requirements, operator training, and service options for your proposed line.
Request a Custom Line Quotation
Tell us about your coil material, required blank dimensions, and production capacity. Our team can review your requirements and discuss a suitable line configuration.