
High-Precision CNC Tube & Pipe Laser Cutting Machines
Haden CNC tube laser cutting machines are engineered for efficient processing of round, square, rectangular, and structural profiles. Configure laser power, tube diameter, chuck system, loading automation, and material handling around your production requirements. Explore our industrial laser cutting machines for different metal fabrication applications.
Tube Laser Cutting Machine Series and Engineering Selection Matrix
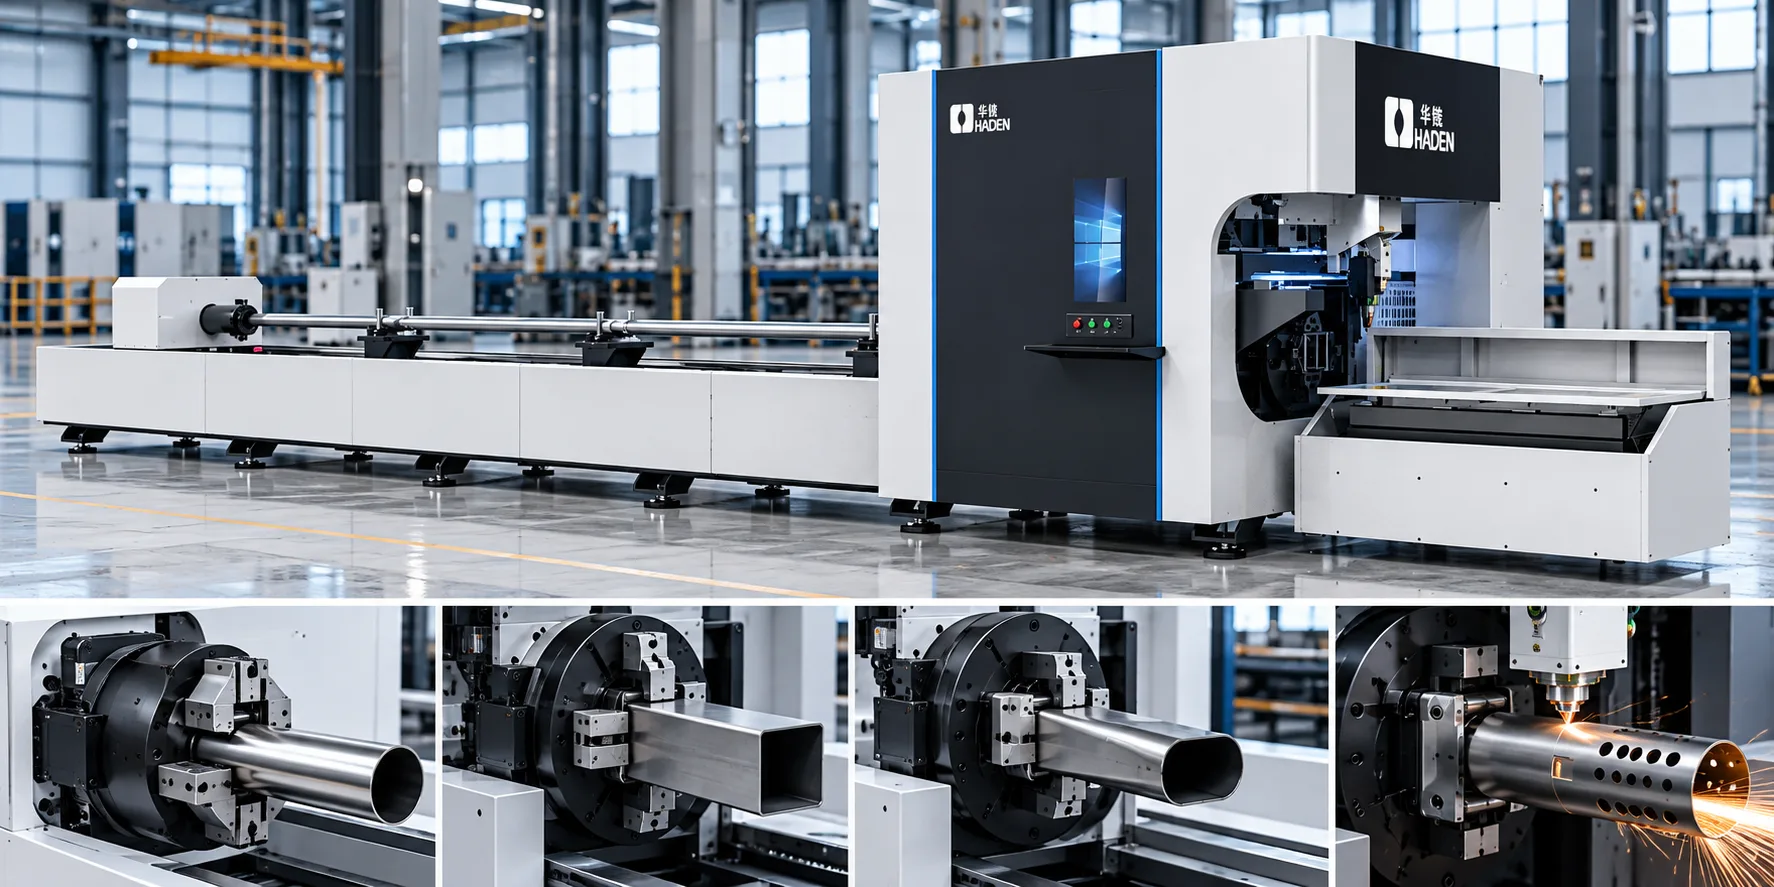
Selecting the right CNC pipe and tube fiber laser cutting machine requires matching profile cross-sections, wall thicknesses, batch volumes, and downstream assembly requirements. As part of Haden's advanced portfolio of industrial laser cutting machines, we engineer high-precision tube cutting platforms categorized into purpose-built configurations. From high-throughput standard tubular production to general tube fabrication to three-chuck processing for improved tube support and reduced tail material, the HD-R Series provides six verified configurations with pneumatic, servo and automatic loading options.
HD-R X1/X2 Pneumatic Chuck Series
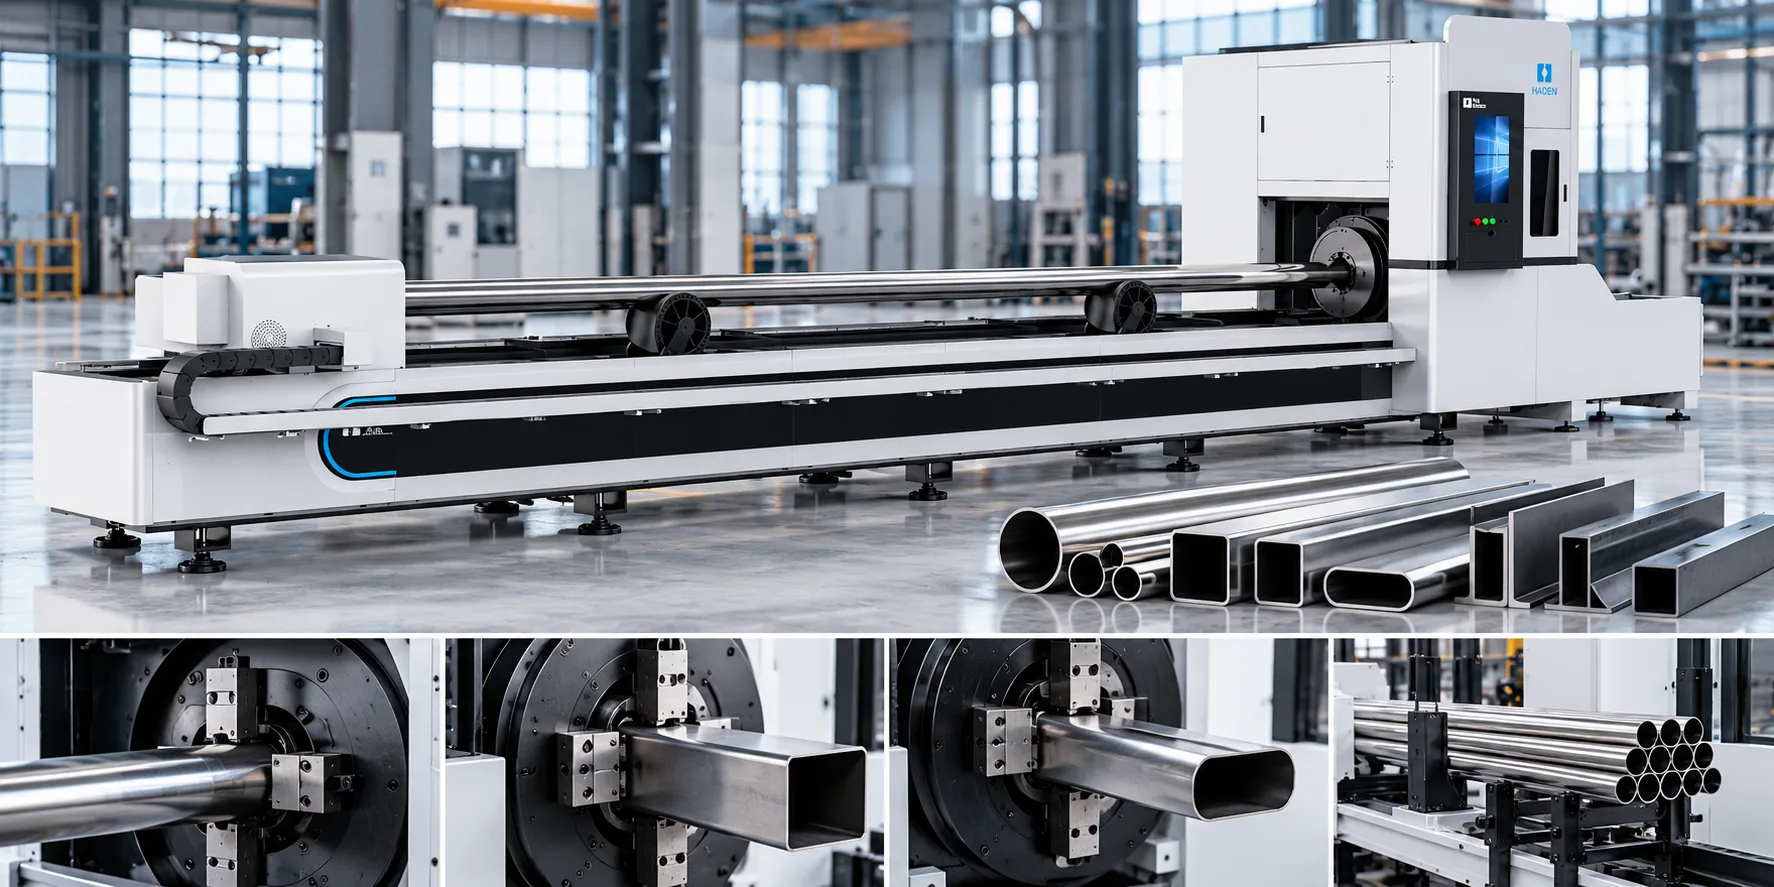
Designed for high-mix, continuous production in contract manufacturing, the HD-R series handles round, square, rectangular, and flat-oval profiles with effortless changeovers. For fabricators requiring dual-purpose flat plate and tubular processing, we also engineer multi-function sheet and tube laser cutting machines. Equipped with dual synchronized full-stroke self-centering pneumatic chucks and an optional automatic bundle loader, this system eliminates manual jaw setups while reducing cycle times on repetitive tubular parts.
- ✔Zero-Setup Pneumatic Chucks: Full-stroke self-centering chucks automatically modulate clamping force by material thickness, preventing deformation on thin walls while securing heavy tubing.
- ✔Active Follow-Up Servo Support: Real-time dynamic V-supports track tube rotational movement to prevent center sagging and vibration during high-speed cutting passes.
- ✔Automated Scrap Sorting: Finished components and drop remnants are segregated automatically across dual programmable unloading conveyor tables.
Published Cutting Accuracy
±0.05 mm, subject to application
Comprehensive Series Specification Matrix
Compare clamping dimensions, chuck architectures, remnant lengths, and automated material handling options across the Haden tube laser catalog, designed to work seamlessly alongside our high-speed sheet metal laser cutting machines.
| Model Configuration | Working Tube Range | Available Power | Chuck Configuration | Tail Remnant Length | Bundle Loader Option |
|---|---|---|---|---|---|
| X1 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Bed-Type Pneumatic | Application-dependent | Automatic loading available |
| X2 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Side-Mounted Pneumatic | Application-dependent | Automatic loading available |
| X3 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Bed-Type Servo | Application-dependent | Automatic loading available |
| X4 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Side-Mounted Servo | Application-dependent | Automatic loading available |
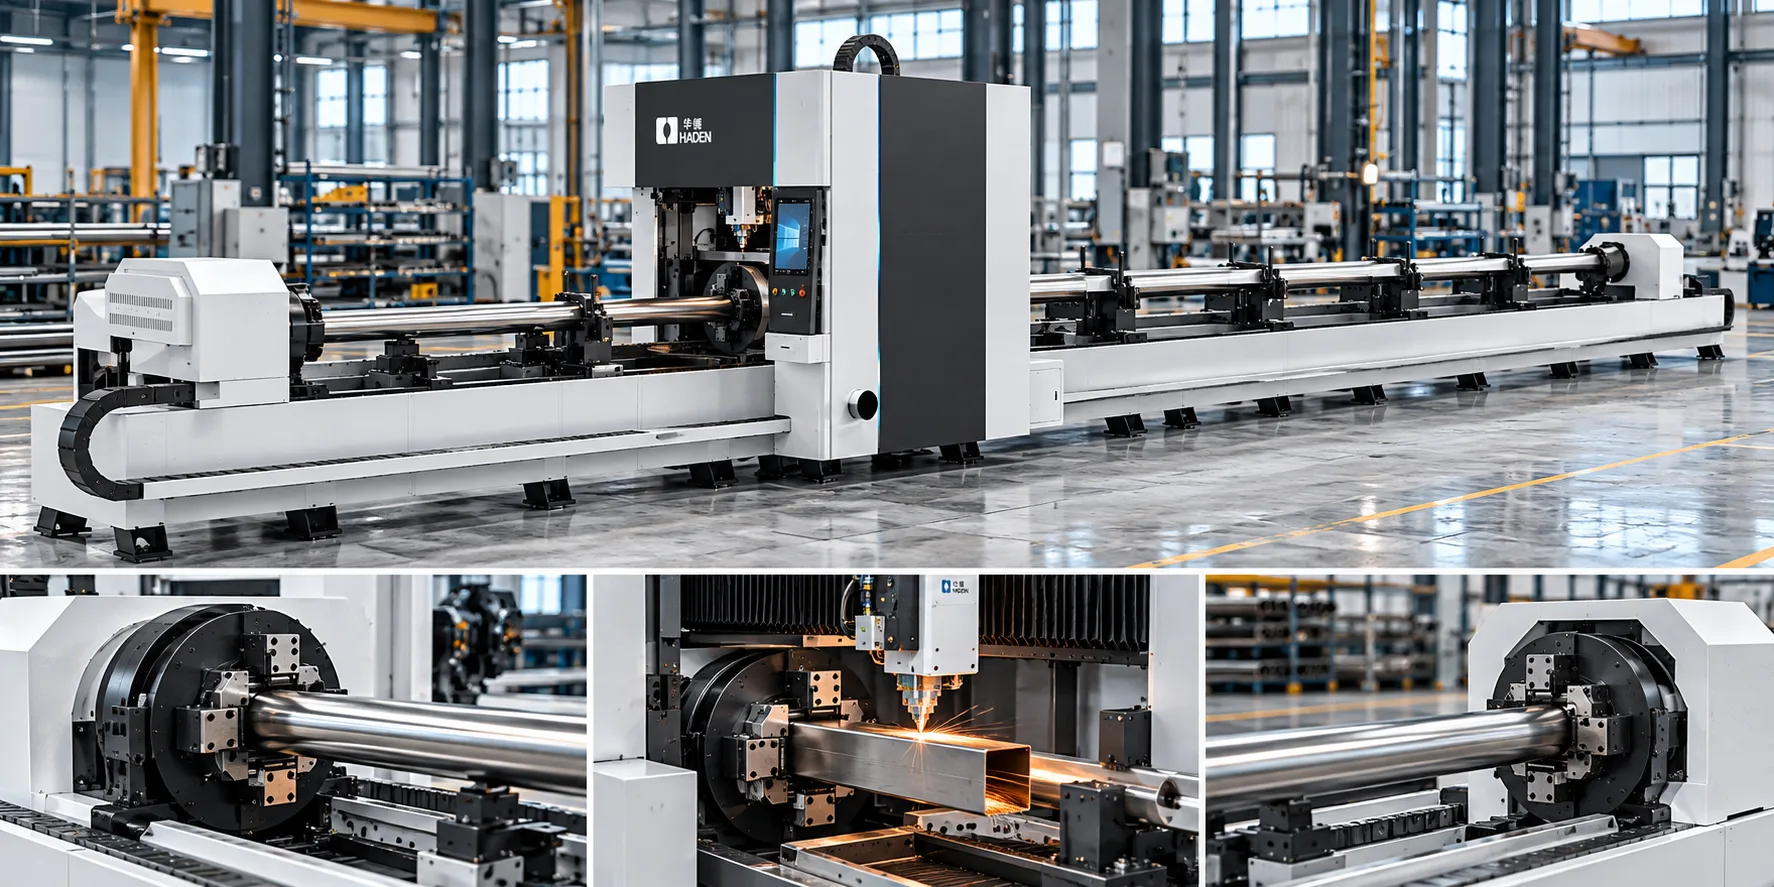
| X5 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Three-Chuck Bed-Type | Reduced tail material | Automatic loading available |
| X6 | HD-R range: Round Ø19–520mm; Square 19–520mm* | 1.5–30 kW* | Three-Chuck Side-Mounted | Reduced tail material | Automatic loading available |
* Published values describe the available HD-R Series envelope, not the capacity of every individual configuration. Final tube range, thickness, laser power, loading method, cycle time and remnant length must be confirmed against material grade, profile geometry and part drawings in the signed technical proposal.
Supported Profile Versatility and Multi-Axis CNC Laser Processing
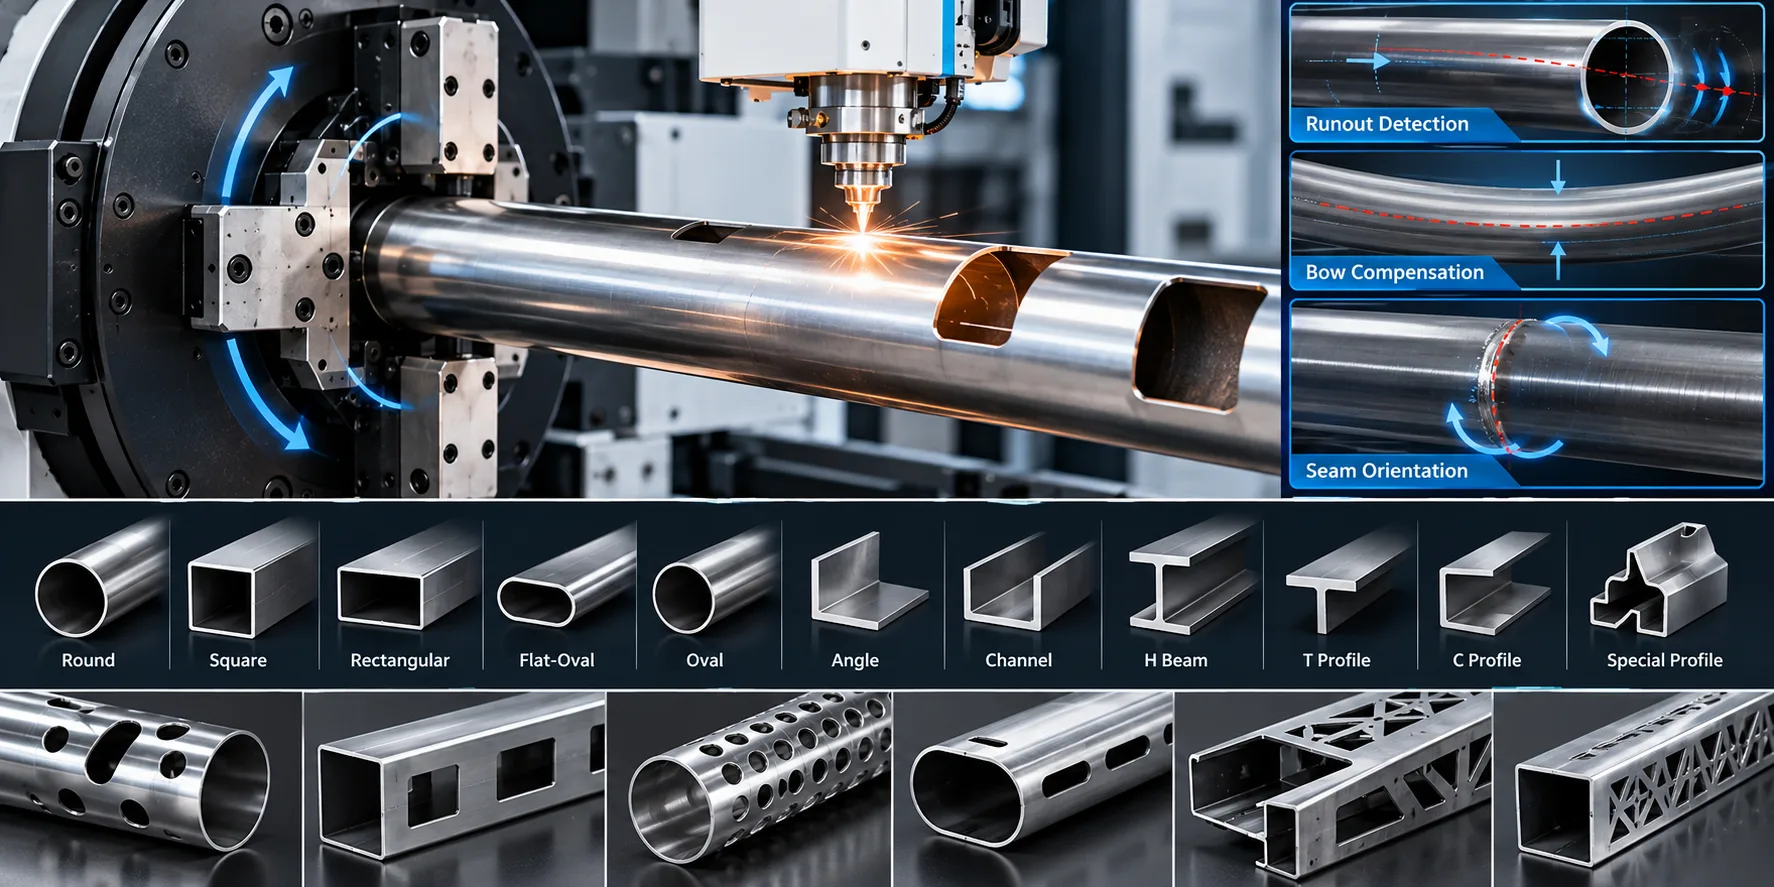
High-throughput tube fabrication demands broad cross-section adaptability and precise kinematic toolpaths. Engineered among the industry's premier industrial laser cutting machines, Haden CNC pipe cutters utilize synchronous multi-axis interpolation and dynamic capacitive surface tracking to process closed structural hollow sections, asymmetrical open extrusions, and heavy structural beams without mechanical die changes or tooling changeovers.
Comprehensive Cross-Section Profile Compatibility
Haden tube laser systems integrate full-stroke pneumatic self-centering chucks with real-time rotational coordinate compensation. The machine automatically measures incoming raw stock runout, bow, and seam orientation, dynamically offsetting laser nozzle delivery across symmetrical and non-symmetrical profiles.
Advanced 3D Contouring & Weld Prep Routines
Replace legacy band sawing, milling, coping, and punching with one-pass thermal processing. For facilities managing hybrid production runs, versatile sheet and tube laser cutting machines offer seamless adaptability alongside dedicated tube systems. Multi-axis CNC kinematics execute intricate intersecting profiles and self-locating joints ready for direct robotic or manual assembly.
- ✓Complex Saddle & Intersection Cuts:
High-precision branch-to-header coping and compound angled intersection cuts for pipe trusses, roll cages, and pressure vessels.
- ✓Profile Cutting Capability:
Automated V, Y, K, and X weld-prep bevels across wall suitable wall thicknesses after engineering review, reducing manual edge grinding.
- ✓Interlocking Tab-and-Slot Joints:
Self-indexing mortise-and-tenon cutouts and positioning tabs that eliminate complex welding fixtures and accelerate framing assembly steps.
- ✓Dense Perforation & Flow Slots:
High-frequency piercing patterns and micro-bridge arrays engineered for exhaust baffles, oil screen pipes, and acoustic attenuation tubes.
Corner Deceleration & Power Frequency Modulation
Haden CNC trajectory control dynamically modulates fiber laser power, duty cycle, and assist gas pressure during tight-radius turns on square and rectangular tubing. This avoids corner thermal over-burning, preserves opposite-wall integrity, and produces sharp, dross-free transition radii.
Material Adaptability & Wall Thickness Thresholds
Engineered to process carbon structural steel, corrosion-resistant alloys, and highly reflective non-ferrous metals with optimized assist-gas parameters and strict dimensional accuracy.
| Material Family | Common Specifications | Wall Thickness (1.5 kW – 6 kW) | Wall Thickness (8 kW – 12 kW) | Cut Surface Characteristics |
|---|---|---|---|---|
| Carbon & Mild Steel (HSS) | ASTM A500 Gr.B/C, S275, S355, Q235B | 0.8 mm – 10.0 mm | 10.0 mm – 22.0 mm | Clean, perpendicular kerf with minimal slag; weld-ready with O₂ or high-pressure air |
| Stainless Steel | AISI 304/304L, 316/316L, 409, 430 | 0.5 mm – 6.0 mm | 6.0 mm – 14.0 mm | Oxide-free, bright metallic edge under high-pressure nitrogen delivery |
| Aluminum Alloys | 6061-T6, 6063-T5, 5052, 5083 | 0.8 mm – 5.0 mm | 5.0 mm – 12.0 mm | Burr-free contouring supported by back-reflection optical isolation circuitry |
| Copper & Brass Alloys | C26000, C36000, C11000 ETP | 0.8 mm – 4.0 mm | 4.0 mm – 8.0 mm | Consistent high-beam-density cutting with active thermal load management |
| Galvanized Structural Tubing | Pre-galvanized & hot-dip galvanized conduit | 0.8 mm – 6.0 mm | 6.0 mm – 10.0 mm | Micro-pulse piercing profiles designed to minimize zinc coating vapor blowout |
Precision Chuck Hardware & Material Utilization
Haden integrates high-speed pneumatic chucks, dynamic servo-controlled follower supports, and pass-through cutting geometry across our high-performance laser cutting machines to maximize structural stability and raw material yield on every cycle.
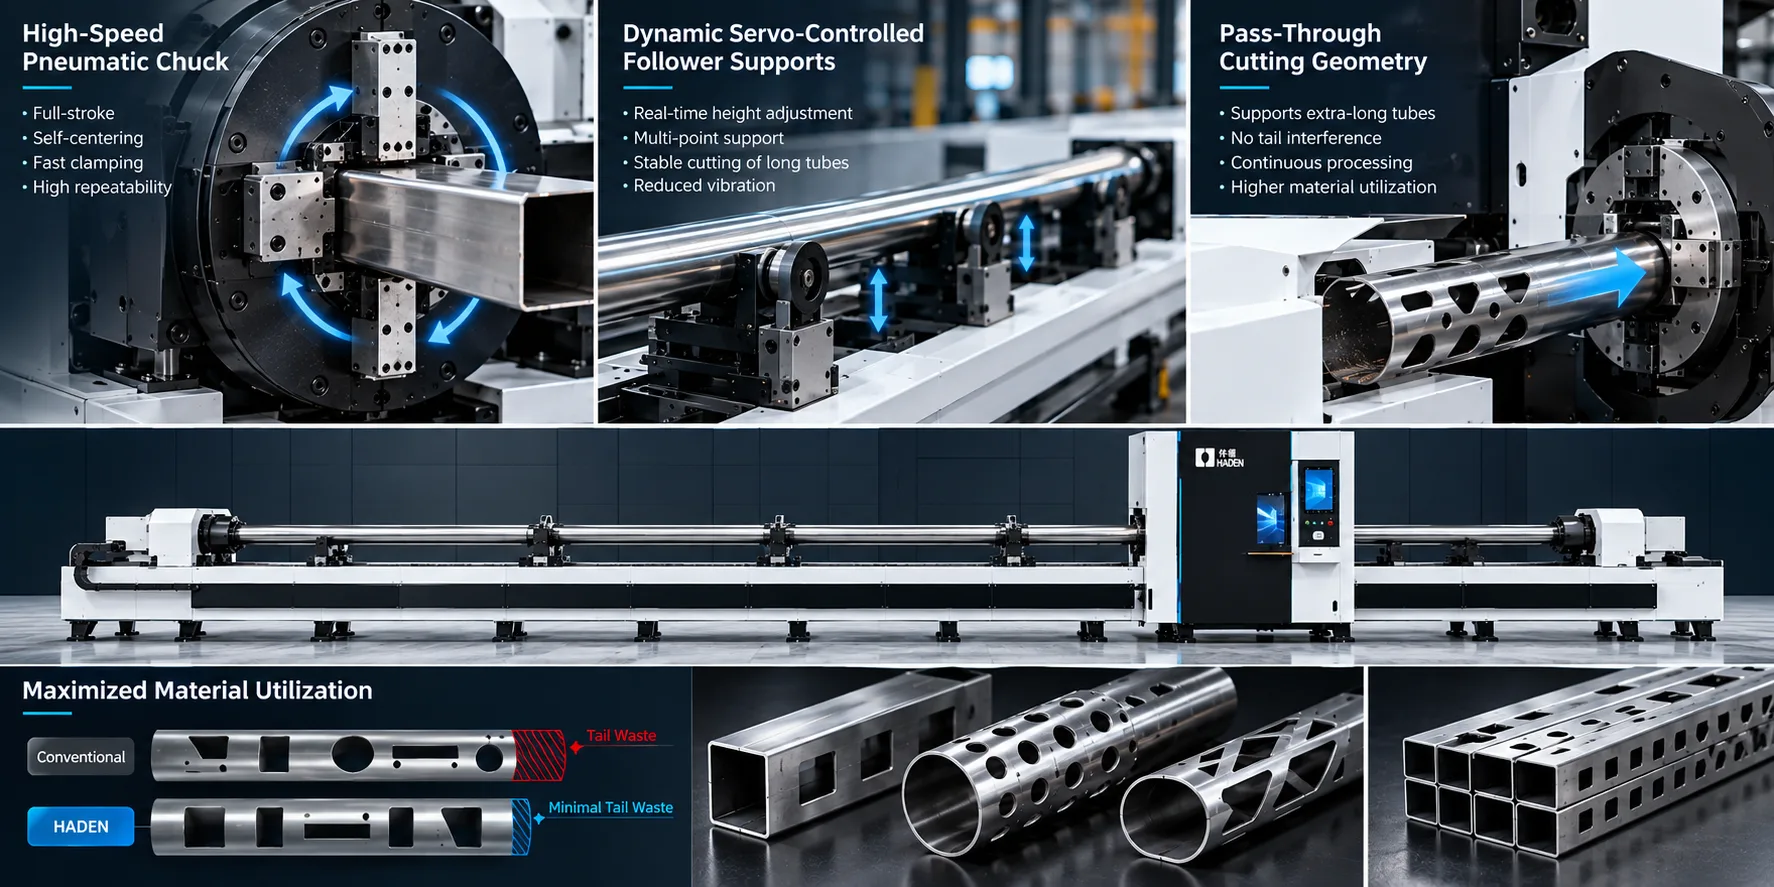
Synchronized front and rear chuck pass-through allows the cutting head to reach the extreme end of the tube, slashing scrap costs.
Full-stroke self-centering pneumatic chucks automatically adjust grip force without manual jaw changeovers across full diameter ranges.
Dual Full-Stroke Pneumatic Chucks
Intelligent pneumatic clamping actively regulates clamping torque according to pipe geometry and wall thickness. This prevents deformation on fragile thin-wall tubes while eliminating slippage on heavy-gauge structural profiles.
Full-Span Servo Follow-Up Support
Multi-point servo follow-up support brackets dynamically elevate and descend in real time as tubes rotate. This continuous stabilization eliminates gravitational sagging and dampens high-speed harmonic vibration on tubes up to 12 meters.
Three-Chuck Remnant Optimization
By coordinating rear chuck extension through the front chuck zone, the cutting head processes workpieces with minimal dead zones. Engineered into our versatile sheet-and-tube-laser-cutting-machines, this reduces tailing loss according to the part layout and cutting sequence, improving raw-material utilization in continuous production.
Automated Material Handling & Processing Efficiency Benchmarks
Consolidate multi-stage tube fabrication into a continuous, single-operator process. Integrating Haden automated bundle loading with precision laser cutting machines can deliver substantially higher throughput while drastically lowering operational costs.
Conventional Multi-Step Pipe Processing
- 1
Cold Sawing & Band Sawing
Individual cut-off steps cause thermal distortion, blade wear, and rough edge surfaces requiring secondary cleanup.
- 2
Manual Edge Deburring
Labor-intensive wire brushing and grinding required to remove sharp slag, chips, and flash before downstream work.
- 3
Secondary Milling, Drilling & Punching
Separate machine setups, custom fixtures, and manual realignment across stations introduce cumulative positional errors.
- 4
Staging, Part Inspection & Offcut Scrap
Excessive intermediate inventory staging between stations and unoptimized nesting can increase offcut and remnant waste.
Labor Footprint: 3–4 dedicated machine operators
Batch Cycle Time: 60–90 minutes per 50 complex parts
Raw Material Loss: depends on nesting, part mix and remnant handling
Haden All-in-One Automated Laser Fabrication
- ✓
One-Pass Multi-Feature Execution
Performs high-speed cut-offs, miter joints, intersecting saddle cuts, slots, and bolt holes within a single clamping cycle.
- ✓
Direct Weld-Ready Edge Quality
Fiber laser cutting produces dross-free, oxide-free edges that eliminate grinding and transfer directly to robotic welding.
- ✓
Integrated CAD/CAM 3D Nesting
Smart software optimizes nested layouts, common-line cutting, and micro-jointing across varied cross-sections automatically.
- ✓
Continuous Automated Material Flow
Heavy bundle loading, tube singularization, dynamic servo support, and finished-part sorting run with minimal operator input.
Labor Footprint: 1 operator (staging & supervision)
Batch Cycle Time: 15–20 minutes per 50 complex parts
Raw Material Loss: <3% with ultra-short remnant control
Production Economics & ROI Benchmarks
| Performance Metric | Traditional Saw & Drill Line | Haden Automated Tube Laser | Operational Gain |
|---|---|---|---|
| Cutting Throughput (parts/hr) | 20–35 parts/hour | 90–140 parts/hour | +300% to +400% |
| Direct Labor per 1,000 Tubes | 120–160 labor hours | 10–14 labor hours | −90% labor demand |
| Raw Material Yield Rate | 75–82% utilization | 96–98.5% utilization | +15% to +20% yield |
| Secondary Deburring & Cleanup | 30–45% of total cycle | 0% (direct to fabrication) | 100% eliminated |
| Fully Burdened Part Cost | $9.50–$16.00 / piece | $2.20–$4.50 / piece | −70% to −75% |
Four-Step Automated Bundle Loading & Processing Cycle
The Haden automated loading architecture handles round, square, rectangular, and open profiles up to 3 tons per bundle, ensuring uninterrupted cutting without manual crane staging.
Heavy Bundle Staging
Overhead crane or forklift loads entire tube bundles (up to 3,000 and up to 12m length) onto a loading system configured for the tube with safety interlocks.
Intelligent Singularization
Servo-actuated lifting arms and singulation fingers separate individual tubes from the bundle, verifying dimensional profiles and screening for overlap.
Continuous Servo Infeed
Tubes advance onto V-shaped servo positioning rollers that automatically center the profile and feed it directly into the rear full-stroke pneumatic chuck.
Part Sorting & Remnant Drop
Finished components transfer onto automated unloading belts categorized by job program, while process-dependent tail remnants drop into dedicated scrap bins.
Financial ROI & Payback Model
Annual Labor Reduction
Reallocate 2 to 3 full-time shop floor operators to high-value assembly and finishing operations.
Raw Material Optimization
Save thousands in alloy and structural steel through micro-tailing clamping and common-line nesting.
Tooling & Fixture Elimination
Zero blade replacement costs, no punch die wear, and no specialized welding jig fabrication requirements.
Investment Payback Timeline
Annual Production Baseline: 60,000 tube profiles / 2 shifts
Net Annualized Cost Savings: $130,000–$205,000
Standard System Capital Expenditure: Factory-direct competitive pricing
12–18 Months Average Payback
High-mix contract fabricators and automotive suppliers frequently achieve full capital breakeven in under 12 months through expanded capacity.
Quantifiable Plant Floor Transformation
Before Laser Automation
- 4 operators spread across sawing, deburring, and manual drilling cells
- 25 parts/hour ceiling; high bottleneck vulnerability during peak orders
- 18–22% offcut scrap loss due to fixed clamp margins and standard cutoffs
- High rework and scrap rates caused by manual alignment inconsistencies
With Haden Automated Tube Laser
- 1 operator oversees bundle staging, auto-processing, and output sorting
- 100–120 parts/hour steady output with lights-out continuous processing
- <3% remnant waste via zero-tail clamping and smart software nesting
- Micron-level repeatability ensures perfect snap-fit welding joints every time
Evaluate Your Tube Fabrication Efficiency & Production Costs
Send us your production drawings or CAD files. Haden application engineers can review nesting, cycle time, material utilization, and machine configuration based on your tube fabrication requirements.
High-Performance Tube Laser Cutting Applications in Structural Pipe Fabrication
Modern industrial manufacturing demands microscopic dimensional tolerances, robust structural integrity, and short turnaround cycles. Haden CNC tube laser cutting systems replace labor-intensive, multi-step routines—such as bandsawing, manual milling, mechanical punching, and edge deburring—with an all-in-one automated fiber laser workflow. From large-diameter structural steel columns to intricate hydroformed automotive exhaust pipes, our multi-axis profile laser cutting machines deliver burr-free edges, exact intersecting geometry, and weld-ready bevel cuts across continuous production runs.
Engineered with full-stroke self-centering pneumatic chucks, dynamic servo-controlled supports and professional tube-cutting systems, Haden pipe laser cutters process round, square, rectangular, oval, channel, and custom open structural profiles. For facilities handling mixed flat sheet and profile workloads, versatile sheet and tube laser cutting machines further optimize shop-floor throughput. Explore how global leaders in structural steel engineering, automotive manufacturing, commercial fitness equipment, and heavy agricultural machinery achieve lean fabrication and eliminate secondary fitting operations.

Heavy Structural Steel Framing & Intersecting Pipe Joints
Large-span space frames, bridge trusses, offshore platforms, and architectural steel structures require precision saddle cuts, multi-planar fish-mouth intersections, and multi-angle weld preps on heavy hollow sections. Haden structural pipe laser systems process structural tubes within the verified HD-R range, subject to profile, wall thickness, material and model selection.
- ✓ Complex Saddle Joints: Real-time multi-axis compensation generates zero-gap saddle intersections tailored for robotic and submerged arc welding.
- ✓ Application-Specific Processing: Verified cutting replaces manual torch gouging and angle grinding for full AWS D1.1 and EN 1090 structural code compliance.
- ✓ Heavy Open Profiles: Streamlined CNC cutting on angle iron, C-channels, U-channels, and H-beams without requiring costly custom tooling retrofits.
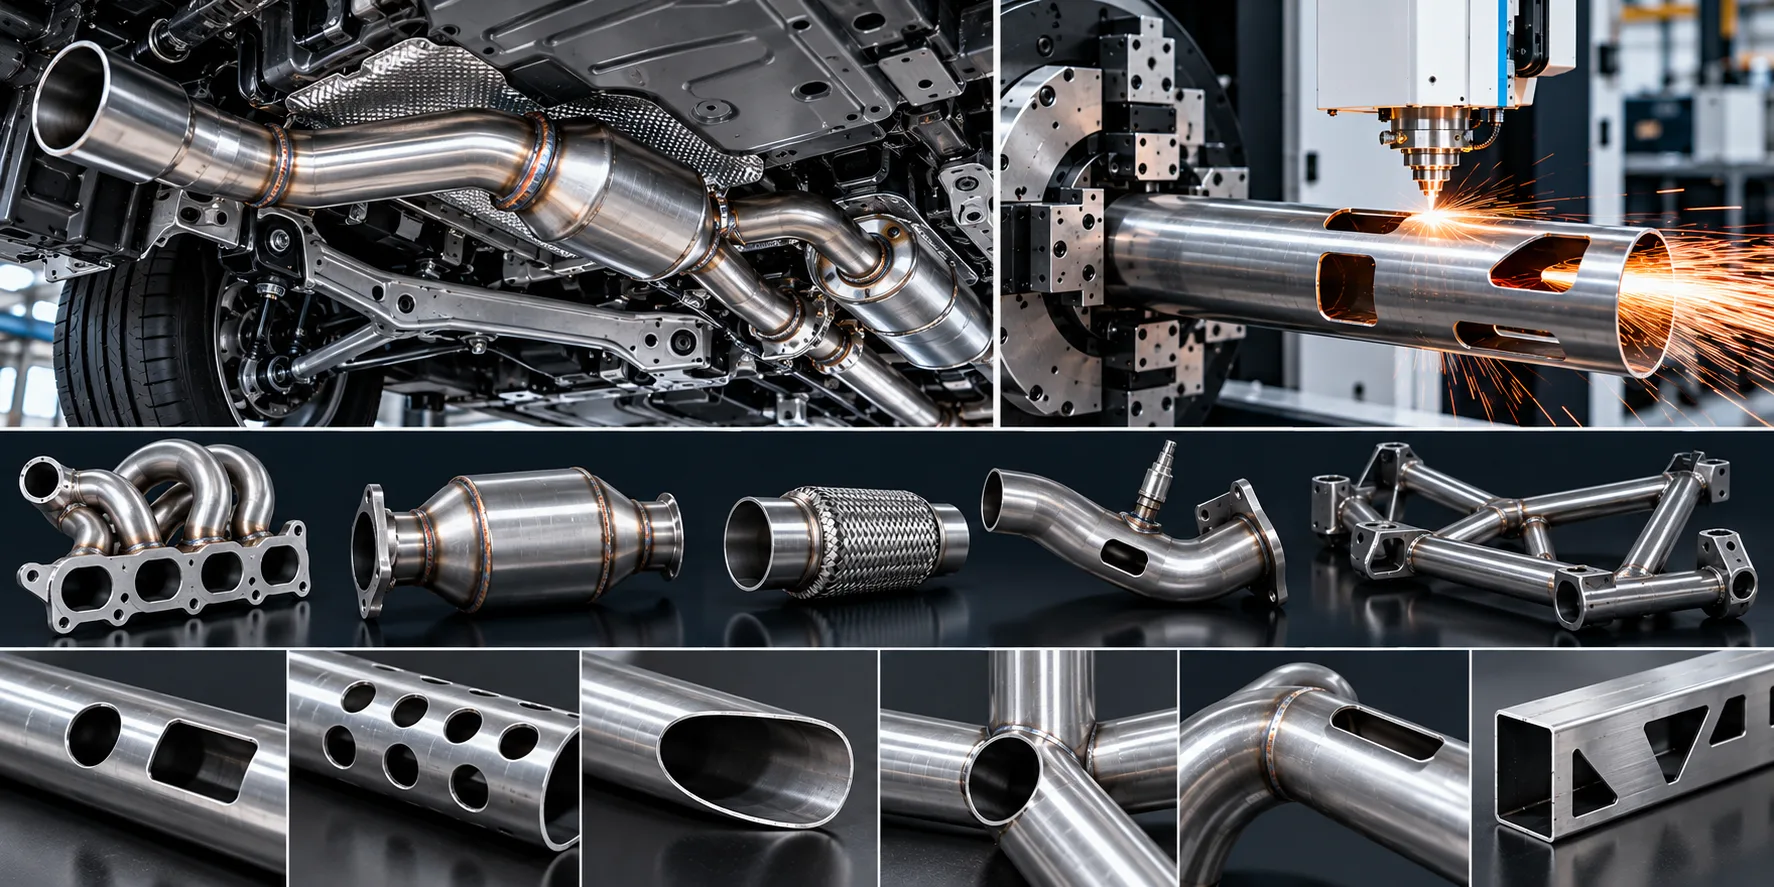
Automotive Exhaust Systems & Tubular Chassis Subframes
Automotive OEM and tier-1 supplier workflows demand rapid cycle times across thin-walled stainless steel (grades 304, 409, 316L) and hydroformed shapes. Haden CNC tube laser cutters produce burr-free cutouts for oxygen sensors, catalytic converters, flexible decoupling sleeves, and tubular suspension links with zero mechanical stress or distortion.
- ✓ Non-Contact Thermal Processing: Thin-wall exhaust tubes (0.8 mm to 2.5 mm) cut at ultra-high rotational speeds without crush deformation.
- ✓ Oxide-Free Nitrogen Cutting: Clean inert gas cutting leaves pristine, spatter-free edges ready for automatic orbital TIG or automated laser seam welding.
- ✓ Optical Weld-Seam Tracking: Intelligent vision sensors automatically detect tube longitudinal seams to orient holes away from critical bending zones.
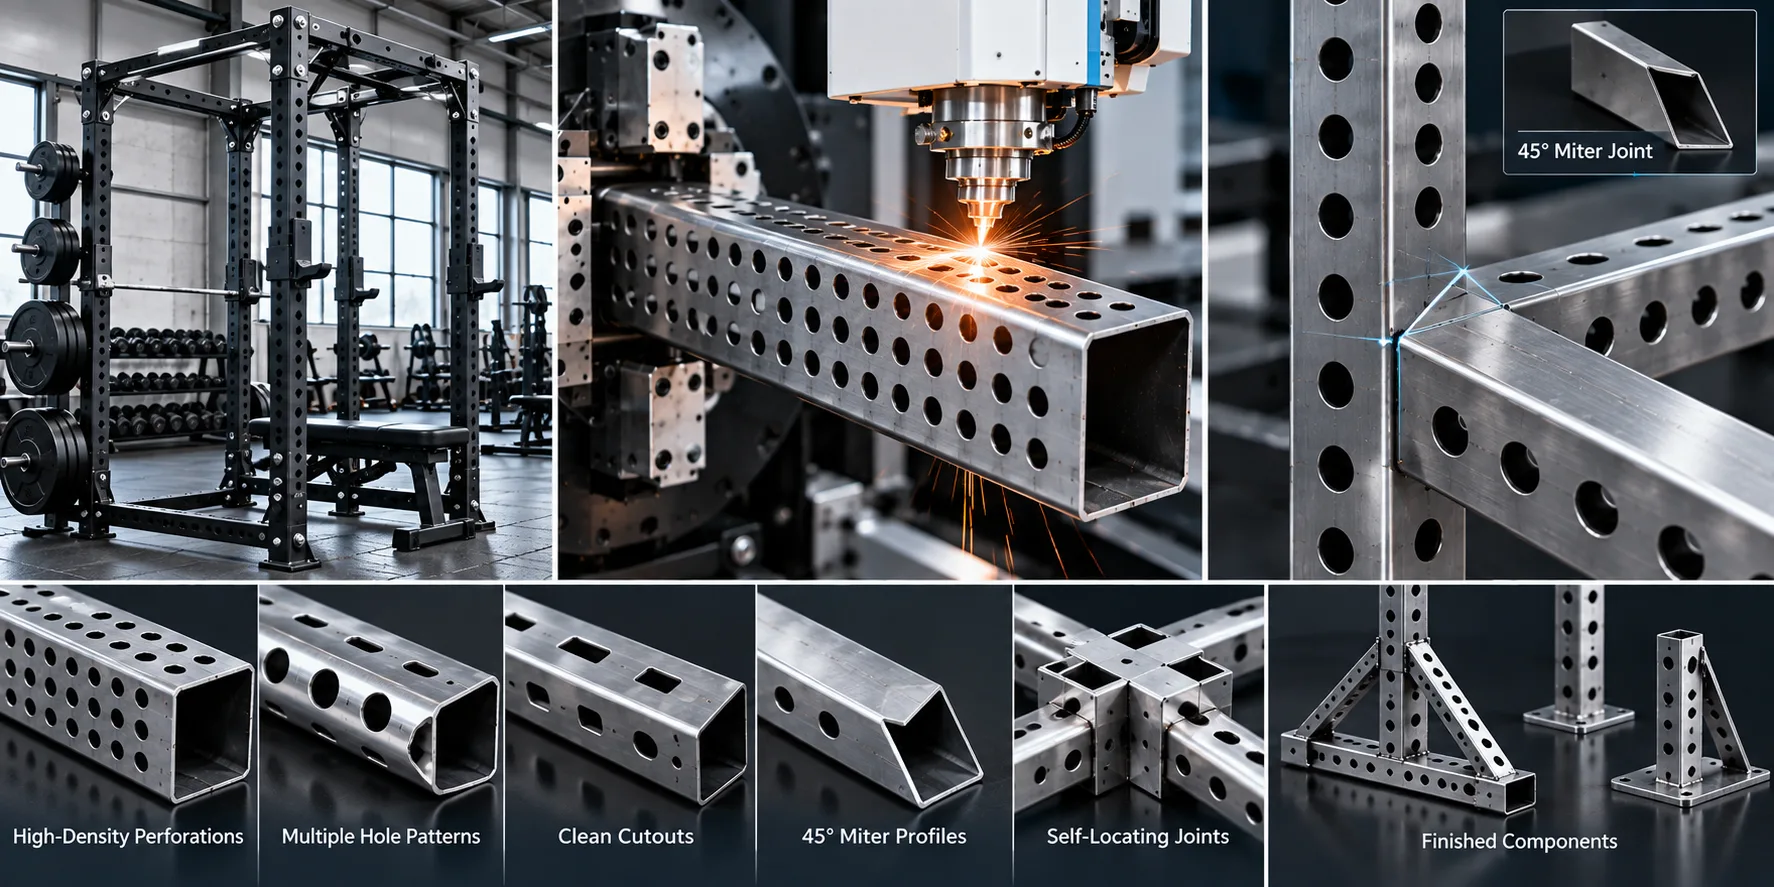
High-Density Perforations & Self-Locating Miter Joints
Commercial power racks, strength-training machinery, and architectural steel furniture demand flawless aesthetic finishes and dense hole patterns. Haden fiber tube lasers produce hundreds of clean pin-selector holes and 45-degree miter profiles in seconds, replacing multiple punch presses, drill presses, and manual cut-off saws.
- ✓ Tab-and-Slot Joint Engineering: Interlocking mortise-and-tenon laser cutouts eliminate complex clamping fixtures and reduce downstream assembly steps.
- ✓ Continuous Fly-Cutting: High-speed fly-cutting routines execute linear hole patterns and laser-etched numerical markers in a rapid single-pass cycle.
- ✓ Anti-Spatter Internal Protection: Integrated inner-tube lubrication and slag extraction prevent dross accumulation inside weight-selector channels.
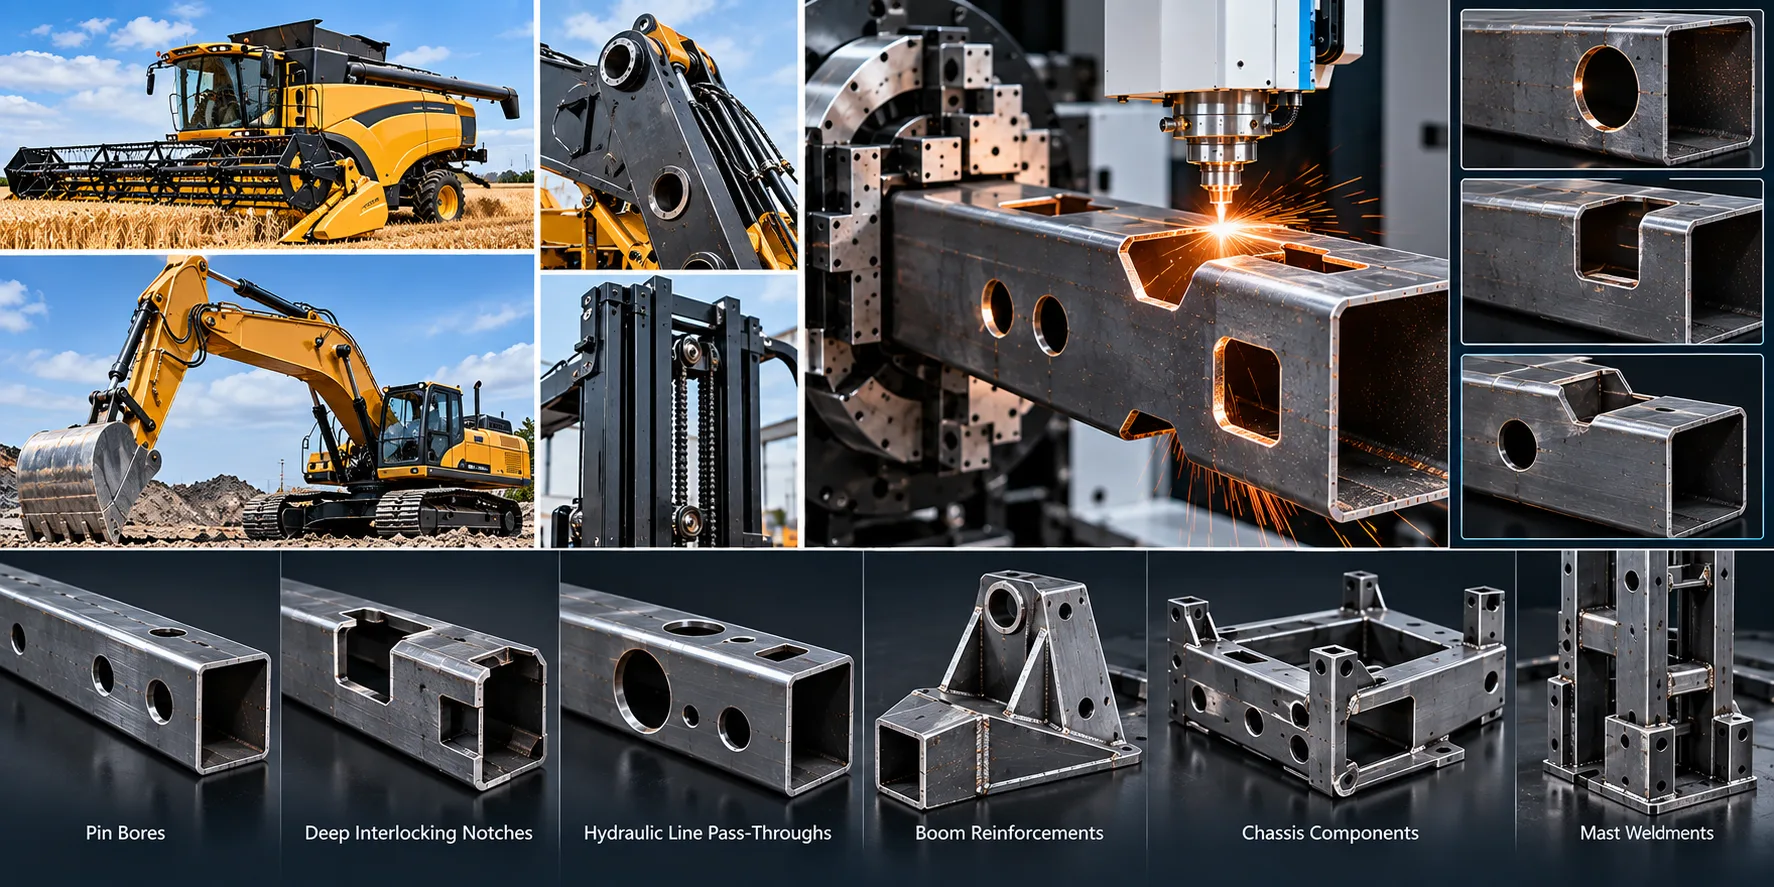
Thick-Wall Square Hollow Sections & Boom Assemblies
Combine harvester chassis, excavator boom reinforcements, tractor frames, and material handling mast weldments endure intense cyclic stress. Equipment manufacturers deploy high-power Haden tube laser systems selected from 1.5 kW to 30 kW to cut suitable structural tubing with deep interlocking notches, precise pin bores, and internal hydraulic line pass-throughs. For comprehensive heavy plate forming, operations often integrate these with heavy-duty plate rolling machines .
- ✓ High-Power Piercing in Thick Walls: High-pressure oxygen and compressed air piercing cut verified structural-steel wall thicknesses with perpendicular accuracy.
- ✓ Dynamic Sag Follower Supports: Multi-point servo-controlled lifting rollers counteract gravitational deflection on long 9 m and 12 m pipes during high-speed rotation.
- ✓ Reduced Remnant Potential: Synchronized clamping dynamics allow the rear chuck to feed inside the front chuck, helping reduce scrap tails according to the part program and tube configuration.
Cross-Industry Fabrication Benchmark: Traditional Workflow vs. Haden Tube Laser
The quantitative comparison below highlights operational, labor, and material savings achieved by replacing multiple standalone sawing, milling, drilling, and deburring workcells with a unified Haden CNC tube laser cutting center.
| Fabrication Metric | Traditional Multi-Machine Cell | Haden CNC Tube Laser Cell | Typical Production Impact |
|---|---|---|---|
| Labor Requirement | 3–4 operators across saw, mill, drill, & deburring stations | 1 operator (with automated bundle loader) | Reduced Manual Handling |
| Process Routing | Cut off → Deburr → Drill holes → Mill slots → Manual bevel | Single automated CNC laser setup | Zero In-Process WIP Buffer |
| Cut Edge Quality | Heavy burrs, clamping deformation, chips, thermal heat tint | Clean, dross-free, weld-ready micro-edges | Eliminates Secondary Grinding |
| Joint Fit-Up Method | Manual measuring, alignment jigs, repeated tack adjustments | Self-locating interlocking tab-and-slot cutouts | Faster Fit-Up & Welding |
| Material Scrap & Tailings | Conventional processes may leave longer unclampable tail scrap | Reduced remnant potential (Three-chuck configuration) | Potential Material-Yield Improvement* |
Interlocking Tab & Slot Engineering
Eliminate complex assembly jigs by laser-cutting mating tabs, tenons, and locating slots directly into round or rectangular tubes. Workpieces lock precisely into place prior to automated or manual welding.
Dynamic 3D Weld Prep Beveling
Our multi-axis 3D cutting head achieves precise V, Y, and K-type programmed profile cuts on suitable structural hollow sections, delivering optimal root face geometry for deep weld penetration in certified structures.
Intelligent Nesting & Scrap Optimization
Advanced 3D nesting algorithms automatically sequence common cutline sharing, dynamic micro-joints, and remnant nesting. Paired with synchronized chucks, raw pipe material utilization can improve tube utilization.
Heavy-Duty Machine Bed Quality, Precision Metrology, and Global Service
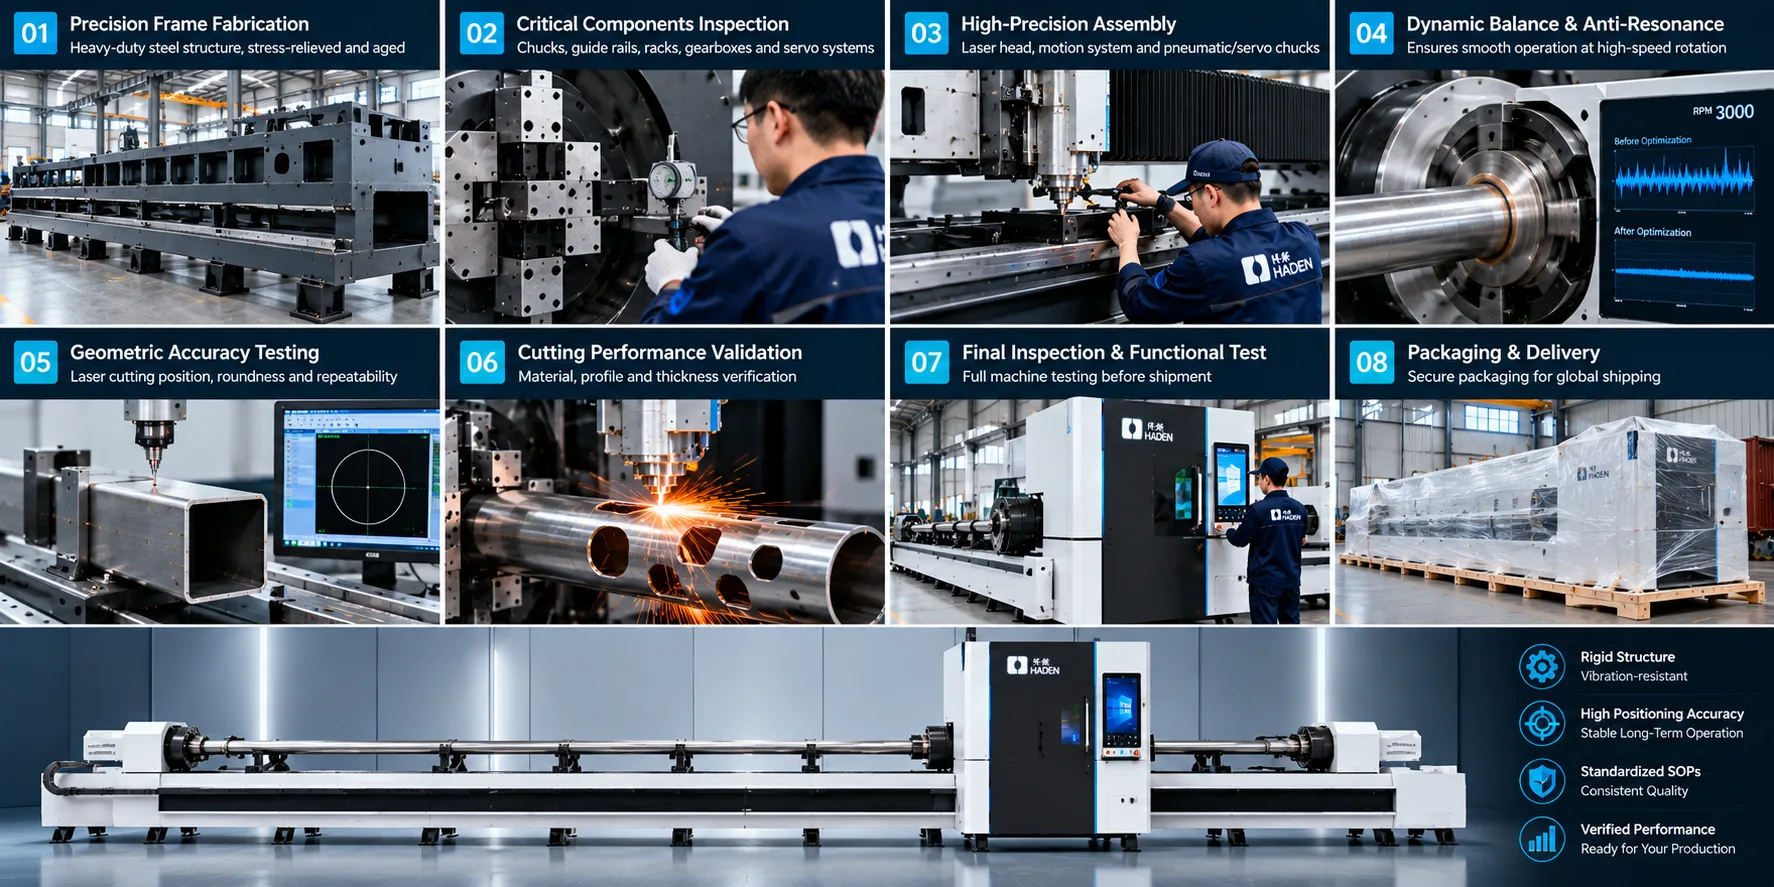
Haden builds high-precision laser cutting machines with ultra-rigid frames engineered to sustain high-acceleration rotational dynamics without deflection. Every structural weldment undergoes controlled thermal stress relief, single-setup gantry milling, and multi-axis optical interferometry before global deployment.
Stress-Relief Heat Treatment
Fabricated heavy steel beds undergo an electric furnace heat soak with controlled cooling to reduce internal welding stress and support long-term structural stability.
5-Face Gantry Machining
Linear guide rail datum planes, helical rack mounting surfaces, and dual-chuck alignment tracks are precision-milled in a single clamping setup to secure micron-level geometric straightness and parallelism.
Interferometer & Ballbar QA
Every axis undergoes full-stroke laser interferometer pitch compensation, collimator optical alignment, and Renishaw dynamic ballbar circularity verification to guarantee consistent positional repeatability.
Worldwide Engineering Support
Haden provides direct on-site factory commissioning, turnkey nesting software training, dedicated regional spare parts hubs, and encrypted remote IoT diagnostics for uninterrupted production uptime across our advanced sheet metal laser cutting machines worldwide.
Manufacturing Facility
Heavy Machine Bed Stress Relief & Metrology Center
Standardized Quality Protocols for Every Machine Tool
Every production stage follows strict standard operating procedures to eliminate resonance, maintain dynamic accuracy under high-speed chuck rotation, and guarantee stable long-term operation across our dedicated sheet and tube laser cutting machines.
Thermal Annealing & Natural Aging
High-temperature furnace heat soaking followed by natural outdoor stabilization relieves residual stresses and locks in dimensional geometry.
Monolithic 5-Face Gantry Milling
Continuous single-pass milling of guide surfaces, chuck track baselines, and rack mounting points ensures precise coaxial alignment.
Dual-Pass Metrology Calibration
Full-stroke laser interferometer pitch compensation combined with Renishaw dynamic circular testing verifies micron-level accuracy.
Continuous Endurance Validation
Multi-axis high-speed traversing, pneumatic chuck cycling, and thermal monitoring under continuous load profiles precede final dispatch.
Verified
Furnace Annealing
±0.005mm
Guide Rail Alignment
100%
Laser Optical QA
24/7
Technical Telemetry
Frequently Asked Questions on Tube Laser Selection and Operation
Selecting the right CNC pipe and profile laser cutting system involves evaluating assist gas economics, 3D nesting software compatibility, clamping automation, and dynamic geometric compensation. Explore technical answers prepared by Haden application engineers to guide your machine procurement and factory floor deployment.
1. Which auxiliary assist gas should be chosen for stainless steel, carbon steel, and aluminum tube cutting?
Assist gas selection dictates cut edge metallurgy, dross formation, feed rates, and hourly operating costs. Haden advanced laser cutting machines feature automated proportional valve switching between liquid nitrogen, industrial oxygen, and shop compressed air based on configured CNC material libraries:
-
Liquid Nitrogen (N2 | 16–25 bar)
Standard for stainless steel (0.5–12mm), aluminum alloys, and brass. Uses high kinetic pressure to eject molten material, producing clean, oxide-free, weld-ready edge quality without secondary polishing.
-
Industrial Oxygen (O2 | 0.5–3 bar)
Recommended for heavy-wall carbon steel structural pipes and profiles (6–20mm+). Leverages an exothermic reaction to lower laser power consumption and minimize gas flow costs on thick sections.
-
Clean Shop Air (16–20 bar)
The most economical choice for thin galvanized tubing and carbon steel under 3mm. Requires 4-stage refrigerated air filtration and desiccant drying down to 0.01 micron to prevent optical lens contamination.
2. Which 3D CAD/CAM nesting software suites and structural file formats are natively supported?
Haden pipe laser cutting machines connect seamlessly with industry-standard tube CAD/CAM and structural nesting software, including TubesT, Lantek Flex3d, SigmaTube, SolidWorks, and Tekla Structures . Built-in geometric parsers import native 3D solid models (.STEP, .IGES, .SAT, .X_T) without requiring manual 2D drawing conversions.
Automated Joint & Interlocking Recognition
Nesting algorithms automatically detect saddle joints, mortise-and-tenon positioning slots, mitered 45° cuts, weld prep bevels, and multi-face hole arrays directly from 3D models.
Common-Line Slicing & Remnant Optimization
By merging adjoining pipe cuts into shared toolpaths, the software can shorten piercing cycles, reduce unnecessary travel and improve raw-tube utilization by application.
3. How do full-stroke self-centering pneumatic chucks eliminate manual jaw changeovers?
Conventional pipe laser chucks require operators to manually unbolt and reposition jaw steps whenever switching tube profiles or adjusting diameters. Built for standalone systems as well as high-versatility sheet and tube laser cutting machines, Haden equipment features dual synchronized, full-stroke pneumatic self-centering chucks engineered for continuous automated production.
HD-R Geometric Range (Ø19–520mm*)
Chuck jaws traverse the entire diameter range via pneumatic stroke modulation. Operators transition from small round tubes to large rectangular sections without mechanical adjustments.
Dynamic Adaptive Clamping Force
Digital proportional valves calibrate clamping pressure automatically, preventing thin-wall tube crushing and ovality while providing controlled holding force for suitable structural stock.
4. How does the CNC control system maintain precision on bowed, twisted, or welded-seam raw tubes?
Standard commercial raw tubing often presents longitudinal camber, cross-sectional distortion, or raised longitudinal weld seams. Haden addresses material imperfections through integrated multi-axis sensor tracking and optical seam detection routines:
- Dynamic Non-Contact Centerline Probing: Capacitive sensing heads take multi-point measurements along the tube profile, recalculating real-time centerlines to compensate for rotational bow along the X/Y axes.
- Optical Weld Seam Detection: Industrial vision sensors identify weld seam positions automatically, orienting cut geometry away from seam lines or placing perforations in programmed quadrants.
- Servo-Driven Dynamic Follower Supports: Multi-point intermediate follower rollers adjust their vertical height dynamically during rotation, preventing sagging and limiting vibration during programmed indexing.
5. What are the typical consumable replacement intervals and standard preventative maintenance schedules?
Solid-state fiber laser beam delivery eliminates internal resonator mirrors and routine gas recharging. Preventative maintenance focuses primarily on cutting head optics, nozzle wear, and linear drive lubrication to maintain high positioning accuracy:
| Component / Wear Item | Estimated Service Lifecycle | Required Maintenance Action |
|---|---|---|
| Protective Cover Lens | 150 – 300 Beam Hours | Daily optical inspection; clean with optical wipes and high-purity IPA |
| Single / Double Copper Nozzles | 200 – 400 Operating Hours | Clean spatter buildup; replace if orifice roundness deviates > 0.05mm |
| Ceramic Sensor Ring | 600 – 1,000 Hours | Recalibrate capacitance height sensing; inspect threads following head collisions |
| Chuck Bearings & Linear Guide Rails | Continuous / Automated | Monitored through centralized automated lubrication pump; replenish ISO VG 68 grease |
Request a Custom Tube Cutting Solution & Application Review
Share your tube drawings, profile dimensions, material specifications, and production requirements. Haden application engineers can evaluate nesting, cutting workflow, cycle time, laser power, and machine configuration for your tube fabrication project.
Request Engineering Review
Provide your basic tube specifications for a machine configuration review.