
Electrical Enclosure Manufacturing Machinery & Automated Fabrication Systems
Engineered for high-protection control cabinets and modular enclosures. Integrate high-speed fiber sheet metal laser cutting machines, CNC sheet metal V-grooving, automated bidirectional panel bending, and flexible production cells to meet rigorous IP65, IP66, and NEMA 4X standards with zero surface marking.
Tight dimensional tolerances ensure distortion-free frame welding and smooth door operation.
Automated universal manipulator on panel benders supports agile high-mix batch-size-one production.
Precise return hems and grooved micro-radii provide ideal sealing flat surfaces for PU foam gaskets.
Continuous automated forming drastically outpaces traditional multi-operator press brake lines.
End-to-End Sheet Metal Machinery for Electrical Enclosure Fabrication
Modern electrical enclosure fabrication demands tight dimensional repeatability, scratch-free surface finishes, and versatile forming sequences. From high-volume distribution boxes and 19-inch server racks to NEMA 4X stainless steel enclosures and heavy-gauge energy storage cabinets, Haden delivers advanced laser cutting machines, precision V-grooving equipment, and panel bending systems built for demanding industrial standards.
Power Distribution & Modular Lighting Boxes
High-speed blanking and four-sided pan forming for standardized DIN-rail distribution boxes, consumer units, and modular branch circuit enclosures.
- ✔ Materials: 0.8–1.5 mm galvanized steel, cold-rolled sheet (SPCC).
- ✔ Key Processes: High-speed fiber laser blanking, automatic 4-sided positive/negative panel bending.
- ✔ Throughput: Single-piece door and pan-wrapper cycle times under 30 seconds.
Industrial Modular Control Cabinets
Engineered for automation control systems (Rittal TS8 and VX25 architecture), requiring rigid structural frameworks and complex multi-fold upright profiles.
- ✔ Materials: 1.5–2.5 mm high-strength steel, zinc-plated framing members.
- ✔ Key Processes: 9-fold and 16-fold upright roll forming, precision press brake deflection compensation.
- ✔ Tolerance: Diagonal frame repeatability within ±0.2 mm across 2.2 m vertical posts.
19-Inch Server Racks & Network Enclosures
Data center and telecommunication chassis production requiring high-density ventilation arrays, micro-flanged rails, and zero sheet distortion.
- ✔ Materials: 1.0–2.0 mm SPCC, electro-galvanized sheet, aluminum 5052.
- ✔ Key Processes: Cluster-pattern processing via sheet metal laser cutting machines, scratch-free panel hemming and stiffener forming.
- ✔ Ventilation: Up to 75% hexagonal open-area airflow patterns without thermal plate warping.
Outdoor NEMA 4X & IP66 Enclosures
Harsh marine and washdown environments demand high-grade stainless steel fabrication with sharp corners to seat continuous polyurethane foam gaskets.
- ✔ Materials: 1.5–3.0 mm AISI 304 and 316L brushed stainless steel.
- ✔ Key Processes: CNC sheet metal V grooving for micro-radius corners, scratch-free panel bending.
- ✔ Sealing Integrity: Double-break water shedding gutters engineered for NEMA 4X hose-down protection.
Renewable ESS & Solar Inverter Housings
Utility-scale battery energy storage systems (BESS) and high-capacity PCS containers requiring heavy-gauge structural channels and rigid internal framing.
- ✔ Materials: 2.0–4.0 mm structural carbon steel, Zn-Al-Mg coated corrosion-resistant sheet.
- ✔ Key Processes: High-tonnage CNC hydraulic press brake bending, heavy structural profiling with sheet and tube laser cutting machines.
- ✔ Structural Load: Internal battery rack mounts formed to comply with stringent seismic loading criteria.
Medium & Low Voltage Switchgear Cubicles
GCK, GCS, and MNS switchgear manufacturing demanding strict dimensional interchangeability for withdrawable drawer units, copper busbars, and internal partitions.
- ✔ Materials: 2.0–2.5 mm Al-Zn coated steel, high-conductivity electrolytic copper busbars.
- ✔ Key Processes: Multi-axis backgauge press brake bending, precision mounting hole laser cutting.
- ✔ Drawer Fit: Slide rail mounting clearances held within ±0.1 mm across modular compartments.
Comprehensive Workpiece Fabrication Capability Matrix
Compare sheet metal machine allocations, material thickness parameters, and achievable tolerances across primary electrical enclosure sub-assemblies.
| Enclosure Component | Standard Material | Thickness | Recommended Machinery | Key Precision Metric |
|---|---|---|---|---|
| Cabinet Door Panels | Cold-Rolled Steel / SS304 | 1.0 – 2.0 mm | Multilateral Panel Bender | Bending angle tolerance: ±0.2° with zero surface marring |
| Main Frame Uprights (9-Fold / 16-Fold) | High-Strength Galvanized Steel | 1.5 – 2.5 mm | CNC Press Brake / Custom Roll Forming | Straightness: ≤ 0.5 mm/m over 2.2 m vertical uprights |
| NEMA 4X Sharp-Corner Enclosures | AISI 304 / 316L Stainless Steel | 1.5 – 3.0 mm | CNC V Groover + Panel Bender | Outer radius < 0.3 mm; joint fit-up gap < 0.15 mm |
| Perforated Server Rack Skins | SPCC / Electro-Galvanized Sheet | 0.8 – 1.5 mm | High-Speed Fiber Laser Cutter | Hole pitch accuracy: ±0.03 mm without thermal distortion |
| Internal Mounting Backplates | Zinc-Plated Carbon Steel | 2.0 – 3.2 mm | Heavy-Duty CNC Press Brake | Full-bed mechanical crowning compensation over 3.2 m spans |
| Continuous Gasket Water Gutters | SS304 / Galvannealed Steel | 1.2 – 2.0 mm | Automated Panel Bender (Special Tooling) | Uniform 30% wider seating surface for automated PUR dispensing |
Need Custom Tooling or an Automated Cabinet Production Cell?
Share your cabinet, enclosure, door, or panel drawings with Haden. Our engineers can evaluate suitable machinery, tooling, process sequences, material handling, and automation configurations around your parts and production requirements.
Precision Metalworking Machinery Portfolio for Electrical Enclosure Manufacturing
Fabricating high-performance electrical enclosures demands structural rigidity, pristine scratch-free surfaces, and exact dimensional accuracy. Haden engineers an integrated equipment lineup of automated panel benders, CNC sheet metal V-groovers, industrial laser cutting machines, and synchronized press brakes tailored to achieve strict NEMA 4X, IP65, and IP66 production standards.
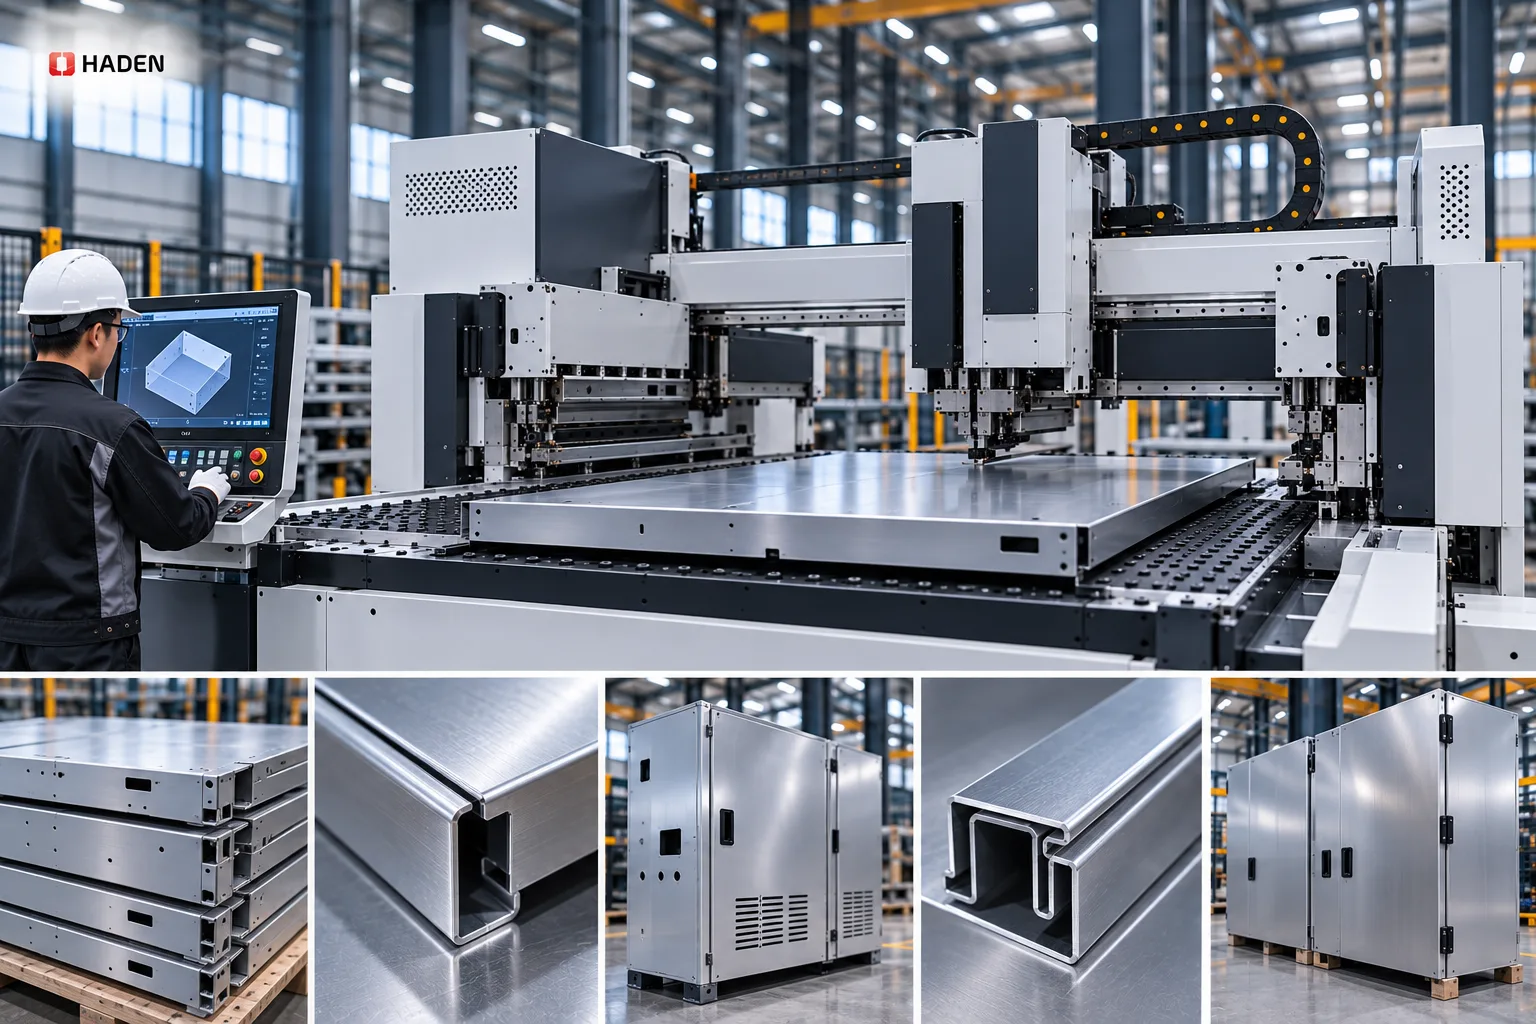
Multilateral Automatic Panel Benders for Enclosure Paneling & Doors
Engineered for continuous 4-sided positive and negative bending, Haden panel benders eliminate manual sheet manipulation and tool change downtime. Universal folding blades execute complex profiles, double hems, Dutch folds, and narrow polyurethane foam gasket channels in a single rapid automated sequence.
- Workpiece Scope: Control cabinet doors, side skins, top roof canopies, and modular enclosure covers.
- Material Compatibility: Galvanized steel, pre-painted sheets, cold-rolled mild steel, and stainless steel up to 2.5 mm.
- Scratch-Free Forming: Smooth oscillating bending motion prevents zinc flaking and leaves no die pressure marks.
Cabinet Fabrication Machinery Comparison Matrix
Evaluate machine capabilities across cycle times, suitable part geometries, and automation readiness to configure your production line.
| Equipment Category | Primary Enclosure Target Parts | Material Thickness | Production Rate | Sealing & Tolerance Role | Tooling Setup Mode |
|---|---|---|---|---|---|
Automatic Panel Bender
| Door panels, side walls, roof covers, shallow base trays | 0.5 mm – 2.5 mm | 20–35s / panel | Forms continuous return hems for polyurethane foam adhesion | Zero setup, automatic universal folding blades |
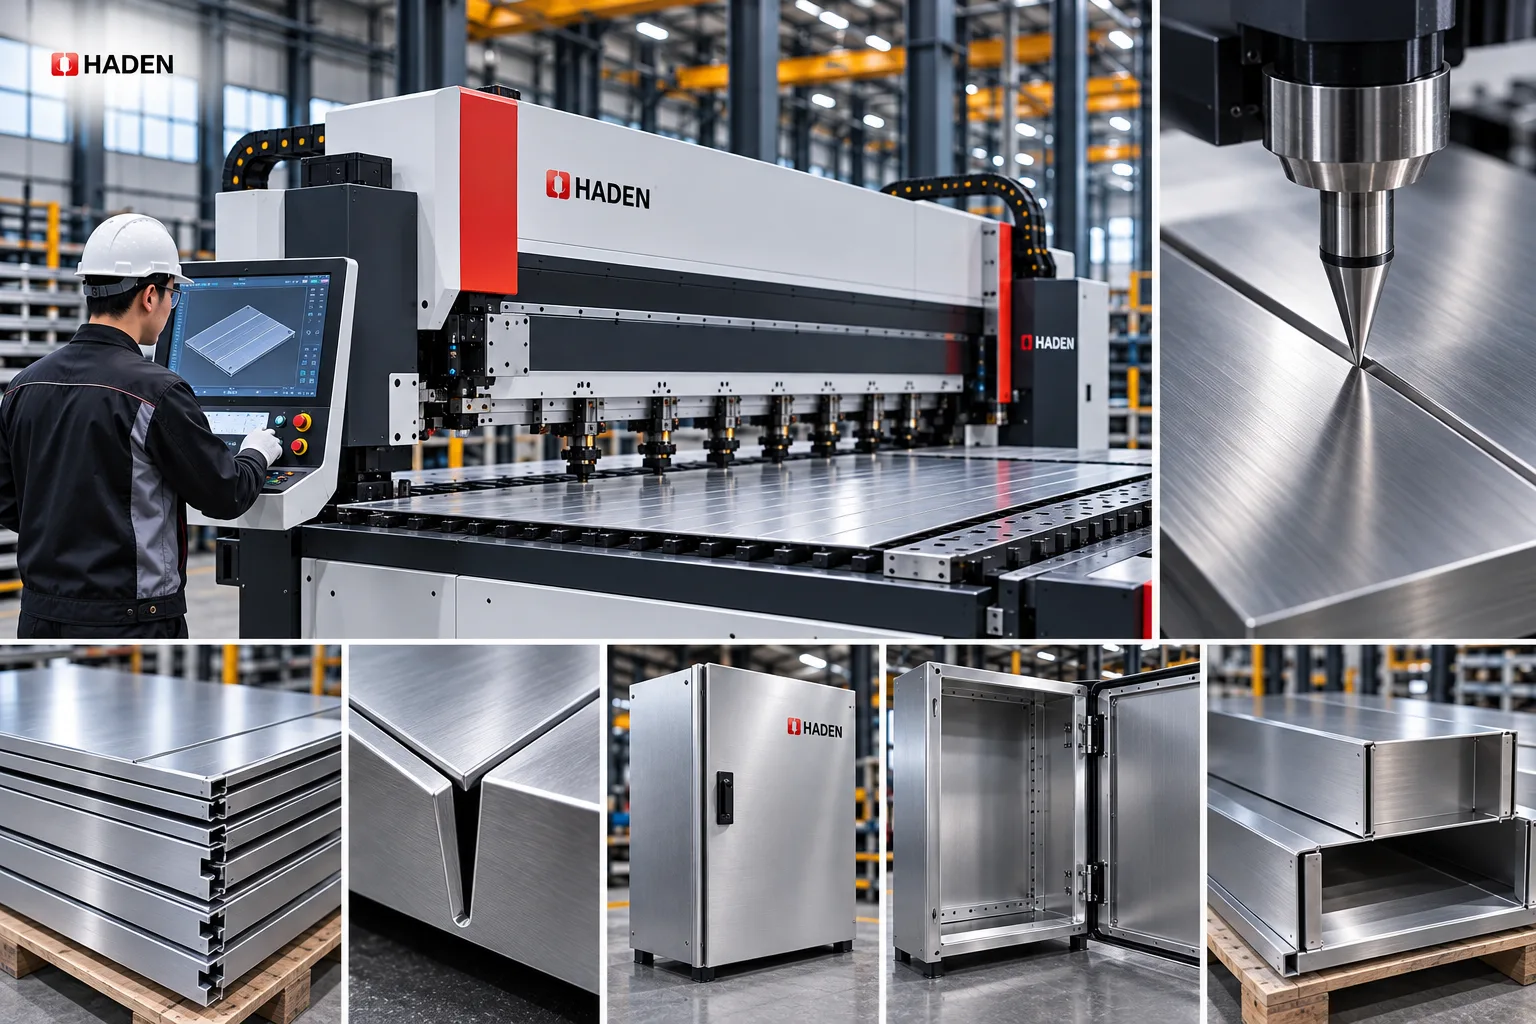
CNC Sheet Metal V-Groover
| Stainless 304/316 exterior bodies, architectural enclosure corners | 0.6 mm – 6.0 mm | 45–75 m/min feed | Zero-radius sharp corners, eliminates corner bulging for IP66 gaskets | Programmable CNC multi-blade depth offset |
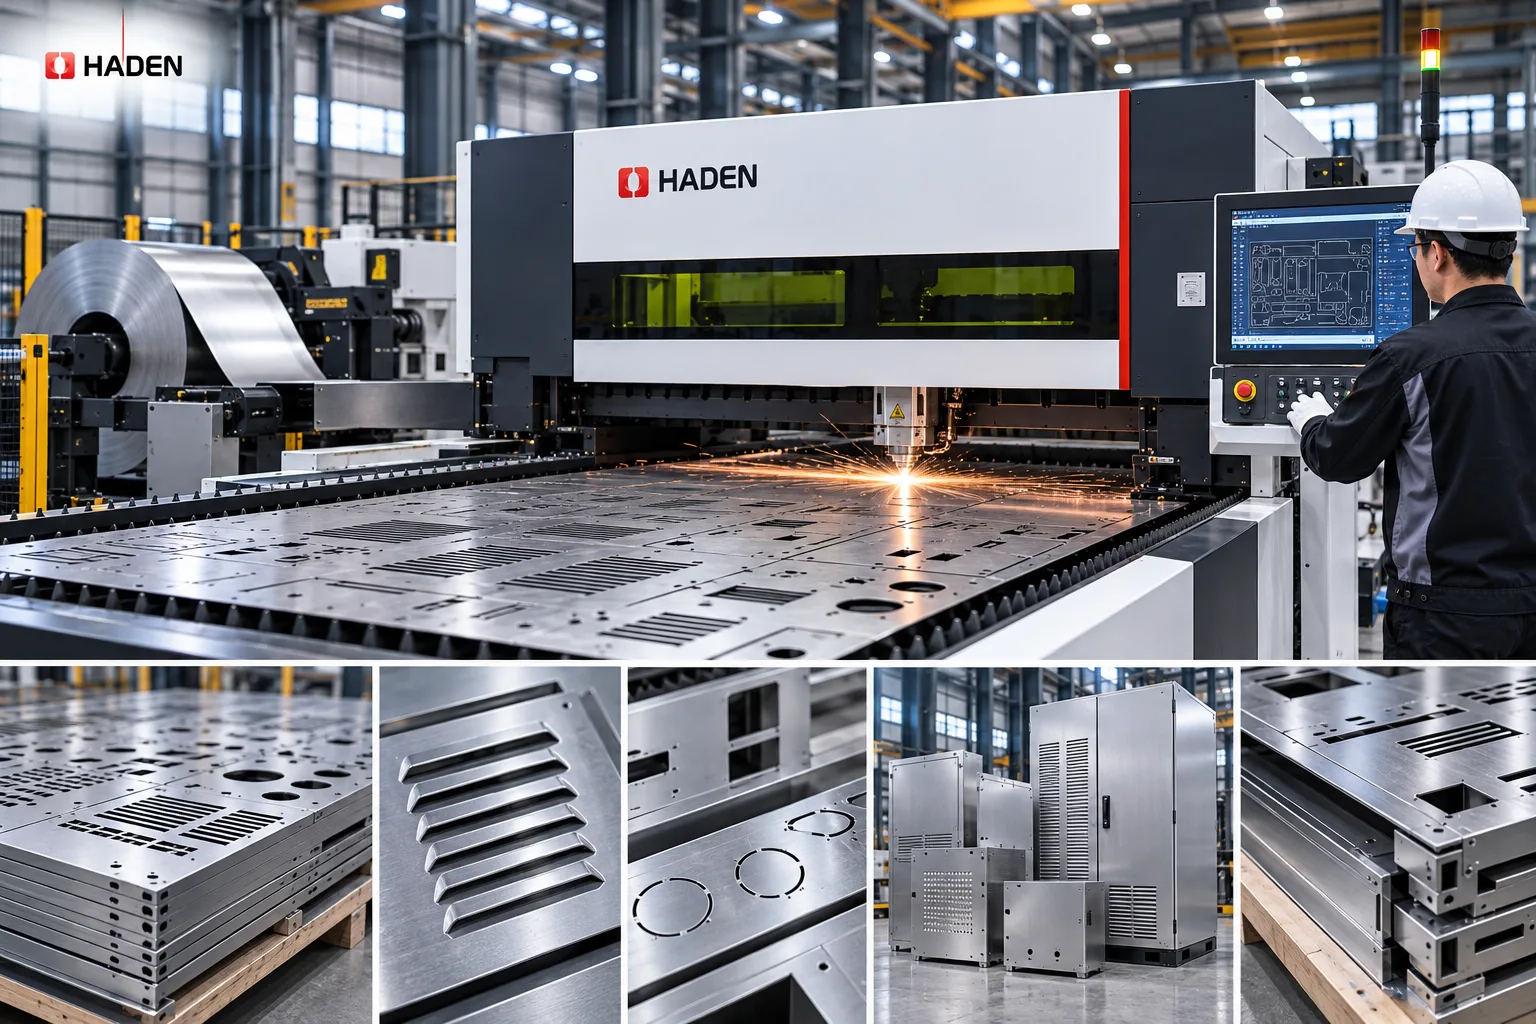
Precision Fiber Laser Blanker
| Mounting plates, louver arrays, knockout grids, blank skins | 0.5 mm – 16.0 mm | Up to 120 m/min | Positioning repeatability ±0.03 mm for hinge and latch alignment | Instant CAD/CAM software nesting changeover |
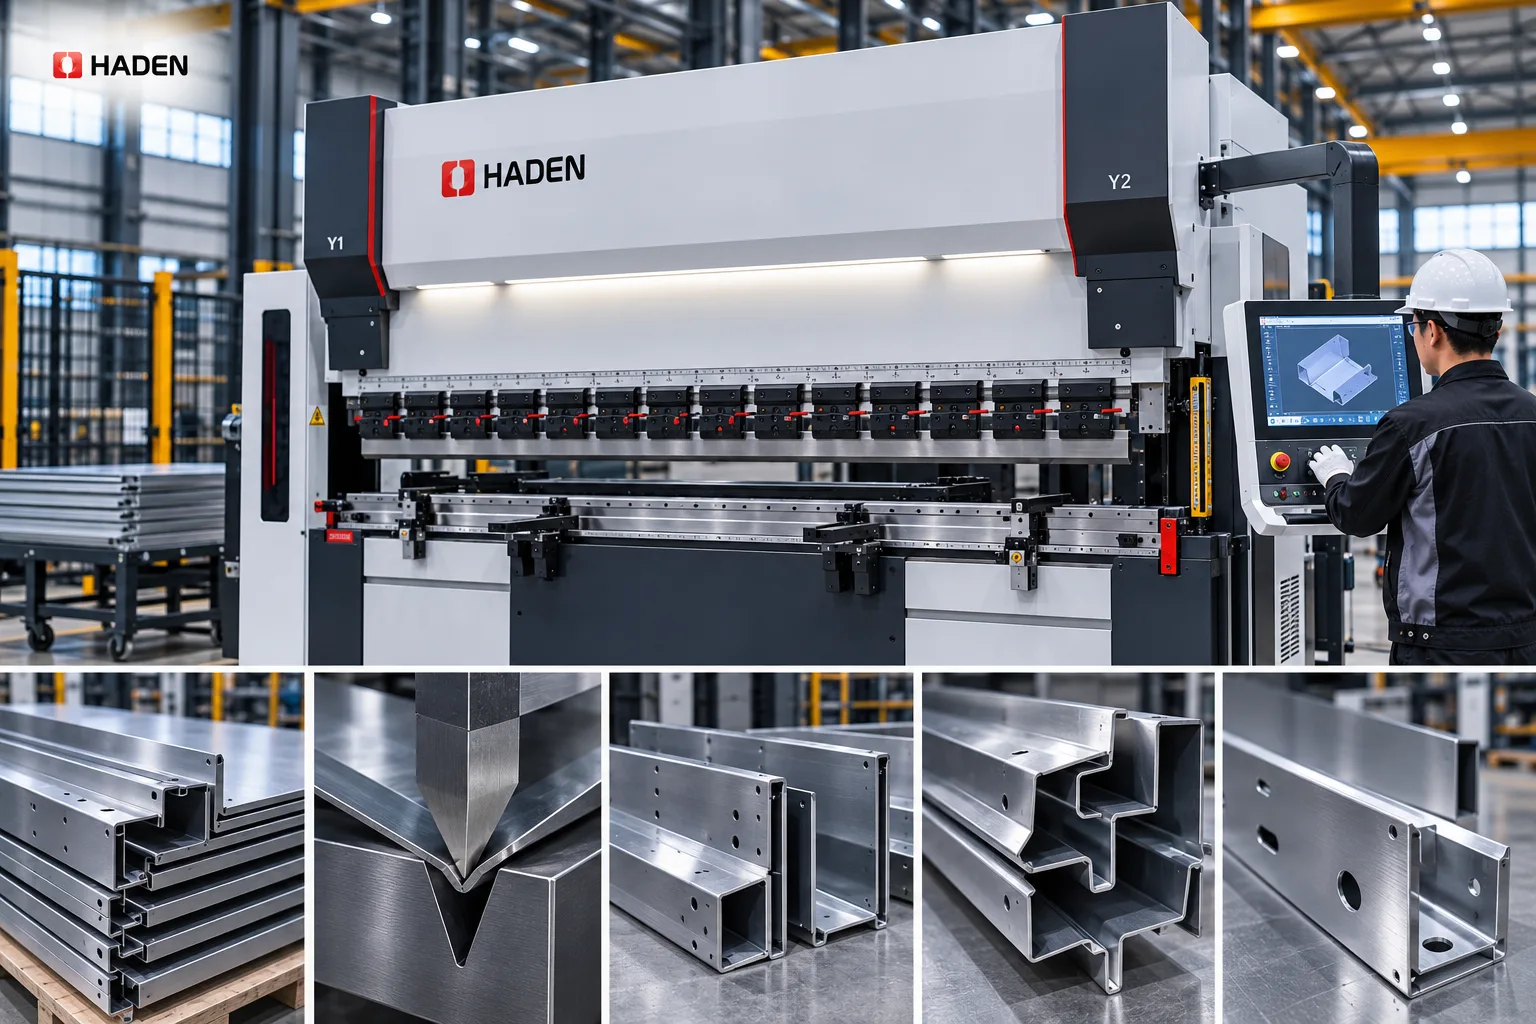
Multi-Axis CNC Press Brake
| 9-fold vertical pillars, heavy base plinths, deep transformer boxes | 1.0 mm – 12.0 mm | 12–18 strokes/min | Dynamic crowning prevents diagonal twist across 3000 mm frames | Hydraulic rapid-clamp precision standard tooling |
Unified Flexible Enclosure Manufacturing Cells
Connecting laser blanking, V-grooving, and panel bending through intelligent robotic material handling enables true Batch Size 1 automation. Fabricate high-mix custom electrical enclosures with minimal changeover and zero manual bottlenecks.
Direct Laser-to-Bend Link
Automated vacuum de-stackers transfer laser-cut blanks directly to panel bender centering tables with integrated vision orientation checks.
V-Groove & Fold Workcells
Synchronized transfer shuttles feed stainless sheets from CNC V-groovers into bending stations for instant sharp-corner forming.
Automatic Stud & Gasket Cell
Formed enclosure doors advance immediately to automated CNC capacitor discharge stud welding and inline cast-in-place PUR foaming.
Central MES Scheduling
Haden proprietary CAM software suites integrate with plant ERP systems, dispatching 3D bend profiles and laser cutting nesting plans on demand.
Overcoming Enclosure Fabrication Bottlenecks: Scratch-Free Bending and Zero-Radius Sharp Corners
Modern industrial control cabinets, outdoor power distribution units, and telecommunication racks require strict aesthetic surface integrity and tight structural tolerances. Conventional press brake tooling frequently introduces friction drag marks, unpredictable angular springback, and wide outer bend radii that compromise sealing gasket compression. Haden integrates servo-driven oscillating blade panel bending with high-speed CNC V-grooving to eliminate post-weld corner grinding, optimize polyurethane foam gasket adhesion, and secure verified IP66 and NEMA 4X performance on high-volume production lines.
Eliminates manual corner TIG welding, wire feeding, and abrasive blending on pre-grooved cabinet seams.
Real-time closed-loop deflection and material springback compensation across 0.5 mm to 2.5 mm sheet metals.
CNC V-groove micro-milling achieves tight, gap-free 45-degree miter returns on stainless and prepainted steel.
Friction-free rolling tool contact protects polished 304/316 stainless and galvannealed surfaces completely.
Automated Panel Bending for Friction-Free Forming
Traditional press brakes rely on vertical punch-and-die sliding penetration, inevitably creating die scrape marks, micro-cracks, and zinc flaking on coated metals. Haden multilateral automatic panel benders utilize universal servo-driven oscillating bending blades. The tooling executes a controlled rolling-contact path that transfers pure bending moment directly into the flange without lateral sliding friction.
- ✓
Zero Surface Galling: Shields zinc coatings on galvanized panels, prepainted powder layers, and No. 4 brushed stainless without requiring single-use protective film.
- ✓
Positive & Negative 4-Side Folding: Universal blade kinematics execute rapid upward, downward, and hemmed return folds on cabinet doors and side covers in a single automated cycle.
- ✓
Closed-Loop Sensor Compensation: Integrated thickness verification and laser angle feedback dynamically calculate rolling stroke adjustments to hold ±0.2° bend consistency.
CNC V Grooving for Sharp Edge Miters & IP66 Sealing Planarity
Standard sheet metal bending generates an external radius directly tied to sheet thickness (typically R ≥ 1.5 × T), producing rounded corner profiles that create localized corner gaps when doors mate with cabinet frames. Haden high-speed CNC V grooving machines pre-mill micro-notches along programmed bend lines, lowering local yield resistance and forming razor-sharp architectural profiles.
- ✓
Near-Zero External Radius (R ≤ 0.3 mm): Produces crisp, square-profile cabinet outer rims and flush modular enclosures that align cleanly across multi-bay cabinet suites.
- ✓
+30% Gasket Contact Sealing Surface: Flat, non-deformed miter edges create a true continuous plane for cast-in-place polyurethane (PUR) foam sealing paths under high-pressure hose-down tests.
- ✓
Engineered Web Thickness Retention: Precision depth control retains 40% to 50% of the core sheet thickness, preserving enclosure torsional strength while reducing bending tonnage requirements by up to 70%.
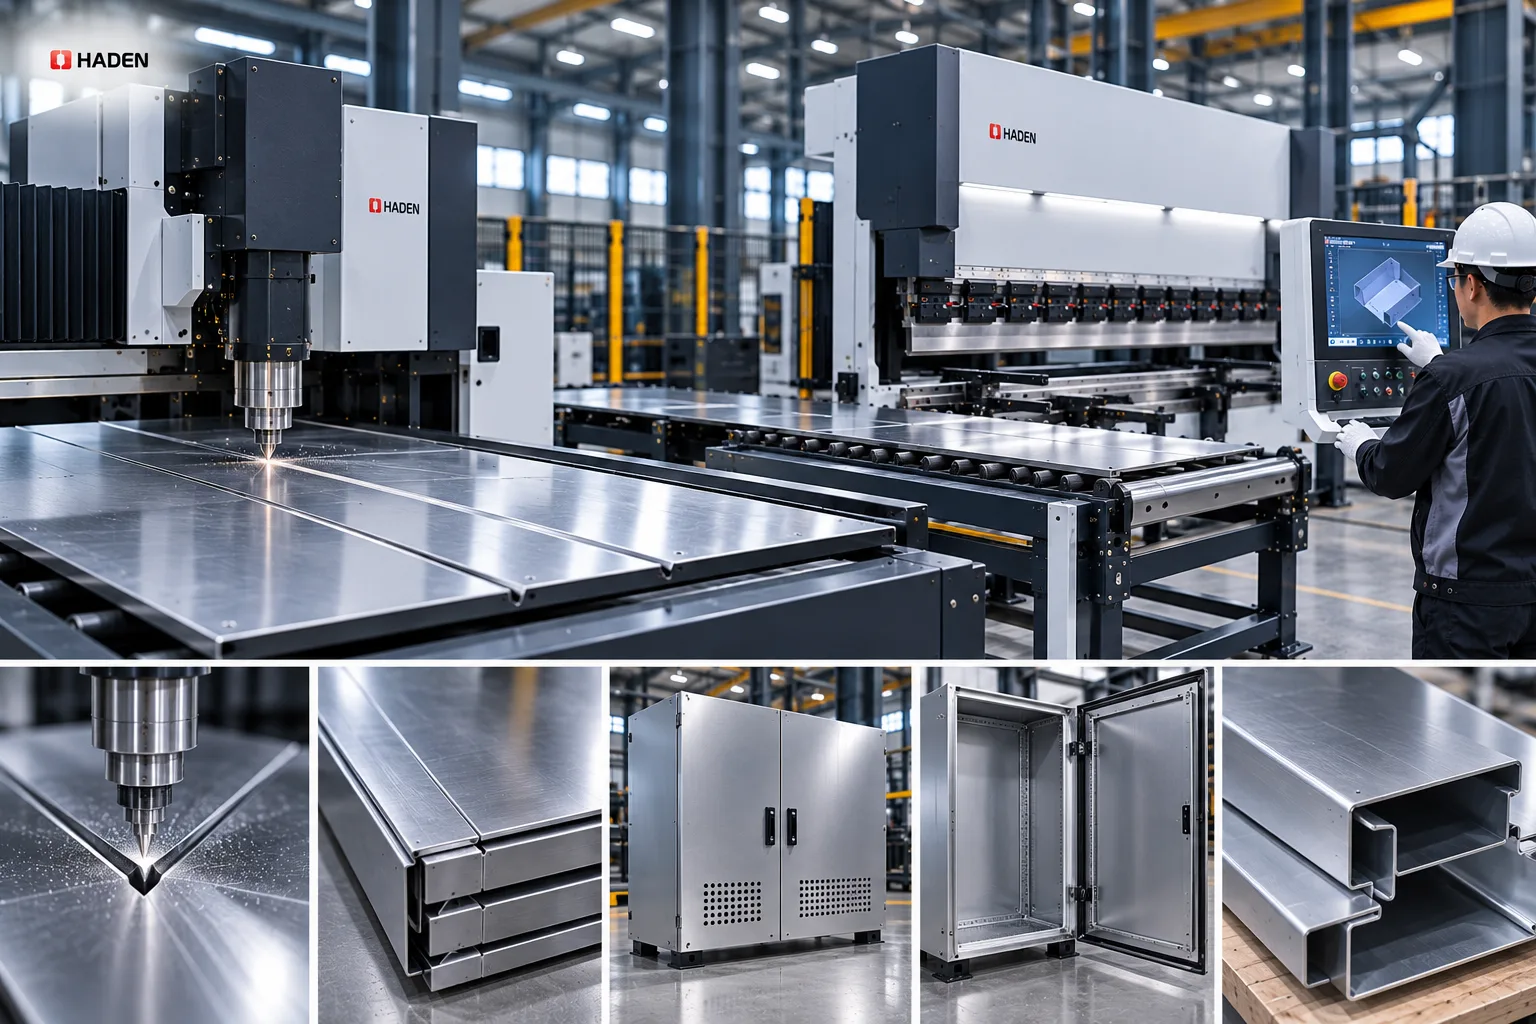
Harmonized V-Groove Milling and Panel Bending for High-Protection Cabinets
Coupling CNC V grooving with automated panel bending creates an agile fabrication loop. Laser-cut sheet blanks are routed along critical perimeter lines on the V-groover, fed into the panel bending cell, and formed into completed box structures in under 30 seconds. This workflow delivers the uniform planarity demanded by automated two-component polyurethane (PUR) continuous dispensing systems.
Forming Process Comparison: Conventional Press Brake vs. Haden Integrated Panel Solution
Compare key engineering metrics between manual press brake methods and Haden’s combined CNC V-grooving and automated panel bending technology.
| Process Parameter | Traditional Press Brake | Haden Panel Bender + V Groover | Fabrication Advantage |
|---|---|---|---|
| Surface Finish & Coating Protection | Friction die marks demand post-process polishing or protective films | 100% scratch-free rolling contact bending mechanics | Eliminates surface repair on stainless, galvannealed, and pre-coated sheets |
| Outer Bend Radius | R = 1.2 mm to 3.0 mm (dependent on sheet thickness and die V-opening) | R ≤ 0.3 mm (micro-milled sharp outer corner) | Tight exterior visual seam lines and flush multi-door cabinet alignment |
| Gasket Sealing Plane Geometry | Rounded flanges create irregular radius zones and potential leak paths | Uniform planar flange return with crisp 90-degree corners | 30% wider PUR foam contact width ensures reliable IP66 / NEMA 4X seals |
| Tool Setup & Program Changeover | 15 to 45 minutes of manual punch/die physical reconfiguration | 0 seconds (universal automatic segment positioning) | True Batch Size 1 mixed-model production for bespoke control panels |
| Corner Welding & Finishing Labor | Extensive corner seam filling, manual TIG bead deposit, and abrasive grinding | Ultra-tight 0.15 mm miter joints require only localized tack/laser stitch | Cuts corner post-weld grinding and polishing cycle time by over 60% |
| Cycle Time (4-Sided Door / Cover) | 90 to 150 seconds (manual repositioning and multi-stage handling) | 22 to 32 seconds (fully automated 4-axis servo manipulator) | 3x to 5x higher throughput per production shift with single-operator control |
Automated Electrical Enclosure Production Lines & Flexible Sheet Metal Systems
Eliminate discrete batch bottlenecks with synchronized, lights-out cabinet automation. Haden turnkey flexible manufacturing systems bridge continuous coil de-reeling, high-speed laser cutting machines for precision blanking, robotic transfer buffering, intelligent panel bending, and inline assembly. Purpose-built for industrial control cabinets, server racks, switchgear cubicles, and NEMA 4X / IP66 enclosures, our integrated production lines deliver consistent dimensional accuracy, scratch-free surface integrity, and instant batch size 1 changeover.
Eliminates manual sheet loading, inter-station pallet staging, and repetitive manual press brake tool repositioning.
Inline process flow removes buffer staging areas and excess work-in-progress (WIP) storage between cutting and folding.
Continuous cycle time to uncoil, laser cut louvers and mounting cutouts, sort blanks, and 4-side bend enclosure doors or wrappers.
Parametric CAM software communicates directly with universal panel bending tooling for zero-second profile changeovers.
5-Stage Automated Electrical Enclosure Manufacturing Process
Follow the synchronized path from raw steel coil to fully formed, certified electrical cabinets and chassis components.
Raw material handling begins with heavy-duty hydraulic decoilers supporting 5-ton to 15-ton coils of cold-rolled, galvanneal, and stainless steel. A multi-roll precision leveling unit eliminates residual coil set and cross-bow stresses, guaranteeing optimal flatness for subsequent processing on high-speed sheet metal laser cutting machines and precision folding units.

Modular Flexibility for High-Mix Cabinet Portfolios
Haden FMS architectures synchronize discrete fabrication stages through centralized supervisory control. Whether running 19-inch IT server rack doors, modular switchgear drawer units, or stainless-steel outdoor terminal boxes, the system dynamically routes workflows to prevent production bottlenecks.
- Zero-Scratch Surface Quality: Rolling-contact forming protects pre-painted coatings and stainless finishes.
- Inline V-Grooving Integration: Delivers sharp 90° corners and tight seam fits for premium control enclosures.
- Direct MES/ERP Handshake: Automated monitoring of scrap rates, cycle times, order queues, and overall equipment effectiveness (OEE).
Performance Comparison: Manual Workstations vs. Haden Turnkey Automation
Compare operational metrics between traditional standalone machine setups and fully integrated flexible manufacturing lines.
| Fabrication Metric | Conventional Manual Shop | Haden Integrated Flexible Line | Operational Impact |
|---|---|---|---|
| Changeover & Tool Setup | 15 – 45 min per punch/brake tooling change | 0 seconds (Universal automated tooling) | True Batch Size 1 capability |
| Sheet Material Utilization | 70% – 78% (Standard precut sheets) | 88% – 94% (Dynamic continuous coil nesting) | 15% - 18% raw steel cost savings |
| Labor Requirements | 6 – 10 skilled operators per shift | 1 – 2 supervisory technicians per line | 70% direct labor overhead reduction |
| Surface Scratch & Defect Rate | 3.5% – 5.0% (Manual sliding friction damage) | <0.2% (Vacuum handling & rolling blades) | Near-zero post-weld polishing labor |
| Sealing Tolerance (IP66/NEMA 4X) | ±0.5 mm to ±0.8 mm (Manual backgauge variance) | ±0.1 mm to ±0.15 mm diagonal fit-up | Uniform PUR gasket compression |
Engineered to Meet IEC 62208, UL 508A & NEMA 250 Tolerances
In electrical cabinet and control console manufacturing, structural rigidity and precise sealing channels are mandatory for maintaining ingress protection ratings. Haden integrated manufacturing solutions maintain continuous knife-edge gutter tolerances, exact multi-bend returns, and thermal stress-free perimeter blanks required for compliant low-voltage switchgear cubicles and outdoor weatherproof enclosures.
Submit your cabinet 3D STEP drawings. Our technical tooling engineers will provide a comprehensive line layout, cycle time simulation, and ROI audit within 48 hours.
Built to Meet IEC 62208, NEMA 250, and IP Code Manufacturing Tolerances
In heavy-duty electrical enclosure fabrication, meeting ingress protection ratings like IP65, IP66, and NEMA 4X is determined long before the sealing gasket is cured. Structural precision across industrial laser cutting machines, V-grooving, and panel bending dictates whether a finished cabinet maintains continuous seam compression or suffers from localized gasket distortion and micro-gapping.
Haden metalworking machinery is engineered around micron-level kinematic positioning, active deflection compensation, and frictionless forming technologies. By eliminating cumulative dimensional drift and protecting raw metallurgical coatings, our equipment ensures high-volume electrical enclosures achieve full compliance with global electrical safety, environmental protection, and mechanical impact standards.
Kinematic Precision for True Door & Frame Alignment
Door sagging, hinge binding, and unequal reveals are primary causes of seal failure in industrial control cabinets. Haden machinery integrates closed-loop linear encoders and multi-axis synchronizers that deliver exceptional dimensional repeatability across every production run.
- ✓ ±0.03 mm Repeatability: Laser cutouts for hinges, DIN rails, and interlocks align precisely without manual filing.
- ✓ ±0.2 mm Diagonal Tolerance: Multi-axis backgauging guarantees square frames across tall 2000 mm baying enclosures.
- ✓ Zero Latch Binding: Multi-point cam locks engage with consistent torque, preserving long-term compression.
Continuous Sealing Gutter Profiles for IP65 & IP66 Defense
High-pressure washdown environments (NEMA 4X / IP66) require continuous knife-edge drainage gutters and ultra-flat return flanges. Irregular bend angles create localized pressure drops that allow liquid penetration past polyurethane foam gaskets.
- ✓ Uniform Return Hems: Knife-edge gutter profiles provide continuous 100% compression beds for formed-in-place foam gaskets (FIPFG).
- ✓ Zero-Radius Miter Corners: CNC V-grooving creates tight 90-degree corner joints that eliminate corner welding blow-through.
- ✓ Hydraulic Deflection Compensation: Maintains linear straightness within 0.1 mm per meter on long water troughs.
Surface Integrity Protection for Anti-Corrosion Longevity
Micro-scratches on stainless steel or zinc-plated steel compromise corrosion barriers, causing premature oxidation in marine and chemical installations. Haden equipment incorporates specialized kinematics that preserve base metallurgical layers.
- ✓ Rolling Tool Kinematics: Panel bender blades roll smoothly over sheet surfaces instead of scraping under friction.
- ✓ Passivation Layer Security: 304 and 316L stainless protective oxide films remain completely intact during extreme bends.
- ✓ Non-Marking Die Sets: Urethane inserts and segmented tooling prevent flaking on prepainted and galvannealed stock.
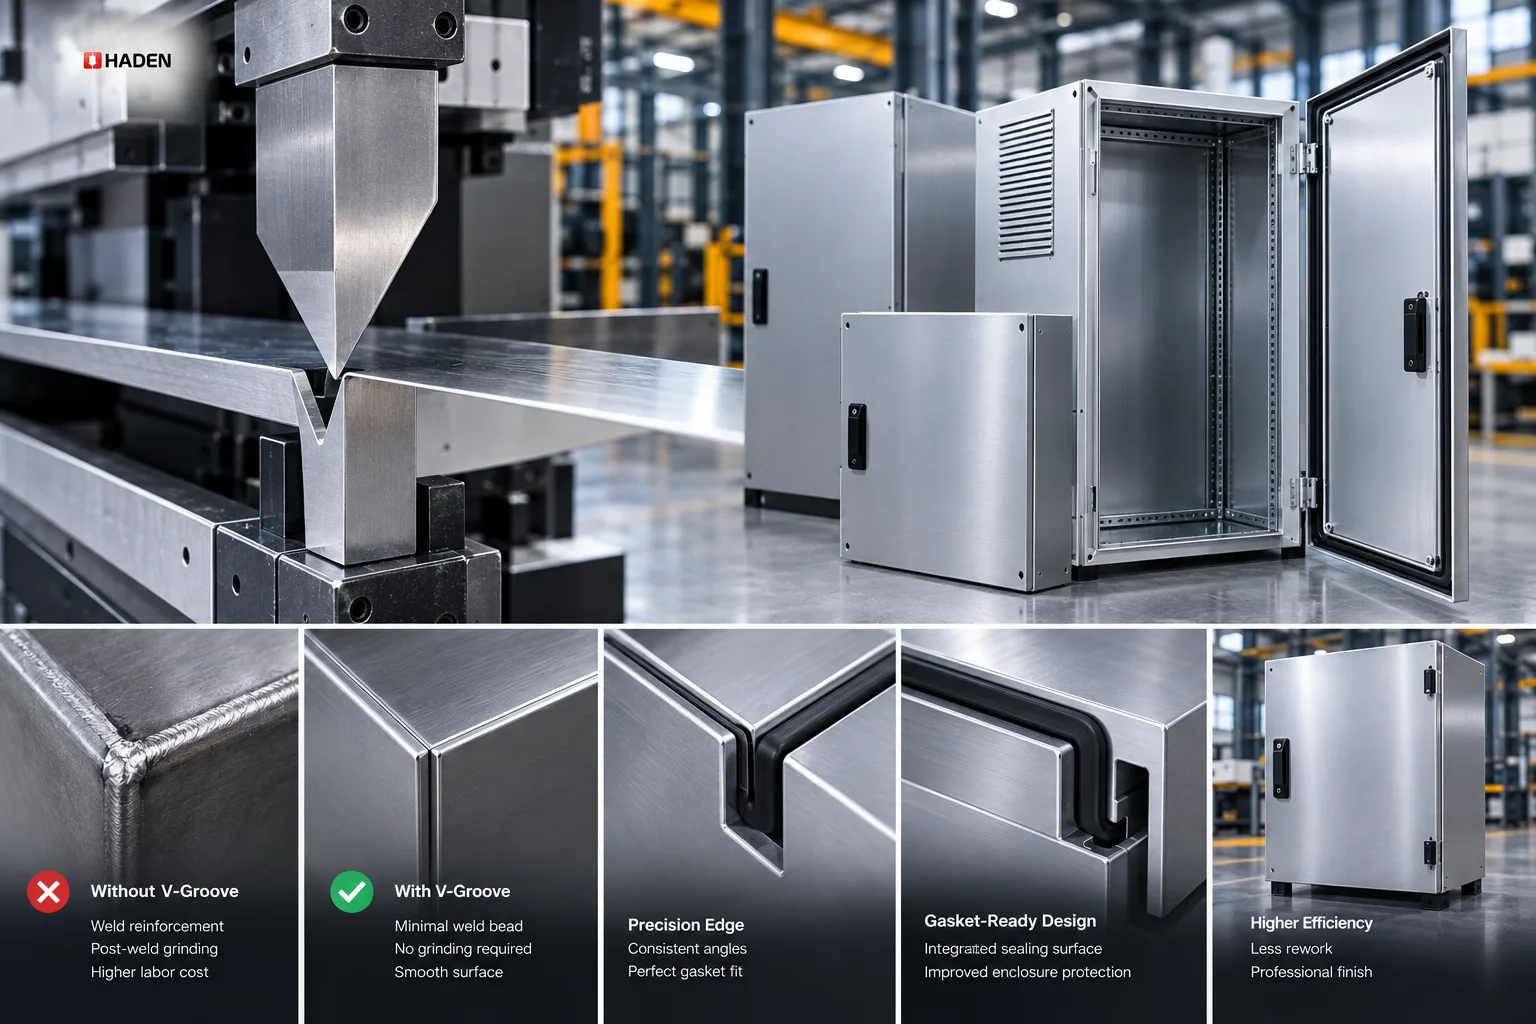
INSPECTION CRITERIA: Seam Gap ≤ 0.15 mm | Gasket Flange Planarity ≤ 0.1 mm/m
Eliminating Post-Weld Grinding and Gasket Rework
Traditional cabinet manufacturing relies heavily on manual fitting, corner seam welding, and labor-intensive weld grinding to achieve a clean outer edge. This process introduces localized heat distortion, damages raw sheet coatings, and creates unpredictable sealing surfaces.
By combining Haden high-speed CNC V-grooving with automated panel bending, manufacturers produce razor-sharp 90-degree corners with virtually zero outer radius. Mitered joints close tightly under mechanical tension, allowing automated TIG or laser corner welding without filler wire, cutting post-weld surface finishing labor by over 60%.
Manufacturing Standards to Machine Capability Matrix
Evaluate how Haden machine kinematics, CNC software intelligence, and specialized tooling directly translate into compliance with worldwide electrical enclosure certification standards.
| Industry Standard | Typical Application | Crucial Sheet Metal Requirements | Haden Machine Solution |
|---|---|---|---|
| IP55 / NEMA 12 | Indoor industrial automation, PLC racks, motor control centers | Dust resistance, light splash protection, consistent multi-bend door perimeter straightness | Automatic panel bender positive/negative cycling with continuous crowning compensation |
| IP65 / NEMA 4 | Outdoor power distribution boxes, traffic control, solar string combiner enclosures | Water jet resistance, continuous drain gutter profile, tight diagonal tolerance (±0.2 mm) | Universal bending tooling with automated angle compensation and micro-joint laser profiling |
| IP66 / NEMA 4X | Marine, coastal, food processing, and chemical washdown enclosures (304/316L Stainless) | Scratch-free surface integrity, zero-gap corner miters, ultra-flat FIPFG polyurethane gasket beds | High-speed CNC V-grooving for sharp edge forming + rolling non-friction panel bending |
| IEC 62208 / UL 508A | Modular low-voltage switchgear cubicles (Rittal TS8/VX25 style, GCK, MNS) | 9-fold and 16-fold structural uprights, high hole pitch repeatability (±0.03 mm), heavy busbar load rigidity | Multi-axis CNC hydraulic and electric press brakes with automated dynamic deflection crowning |
| NEMA 7/9 / ATEX | Explosion-proof hazardous location control cabinets and junction boxes | Heavy-gauge plate fabrication, precise deep-box side returns, flame-path gap tolerances < 0.1 mm | High-tonnage electric-hydraulic servo press brakes equipped with 6-axis custom backgauge fingers |
Hole positioning repeatability
Full closed-loop angle control
V-grooved fit-up tolerance
Scratch-free coating protection
Why Global Cabinet Fabricators Choose Haden Metalworking Equipment
Engineered specifically for demanding electrical enclosure and control cabinet manufacturing, our high-precision servo-electric press brakes and forming solutions pair heavy-duty machine rigidity with intelligent proprietary control systems to deliver repeatable precision and low unit costs.
Zero thermal or mechanical distortion under intensive multi-shift cycles
Single-setup milling guarantees micron-level geometric accuracy
Automated 3D bend simulation shortens programming and training
Encrypted real-time telemetry enables rapid remote troubleshooting
Heavy-Duty Annealed Monoblock Frames
High-tensile steel frames undergo high-temperature furnace annealing and stress-relief treatment, followed by precision machining on heavy 5-face milling centers to permanently eliminate structural deflection.
- Vibration-damped welded monoblock construction maintains long-term frame stability
- Precision-ground reference guides ensure consistent angular accuracy across all lengths
- High torsional rigidity prevents frame twisting during off-center or multi-station bending
Proprietary Enclosure CNC Operating System
Our specialized control software engineered for heavy-duty CNC hydraulic press brakes is configured around electrical enclosure workflows, delivering automated multi-flange sequencing, real-time collision simulation, and fast CAD-to-part execution.
- Instant bend sequence calculation directly from standard 3D STEP and DXF files
- Dynamic 3D collision detection prevents tool interference on deep box profiles
- Intuitive multi-touch interface accelerates daily operator onboarding and batch setups
Turnkey Co-Engineering & Tooling Support
Our application engineering team collaborates directly with cabinet manufacturers to develop tailored bending tooling, custom segmented dies, and specialized V-grooving cutters for non-standard enclosure geometry.
- Custom segmented tools designed for narrow return flanges and deep multi-tier boxes
- High-durability V-grooving inserts optimized for micro-radius stainless steel assemblies
- Process development support for outdoor weatherproof and IP66 gasket profile forming
Global Field Service & Remote Diagnostics
Haden provides comprehensive operational support through regional technical teams, rapid-dispatch wear-part centers, and encrypted cloud-connected diagnostics to safeguard plant productivity.
- Instant remote PLC and CNC diagnostics with secure end-to-end telemetry
- Strategic regional inventory hubs ensuring fast replacement component delivery
- Factory-trained field engineers offering turnkey commissioning and regular PM audits
Engineered for Precision, Scaled for Industrial Throughput
From single-door distribution boxes to high-density server racks and NEMA 4X stainless steel enclosures, Haden sheet metal laser cutting machines and metalworking machinery help fabricators eliminate fabrication bottlenecks, minimize scrap rates, and hold tight assembly tolerances across high-volume production schedules.
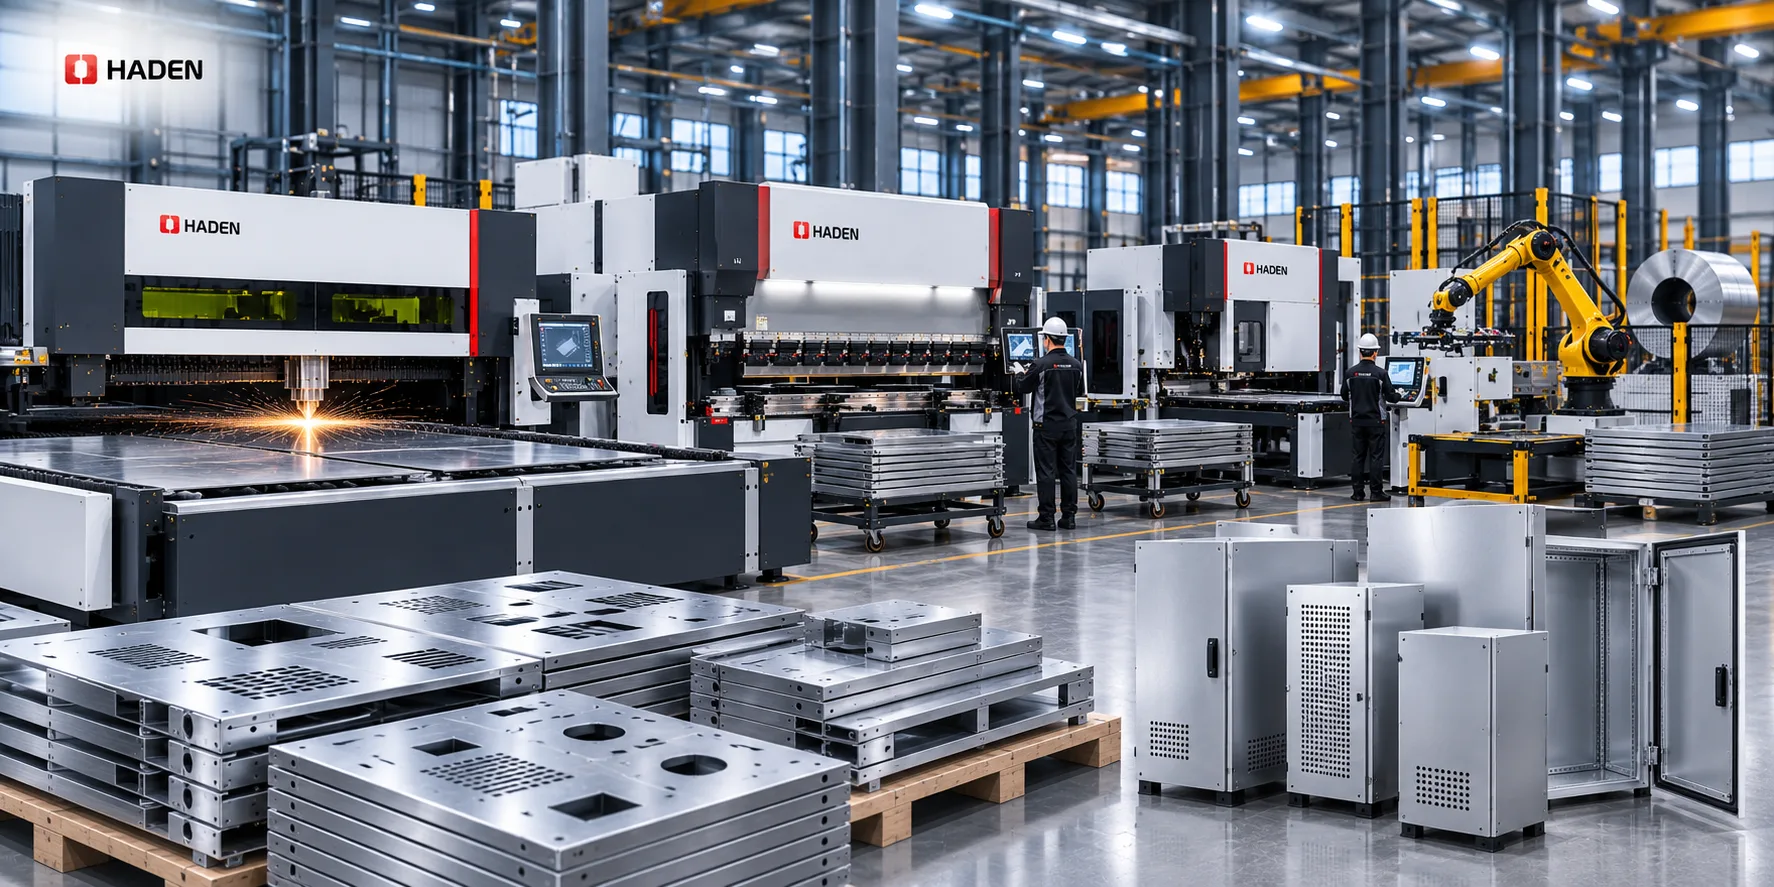
Electrical Cabinet Machinery Selection Guide and Engineering FAQs
Selecting the right sheet metal fabrication machinery for electrical enclosures requires balancing structural rigidity, rapid cycle times, seamless IP-sealing geometry, and agile batch changeovers. Whether configuring a high-volume automated line with high-precision sheet metal laser cutting machines for modular power distribution boxes or deploying a flexible cell for custom NEMA 4X control cabinets, matching machine kinematics to enclosure profiles maximizes capital efficiency and accelerates operational ROI.
Machinery Selection Matrix by Workpiece Profile
Evaluate core cutting, grooving, and forming technologies across electrical enclosure geometries, material gauges, and production volumes.
| Equipment Category | Primary Enclosure Target | Gauge Capacity | Tooling Setup Overhead | Key Production Advantage |
|---|---|---|---|---|
| Automatic Panel Bender | Cabinet doors, modular side panels, top canopies, shallow base pans (<250 mm / 10 in depth) | 0.5 mm – 2.5 mm (24–12 ga) CR / SS / AL | Zero Setup (Universal Servo Blade) | 3x–5x throughput versus press brakes; scratch-free rolling bend preserves pre-coated and galvanized finishes. |
| CNC Press Brake | High-moment 9-fold & 16-fold profiles, structural frames, deep switchgear wrappers, heavy mounting plates | 0.8 mm – 6.0+ mm Heavy Plate & Busbars | Tool Dependent (10–30 min Setup) | Multi-axis backgauge positioning with dynamic CNC crowning for continuous angle consistency on parts up to 4000 mm. |
| CNC V-Grooving Machine | Architectural control consoles, sanitary stainless cabinets, ultra-sharp IP66 / NEMA 4X gasket returns | 0.8 mm – 4.0 mm SS / AL / CR | Programmable CNC Indexing | Micro-radius outer edges; flat perimeter gasket planes; eliminates corner welding filler and grind labor. |
| Fiber Laser Cutting System | High-density ventilation louvers, DIN rail mounting arrays, meter cutouts, interlocking enclosure blanks | 0.5 mm – 12.0+ mm Sheet & Coil Stock | Instant (Digital Nesting Program) | High-frequency micro-pulse arrays prevent thermal warping while integrated coil-fed laser cutting machines boost material yield by up to 15%. |
The optimal fabrication line configuration pairs both machines based on workpiece geometry rather than treating them as mutually exclusive:
- Automated Panel Benders: Deliver maximum throughput for 4-sided enclosure door panels, modular side covers, top canopies, and shallow base trays up to 250 mm deep. The universal bending blades automatically adjust per bend line without physical tool changes, achieving single-panel cycle times under 30 seconds across cold-rolled and stainless steel thicknesses from 0.5 mm to 2.5 mm.
- CNC Press Brakes: Essential for heavy 3D structural skeletons, deep switchgear boxes exceeding 250 mm depth, high-moment 9-fold or 16-fold vertical frame profiles (Rittal TS8/VX25 styles), and internal copper busbar mounting plates over 3.0 mm.
Pairing an automated panel bender with a synchronized CNC press brake eliminates up to 80% of secondary staging bottlenecks in high-mix electrical enclosure shops.
Validate Cabinet Forming & Cycle Times
Verify machine capability on your exact workpiece geometry before finalizing machinery capital allocations.
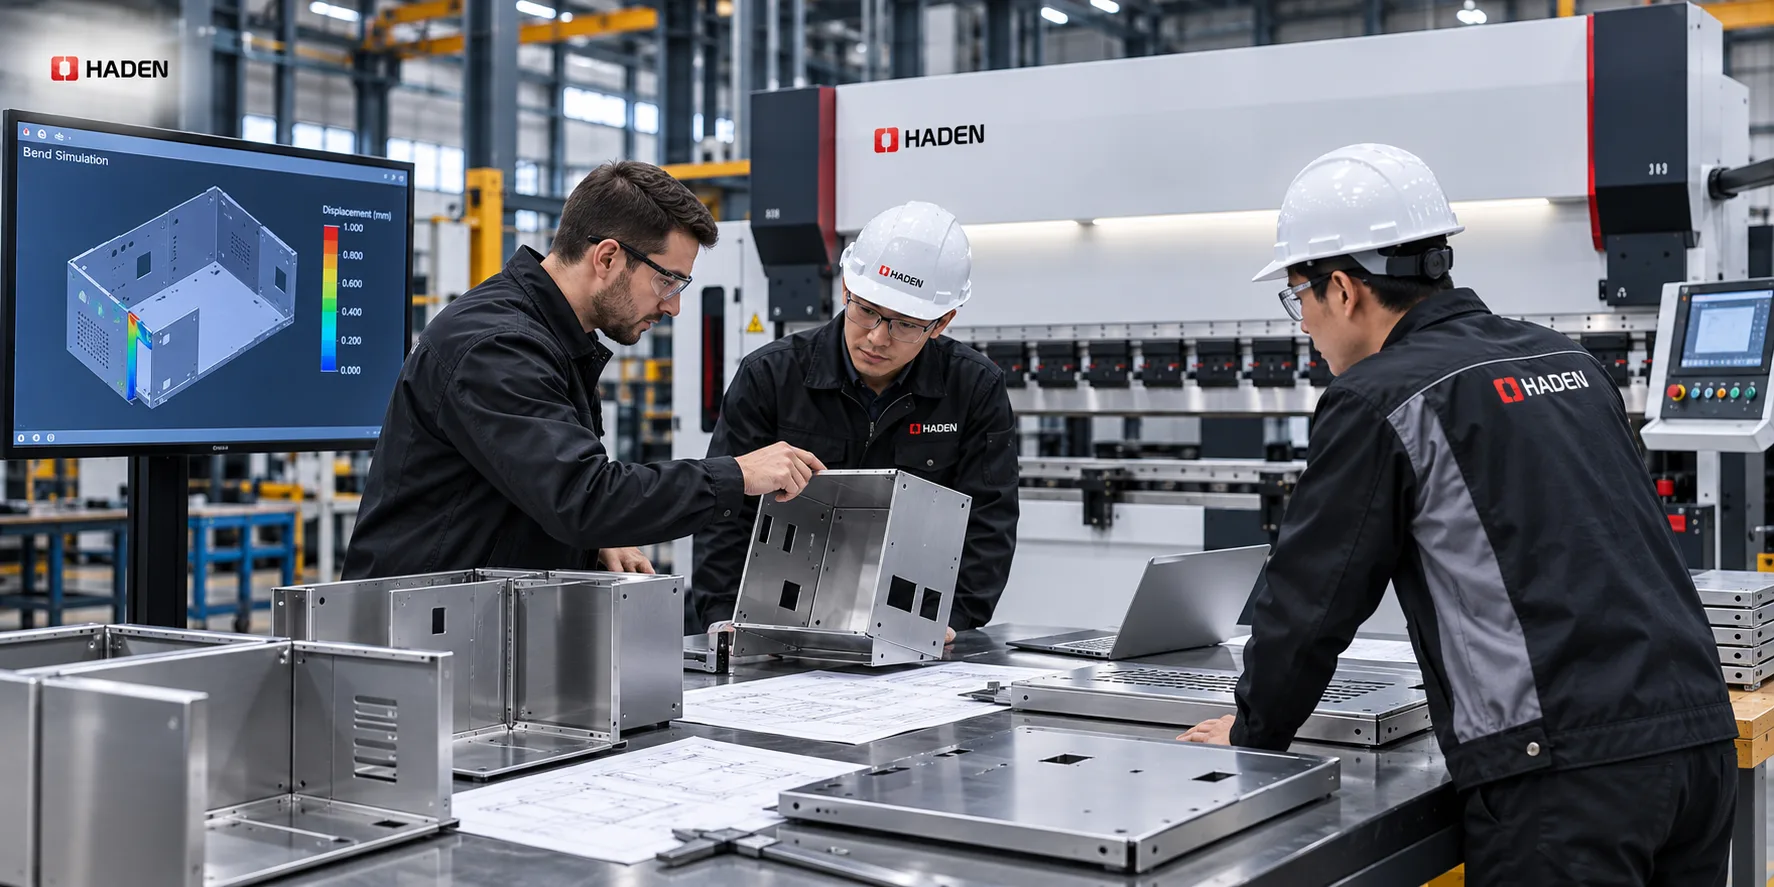
Haden sheet metal machinery supports strict structural, dimensional, and sealing tolerances for enclosures built to IEC 62208, NEMA 250 (Type 12, 4, 4X), and IP55 through IP66 industrial ratings.
Discuss Your Electrical Enclosure Manufacturing Project
Share your cabinet types, materials, dimensions, production targets, and current manufacturing process. Haden engineers can help evaluate suitable cutting, bending, panel forming, V-grooving, tooling, automation, and production-line configurations for your application.
Tell Us About Your Enclosure Production Requirements
Provide a brief overview of your parts and production needs. Our team can follow up for any additional technical information.
From Your Parts to a Machinery Configuration
Project requirements are reviewed around the parts you manufacture, the processes involved, and your production objectives.
Application Review
Review enclosure geometry, materials, thickness range, production volume, and manufacturing requirements.
Process & Equipment Configuration
Evaluate cutting, bending, panel forming, grooving, tooling, material handling, and automation requirements.
Technical Proposal
Develop a suitable machinery or production-line configuration based on the confirmed application requirements.
What to Share with Our Engineers
Control cabinets, electrical enclosures, doors, panels, frames, or other representative parts.
Material grades, sheet thickness, part dimensions, and surface requirements.
Production volume, product mix, process sequence, and automation targets.
Existing equipment, production bottlenecks, manual operations, or processes you want to automate.
Planning a Complete Enclosure Production Line?
Explore Haden solutions for integrated sheet metal processing, material flow, and production automation.
Explore Automated Production Lines